EP0119853A2 - Panier intermédiaire pourvu d'un élément chauffant pour métal liquide - Google Patents
Panier intermédiaire pourvu d'un élément chauffant pour métal liquide Download PDFInfo
- Publication number
- EP0119853A2 EP0119853A2 EP84301814A EP84301814A EP0119853A2 EP 0119853 A2 EP0119853 A2 EP 0119853A2 EP 84301814 A EP84301814 A EP 84301814A EP 84301814 A EP84301814 A EP 84301814A EP 0119853 A2 EP0119853 A2 EP 0119853A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- tundish
- channel
- heating device
- iron core
- induction
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000010438 heat treatment Methods 0.000 title claims abstract description 48
- 229910000831 Steel Inorganic materials 0.000 title abstract description 21
- 239000010959 steel Substances 0.000 title abstract description 21
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical group [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims abstract description 28
- 238000009749 continuous casting Methods 0.000 claims abstract description 15
- 239000011819 refractory material Substances 0.000 description 11
- 238000010276 construction Methods 0.000 description 4
- 239000000498 cooling water Substances 0.000 description 3
- 229910000805 Pig iron Inorganic materials 0.000 description 2
- 230000006698 induction Effects 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 230000006735 deficit Effects 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 238000007654 immersion Methods 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 229910052742 iron Inorganic materials 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 229910052751 metal Inorganic materials 0.000 description 1
- 230000002035 prolonged effect Effects 0.000 description 1
- 238000007670 refining Methods 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
- 210000002268 wool Anatomy 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/10—Supplying or treating molten metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D41/00—Casting melt-holding vessels, e.g. ladles, tundishes, cups or the like
- B22D41/005—Casting melt-holding vessels, e.g. ladles, tundishes, cups or the like with heating or cooling means
- B22D41/01—Heating means
-
- H—ELECTRICITY
- H05—ELECTRIC TECHNIQUES NOT OTHERWISE PROVIDED FOR
- H05B—ELECTRIC HEATING; ELECTRIC LIGHT SOURCES NOT OTHERWISE PROVIDED FOR; CIRCUIT ARRANGEMENTS FOR ELECTRIC LIGHT SOURCES, IN GENERAL
- H05B6/00—Heating by electric, magnetic or electromagnetic fields
- H05B6/02—Induction heating
- H05B6/16—Furnaces having endless cores
- H05B6/20—Furnaces having endless cores having melting channel only
Definitions
- This invention relates to a tundish provided with a heating device for molten metal, and more particularly to a tundish for continuous casting provided with a channeled induction-heating device for molten steel.
- molten steel is poured from a refining vessel such as converter or the like into a ladle, which is transported and poured into a tundish for continuous casting. Thereafter, molten steel is further poured into a mold through an immersion nozzle disposed in the bottom of the tundish. Therefore, the temperature of molten steel necessarily lowers in the course of transporting molten steel from the ladle to the mold through the tundish. Since the pouring temperature is very important in the continuous casting, however, it is desirable to use a tundish provided with a heating device for molten steel taking into consideration that the temperature of molten steel in the tundish may reduce below the predetermined pouring temperature.
- a low-frequency channeled induction-heating furnace usually called as an Ajax-Wyatt furnace.
- Such an induction-heating furnace has been known from old in the iron and steel field, which is mainly used as a holding furnace for foundary pig iron.
- a holding furnace is applied to the tundish used in the continuous casting of molten steel, however, there are fundamentally great differences as mentioned below:
- Fig. 1 is sectionally shown the tundish provided with the conventional channeled induction-heating device as mentioned above, which is also shown in Fig. 2 as a plan view.
- a channeled induction-heating device 1 is attached to a tundish 3 for the continuous casting at a position near the bottom of the sidewall thereof through a flange 5a of a shell 5 and a flange 7a of a shell 7.
- the induction-heating device 1 comprises an iron core 9 and a heating coil 11 wound around the iron core 9.
- a through-hole 13 receiving that portion of the iron core 9 which is surrounded with the heating coil 11.
- the inside of the shell 7 defining the device 1 is filled with a refractory material 15 containing a channel 17 therein.
- the channel 17 has a U-shape in plane surrounding the through-hole 13, both openings of which communicate with an opening 19 of the tundish 3 formed in the shell 5 and a refractory lining 21.
- the heating coil 11 is connected at both ends to water-cooled feed cables 23 and 25.
- the channel 17 is filled with molten steel 27 to form a closed loop (corresponding to a secondary induction coil). Further, molten steel 27 is heated to a predetermined temperature in the channel 17 by applying a voltage to the heating coil 11 (corresponding to a primary induction coil) through the cables 23, 25, during which molten steel 27 can be returned back to the tundish 3 through the channel 17 by the convection caused by electromagnetic heating.
- a voltage to the heating coil 11 corresponding to a primary induction coil
- a tundish for continuous casting comprising a tundish body and a channeled induction-heating device attached to a sidewall of said tundish body, said device including a channel communicated with an opening formed in said sidewall of the tundish body, an iron core and a heating coil wound around said iron core, the improvement wherein said iron core is a split-type iron core assembly composed of an upper core member and a lower core member, and said heating coil is wound around said lower core member.
- a tundish for continuous casting comprising a tundish body and a channeled induction-heating device attached to a sidewall of said tundish body, said device including a channel communicated with an opening formed in said sidewall of the tundish body, an iron core and a heating coil wound around said iron core, the improvement wherein said channel is opened at its upper portion to atmosphere, leaving a part of said channel near said sidewall of the tundish body closed.
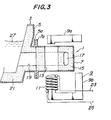
- Fig. 3 is sectionally shown a first embodiment of the tundish provided with the channeled induction-heating device according to the invention, which has the same construction as the conventional tundish of Fig. 1, except that the iron core 9 is divided into an upper core member 9a and a lower core member 9b and the heating coil 11 is wound around the lower core member 9b as shown in Fig. 3.
- the core members 9a, 9b are assembled with each other to form the iron core assembly 9 in use, so that the water-cooled feed cables 23, 25 can be always kept at a connected state to the heating coil 11 without requiring the detaching of the cables.
- Fig. 4 is shown an example of mounting the tundish of Fig. 3 onto a tundish car in the actual operation.
- the tundish car 30 comprises a car frame 32 provided at its bottom with plural travelling wheels 34, a pair of cylinders 36 arranged upright on both side portions of the car frame 32, and a frame 38 going up and down by the cylinders 36.
- the tundish 3 When the tundish 3 is mounted on the frame 38, it can be elevated up to a highest position as shown by a phantom line in Fig. 4.
- the upper core member 9a and the lower core member 9b defining the iron core assembly 9 are kept at the assembled state in the operation of the tundish 3, the upper core member 9a is first detached from the assembled state by means of a crane (not shown) when the tundish 3 is elevated upward after the use, while the lower core member 9b is kept leaving on a support stand 40 disposed on the car frame 32. Therefore, the water-cooled feed cables 23, 25 connected to the heating coil 11 surrounding the lower core member 9b are kept at the connected state in the detaching of the upper core member 9a.
- cables 23, 25 are connected to power and water sources (not shown) through a fitting member 42 fixed to one end of the car frame 32 and a pully 44 supported by a guide rail 46. Since these cables can not be bent at a small radius of curvature, they are properly fixed to the car frame 32 therealong.
- the iron core to be used in the channeled induction-heating device is a split-type iron core assembly composed of an upper core member and a lower core member, so that the removal of the iron core from the induction-heating device is very easy in the repairing of the tundish and the like.
- Figs. 5A to 5C a second embodiment of the tundish provided with the channeled induction-heating device according to the invention, which has the same construction as the conventional tundish of Fig. 1, except that the channel formed in the induction-heating device is opened at its upper portion to atmosphere, leaving a part of the channel near the sidewall of the tundish body closed.
- the channel 17 formed in the refractory material 15 is kept at a closed state in the induction-heating device 1 attached to the conventional tundish.
- a core is first set in the shell 5 at a position corresponding to the formation of a channel 17a and then the refractory material 15 is filled in the whole of the shell 5 and thereafter the core is dissolved in the refractory material 15 or removed off therefrom, whereby the upper portion of the channel 17a is opened to atmosphere so as to leave only a part of the channel 17a near the side wall of the tundish closed.
- the portion of the refractory material 15 closing the channel 17a has a size of y and z enough to support the upper portion of the remaining island-like refractory material 15 having the through-hole 13 for the iron core 9 therein without wobbling.
- the channel 17a may be covered with a lid (not shown) without being kept at an opened state or the upper portion of the opened channel 17a may be covered with a refractory wool instead of the lid.
- the channel is substantially opened at its upper portion, so that the inspection, preheating, local repairing and the like of the refractory material in the channel are very easy.
- the poor baking of the refractory material in the induction-heating device due to the poor preheating, so that the durable life of the refractory material can be prolonged.
- there is no risk of leaking molten steel from the deficit of the refractory material so that the safety of the operation can be ensured without troubles.
- the split-type iron core assembly and the opened channel are applied to the channeled induction-heating device, whereby the repair of this device can be performed more easily without difficulties.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Casting Support Devices, Ladles, And Melt Control Thereby (AREA)
- General Induction Heating (AREA)
- Furnace Details (AREA)
- Continuous Casting (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP39165/83U | 1983-03-18 | ||
| JP1983039165U JPS59143559U (ja) | 1983-03-18 | 1983-03-18 | 溶鋼加熱装置付き連鋳タンデイツシユ |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0119853A2 true EP0119853A2 (fr) | 1984-09-26 |
| EP0119853A3 EP0119853A3 (en) | 1985-05-22 |
| EP0119853B1 EP0119853B1 (fr) | 1988-12-07 |
Family
ID=12545506
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP84301814A Expired EP0119853B1 (fr) | 1983-03-18 | 1984-03-16 | Panier intermédiaire pourvu d'un élément chauffant pour métal liquide |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0119853B1 (fr) |
| JP (1) | JPS59143559U (fr) |
| KR (1) | KR900003546Y1 (fr) |
| AT (1) | ATE39072T1 (fr) |
| DE (1) | DE3475491D1 (fr) |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4735256A (en) * | 1985-02-21 | 1988-04-05 | Asea Ab | Heating apparatus for intermediate ladles or tundishes |
| DE4035552A1 (de) * | 1989-11-09 | 1991-05-16 | Fuji Electric Co Ltd | Vorrichtung zum erhitzen von geschmolzenem metall in einer giesspfanne |
| US5192488A (en) * | 1989-11-09 | 1993-03-09 | Fuji Electric Co., Ltd. | Apparatus for heating molten in a ladle |
| DE10058681B4 (de) * | 2000-11-25 | 2006-02-23 | Inductotherm Coating Equipment S.A. | Metallurgisches Gefäß zur Aufnahme einer Schmelze, Verfahren zum Wechsel einer Induktionsheizeinrichtung eines metallurgischen Gefäßes und Stopfen zum Verschließen eines Verbindungskanals |
| US8056608B2 (en) | 2008-04-25 | 2011-11-15 | Goodwin Plc | Method of mitigating against thermal contraction induced cracking during casting of a super Ni alloy |
| DE102014119109A1 (de) | 2014-12-18 | 2016-06-23 | Voestalpine Stahl Gmbh | Verteiler für Stranggießanlagen |
| CN108339969A (zh) * | 2017-04-14 | 2018-07-31 | 上海新研工业设备股份有限公司 | 分离式沟槽感应器 |
| DE102023132701B3 (de) | 2023-11-23 | 2025-03-20 | Voestalpine Stahl Gmbh | Stranggießanlage, Verteiler für Stranggießanlagen und Verfahren zum Stranggießen |
| WO2025109084A1 (fr) | 2023-11-23 | 2025-05-30 | Voestalpine Stahl Gmbh | Procédé de coulée d'acier et panier de coulée associé |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01224151A (ja) * | 1988-03-04 | 1989-09-07 | Kawasaki Steel Corp | タンディッシュ溶鋼加熱装置の操業後の冷却方法 |
| DE10159306A1 (de) * | 2001-12-04 | 2003-06-12 | Induga Industrieoefen Und Gies | Induktiv heizbares Gefäß für metallisches Schmelzgut und Verwendung dieses Gefäßes |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB757152A (en) * | 1954-07-05 | 1956-09-12 | Aldo Tagliaferri | Improvements in or relating to electric induction furnaces |
| US2888506A (en) * | 1957-06-17 | 1959-05-26 | Lindberg Eng Co | Salt bath furnace |
| DE1215833B (de) * | 1962-11-14 | 1966-05-05 | Bbc Brown Boveri & Cie | Induktions-Rinnen- oder Ring-Tiegelofen |
| DE1815265A1 (de) * | 1968-12-18 | 1970-02-26 | Bbc Brown Boveri & Cie | Giessverfahren und Einrichtung fuer induktiv beheizte Stopfenpfanne |
| JPS5857444B2 (ja) * | 1977-07-20 | 1983-12-20 | 大阪曹達株式会社 | 電解用陽イオン交換膜 |
| JPS57182099U (fr) * | 1981-05-14 | 1982-11-18 | ||
| JPS5835050A (ja) * | 1981-08-25 | 1983-03-01 | Kawasaki Steel Corp | 溶湯の加熱機能を有する連続鋳造用タンデイツシユ |
-
1983
- 1983-03-18 JP JP1983039165U patent/JPS59143559U/ja active Granted
-
1984
- 1984-03-16 AT AT84301814T patent/ATE39072T1/de not_active IP Right Cessation
- 1984-03-16 EP EP84301814A patent/EP0119853B1/fr not_active Expired
- 1984-03-16 DE DE8484301814T patent/DE3475491D1/de not_active Expired
- 1984-03-17 KR KR848402332U patent/KR900003546Y1/ko not_active Expired
Cited By (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4735256A (en) * | 1985-02-21 | 1988-04-05 | Asea Ab | Heating apparatus for intermediate ladles or tundishes |
| DE4035552A1 (de) * | 1989-11-09 | 1991-05-16 | Fuji Electric Co Ltd | Vorrichtung zum erhitzen von geschmolzenem metall in einer giesspfanne |
| GB2238496A (en) * | 1989-11-09 | 1991-06-05 | Fuji Electric Co Ltd | Ladle with apparatus for heating molten metal |
| US5164148A (en) * | 1989-11-09 | 1992-11-17 | Fuji Electric Corporation, Ltd. | Apparatus for heating molten metal in a ladle |
| US5192488A (en) * | 1989-11-09 | 1993-03-09 | Fuji Electric Co., Ltd. | Apparatus for heating molten in a ladle |
| GB2238496B (en) * | 1989-11-09 | 1994-07-06 | Fuji Electric Co Ltd | Apparatus for heating molten metal in a ladle |
| DE10058681B4 (de) * | 2000-11-25 | 2006-02-23 | Inductotherm Coating Equipment S.A. | Metallurgisches Gefäß zur Aufnahme einer Schmelze, Verfahren zum Wechsel einer Induktionsheizeinrichtung eines metallurgischen Gefäßes und Stopfen zum Verschließen eines Verbindungskanals |
| US8056608B2 (en) | 2008-04-25 | 2011-11-15 | Goodwin Plc | Method of mitigating against thermal contraction induced cracking during casting of a super Ni alloy |
| DE102014119109A1 (de) | 2014-12-18 | 2016-06-23 | Voestalpine Stahl Gmbh | Verteiler für Stranggießanlagen |
| WO2016096596A1 (fr) | 2014-12-18 | 2016-06-23 | Voestalpine Stahl Gmbh | Répartiteur pour installations de coulée continue |
| DE102014119109B4 (de) | 2014-12-18 | 2018-12-13 | Voestalpine Stahl Gmbh | Verteiler für Stranggießanlagen |
| US10632527B2 (en) | 2014-12-18 | 2020-04-28 | voestalpine Stalh GmbH | Tundish for a continuous casting plant |
| CN108339969A (zh) * | 2017-04-14 | 2018-07-31 | 上海新研工业设备股份有限公司 | 分离式沟槽感应器 |
| DE102023132701B3 (de) | 2023-11-23 | 2025-03-20 | Voestalpine Stahl Gmbh | Stranggießanlage, Verteiler für Stranggießanlagen und Verfahren zum Stranggießen |
| WO2025109084A1 (fr) | 2023-11-23 | 2025-05-30 | Voestalpine Stahl Gmbh | Procédé de coulée d'acier et panier de coulée associé |
| WO2025109083A1 (fr) | 2023-11-23 | 2025-05-30 | Voestalpine Stahl Gmbh | Procédé de coulée continue |
| WO2025109082A1 (fr) | 2023-11-23 | 2025-05-30 | Voestalpine Stahl Gmbh | Installation de coulée continue, panier de coulée pour installations de coulée continue et procédé de coulée continue |
Also Published As
| Publication number | Publication date |
|---|---|
| KR900003546Y1 (en) | 1990-04-28 |
| EP0119853B1 (fr) | 1988-12-07 |
| DE3475491D1 (en) | 1989-01-12 |
| EP0119853A3 (en) | 1985-05-22 |
| JPS6347399Y2 (fr) | 1988-12-07 |
| JPS59143559U (ja) | 1984-09-26 |
| ATE39072T1 (de) | 1988-12-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0119853B1 (fr) | Panier intermédiaire pourvu d'un élément chauffant pour métal liquide | |
| EP0439900A2 (fr) | Appareil de chauffage à induction et procédé | |
| DK0403808T3 (da) | Neddykningsstøberør til tilførsel af stålsmelte i en strengstøbekokille | |
| US3311361A (en) | Induction furnace | |
| US3971547A (en) | Apparatus and method for refining metal | |
| US4735256A (en) | Heating apparatus for intermediate ladles or tundishes | |
| JPS62267063A (ja) | 取鍋/タンデイツシユ | |
| JPS6339343B2 (fr) | ||
| US4931090A (en) | Pneumatic steelmaking vessel and method of producing steel | |
| US2962278A (en) | Holding apparatus for molten metals | |
| JPS6440155A (en) | Metallurgical treating apparatus in tundish for continuous casting | |
| US3189315A (en) | Teeming gate with consumable anti-splash shield | |
| KR20000014356U (ko) | 턴디쉬 스토퍼 예열용 화염안내장치 | |
| US3495812A (en) | Apparatus for removing and handling covers for converters or crucibles and for renewing the refractory lining | |
| US5799718A (en) | Device and frame for preheating a metal casting channel | |
| JPH1043840A (ja) | 金属ストリップ鋳造方法及び装置 | |
| US4276082A (en) | Process for the heating and/or melting of metals and an induction furnace to carry out the process | |
| US4323108A (en) | Tundish and process for casting from charge to charge in continuous steel foundry | |
| JPS60244452A (ja) | 溶融金属保持容器の誘導加熱器保守用支持装置 | |
| JPS6347402Y2 (fr) | ||
| US1347984A (en) | Hot-metal ladle-car | |
| JP5258149B2 (ja) | 転炉設備の操業方法 | |
| JPS61103653A (ja) | タンデイツシユのスラグ除去方法 | |
| JP2856075B2 (ja) | 連続鋳造機のタンディッシュ使用方法,改造方法および鋳込床設備 | |
| US3734164A (en) | Installations for the electroslag remelting of metallic consumable electrodes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): AT DE FR GB SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): AT DE FR GB SE |
|
| 17P | Request for examination filed |
Effective date: 19851120 |
|
| 17Q | First examination report despatched |
Effective date: 19861029 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT DE FR GB SE |
|
| REF | Corresponds to: |
Ref document number: 39072 Country of ref document: AT Date of ref document: 19881215 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3475491 Country of ref document: DE Date of ref document: 19890112 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| EAL | Se: european patent in force in sweden |
Ref document number: 84301814.4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19980309 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19980310 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19980311 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19980317 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19980320 Year of fee payment: 15 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990316 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990316 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990317 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 84301814.4 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19990316 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19991130 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 84301814.4 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000101 |