EP0299946A1 - Feuerfeste Buchse einer Transportrolle für ein warmes Metallprodukt und Verfahren zur Herstellung derselben - Google Patents
Feuerfeste Buchse einer Transportrolle für ein warmes Metallprodukt und Verfahren zur Herstellung derselben Download PDFInfo
- Publication number
- EP0299946A1 EP0299946A1 EP88870123A EP88870123A EP0299946A1 EP 0299946 A1 EP0299946 A1 EP 0299946A1 EP 88870123 A EP88870123 A EP 88870123A EP 88870123 A EP88870123 A EP 88870123A EP 0299946 A1 EP0299946 A1 EP 0299946A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- refractory
- sleeve
- bodies
- mold
- refractory material
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F27—FURNACES; KILNS; OVENS; RETORTS
- F27D—DETAILS OR ACCESSORIES OF FURNACES, KILNS, OVENS OR RETORTS, IN SO FAR AS THEY ARE OF KINDS OCCURRING IN MORE THAN ONE KIND OF FURNACE
- F27D3/00—Charging; Discharging; Manipulation of charge
- F27D3/02—Skids or tracks for heavy objects
- F27D3/026—Skids or tracks for heavy objects transport or conveyor rolls for furnaces; roller rails
Definitions
- the present invention relates to a refractory sleeve for a roller for transporting a metallic product at high temperature.
- the cold rolled steel strip In a continuous annealing furnace, the cold rolled steel strip generally enters at room temperature and it is brought, under a protective atmosphere, to the required temperature which is frequently above about 700 ° C. It gradually undergoes this heating by traveling a sinuous trajectory defined by a series of rotating guide rollers. During the last part of this trajectory, the strip is maintained at the desired temperature and it is the seat of metallurgical phenomena, in particular a recrystallization of its structure, before leaving the furnace towards the subsequent stages of its treatment.
- the temperature of the strip may be higher than the temperature of the guide rollers. This difference can be due to various causes, for example the arrival of a hot strip on a colder roller when the width of the strip changes, or heterogeneities in the heat transfer between the strip and these rollers. .
- the strip undergoes local cooling and consequently localized contractions in areas which are thus subjected to the entire tensile force which ensures the progression of the strip.
- the elastic limit of steel can be exceeded in these zones which are then the seat of plastic deformations resulting in "thermal undulations" (heat buckling) during cooling of the strip.
- GB-A-1,389,852 describes a roller for a continuous heat treatment oven, which consists of a metal core surrounded by a sleeve of refractory material based on fused silica.
- Patent application EP-A-0090428 raises a roller for a continuous annealing installation, consisting of a metal core coated with a layer of cermet at niobium.
- the present invention relates to a refractory sleeve for a roller for transporting a metal product at high temperature, in particular in a continuous annealing furnace, which has certain advantages over already known devices; it makes it possible, among other things, to avoid the appearance of local thermal deformations and surface defects in the transported product, while having a long service life thanks to a sufficient mechanical strength to prevent its cracking and a high resistance to abrasion.
- the present invention provides a refractory sleeve for a transport roller having a small contact surface with the product transported.
- the refractory sleeve for a roller for transporting a high-temperature steel product is characterized in that its outer lateral surface has a plurality of gradations defining an alternation of raised zones and of hollow zones and that the radially highest points of said raised areas define a cylindrical surface coaxial with said sleeve.
- the sleeve is constituted by a hollow cylindrical part made of a first refractory material, furnished with a plurality of bodies made of a second refractory material, partially embedded in the outer surface layer of said hollow cylindrical part.
- Said bodies can have any shape without leaving the part of the present invention. It is however preferable that their shape is regular, in particular spherical or cylindrical.
- the end surfaces of the cylinders can be planar or curved and in particular spherical.
- the bodies are spherical balls, they are preferably contiguous and arranged either in squares or in staggered rows; if they consist of cylinders, these are preferably aligned along external generatrices of the sleeve, with their end surfaces contiguous or spaced, said cylinders also being able to be offset transversely relative to the another between two neighboring cylinder lines.
- said first refractory material constituting the hollow cylindrical part, is advantageously a concrete with a high alumina content (Al2O3) and preferably of so-called “tabular" alumina.
- said second refractory material, constituting said bodies is advantageously a ceramic material having a high abrasion resistance, preferably composed of very pure alumina (Al2O3), isostatically pressed and sintered.
- said raised zones are constituted by portions of the external lateral surface of said sleeve, while the hollow zones are constituted by cavities cut in said external lateral surface.
- These recessed areas may be separate cavities hollowed out in the surface of said sleeve and therefore surrounded by a single raised area; these recessed areas can also be formed by a network of grooves, which surround a plurality of individual raised areas forming part of the external lateral surface of said sleeve.
- At least the outer surface layer of said sleeve is made of a refractory material having a high resistance to abrasion.
- said raised areas and therefore also said hollow areas, and in particular said bodies are distributed in a regular manner in the external lateral surface of the hollow cylindrical part.
- Such a distribution makes it possible to offer a support as homogeneous as possible for the product such as a steel strip, transported by the roller equipped with said sleeve.
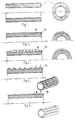
- FIG. 1 there is shown a refractory sleeve 1 for a transport roller of the prior art.
- the outer lateral surface of the sleeve 1 is substantially smooth and gives rise to the drawbacks mentioned above.
- Figures 2 to 5 show fragments of refractory sleeves 1 made in accordance with different variants of the present invention.
- FIG. 2 shows such a sleeve 1a carrying spherical balls 2, preferably contiguous, partially embedded in the refractory material of the sleeve.
- the penetration depth of the balls 2 in the refractory material is advantageously between 1.2 times and 1.8 times the radius of said balls, so as to guarantee the stability of their positioning in the sleeve.
- the diameter and the number of balls are in principle arbitrary. However, the number of balls should be sufficient to offer uniform support to the moving steel strip; this number should not however be too high, otherwise the sleeve would in practice approach the conventional sleeves of FIG. 1.
- a number of balls between 5 balls / dm2 and 500 balls / dm2 makes it possible to offer the strip sufficient support without inducing the aforementioned risk of deformation of the strip.
- These numbers of balls per unit area correspond substantially to ball diameters of 5 mm to 50 mm and assume that the balls are contiguous.
- a diameter of beads of the order of 10 mm to 25 mm has proved to be interesting. In the case of 10 mm diameter beads, their number is approximately 115 beads / dm2.
- the spherical balls 2 can be arranged in any desired manner; the most frequent arrangements are however the square arrangement and staggered arrangement.
- FIG. 3 illustrates another variant of refractory sleeve 1b in accordance with the invention, in which the bodies are constituted by cylindrical elements 3, of a length between 10 mm and 50 mm and of identical diameter with shaped ends. spherical caps. Similarly to Figure 2, these cylindrical bodies penetrate to a depth between 1.2 times and 1.8 times the radius of their cylindrical part.
- These cylindrical elements are aligned with their longitudinal axis parallel to the longitudinal axis of the sleeve. They are preferably contiguous in the same line and two adjacent lines are preferably contiguous, while possibly being offset longitudinally by a fraction of the length of one of said cylindrical elements.
- FIG. 4 shows, in longitudinal section and in perspective, a cylindrical sleeve 1c, the lateral surface of which is divided into zones 4, preferably regular, by means of a network of grooves 5.
- a network of substantially square meshes has been shown here , which also leads to substantially square zones 4. It is however obvious that the meshes of this network can have any shape and orientation. They can be wide.
- FIG 5 there is shown, also in longitudinal section and in perspective, a refractory sleeve 1d whose side surface 6 carries a plurality of cavities 7.
- the dimensions and shape of said cavities 7 may be any; similarly, their distribution can be arbitrary, although it is advantageous to produce a regular distribution in a square or staggered fashion.
- the contact zones with the strip are different depending on the variant envisaged. Punctual in the case of balls 2 and linear with the cylindrical bodies 3, these contact zones are two-dimensional in the case of surfaces 4 and 5.
- the present invention also relates to a method of manufacturing a refractory sleeve; this method, which uses the centrifugation process, is particularly applicable to the production of sleeves comprising bodies partially embedded in the outer surface layer of said sleeve, as illustrated in FIGS. 2 and 3.
- the method of manufacturing a refractory sleeve is characterized in that bodies of a first refractory material are introduced, inside a rotary cylindrical mold, in that one makes rotate said mold about its longitudinal axis and said bodies are distributed over the inner surface of said rotating mold, in which at least one second refractory material is poured into said rotating mold, so as to form a layer which coats said bodies and the total thickness of which is greater than the radial dimension of said bodies, in that said layer is maintained by support means, in that said layer is set, in that said immobilized cylinder mold, in that said support means are removed, in that said layer is removed from the mold in the form of a sleeve whose surface area contains said bodies, in that at least a portion is removed said second refractive material area located between said bodies in the outer lateral surface of said sleeve and in that said sleeve is subjected to a drying operation, respectively baking.
- the bodies can a priori have any shape without departing from the scope of the invention; the method is however particularly advantageous when using bodies having a shape of revolution, such as spheres or cylinders.
- said second refractory material can be made entirely with fine-grained refractory concrete, capable of flowing in the interstices between the bodies which constitute said first refractory material.
- a fine-grained refractory concrete only to fill the voids existing between said bodies and the interior surface of said mold and to use a coarser-grained refractory concrete to produce the radially inner part of the diaper in contact with bodies; in this case, the fine grain refractory concrete constitutes said second refractory material, while the coarser grain refractory concrete constitutes a third refractory material.
- said support means are constituted by a quick setting material, such as quick setting plaster, which is poured inside said refractory sleeve, then which is remove after taking the set.
- a quick setting material such as quick setting plaster
- said support means comprise a tube, preferably metallic, the outside diameter of which corresponds substantially to the desired inside diameter of the sleeve.
- the operation of removing said second refractory material between the bodies is carried out by sandblasting, that is to say by spraying sand which removes the refractory material infiltrated around the radially external part of the bodies.
- the "sand” considered here includes not only conventional sand, but also a substance called "metallic sand” and made up of fine particles of metal.
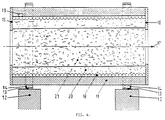
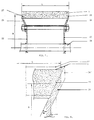
- a cylindrical mold 11 rests on a foundation 12 by means of raceways 13 and bearings 14.
- the ends of the mold 11 are provided with annular plates 15, 16, pierced with a central opening which gives access to the interior. of the mold.
- the internal diameter of the mold 11 corresponds to the diameter of the external envelope of the sleeve to be produced.
- the mold 11 can be rotated about its longitudinal axis 17 by means of a known type of motor, not shown.
- the mold 11 is rotated about the axis 17, then a plurality of bodies made of a first refractory material are introduced into the mold, such as balls 18 of alumina.
- a second refractory material is then poured into the mold 11, namely a fine-grain refractory concrete which, also under the effect of centrifugal force, fills the voids 19 existing between the balls 18 and the wall of the mold 11.
- a third refractory material is then poured which is a coarser refractory concrete and which forms a substantially cylindrical layer 20. This coarse-grained refractory concrete ensures the mechanical resistance of the sleeve.
- a quick-setting material such as plaster 21, to hold the assembly.
- the radial width of the annular plates 15, 16 corresponds at least to the total thickness of the walls of the mold and of the refractory sleeve.
- the central openings of the plates 15, 16 can be closed or reduced, for casting the plaster.
- part of the refractory material which has passed through the interstices between the balls 18 is removed by sandblasting, in order to release the external part of these balls 18 to the desired depth.
- the mold 11 may possibly be subjected to slight vibrations. Stronger vibrations then contribute to ensuring good distribution and good densification of refractory concretes.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Compositions Of Oxide Ceramics (AREA)
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| BE8700798 | 1987-07-16 | ||
| BE8700800 | 1987-07-16 | ||
| BE8700800A BE1000750A7 (fr) | 1987-07-16 | 1987-07-16 | Procede de fabrication d'un manchon refractaire par centrifugation. |
| BE8700798A BE1000748A6 (fr) | 1987-07-16 | 1987-07-16 | Manchon refractaire pour un rouleau de transport d'un produit en acier a haute temperature et rouleau de transport equipe d'un tel manchon refractaire. |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0299946A1 true EP0299946A1 (de) | 1989-01-18 |
Family
ID=25662293
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP88870123A Withdrawn EP0299946A1 (de) | 1987-07-16 | 1988-07-14 | Feuerfeste Buchse einer Transportrolle für ein warmes Metallprodukt und Verfahren zur Herstellung derselben |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP0299946A1 (de) |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3087599A (en) * | 1960-07-19 | 1963-04-30 | Osborn Mfg Co | Conveyor roll |
| FR94427E (fr) * | 1967-11-23 | 1969-08-14 | Long Bernard | Procédé pour améliorer la qualité des faces d'un ruban continu de verre. |
| FR2124525A1 (de) * | 1971-02-08 | 1972-09-22 | Uss Eng & Consult | |
| US3941181A (en) * | 1972-05-17 | 1976-03-02 | Stoody Company | Process for casting faced objects using centrifugal techniques |
| GB2011028A (en) * | 1977-12-08 | 1979-07-04 | Leuze G | Improvements in or Relating to a Frictional Drive Element and Means for its Production |
| US4385650A (en) * | 1981-04-10 | 1983-05-31 | Weyerhaeuser Company | Feed roll with spikes |
| EP0090428A1 (de) * | 1982-03-31 | 1983-10-05 | Nippon Steel Corporation | Herdrolle, die das Ablagern von Fremdstoffen wesentlich verhindert, zum Transportieren eines Stahlbandes durch einen Durchlaufglühofen |
| GB2124333A (en) * | 1982-06-09 | 1984-02-15 | Siti | Roller for supporting and feeding ceramic articles |
-
1988
- 1988-07-14 EP EP88870123A patent/EP0299946A1/de not_active Withdrawn
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3087599A (en) * | 1960-07-19 | 1963-04-30 | Osborn Mfg Co | Conveyor roll |
| FR94427E (fr) * | 1967-11-23 | 1969-08-14 | Long Bernard | Procédé pour améliorer la qualité des faces d'un ruban continu de verre. |
| FR2124525A1 (de) * | 1971-02-08 | 1972-09-22 | Uss Eng & Consult | |
| US3941181A (en) * | 1972-05-17 | 1976-03-02 | Stoody Company | Process for casting faced objects using centrifugal techniques |
| GB2011028A (en) * | 1977-12-08 | 1979-07-04 | Leuze G | Improvements in or Relating to a Frictional Drive Element and Means for its Production |
| US4385650A (en) * | 1981-04-10 | 1983-05-31 | Weyerhaeuser Company | Feed roll with spikes |
| EP0090428A1 (de) * | 1982-03-31 | 1983-10-05 | Nippon Steel Corporation | Herdrolle, die das Ablagern von Fremdstoffen wesentlich verhindert, zum Transportieren eines Stahlbandes durch einen Durchlaufglühofen |
| GB2124333A (en) * | 1982-06-09 | 1984-02-15 | Siti | Roller for supporting and feeding ceramic articles |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0476496B1 (de) | Verfahren zur Herstellung eines bimetallischen Gussstückes und Verschleissteil nach diesem Verfahren | |
| EP0616982B1 (de) | Verfahren und Vorrichtung zum Schmelzen von Glas | |
| EP2025422B1 (de) | Thermostrukturelle Verbundwalze | |
| FR2793311A1 (fr) | Dispositif de chargement de pieces a traiter thermiquement | |
| FR2503133A1 (fr) | Procede et dispositif pour lutter contre l'erosion d'un seuil de matiere refractaire | |
| WO2005084809A1 (fr) | Galets de broyage pour broyeur vertical | |
| EP0345147A1 (de) | Rolle für die Handhabung von Produkten der Eisen- und Stahlindustrie, gefördert in einem Ofen | |
| FR2819047A1 (fr) | Support approprie pour le traitement thermique d'une piece metallique et procede de traitement thermique | |
| EP2751051B1 (de) | Stopfmasse für die feuerfeste auskleidung eines metallurgischen gefässes, metallurgisches gefäss, beispielsweise ein hochofen, das eine auskleidung umfasst, die die genannte stopfmasse verwendet | |
| LU88549A1 (fr) | Procédé de fabrication d'un galet de broyage bimétallique et galet de broyage obtenu par la mise en oeuvre de ce procédé | |
| LU87282A1 (fr) | Manchon refractaire pour un rouleau de transport d'un produit metallique a haute temperature et procede de fabrication d'un tel manchon | |
| FR2952943A1 (fr) | Rouleau composite de ligne de recuit | |
| BE1000748A6 (fr) | Manchon refractaire pour un rouleau de transport d'un produit en acier a haute temperature et rouleau de transport equipe d'un tel manchon refractaire. | |
| BE1000750A7 (fr) | Procede de fabrication d'un manchon refractaire par centrifugation. | |
| CH345218A (fr) | Procédé de formation d'alliage superficiel et four pour la mise en oeuvre de ce procédé | |
| JPS59150011A (ja) | 耐ビルドアツプ性にすぐれた搬送ロ−ル | |
| LU88246A1 (fr) | Procédé de fabrication de pièces d'usure composite et pièces réalisées par ce procédé | |
| CA1086806A (fr) | Poche metallurgique pour les traitements inductifs des metaux | |
| EP1880157B1 (de) | Gekühlte walze zur handhabung von stahlprodukten | |
| EP0407323A1 (de) | Verfahren und Vorrichtung zum Stranggiessen mit Doppelrollen von dünnen metallischen Produkten, geeignet zum Kaltwalzen | |
| JPH0238513A (ja) | 高温の金属製品の移送用コロのための耐熱性ローラおよびその製造方法 | |
| CA2127343A1 (fr) | Rouleaux refroidis pour la manutention de produits, notamment metallurgiques et siderurgiques | |
| EP0552125B1 (de) | Doppelrollen Stranggiessanlage mit feuerfesten Seitenwänden | |
| BE1003548A4 (fr) | Revetement refractaire pour chenets tubulaires de fours industriels et coquilles refractaires pour la fabrication d'un tel revetement. | |
| LU87198A1 (fr) | Panneau de refroidissement pour four a cuve |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE ES FR GB IT NL SE |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19890719 |