EP0823190B1 - Verfahren, vorrichtung zur thermischen behandlung von stoffen in einem mikrowellenofen und verwendung dieses verfahrens und dieser vorrichtung - Google Patents
Verfahren, vorrichtung zur thermischen behandlung von stoffen in einem mikrowellenofen und verwendung dieses verfahrens und dieser vorrichtung Download PDFInfo
- Publication number
- EP0823190B1 EP0823190B1 EP96907289A EP96907289A EP0823190B1 EP 0823190 B1 EP0823190 B1 EP 0823190B1 EP 96907289 A EP96907289 A EP 96907289A EP 96907289 A EP96907289 A EP 96907289A EP 0823190 B1 EP0823190 B1 EP 0823190B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- microwave
- cassettes
- tunnel
- cassette
- length
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000000463 material Substances 0.000 title claims abstract description 23
- 238000000034 method Methods 0.000 title claims abstract description 17
- 238000010438 heat treatment Methods 0.000 title claims abstract description 16
- 230000005855 radiation Effects 0.000 claims abstract description 17
- 239000000919 ceramic Substances 0.000 claims abstract description 8
- 229910052751 metal Inorganic materials 0.000 claims abstract description 8
- 239000002184 metal Substances 0.000 claims abstract description 8
- 238000009768 microwave sintering Methods 0.000 claims abstract description 5
- 150000002739 metals Chemical class 0.000 claims abstract description 4
- 238000005245 sintering Methods 0.000 claims description 15
- 238000009826 distribution Methods 0.000 claims description 8
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 4
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 4
- 238000001816 cooling Methods 0.000 claims description 4
- 239000000956 alloy Substances 0.000 claims description 3
- 229910045601 alloy Inorganic materials 0.000 claims description 3
- 229910052782 aluminium Inorganic materials 0.000 claims description 3
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 3
- 230000015572 biosynthetic process Effects 0.000 claims description 3
- 229910002804 graphite Inorganic materials 0.000 claims description 3
- 239000010439 graphite Substances 0.000 claims description 3
- 230000001681 protective effect Effects 0.000 claims description 3
- UONOETXJSWQNOL-UHFFFAOYSA-N tungsten carbide Chemical compound [W+]#[C-] UONOETXJSWQNOL-UHFFFAOYSA-N 0.000 claims description 3
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims description 2
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 claims description 2
- 229910000831 Steel Inorganic materials 0.000 claims description 2
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 claims description 2
- 229910052802 copper Inorganic materials 0.000 claims description 2
- 239000010949 copper Substances 0.000 claims description 2
- 238000011049 filling Methods 0.000 claims description 2
- 229910052750 molybdenum Inorganic materials 0.000 claims description 2
- 239000011733 molybdenum Substances 0.000 claims description 2
- 229910052759 nickel Inorganic materials 0.000 claims description 2
- 239000000843 powder Substances 0.000 claims description 2
- 239000010959 steel Substances 0.000 claims description 2
- 238000003786 synthesis reaction Methods 0.000 claims description 2
- GUVRBAGPIYLISA-UHFFFAOYSA-N tantalum atom Chemical compound [Ta] GUVRBAGPIYLISA-UHFFFAOYSA-N 0.000 claims description 2
- 239000010936 titanium Substances 0.000 claims description 2
- 229910052719 titanium Inorganic materials 0.000 claims description 2
- 239000007789 gas Substances 0.000 claims 2
- 239000011261 inert gas Substances 0.000 claims 1
- 238000011068 loading method Methods 0.000 description 4
- 238000010521 absorption reaction Methods 0.000 description 3
- 238000005516 engineering process Methods 0.000 description 3
- 239000000203 mixture Substances 0.000 description 3
- 239000011195 cermet Substances 0.000 description 2
- 238000010924 continuous production Methods 0.000 description 2
- 238000011161 development Methods 0.000 description 2
- 230000018109 developmental process Effects 0.000 description 2
- 230000001105 regulatory effect Effects 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- 238000007669 thermal treatment Methods 0.000 description 2
- MEOSMFUUJVIIKB-UHFFFAOYSA-N [W].[C] Chemical compound [W].[C] MEOSMFUUJVIIKB-UHFFFAOYSA-N 0.000 description 1
- 238000004364 calculation method Methods 0.000 description 1
- 229910010293 ceramic material Inorganic materials 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 230000001143 conditioned effect Effects 0.000 description 1
- 239000000470 constituent Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000008878 coupling Effects 0.000 description 1
- 238000010168 coupling process Methods 0.000 description 1
- 238000005859 coupling reaction Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 238000001704 evaporation Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 239000011872 intimate mixture Substances 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 description 1
- 230000000750 progressive effect Effects 0.000 description 1
- 239000002994 raw material Substances 0.000 description 1
- 238000012216 screening Methods 0.000 description 1
- 229910052715 tantalum Inorganic materials 0.000 description 1
- 229910052721 tungsten Inorganic materials 0.000 description 1
- 239000010937 tungsten Substances 0.000 description 1
- HHIQWSQEUZDONT-UHFFFAOYSA-N tungsten Chemical compound [W].[W].[W] HHIQWSQEUZDONT-UHFFFAOYSA-N 0.000 description 1
- 238000011144 upstream manufacturing Methods 0.000 description 1
Images

Classifications
-
- H—ELECTRICITY
- H05—ELECTRIC TECHNIQUES NOT OTHERWISE PROVIDED FOR
- H05B—ELECTRIC HEATING; ELECTRIC LIGHT SOURCES NOT OTHERWISE PROVIDED FOR; CIRCUIT ARRANGEMENTS FOR ELECTRIC LIGHT SOURCES, IN GENERAL
- H05B6/00—Heating by electric, magnetic or electromagnetic fields
- H05B6/64—Heating using microwaves
- H05B6/78—Arrangements for continuous movement of material
- H05B6/782—Arrangements for continuous movement of material wherein the material moved is food
Definitions
- the invention relates to a method for thermal treatment of substances according to the preamble of claim 1.
- the invention further relates to a device according to the Preamble of claim 4.
- the with a measuring, control and regulating device for temperature-controlled Regulation of microwave power and / or hood speed are connected.
- the ceramic bodies to be sintered can be in a microwave transparent and thermally insulated Cassette can be arranged, for example, made of an aluminum oxide fiber consists.
- DE 36 43 649 A1 also describes a device for continuous Heating polar, preferably temperature sensitive Goods or highly viscous products under simultaneous Use of microwave energy and conditioned Atmosphere in which the goods to be treated are sufficient dimensioned resonator chamber more than once in changing Direction goes through.
- the conveyance of the goods through the device can optionally with the help of conveyor belts, gutters, Coils or tubes are made without or with additional vibration, optionally with negative, normal or positive pressure.
- DE 41 36 416 A1 describes a device for microwave radiation of materials, especially the raw materials for ceramic materials, alloys etc. with a conveyor line suggested that at least in places by a Channel or pipe arrangement is defined, the walls of which has certain microwave absorption capacity.
- This device owns the wall at least in places surrounding resonator and at least one generator for Generation of the microwave radiation, the wall of the channel or tube arrangement different microwave absorption properties over its length having.
- a device upstream of the conveyor section is provided be, by means of which the materials with additional materials high microwave absorption capacity can be added.
- this device is on the treatment of such Limited materials that can be deformed or extruded can be conveyed with a screw conveyor.
- the process should be as continuous as possible and be economically feasible, being gradual Treatment of the body to be treated in different Temperature levels with the least possible design effort is economically feasible.
- a multi-mode resonator is thus created, the size of which corresponds at most to only a few wavelengths of the microwave radiation used, such that, based on the microwave length used, the constituents of the batch act as mode mixers, which contribute to the multiple reflection of the microwaves.
- the division of the sintered goods into individual cassettes also represent the cavity, enables sintering in a quasi-continuous process that is analogous to conventional tunnel kilns can be regulated.
- sintering in a quasi-continuous process that is analogous to conventional tunnel kilns can be regulated.
- Through the low loading of the cassettes with material to be treated (Pre-sintered products) remains the same to a corresponding extent Field homogeneity largely preserved. While according to the state of the Technology prevailed that with increasing Resonator size the field can be made uniform has been shown experimentally that field distribution is essential is affected by the batch. So that each one Calculation of the furnace rooms difficult because each different Loading results in a different field distribution.
- the present invention is directed to small cassettes that act as a resonator and the condition defined in claim 1 fulfill.
- a row of cartridges can be placed under a row are moved through by microwave sources, the radiation power each microwave source on the one in the cassette desired temperature level is tunable. This is it for example possible warm-up, hold and cool down phases one after the other and next to each other.
- the individual Cassettes in a row by one with magnetrons populated tunnel moves, so that each cassette successively from the magnetrons are irradiated. It is a continuous one or discontinuous movement of the cassettes with respect to the Microwave sources possible in every direction.
- the cassettes have at least one slidable side wall, which in front of thermal treatment to the degree of filling of the material to be treated and the irradiated microwave length is adjusted.
- the resonance space is adapted to the batch quantity.
- the postponement a side wall or a corresponding piston shown in principle, for example, in EP 0 234 528 A1, FIG. 8 and explained. This system can also be used with the Use multi-mode cassettes to be used here.
- This device is according to the invention characterized in that several in the microwave sintering furnace cassettes filled with material to be treated are arranged with Except for an opening necessary for microwave radiation have essentially microwave-impermeable walls, and which are also tailored to the type of material and load Have length, width and / or height, which for loading without Formation of discrete modes leads, the cassettes one Have length, width and / or height in the unloaded Condition is too low to use the microwave frequency to generate a continuous energy distribution that enable homogeneous heating when loaded, preferably 6 wavelengths of the microwave radiation used does not exceed, the cassettes each as Microwave resonance rooms are formed.
- the sintering furnace as with fixed microwave sources designed tunnel through which the cassettes are longitudinally movable, for example by means of a tunnel Recording of the cassette arranged conveyor belt.
- the cassette walls are made microwave reflecting material, preferably graphite, Steel, molybdenum, nickel, titanium, tantalum, copper, aluminum and / or their alloys.
- at least a cassette wall slidably disposed to the floor be in order to tune or enlarge the resonance space downsize.
- the tunnel multiple microwave sources arranged at a distance are about the length of the cassette, preferably this exceeds the waveguide width.
- At batchwise movement of the row of cassettes in the Microwave tunnels can be moved one cassette length expose each cassette to a microwave source so that individual radiation outputs and temperatures per Cassette are adjustable.
- a microwave-impermeable side of each microwave source vertical shielding wall in the tunnel preferably in one Distance that corresponds approximately to the cassette length. This will ensures that the microwave radiation is shielded from the side is preferred, i.e. to the current one Cassette is directed below the source.
- the cassettes are open or point out at the top a microwave-permeable lid.
- This second embodiment has the advantage that the cassette as closed to the outside Space can be represented.
- the cassettes have a rectangular shape depending on the microwave and sintering or Heating technology have more complex shapes, e.g. Polygons, cylinders Etc..
- each cassette has at least one valve lockable Nozzle that can be supplied or removed via the gas is.
- protective gas atmospheres can be assemble the cassette.
- the cassettes can preferably be conveyed through the tunnel in such a way that that their top edge of the side walls with the least possible Distance below the lower edge of the vertical shielding walls can be passed laterally of the microwave sources. This ensures optimum shielding, i.e. it is excluded that the microwave fields are two neighboring sources are superimposed.
- the tunnel preferably has different strengths heated areas, such as those required for sintering:
- sintered bodies can be waxed, for what appropriate suction device are provided; the sintering area should be at temperatures between 400 ° C and 1800 ° C, preferably 600 ° C to 1400 ° C, heatable, the cooling area can be heated weakly or not at all, if necessary a rinse with a protective gas, intergas, reactive gas and / or gas mixture to provide.
- individual zones of the furnace can also be conventional be heated.
- microwave treatment of the Also good on individual process steps in the process restrict.
- the method and / or the device are preferably also usable for the synthesis of tungsten carbide, but also for separate ones Heat treatment alone, like the dewaxing of components.
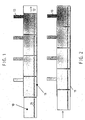
- the sintered material is individual Cassettes 10 distributed in a row one after the other arranged through a tunnel 11 in the direction of arrow 12 can be passed through.
- equidistant Distance microwave sources 13 magnetrons
- the tapes are with material to be treated, here pre-pressed cutting plates 14 made of hard metal, cermet or ceramic.
- the different Power densities or radiation powers of the microwave sources 13 are recognizable by different darknesses made. In the present case, the last source 13 radiates with the strongest performance, so that the material to be treated 14 in progressive movement from left to right warmed more becomes.
- Fig. 2 is the same row of 5 cartridges after a certain one Feed shown.
- each microwave source 13 In the position shown in Fig. 2 is each microwave source 13 centrally above the relevant cassette 10.
- the cassettes are facing the microwave sources 13 electrically conductive with the tunnel wall connected, preferably by sliding contacts.
- Fig. 3 In the embodiment shown in Fig. 3 are additional screening walls 15 are provided, the lower edge of which is scarce ends above the upper edge of the side walls 16. This will ensures that the cassettes 10 are in a centered position below the respective magnetron 13 exclusively with whose radiation is applied. Are in this position Field overlays caused by neighboring microwave radiation Sources are caused to be excluded in all others Positions are possible.
- the cassettes 10 can either be open at the top or have a microwave-permeable lid.
- the sidewalls 16 and the bottom are made of microwave-proof Material. This measure, i.e. the subdivision of the sintered material on small cassettes, which are also the so-called Cavity will represent the sintering in a quasi-continuous Process enabled, which is analogous to conventional tunnel kilns is adjustable.
- the dimensions of the sinter boxes are on matched the irradiated microwave, with a uniform loading ensures optimal field homogeneity becomes. This field homogeneity is independent of throughput, since this is due to the conveyor speed of the cassettes 10 is determined.
- each closed resonators with separate Represent microwave sources 13 the flexibility of Process can be increased. So it is possible to use different temperature ranges as well as the heating and the Accelerate cooling due to the lower sintering units. This can take advantage of the whole Let the sintering cycle run in about 2 hours. Longer Cooling down times, as with larger batches in conventional Microwave ovens are completely eliminated.
- cassettes 10 loaded in one layer with a batch of wax-containing hard metal indexable inserts, are spaced 3 mm apart, at a speed of ⁇ 20 cmmin -1 by means of microwaves with a frequency of 2.45 GHz and with increasing power density driven tunnel.
- the maximum temperature reached is 500 ° C.
- the evaporating wax is continuously sucked off through openings in the tunnel ceiling.
- the samples that have been dewaxed in this way are then fed to a sintering furnace heated conventionally or by means of microwaves.
- a plurality of graphite cassettes 10 with the dimensions 50x50x30 cm 3 , each loaded with a plurality of compression tablets of high porosity, which consist of an intimate mixture of tungsten and carbon powder, at a speed of ⁇ 10 cmmin - 1 through the tunnel loaded with 2.45 GHz microwaves and with variable power density.
- the mixture is converted to tungsten carbide powder by microwave dissipation at temperatures between 1000 and 1800 ° C.
Landscapes
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Furnace Details (AREA)
- Powder Metallurgy (AREA)
- Constitution Of High-Frequency Heating (AREA)
- Tunnel Furnaces (AREA)
- Physical Or Chemical Processes And Apparatus (AREA)
Description
- Fig. 1 und 2
- jeweils schematische Seitenansichten einer Reihe von 5 Kassetten in unterschiedlichen Relativstellungen zu den Mikrowellenquellen und
- Fig. 3
- eine alternative Ausführungsform des Mikrowellen-Tunnelofens.
Claims (10)
- Verfahren zur thermischen Behandlung von beliebigen Stoffen in einem Mikrowellenofen, insbesondere von Pulvern, Hartmetallen, Cermets und/oder Keramiken, bei dem das Behandlungsgut (14) relativ zu einer oder mehreren Mikrowellenquellen (13) bewegt wird,
dadurch gekennzeichnet,
daß das Behandlungsgut (14) in einzelnen Kassetten (10) angeordnet und bewegt wird, die mit Ausnahme einer für die Mikrowelleneinstrahlung notwendigen öffnung aus mikrowellenundurchlässigem Material bestehen und gleichzeitig den Resonanzraum bilden, dessen Länge, Höhe und/oder Breite im unbeladenen Zustand zu gering ist, um bei der verwendeten Mikrowellenfrequenz eine kontinuierliche Energieverteilung zu erzeugen, die im beladenen Zustand aber eine homogene Erwärmung ermöglichen, wobei vorzugsweise dessen Länge, Höhe und/oder Breite 6 Wellenlängen der verwendeten Mikrowellenstrahlung nicht überschreiten. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß die einzelnen Kassetten (10) in einer Reihe durch einen mit Magnetrons (13) bestückten Tunnel (11) bewegt werden, vorzugsweise kontinuierlich und/oder diskontinuierlich relativ zu den Mikrowellenquellen.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Kassetten (10) durch Veränderung ihrer Geometrie und Größe, vorzugsweise durch Verschiebung mindestens einer Kassettenwand vor der thermischen Behandlung auf den Füllgrad und die Art des Behandlungsgutes (14) und die eingestrahlte Mikrowellenlänge einjustiert werden.
- Vorrichtung zur thermischen Behandlung von Hartmetallen, Cermets und/oder Keramiken, mit einem Mikrowellen-Sinterofen, zu dessen Mikrowellenquellen (13) das Behandlungsgut (14) relativ bewegbar ist, dadurch gekennzeichnet, daß im Mikrowellen-Sinterofen mehrere mit Behandlungsgut (14) gefüllte Kassetten (10) angeordnet sind, die mit Ausnahme einer für die Mikrowelleneinstrahlung notwendigen Öffnung im wesentlichen mikrowellenundurchlässige Wände (16) aufweisen und ferner eine Länge, Breite und/oder Höhe besitzen, die im unbehandelten Zustand zu gering ist, um bei der verwendeten Mikrowellenfrequenz eine kontinuierliche Energieverteilung zu erzeugen, die im beladenen Zustand aber eine homogene Erwärmung ermöglichen, vorzugsweise 6 Wellenlängen der verwendeten Mikrowellenstrahlung nicht überschreitet, wobei die Kassetten (10) jeweils als Mikrowellenresonanzräume ausgebildet sind.
- Vorrichtung nach Anspruch 4, dadurch gekennzeichnet, daß der Mikrowellen-Sinterofen als mit feststehenden Mikrowellenquellen (13) ausgestalteter Tunnel (11) ausgebildet ist, durch den die Kassetten (10) längsbeweglich sind, wobei vorzugsweise im Tunnel ein Förderband zur Aufnahme der Kassetten (10) angeordnet ist.
- Vorrichtung nach einem der Ansprüche 4 und 5, dadurch gekennzeichnet, daß die Kassettenwände (16) aus Graphit, Stahl bzw. aus Molybdän, Nickel, Titan, Tantal, Kupfer, Aluminium und/oder deren Legierungen bestehen und/oder mindestens eine Kassettenwand (16) zur Veränderung der Größe und/oder Geometrie der Kassette verschiebbar ist.
- Vorrichtung nach einem der Ansprüche 5 und 6, dadurch gekennzeichnet, daß der Tunnel (11) mehrere Mikrowellenquellen (13) aufweist, die in einem Abstand angeordnet sind, der etwa der Länge der Kassetten (10) entspricht, vorzugsweise diese um die Hohlleiterbreite überschreitet, wobei vorzugsweise seitlich jeder Mikrowellenquelle (13) mikrowellenundurchlässige vertikale Abschirmwände (15) im Tunnel (11) vorgesehen sind, vorzugsweise in einem Abstand, der etwa der Kassettenlänge entspricht.
- Vorrichtung nach einem der Ansprüche 4 bis 7, dadurch gekennzeichnet, daß die Kassetten (10) oben offen sind oder einen mikrowellendurchlässigen Deckel aufweisen und/oder daß jede Kassette (10) mindestens einen ventilverschließbaren Stutzen zur Einstellung einer beliebigen Druck- und/oder Gasatmosphäre im Kassetteninneren aufweist, wobei vorzugsweise die Kassetten (10) durch den Tunnel (11) derart förderbar sind, daß deren obere Kante der Seitenwände (16) mit geringstmöglichem Abstand unter der Unterkante der vertikalen Abschirmwände (15) hindurchführbar ist.
- Vorrichtung nach einem der Ansprüche 4 bis 8, dadurch gekennzeichnet, daß der Tunnel (11) unterschiedlich stark beheizbare Bereiche, vorzugsweise einen Temperaturbereich bis 600°C zum Entwachsen mit Absaugung, einen Sinterbereich zwischen 600°C und 1400°C und einen Abkühlbereich, der weiterhin vorzugsweise mit einem Schutzgas wie N2 oder einem Inertgas spülbar ist.
- Verwendung des in den Ansprüchen 1 bis 3 beschriebenen Verfahren und/oder der Vorrichtung nach Ansprüchen 4 bis 9 zur Synthese von Wolframcarbid.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19515342A DE19515342A1 (de) | 1995-04-26 | 1995-04-26 | Verfahren, Vorrichtung zur thermischen Behandlung von Stoffen in einem Mikrowellenofen und Verwendung dieses Verfahrens und dieser Vorrichtung |
| DE19515342 | 1995-04-26 | ||
| PCT/DE1996/000536 WO1996034513A1 (de) | 1995-04-26 | 1996-03-21 | Verfahren, vorrichtung zur thermischen behandlung von stoffen in einem mikrowellenofen und verwendung dieses verfahrens und dieser vorrichtung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0823190A1 EP0823190A1 (de) | 1998-02-11 |
| EP0823190B1 true EP0823190B1 (de) | 1999-07-28 |
Family
ID=7760417
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP96907289A Expired - Lifetime EP0823190B1 (de) | 1995-04-26 | 1996-03-21 | Verfahren, vorrichtung zur thermischen behandlung von stoffen in einem mikrowellenofen und verwendung dieses verfahrens und dieser vorrichtung |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5977529A (de) |
| EP (1) | EP0823190B1 (de) |
| JP (2) | JP3847340B2 (de) |
| AT (1) | ATE182736T1 (de) |
| DE (2) | DE19515342A1 (de) |
| WO (1) | WO1996034513A1 (de) |
Families Citing this family (23)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19743792A1 (de) * | 1997-10-02 | 1999-04-08 | Spindelfabrik Neudorf Gmbh | Vorrichtung zum Fixieren von auf Wickelkörpern befindlichen Garnen und Zwirnen |
| DE19859288A1 (de) * | 1998-12-22 | 2000-06-29 | Bayer Ag | Agglomeration von Siliciumpulvern |
| AT3914U1 (de) * | 1999-12-09 | 2000-10-25 | Plansee Tizit Aktiengesellscha | Verfahren zur herstellung von metallkarbidpulvern im mikrowellenofen |
| WO2002032831A1 (en) * | 2000-10-19 | 2002-04-25 | Japan As Represented By Director-General Of National Institute For Fusion Science | Burning furnace, burnt body producing method, and burnt body |
| CN1307121C (zh) * | 2000-12-29 | 2007-03-28 | 康宁股份有限公司 | 利用电磁加工陶瓷的方法 |
| US6562418B2 (en) * | 2001-05-14 | 2003-05-13 | Bwxt Y-12 Llc | Microwave processing of pressed boron powders for use as cathodes in vacuum arc sources |
| JP2003075077A (ja) * | 2001-09-05 | 2003-03-12 | Natl Inst For Fusion Science | マイクロ波焼成炉およびマイクロ波焼成方法 |
| US6753299B2 (en) | 2001-11-09 | 2004-06-22 | Badger Mining Corporation | Composite silica proppant material |
| WO2003056281A2 (en) * | 2002-01-01 | 2003-07-10 | Exxonmobil Chemical Patents Inc. | Method and apparatus for on-line measurement of polymer properties |
| DE102005049533B3 (de) * | 2005-10-17 | 2007-01-25 | Püschner Gmbh & Co. Kg | Mikrowellen-Durchlaufofen |
| US9224303B2 (en) * | 2006-01-13 | 2015-12-29 | Silvertree Media, Llc | Computer based system for training workers |
| DE102008013555A1 (de) * | 2008-03-11 | 2009-10-15 | Straumann Holding Ag | Sinterofen für Dentalpräparate und Verfahren zum Sintern von Dentalpräparaten |
| EP2437020B1 (de) * | 2010-10-01 | 2015-08-12 | Ivoclar Vivadent AG | Mikrowellenofen |
| US9282594B2 (en) * | 2010-12-23 | 2016-03-08 | Eastman Chemical Company | Wood heater with enhanced microwave launching system |
| KR101290570B1 (ko) * | 2012-03-06 | 2013-07-31 | 삼성코닝정밀소재 주식회사 | 고주파 가열 장치 |
| KR101488659B1 (ko) * | 2012-03-06 | 2015-02-02 | 코닝정밀소재 주식회사 | 고주파 가열 장치 |
| KR101402585B1 (ko) | 2012-11-01 | 2014-06-02 | 코닝정밀소재 주식회사 | 글라스의 화학강화 장치 및 이를 이용한 화학강화 방법 |
| JP6407148B2 (ja) | 2013-06-03 | 2018-10-17 | 昭和電工株式会社 | マイクロ波加熱用導電性樹脂組成物 |
| KR101488661B1 (ko) * | 2014-04-28 | 2015-02-06 | 코닝정밀소재 주식회사 | 고주파 가열 장치 |
| KR102550303B1 (ko) * | 2017-02-28 | 2023-07-03 | 서울대학교산학협력단 | 발열 시스템 및 발열체 |
| WO2020223091A1 (en) * | 2019-04-30 | 2020-11-05 | Corning Incorporated | Methods for microwave drying of green ceramic honeycomb bodies using adjustable air flow |
| JP7748762B1 (ja) * | 2024-10-29 | 2025-10-03 | マイクロ波化学株式会社 | 移動炉床炉及び加熱方法 |
| WO2026095070A1 (ja) * | 2024-10-29 | 2026-05-07 | マイクロ波化学株式会社 | 移動炉床炉及び加熱方法 |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1167317B (de) * | 1960-01-13 | 1964-04-09 | Knapsack Ag | Verfahren und Vorrichtung zum Trocknen und Brennen von aus Rohphosphaten bestehenden Formlingen |
| DE1123064B (de) * | 1960-02-12 | 1962-02-01 | Mikrowellen Ges M B H Deutsche | Abschluss eines Durchlaufofens fuer Mikrowellen-Erwaermung |
| DE1935681C3 (de) * | 1969-07-09 | 1974-11-28 | Microwave Furnace & Kiln Consultants Inc., Centerport, N.Y. (V.St.A.) | Verfahren und Vorrichtung zum Erhitzen von dielektrischen Gegenständen |
| DE1947738C3 (de) * | 1969-09-20 | 1979-03-15 | Emag Eislinger Maschinenfabrik Gmbh, 7332 Eislingen | Vorrichtung zum Erwärmen von Behandlungsgut mittels Mikrowellen im Durchlaufverfahren |
| FR2293681A1 (fr) * | 1974-12-04 | 1976-07-02 | Commissariat Energie Atomique | Four continu de frittage |
| FR2548507A1 (fr) * | 1983-06-28 | 1985-01-04 | Lambda Technics Int | Applicateur a micro-ondes, a densite d'energie ajustable, destine au traitement d'objets au moins en partie polaires |
| EP0136453B2 (de) * | 1983-08-10 | 1992-08-26 | Snowdrift Corp. N.V. | Verfahren und Vorrichtung zum Erwärmen von Objekten mittels Mikrowellen |
| US4808782A (en) * | 1986-11-26 | 1989-02-28 | Toppan Printing Co., Ltd. | Microwave irradiating sterilization process |
| DE3643649A1 (de) * | 1986-12-17 | 1988-06-30 | Rudolf W Prof Dr Klingler | Vorrichtung zum erwaermen polarer, temperaturempfindlicher gueter |
| DE3818490A1 (de) * | 1988-05-31 | 1989-12-07 | Bosch Siemens Hausgeraete | Mikrowellen-haushaltgeraet |
| DE3926471A1 (de) * | 1989-08-10 | 1991-02-14 | Reinhard Schulze | Verfahren zur waermebehandlung von organischen substanzgemischen |
| US5250773A (en) * | 1991-03-11 | 1993-10-05 | Mcdonnell Douglas Corporation | Microwave heating device |
| DE4136416C2 (de) * | 1991-11-05 | 1994-01-13 | Gossler Kg Oscar | Vorrichtung zur Mikrowellen-Bestrahlung von Materialien |
| US5266762A (en) * | 1992-11-04 | 1993-11-30 | Martin Marietta Energy Systems, Inc. | Method and apparatus for radio frequency ceramic sintering |
| DE4324606C2 (de) * | 1993-07-22 | 1997-11-20 | Helmut Fleischmann | Heizungsanlagen |
| DE4324635A1 (de) * | 1993-07-22 | 1995-01-26 | Abb Patent Gmbh | Einrichtung zur Sinterung keramischer Körper mittels Mikrowellen |
-
1995
- 1995-04-26 DE DE19515342A patent/DE19515342A1/de not_active Withdrawn
-
1996
- 1996-03-21 AT AT96907289T patent/ATE182736T1/de not_active IP Right Cessation
- 1996-03-21 WO PCT/DE1996/000536 patent/WO1996034513A1/de not_active Ceased
- 1996-03-21 DE DE59602554T patent/DE59602554D1/de not_active Expired - Lifetime
- 1996-03-21 US US08/930,975 patent/US5977529A/en not_active Expired - Fee Related
- 1996-03-21 JP JP53207596A patent/JP3847340B2/ja not_active Expired - Fee Related
- 1996-03-21 EP EP96907289A patent/EP0823190B1/de not_active Expired - Lifetime
-
2006
- 2006-04-12 JP JP2006109759A patent/JP4440899B2/ja not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| DE19515342A1 (de) | 1996-10-31 |
| JPH11504153A (ja) | 1999-04-06 |
| EP0823190A1 (de) | 1998-02-11 |
| JP2006300509A (ja) | 2006-11-02 |
| ATE182736T1 (de) | 1999-08-15 |
| JP4440899B2 (ja) | 2010-03-24 |
| JP3847340B2 (ja) | 2006-11-22 |
| WO1996034513A1 (de) | 1996-10-31 |
| DE59602554D1 (de) | 1999-09-02 |
| US5977529A (en) | 1999-11-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE19515342A1 (de) | Verfahren, Vorrichtung zur thermischen Behandlung von Stoffen in einem Mikrowellenofen und Verwendung dieses Verfahrens und dieser Vorrichtung | |
| EP1060355B1 (de) | Verfahren und vorrichtung zum mikrowellensintern von kernbrennstoff | |
| DE69533647T2 (de) | Vorrichtung und verfahren zur mikrowellenbearbeitung von materialien | |
| EP2340925B1 (de) | Verfahren zum generativen Herstellen eines dreidimensionalen Objekts mit kontinuierlicher Wärmezufuhr | |
| US5408074A (en) | Apparatus for the selective control of heating and irradiation of materials in a conveying path | |
| DE3232525C2 (de) | Heizkammer für Anlagen zum Sintern und isostatischen Heißpressen von Preßkörpern aus Pulver | |
| DE69129814T3 (de) | Vorrichtung zum Laser-Strahlungsenergiesintern | |
| DE1629030C3 (de) | Kontinuierlich arbeitender Vakuumtrockner | |
| DE4318170C2 (de) | Spritzgießbares Einsatzmaterial und Verfahren zur Herstellung eines spritzgegossenen Metallgegenstandes | |
| EP3655234A1 (de) | Verfahren und vorrichtung zum herstellen von 3d-formteilen mit spektrumswandler | |
| DE3434703A1 (de) | Verfahren zum verfestigen eines metallischen, metallisch/ keramischen oder keramischen gebildes sowie vorrichtung zu seiner durchfuehrung | |
| EP0203518B1 (de) | Verfahren zur Herstellung von Formkörpern aus Siliciumgranulat für die Erzeugung von Siliciumschmelzen | |
| DE4313806A1 (de) | Vorrichtung zum Erhitzen von Materialien in einer mit Mikrowellen bestrahlbaren Heizkammer und Verfahren zum Herstellen von keramischem Gut, bei dem das Rohgut mittels Mikrowellen getrocknet wird | |
| EP0113900B1 (de) | Einrichtung und Verfahren zur Behandlung von Nahrungsmitteln mit Mikrowellen | |
| EP2935152B1 (de) | Thermisches abschirmsystem | |
| DE1629764B1 (de) | Verfahren zum herstellen eines gleichmaessig expandierten gegenstandes | |
| DE3525541C2 (de) | Verfahren und Vorrichtung zum Herstellen von β-Siliciumcarbid-Whiskern | |
| DE102011077172A1 (de) | Mikrowellenofen | |
| EP0658416A2 (de) | Verfahren zur Strukturierung von Polymerfolien | |
| WO2020002497A1 (de) | Vorrichtung und verfahren zum vernetzen mit geregelten mikrowellen | |
| DE2819762A1 (de) | Resonanter mikrowellenapplikator | |
| WO2009010201A2 (de) | Verfahren, bei dem durch mikrowellen erwärmtes metallpulver stranggepresst wird | |
| DE10066005C2 (de) | Verfahren zum Sintern von aluminiumbasierten Sinterteilen | |
| WO1998008227A1 (de) | Verfahren zum sintern von pellets aus nuklearbrennstoff | |
| DE102005049533B3 (de) | Mikrowellen-Durchlaufofen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19971002 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT DE FR GB LU SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19981021 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT DE FR GB LU SE |
|
| REF | Corresponds to: |
Ref document number: 182736 Country of ref document: AT Date of ref document: 19990815 Kind code of ref document: T |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19990729 |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 59602554 Country of ref document: DE Date of ref document: 19990902 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20091223 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20100312 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20100402 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20100322 Year of fee payment: 15 Ref country code: AT Payment date: 20100311 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20100324 Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20110321 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110321 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20111130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111001 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110331 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59602554 Country of ref document: DE Effective date: 20111001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110321 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110322 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110321 |