EP0873801A2 - Procédé et dispositif de sectionnement et transport de spires de fil non-refroidi et non-conformant aux tolerances - Google Patents
Procédé et dispositif de sectionnement et transport de spires de fil non-refroidi et non-conformant aux tolerances Download PDFInfo
- Publication number
- EP0873801A2 EP0873801A2 EP98106999A EP98106999A EP0873801A2 EP 0873801 A2 EP0873801 A2 EP 0873801A2 EP 98106999 A EP98106999 A EP 98106999A EP 98106999 A EP98106999 A EP 98106999A EP 0873801 A2 EP0873801 A2 EP 0873801A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- transport
- wire
- turns
- stelmor
- crimp
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/26—Special arrangements with regard to simultaneous or subsequent treatment of the material
- B21C47/262—Treatment of a wire, while in the form of overlapping non-concentric rings
Definitions
- the invention relates to a method and an apparatus for separating uncooled and non-tolerant Wire turns from the beginning and end of one over one Stelmor plant or comparable Wire winding transport systems transported rolled wire.
- the range of dimensions of modern wire rod products ranges from wire diameters from 5.0 to 25 mm with a Range of finish rolling speeds between 120 and approx. 20 m / s.
- To set the required structural properties Stelmor speeds during cooling between 0.1 m / s and about 1.2 m / s required.
- According to the diameter dependent final rolling speed different laying densities on the Stelmor transport or comparable wire winding transport systems between 25 and 300 turns per meter.
- the invention is based, based on the task a method and a Specify device with the help of which so far required manual work when separating uncooled and non-tolerant wire windings from the beginning and end one via a Stelmor system or comparable Wire winding transport systems transported through rolling mill reliable mechanization or automation replaced to be more humane working conditions and to create more economical processes.
- a number of front turns of the Rolling wire counted and according to a predetermined number of This turns the front wire from the finished wire severed. Then the separated turns are opened accelerated a first transport route and the following Finished wire is delayed and thus the interface in transport broadened. Then the separated ones Front crimp turns when passing an initially open one Switch at the end of the first transport route from the level of Stelmor plant or a comparable Wire winding transport system deflected down and transported away, whereas finished wire after closing the switch transported further in the Stelmor plant and the separated and transported turns under the Stelmor plant are collected and chopped up.
- the method according to the invention is of great advantage the separation of uncooled and non-tolerant Wire turns from the collar on the hook of the hook track into the Transport area of the Stelmor plant relocated or one comparable wire winding transport system. This eliminates the previously required human resources, which at the same time significantly improves the economics of the process becomes.
- the measure can preferably be used, that from the front or back crimp turns Pass the switch below the Stelmor system or one comparable wire winding transport system mini bundles for example, formed on a mandrel and this removed and collected for further processing will.
- An embodiment of the method provides that the as Soft trained first transport route to open from the Level of a Stelmor plant or a comparable one Wire winding transport system can be folded down and down can be folded up into the transport level for closing or that the following segment can be opened from the Transport level folded diagonally upwards and to close in the transport level is folded down.
- an embodiment of the invention provides that the Switch for removing front crimp turns at Separation cut opened and immediately before the arrival of the Interface closed at the end of the first transport route is, the finished wire after disconnection and removal of the Front head over the Stelmor plant or one comparable wire winding transport system transported becomes.
- the method according to the invention provides that the Abbot run the crescent turns at that moment is made in which the optical or magnetic monitored rear end of the roll core a predetermined Position, for example, in the area of the wire finishing block has reached.
- a device for separation and removal uncooled and non-tolerant wire turns from Beginning and end of a Stelmor plant or one comparable wire winding transport system transported Rolling wire comprising a wire finishing block with subordinate Driver, a winding layer and scissors, as well as one downstream cooling section in the form of the Stelmor system or a comparable wire winding transport system, in particular to carry out the method according to the Invention, is characterized in that the Wire finishing block a device for monitoring the Position of the rear end of the mill wire is assigned to that within the Stelmor facility or a comparable one Wire winding transport system one with a roller table segment trained first transport route with a terminal Switch is present, and the first transport route is one Device for controlling monitoring of the number of wire windings and location of the migrating interface possesses the means both for controlling the scissors and for Open and close the switch.
- a rolling core runs through (20) under constant control by an electronic Scanning device (15) the wire finishing block (10) and arrives by the driver (11) in the winding layer (12), the Wire turns on a limited first transport route (2) the Stelmor system (1) or a comparable one Wire winding transport system.
- the first Transport route (2) is, for example, at the rear end (7) pivoted in a horizontal axis and on front end (4), supported by a lifting device (19), designed as a flexible switch.
- a scissors (13) is arranged downstream of the winding layer (12) or also upstream, which when starting on a Interface (3) the roll core (20) in a front head (30 ') and finished wire (30) separates.
- the to the switch (4) subsequent Stelmor plant (1) or a comparable one Wire winding transport system transports the from Front head (30 ') separated finished wire (30) in a known 3 over a longer cooling section of the Stelmor plant (1).
- the counter device (14) controls continues the interface (3) and transmits after the course e.g. B. a pre-calculated period of time to the lifting device (19) a close command.
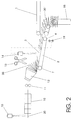
- the separated front crimp turns (30 ') on the limited first transport route (2) accelerates and separate finished wire (30) delayed, whereby the Interface (3) is widened in transport. It shows Fig.
- the Control device (15) using electronic or magnetic detection means the roller core (20) and redeems Signal off as soon as the beginning or end of a given position have reached before or within the wire finishing block (10).
- This signal is connected to the signal line (21, Fig. 4) Transfer scissors (13), which then according to a predetermined length of the end of the roller core (20) this from separates the remaining prefabricated wire (30) on one Separation point (3), as shown in Fig. 4.
- the control device (14) takes control of the migrating interface (3) and prompted according to predetermined Delay time the lifting device (19) for lowering the first transport route (2), d. H. to open the switch (4).
- the piece of finished wire (30) that has already preceded Rolling wire runs over the cooling section of the Stelmor plant (1), while the crimp turns (30 '') when entering the Switch (4) deflected downwards and on the mandrel (18) already collected in mini bundles as described above or for example, be shredded into scrap.
- Figure 4 shows the device at the moment Operating state in which the control device (15) End of the rolling wire (20) detected and a signal with the Triggers signal line (21) to activate the scissors (13). This instantly separates the wire core or the finished wire (30) at the interface (3) in finished wire (30) and one in The remaining part of given length.
- Figure 5 shows the device at the moment Operating state in which the counting device (14) Interface (3) shortly before the end of the transport route (2) detected and with a predetermined delay opening the switch (4) by folding down the transport route (2) using the Lifting device (19) causes.
- This will - according to Representation in Figure 6 - the crescent turns (30 '') below the level of the Stelmor facility (1) or one comparable wire winding transport system distracted, during the finished wire (30) - now after cutting off Front (30 ') - and crested (30' ') turns - over the Stelmor plant (1) or a comparable one Wire winding transport system is promoted.
- the Hinterschopfwinditch (30 '') as before according to FIG. 2 the front crimp turns (30 ') are derived downwards and occasionally collected on the collecting mandrel (18) into mini bundles or shredded into scrap pieces in a chopper.
- Figure 7 shows the formation of a switch (4) on Starting area of the Stelmor plant (1) or one comparable wire winding transport system in the form of a Arrangement of laterally displaceable stub rollers (6). Be the open sale of the stub rollers (6 ') shown fall the wire windings (30 ') according to FIGS. 1 and 2, respectively (30 '') according to FIGS. 5 and 6 through the switch (4) below.
- the measures and configurations according to the invention are not to those shown in the drawing figures Embodiments limited.
- Possible variations of the Device according to the invention can consist in that for example, the separator (13), the execution of the Switch (4) or the collecting device with the mandrel (18) or the monitoring devices (14, 15) in a different type and Are trained.
- the acceleration more separate Turns or the delay of the subsequent turns can by means of variable roller table speeds or by means of separate devices, such as grippers, Chains, transport fingers.
- the respective constructive Design is in line with special designs or uses or problems to the specialist exempt.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Winding, Rewinding, Material Storage Devices (AREA)
- Filamentary Materials, Packages, And Safety Devices Therefor (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Electric Cable Installation (AREA)
- Coiling Of Filamentary Materials In General (AREA)
- Forwarding And Storing Of Filamentary Material (AREA)
- Metal Rolling (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19717770A DE19717770A1 (de) | 1997-04-26 | 1997-04-26 | Verfahren und Vorrichtung zum Abtrennen und Abtransportieren ungekühlter und nicht toleranzhaltiger Drahtwindungen |
| DE19717770 | 1997-04-26 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0873801A2 true EP0873801A2 (fr) | 1998-10-28 |
| EP0873801A3 EP0873801A3 (fr) | 2001-05-02 |
| EP0873801B1 EP0873801B1 (fr) | 2004-06-02 |
Family
ID=7827895
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98106999A Expired - Lifetime EP0873801B1 (fr) | 1997-04-26 | 1998-04-17 | Procédé et dispositif de sectionnement et transport de spires de fil non-refroidi et non-conformant aux tolerances |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US5988551A (fr) |
| EP (1) | EP0873801B1 (fr) |
| JP (1) | JPH1177137A (fr) |
| AT (1) | ATE268230T1 (fr) |
| DE (2) | DE19717770A1 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1077486C (zh) * | 1999-06-24 | 2002-01-09 | 唐基斌 | 木质压花板拉伸模具 |
| CN102825074A (zh) * | 2012-09-14 | 2012-12-19 | 南京钢铁股份有限公司 | 一种胎圈钢丝用盘条的控制冷却工艺 |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1297058B1 (fr) * | 1999-11-10 | 2008-07-30 | O'Neil, Charles | Optimisation des performances de nanofiltration des polymeres |
| KR101253827B1 (ko) * | 2010-09-10 | 2013-04-12 | 주식회사 포스코 | 선재코일 냉각 방법 및 장치 |
| KR101746991B1 (ko) * | 2015-12-24 | 2017-06-14 | 주식회사 포스코 | 소재 냉각영역 검출 장치 및 선재 냉각영역 검출 방법 |
| IT202200006434A1 (it) * | 2022-03-31 | 2023-10-01 | Danieli Off Mecc | Apparato e procedimento di avanzamento e taglio di un prodotto metallico |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3452785A (en) * | 1965-12-07 | 1969-07-01 | David William Mclean | Apparatus for depositing and conveying rod rings in sequence with rod forming means |
| DE3029229A1 (de) * | 1980-08-01 | 1982-04-01 | Moeller & Neumann Gmbh, 6670 St Ingbert | Vorrichtung zur herstellung von stahldraht mit vollstaendig angelassener martinsitschicht |
| CH677652A5 (fr) * | 1989-03-07 | 1991-06-14 | Grapha Holding Ag | |
| US5066430A (en) * | 1989-03-20 | 1991-11-19 | E. I. Du Pont De Nemours And Company | Process for centrifugally spinning pitch carbon fibers |
| DE3919836A1 (de) * | 1989-04-26 | 1990-10-31 | Hamburger Stahlwerke Gmbh | Verfahren und anlage zum coupieren der anfangswindungen und/oder endwindungen eines drahtbundes |
| DE4035192A1 (de) * | 1990-11-06 | 1992-05-07 | Thaelmann Schwermaschbau Veb | Vorrichtung zum schopfen der anfangs- und endwindungen eines drahtwindungsstranges |
| DE4106491A1 (de) * | 1991-03-01 | 1992-09-03 | Schloemann Siemag Ag | Anlage mit einem bundbilde- und transportsystem fuer draht oder feinstahl, insbesondere fuer hohe bundgewichte |
| DE4109201A1 (de) * | 1991-03-18 | 1992-09-24 | Thaelmann Schwermaschbau Veb | Vorrichtung zum transportieren und schopfen einer walzader |
| DE4117906C2 (de) * | 1991-05-31 | 1994-01-05 | Andreas Kubicek | Verfahren und Vorrichtungen zur automatischen Handhabung von Walzdraht in Drahtwalzwerken |
| DE4491537D2 (de) * | 1993-03-19 | 1996-09-26 | Thaelmann Schwermaschbau Veb | Verfahren und Einrichtung zum Abtrennen von Drahtwindungen |
-
1997
- 1997-04-26 DE DE19717770A patent/DE19717770A1/de not_active Withdrawn
-
1998
- 1998-04-17 DE DE59811494T patent/DE59811494D1/de not_active Expired - Lifetime
- 1998-04-17 AT AT98106999T patent/ATE268230T1/de active
- 1998-04-17 EP EP98106999A patent/EP0873801B1/fr not_active Expired - Lifetime
- 1998-04-23 US US09/065,315 patent/US5988551A/en not_active Expired - Lifetime
- 1998-04-24 JP JP10115555A patent/JPH1177137A/ja not_active Withdrawn
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1077486C (zh) * | 1999-06-24 | 2002-01-09 | 唐基斌 | 木质压花板拉伸模具 |
| CN102825074A (zh) * | 2012-09-14 | 2012-12-19 | 南京钢铁股份有限公司 | 一种胎圈钢丝用盘条的控制冷却工艺 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0873801B1 (fr) | 2004-06-02 |
| DE19717770A1 (de) | 1998-10-29 |
| DE59811494D1 (de) | 2004-07-08 |
| JPH1177137A (ja) | 1999-03-23 |
| ATE268230T1 (de) | 2004-06-15 |
| EP0873801A3 (fr) | 2001-05-02 |
| US5988551A (en) | 1999-11-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2910476B1 (fr) | Dispositif de transport de produits alimentaires | |
| EP3507030B1 (fr) | Installation de production pouvant fonctionner en continu et procédé permettant de faire fonctionner une installation de production en cas de défaillance | |
| DE2102684C3 (de) | Vorrichtung zum Durchtrennen von Walzdraht | |
| EP4169637A1 (fr) | Procédé et système de fabrication de ressorts hélicoïdaux | |
| WO2021052834A1 (fr) | Retrait automatisé de bandes de liaison d'une bobine | |
| EP0873801B1 (fr) | Procédé et dispositif de sectionnement et transport de spires de fil non-refroidi et non-conformant aux tolerances | |
| DE102007040035A1 (de) | Verfahren und Vorrichtung zum Erzeugen und nachfolgenden Konfektionieren eines Kabelabschnitts an seinem Vorder- und Hinterende | |
| DE2141972A1 (de) | Vorrichtung zum unterteilen eines drahtwindungsstranges in einer bundbildestation | |
| DE2838155C3 (de) | Förderer zum Transportieren von Drahtwindungen | |
| DE1752196A1 (de) | Verfahren und Vorrichtung zum Unterteilen einer Windungslage | |
| DE3116089C2 (de) | Vorrichtung zum Trennen von Drahtwindungssträngen im Schacht einer Bundsammelstation | |
| EP1514617A1 (fr) | Dispositif de tréfilage et méthode d'utilisation d'un dispositif de tréfilage | |
| EP3351663B1 (fr) | Procédé de maintenance des positions de filage d'un métier à filer ainsi que métier à filer | |
| WO2016110474A1 (fr) | Dispositif et procédé de traitement ultérieur d'un écheveau de fils déroulés | |
| DE19652089A1 (de) | Verfahren und Vorrichtung zum Abtrennen ungekühlter und nicht toleranzhaltiger Drahtwindungen vom Anfang und Ende einer über eine Stelmor-Anlage transportierten Walzader | |
| DE10163427A1 (de) | Schneckenförderer zum Transport von an Hängeträgern hängendem Fördergut | |
| DE2143449C3 (de) | Vorrichtung zum Trennen eines Drahtwindungsstranges in einer Bundbildestation | |
| DE2940761C2 (de) | Vorrichtung zum seitlichen Auswerfen von langgestrecktem Gut | |
| DE4109201A1 (de) | Vorrichtung zum transportieren und schopfen einer walzader | |
| DE4035192A1 (de) | Vorrichtung zum schopfen der anfangs- und endwindungen eines drahtwindungsstranges | |
| DE4117906A1 (de) | Verfahren und vorrichtungen zur automatischen handhabung von walzdraht in drahtwalzwerken | |
| EP0930108A2 (fr) | Dispositif de dépot de boucles de fil | |
| EP4368308A1 (fr) | Procédé et système d'enroulement | |
| DE2150420A1 (de) | Vorrichtung zum unterteilen eines drahtwindungsstranges in einer bundbildestation | |
| DE827642C (de) | Verfahren zum Umfuehren von Walzadern in Walzenstrassen durch Umbiegen der Profile oder Stangen von einer Walze zur andern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19980417 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT DE IT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SMS DEMAG AG |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: AT DE IT SE |
|
| 17Q | First examination report despatched |
Effective date: 20030424 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT DE IT SE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REF | Corresponds to: |
Ref document number: 59811494 Country of ref document: DE Date of ref document: 20040708 Kind code of ref document: P |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050303 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20140418 Year of fee payment: 17 Ref country code: DE Payment date: 20140418 Year of fee payment: 17 Ref country code: AT Payment date: 20140411 Year of fee payment: 17 Ref country code: IT Payment date: 20140429 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59811494 Country of ref document: DE Representative=s name: HEMMERICH & KOLLEGEN, DE Ref country code: DE Ref legal event code: R081 Ref document number: 59811494 Country of ref document: DE Owner name: SMS GROUP GMBH, DE Free format text: FORMER OWNER: SMS SIEMAG AKTIENGESELLSCHAFT, 40237 DUESSELDORF, DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59811494 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 268230 Country of ref document: AT Kind code of ref document: T Effective date: 20150417 Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20151103 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150417 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150418 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150417 |