EP0913217A1 - Vorrichtung zum Verteilen von Schlackenpulver und Stranggiessanlage mit einer derartigen Verteilungsvorrichtung - Google Patents
Vorrichtung zum Verteilen von Schlackenpulver und Stranggiessanlage mit einer derartigen Verteilungsvorrichtung Download PDFInfo
- Publication number
- EP0913217A1 EP0913217A1 EP98420190A EP98420190A EP0913217A1 EP 0913217 A1 EP0913217 A1 EP 0913217A1 EP 98420190 A EP98420190 A EP 98420190A EP 98420190 A EP98420190 A EP 98420190A EP 0913217 A1 EP0913217 A1 EP 0913217A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- powder
- bath
- distribution
- dose
- retracted
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000000843 powder Substances 0.000 title claims abstract description 140
- 239000002893 slag Substances 0.000 title claims abstract description 26
- 238000009749 continuous casting Methods 0.000 title claims abstract description 10
- 238000009434 installation Methods 0.000 title claims abstract description 10
- 238000009826 distribution Methods 0.000 claims abstract description 55
- 239000002184 metal Substances 0.000 claims abstract description 28
- 229910052751 metal Inorganic materials 0.000 claims abstract description 28
- 238000007790 scraping Methods 0.000 claims description 34
- 210000000056 organ Anatomy 0.000 claims description 7
- 235000013365 dairy product Nutrition 0.000 claims description 6
- 238000006073 displacement reaction Methods 0.000 claims description 5
- 230000014759 maintenance of location Effects 0.000 claims description 3
- 239000000470 constituent Substances 0.000 claims 1
- 239000002245 particle Substances 0.000 description 5
- 230000003647 oxidation Effects 0.000 description 4
- 238000007254 oxidation reaction Methods 0.000 description 4
- 230000000694 effects Effects 0.000 description 3
- 238000004891 communication Methods 0.000 description 2
- 239000000428 dust Substances 0.000 description 2
- 230000005484 gravity Effects 0.000 description 2
- 238000010438 heat treatment Methods 0.000 description 2
- 238000005461 lubrication Methods 0.000 description 2
- 239000011819 refractory material Substances 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 238000009833 condensation Methods 0.000 description 1
- 230000005494 condensation Effects 0.000 description 1
- 239000000498 cooling water Substances 0.000 description 1
- 230000001627 detrimental effect Effects 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 230000001050 lubricating effect Effects 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 230000000750 progressive effect Effects 0.000 description 1
- 230000000717 retained effect Effects 0.000 description 1
- 239000005368 silicate glass Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 230000001960 triggered effect Effects 0.000 description 1
- 238000009827 uniform distribution Methods 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/10—Supplying or treating molten metal
- B22D11/108—Feeding additives, powders, or the like
Definitions
- the molten metal is poured, in a known manner, into an ingot mold by through a tube of refractory material called "nozzle" which plunges into a bath of molten metal collected in the ingot mold.
- a layer of liquid slag is placed on the surface of this bath so as to protect the metal from oxidation. This layer is gradually entrained between the metal descending into the ingot mold and the side walls thereof, which provides lubrication of the surfaces facing the ingot mold and metal bar being solidified.
- These means include a hopper for receiving the powder, the lower end of which opens into a tube in which turns an Archimedes screw.
- This tube allows the feeding in slag powder, by its lower part, of a number of distribution devices.
- Each of these includes a frustoconical pocket leading to a nozzle oriented towards a specific area of the surface of the bath.
- Each nozzle is associated with an axial air nozzle tablet for delivering the powder contained in the frustoconical pocket on the surface of the molten metal bath.
- this distribution device has a drawback linked to its inability to distribute satisfactorily any type of slag powder.
- powder some of which are granular, and have a good natural ability to distribute, and others are said to be powdery and have a low natural ability to distribute.
- this has the effect of operating a progressive grinding of the powder circulating therein, so that a initially granular powder gradually has a powder structure which, as explained above, is detrimental to the quality of its distribution.
- a device for distribution of slag powder on the surface of a molten metal comprising a powder reservoir closed by a background.
- the latter which constitutes the reception area of the powder, is generally horizontal and extends to the vertical of a wall of the mold. This background allows the passage of a gas retained in a lower chamber.
- the powder once mixed with gas, is then ejected above the mold pneumatically, in a direction substantially horizontal.
- the invention proposes to overcome all of the drawbacks of the prior art mentioned above.
- the means for distribution include a movable scraper member according to a direction of travel between a position retracted by relative to the bath and an advanced position relative to the bath, said scraping member comprising a suitable pushing surface ejecting said dose of powder during its movement between said retracted and advanced positions of the scraper member.
- the distribution device allows to achieve the previously mentioned objectives. Indeed, it ensures a good distribution of the slag powder on the entire surface of the bath, as will be explained in look at the description below.
- the volume of the dose delivered to the reception area can be perfectly known, depending on the powder flow level supply means and the time during which the powder is delivered from these supply means to the area reception.
- the push surface is able to lift during movement of the scraper member between the advanced and retracted positions, so as to be distant from the receiving element of powder.
- the thrust surface is able to pivot about an axis horizontal during movement of the scraping member between its advanced and retracted positions, and comes into abutment against the minus a protrusion of the scraping member during its movement between its retracted and advanced positions.
- the device comprises at least one lateral retaining surface powder during the movement of the scraping member between its retracted position and its advanced position.
- This retaining surface can be provided integral either with the scraping member or with the element powder reception.
- the scraper member is provided with homogeneous distribution means powder on the powder receiving area.
- the operation ejection of this dose is therefore reliable and allows a distribution satisfactory powder on the surface of the bath.
- These homogeneous means of distribution may include a bow protruding from the vicinity of the thrust surface, towards the bath.
- the scraping member comprises a core disposed substantially perpendicular to the direction of movement of the organ scraping and constituting the thrust surface, and two wings extending, on either side of the soul, towards the bath, and each constituting a lateral retaining surface.
- the scraper member present, with a view to above, for example a U or U shape with inclined wings.
- each wing is extended, at its distal end, by a deflector protruding both in the opposite direction to the soul and in the direction of the opposite wing.
- the presence of these deflectors guarantee satisfactory powder distribution over the entire surface of the bath, in particular on the side of the nozzle opposite the dispensing device.
- the scraper member slides between two parallel edges of which is provided with the powder receiving element.
- the scraping member comprises two wings parallel
- these edges allow the guiding of the scraping during its displacement.
- the organ of scraping only includes a pushing surface
- these edges parallels assume a guiding function, and constitute also a lateral powder retaining surface during its ejection.
- the device comprises a covering cover, in the position retracted, from the scraping member, at least the receiving area powder, this cover being provided with at least one opening powder passage from the feed device powder.
- the invention also relates to an installation for continuous casting comprising an ingot mold defining a volume for receiving a molten metal bath, a supply nozzle of molten metal, means for feeding powder dairy and means of distributing this powder to the surface of the molten metal bath, characterized in that the means of distributing slag powder include at minus a device as described above.
- the means slag powder feed include means of homogeneous distribution of the powder dose over the receipt of each powder dispensing device.
- the means of homogeneous distribution comprise at least one diffuser arranged on the powder flow path and widening towards the reception area, so that form at least two separate powder flows, on the one hand and on the other of the axis of movement of the scraping member.
- the installation includes at least a couple of distribution as described above, each pair of devices being arranged facing each other on the nozzle.
- the installation includes means ensuring the movement of supply means and powder distribution means.
- the means of supply and distribution of powder can be mounted on a carriage running in parallel at the edge of the mold to allow distribution powder at several points for large molds width.
- the powder supply means are provided with means for heating the powder.
- these heating means allow to bring it to a temperature close to 300 at 400 ° C, so that the powder is more easily transformed into dairy, which ensures satisfactory lubrication of ingot molds of small section.
- FIG. 1 shows a billet ingot mold, designated as a whole by the reference 2, and which will assume a rectangular section.
- This mold has interior walls 4 and exterior walls 6, between which is defined a chamber 7 in which flows from cooling water.
- the invention also finds its application to bloom molds.
- a nozzle 8 placed in communication with a tank not represented, allows to deliver molten metal, which one will suppose to be steel, in the mold.
- the nozzle 8, produced in refractory material, opens into a molten metal bath 10 which is in contact with the internal side walls 4 of the mold 2.
- the metal partially solidifies on contact of the cooled walls of the mold, forming a bar which is extracted continuously from the end bottom of the mold using suitable rollers not represented.
- a layer of slag 12 is placed on the upper surface of the bath 10 to protect the latter from oxidation.
- the slag which is for example constituted by a easily fused silicate glass, is gradually driven by capillarity down, constituting a lubricating film which facilitates the descent of the solidified bar and reduces wear inner side walls 4 of the mold.
- the casting installation continuous comprises a device 14 for feeding powder dairy, as well as a device 16 for distributing this powder on the surface of the bath 10 of the molten metal.
- the feed device 14 includes a hopper 18 fed with slag powder.
- the lower end of the hopper 18 is in communication with a tube 20 extending in direction of the bath 10, and inside which is disposed a Archimedes screw 22 driven by a motor 24.
- the end of the tube 20, opposite the hopper 18, includes a nozzle 26 of powder spill. This nozzle 26 flares on the side and on the other side of the longitudinal axis of the tube 20.
- the distribution device 16 comprises, like the show Figures 1 and 2, a plate 30 substantially horizontal constituting an element for receiving the powder of dairy.
- the end 32 of the plate, closest to the bath 10, is substantially flush with the inner side wall 4B of the ingot mold 2.
- a scraping member 34 which is constituted by a substantially U-shaped profile, is arranged on the face upper of the plate 30.
- This profile 34 consists of a core 36 substantially parallel to the wall 4B, extended by two wings 38 extending horizontally towards the bath 10.
- Each wing 38 is provided, at its distal end, with a deflector 40 protruding both in the opposite direction to the core 36, and in the direction of the opposite wing.
- the core 36 is integral, at the level of its face opposite to the wings 38, of the rod 42 of a pneumatic type jack 44.
- the profile 34 is therefore mobile, in direction D substantially perpendicular to its core 36, between a position retracted by relative to the bath and an advanced position relative to the bath.
- the scraper member defines, with its core 36, its wings 38 and the end 32 of the plate 30, an area of reception 46 of the powder coming from the nozzle 26.
- the advanced position of the profile 34 is shown in fine dashed lines in Figure 1, as well as solid lines in Figure 2. In this position, the face 36A of the most close to the wings 38 is substantially flush with the end 32 of the plate 30.
- the jack 44 acts on the rod 42 so as to set the profile in motion 34 to its advanced position shown in phantom purposes in Figure 1, and to eject the powder dose 48.
- This operation can be triggered either manually by a operator, either at a predetermined fixed rate, or again following an indication issued by a sensor, that the level of powder on the surface of the bath is insufficient.
- the core 36 of the profile 34 constitutes a pushing surface of the powder dose 48, then that its wings 38 allow lateral retention of this powder.
- Ejection of slag powder by means of profile 34 ensures a homogeneous distribution of this powder at the surface of the bath 10.
- the speeds horizontal ejection, from the plate 30, of the different powder particles constituting the dose 46, are different between them.
- the powder particles initially placed opposite the core 36 of the profile 34 are ejected at a relatively low speed, and are delivered to the surface of the bath, in the vicinity of the wall 4B adjacent to the distribution device 16, as shown by arrow F 1 .
- the powder particles initially placed in the vicinity of the core 36 will be ejected with a significantly greater speed, and will be distributed in the vicinity of the wall 4A opposite the distribution device 16, as indicated by the arrow F 2 .
- the powder particles initially placed in the center of the zone 46 follow an intermediate trajectory materialized by the arrow F 3 .
- the speed with which the profile 34 is driven in translation must be adjusted so that the powder particles traveling the longest distance, come into contact with the surface of the bath 10 in the vicinity of the wall 4A.
- the dose of powder 48 is ejected when it reaches a volume of 400 cm 3 .
- the speed of the scraper member is 0.3 m / s and its stroke is 150 mm.
- the dose of powder 48 is ejected when it reaches a volume of 160 cm 3 .
- the speed of the scraper member is 0.4 m / s and its stroke is 110 mm.
- the presence of the deflectors 40 ensures the distribution of slag powder, in zone 50 of the surface of the bath located opposite the plate 30.
- the jack 44 acts on the rod 42 so as to return the profile 34 to its position retracted. Then, a new dose of powder is delivered to the level of the receiving surface 46 of the plate 30, and we repeats the ejection process described above.
- Figure 3 shows an alternative embodiment of the device distribution according to the invention.
- the latter designated by the reference 116, includes a plate 130 having 132 lateral flanges extending substantially along the axis of displacement A of the scraping member.
- the latter includes a blade 134 vertical, extending substantially perpendicularly to axis A.
- This blade 134 can be set in motion under the effect of the rod 142 of a jack, not shown, between positions retracted and advanced relative to the bath, analogously to scraping profile 30, in order to eject the powder dose above from the surface of the bath.
- the blade 134 which constitutes a pushing surface of the powder during its ejection, is provided with a bow formed by a tetrahedral lug 148 protruding from the face of the blade opposite the rod 142. This lug ensures a better distribution of the dose powder delivered to reception area 146.
- this distribution device described in FIG. 3 is similar to that of the device 16 described in Figures 1 and 2. It should be noted that during the movement of the blade 134 between its retracted position and its advanced position, the lateral edges 132 of the plate 130 assume both a function of guiding this blade, and of lateral retention powder.
- FIG. 4 illustrates a third embodiment of the dispensing device according to the invention.
- This last designated as a whole by the reference 216, includes a powder receiving element 230 formed by a plate having a central boss 231 on either side of which extend two lateral slides 231A.
- This element of reception also includes side edges 232.
- the distribution device 216 also includes a scraping device designated as a whole by the reference 234.
- the latter comprises a basic body 235 having, in top view, generally a U-shape.
- This basic body 235 is provided with side wings 238 terminated by deflectors 240 similar to those 40 shown in Figures 1 and 2.
- Each wing 238 is provided with a lower rim 238A extending in direction of the opposite wing.
- a projection 238B is provided on the upper face of each of these edges 238A.
- the 235A upper face of the base body 235 is also partially closed and has, in the vicinity of the deflectors 240, a 235B U-shaped recess for the passage of the powder.
- a flap 236 is pivotally mounted around an axis B passing through its upper face 236A, on the wings 238 of the body base 235, at orifices 238C of seals.
- the blind 236 is articulated to the rod 242 of a jack not shown, by through a crosspiece 244 cooperating with yokes 245 with which section 236 is provided.
- the latter presents, at level of its lower end 236B, a corresponding profile both at boss 231 and at slides 231A of the receiving element 230, so that it is able to slide on the upper surface of the latter.
- This component 236 constitutes, as will be explained below, a surface powder pushing.
- a bow 248 is fixed at the level of the upper face 235A of the basic body 235.
- This bow has two sides 248A symmetrical about the longitudinal axis of the organ scraping, both protruding towards the element reception 230 and in the direction of the deflectors 240, that is to say, in service, in the direction of the molten metal bath.
- the scraping member 234 is intended to be covered by a U-shaped top cover 249 whose wings 249A are fixed to the edges 232 of the receiving element 230.
- This cover is provided with a substantially rectangular opening 249B, ensuring the passage of the powder from the supply device.
- This supply device designated as a whole by the reference 214 includes, analogously to the device 14 shown in Figure 1, a tube 220 inside which is arranged an Archimedes screw not shown.
- This tube is fixed to the cover 249 by means of fittings 221. It is provided at its end opposite to the actuation motor the screw, a nozzle 226 ensuring the pouring of the powder onto the receiving element 230.
- This nozzle 226 is provided with a diffuser 228 formed by a recess in its walls, which allows to divide the powder flow coming from the tube 220, according to two distinct flows along passages 228A and 228B arranged on either side of the diffuser 228, and therefore of the axis A of displacement of the scraping member 234. This arrangement ensures a uniform distribution of the powder at the receiving element 230.
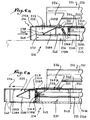
- the scraping member 234 is movable between a position retracted shown in Figures 5A and 6A and a position projection shown in Figures 5B and 6B.
- the front end of the wings 238 is substantially flush with the end before the receiving element 230.
- the front end is, in use, adjacent to the bath.
- the powder slag conveyed by the Archimedes screw pours out, level of nozzle 226, according to passages 228A, 228B formed at within it.
- the symmetrical 248A faces of the bow ensure a good distribution of the powder, both on the central boss 231 and the slides 231A of the element reception, which constitute a reception area 246 of the powder.
- the flap 236 In the advanced position of the scraping member, the flap 236 is substantially flush with the front end of the element reception 230. Once the powder has been ejected, the rod 242 acts on the flap 236 so as to move the scraping member 234 towards its retracted position. During this movement, as shown in particular in FIG. 6A, the flap 236 tends to be lift backwards, under the effect of the traction exerted by rod 242, so as to limit the loss of powder residual during the return of the scraping member. Once this last returned to its retracted position, an additional dose powder can be admitted in the reception area 246 as soon as desired by the user, then ejected under the action of the scraping member 234.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Continuous Casting (AREA)
- Furnace Details (AREA)
- Coating Apparatus (AREA)
- Dairy Products (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9713133A FR2769526B1 (fr) | 1997-10-15 | 1997-10-15 | Dispositif de distribution de poudre de laitier et installation de coulee continue incluant un tel dispositif |
| FR9713133 | 1997-10-15 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0913217A1 true EP0913217A1 (de) | 1999-05-06 |
| EP0913217B1 EP0913217B1 (de) | 2002-05-08 |
Family
ID=9512440
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98420190A Expired - Lifetime EP0913217B1 (de) | 1997-10-15 | 1998-10-14 | Vorrichtung zum Verteilen von Schlackenpulver und Stranggiessanlage mit einer derartigen Verteilungsvorrichtung |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0913217B1 (de) |
| AT (1) | ATE217223T1 (de) |
| DE (1) | DE69805263T2 (de) |
| ES (1) | ES2173559T3 (de) |
| FR (1) | FR2769526B1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20220135369A (ko) * | 2021-03-30 | 2022-10-07 | 현대제철 주식회사 | 파우더 공급 장치 |
| CN119016695A (zh) * | 2024-10-29 | 2024-11-26 | 洛阳科丰冶金新材料有限公司 | 一种分层熔渣炉 |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AT509547B1 (de) * | 2010-03-12 | 2013-12-15 | Siemens Vai Metals Tech Gmbh | Verfahren und anlage zum aufbringen eines pulverförmigen stoffs auf einen badspiegel einer metallischen schmelze in einem metallurgischen gefäss |
| CN102319878A (zh) * | 2011-08-05 | 2012-01-18 | 包头联方高新技术有限责任公司 | 方坯连铸保护渣加入装置 |
| WO2017135074A1 (ja) * | 2016-02-04 | 2017-08-10 | 新日鐵住金株式会社 | 溶融金属用の添加材投入方法、および溶融金属用の添加材投入装置 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1529099A (en) * | 1975-11-12 | 1978-10-18 | Nippon Steel Corp | Apparatus for supplying powder to casting mould |
| FR2393746A1 (fr) * | 1977-06-10 | 1979-01-05 | Siderurgie Fse Inst Rech | Distributeur automatique de produits pulverulents |
| FR2421015A1 (fr) * | 1978-03-31 | 1979-10-26 | Mannesmann Ag | Procede et dispositif pour deposer des adjuvants de coulee en quantites dosees sur la surface libre d'un bain de metal fondu |
| DE3044591A1 (de) * | 1978-03-31 | 1982-07-08 | Mannesmann AG, 4000 Düsseldorf | Vorrichtung zum dosierten einbringen von giesspulver in eine stranggiesskokille |
| JPS61199560A (ja) * | 1985-02-28 | 1986-09-04 | Nippon Kokan Kk <Nkk> | エア−スライド式モ−ルドパウダ供給装置 |
-
1997
- 1997-10-15 FR FR9713133A patent/FR2769526B1/fr not_active Expired - Fee Related
-
1998
- 1998-10-14 EP EP98420190A patent/EP0913217B1/de not_active Expired - Lifetime
- 1998-10-14 DE DE69805263T patent/DE69805263T2/de not_active Expired - Fee Related
- 1998-10-14 AT AT98420190T patent/ATE217223T1/de not_active IP Right Cessation
- 1998-10-14 ES ES98420190T patent/ES2173559T3/es not_active Expired - Lifetime
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1529099A (en) * | 1975-11-12 | 1978-10-18 | Nippon Steel Corp | Apparatus for supplying powder to casting mould |
| FR2393746A1 (fr) * | 1977-06-10 | 1979-01-05 | Siderurgie Fse Inst Rech | Distributeur automatique de produits pulverulents |
| FR2421015A1 (fr) * | 1978-03-31 | 1979-10-26 | Mannesmann Ag | Procede et dispositif pour deposer des adjuvants de coulee en quantites dosees sur la surface libre d'un bain de metal fondu |
| DE3044591A1 (de) * | 1978-03-31 | 1982-07-08 | Mannesmann AG, 4000 Düsseldorf | Vorrichtung zum dosierten einbringen von giesspulver in eine stranggiesskokille |
| JPS61199560A (ja) * | 1985-02-28 | 1986-09-04 | Nippon Kokan Kk <Nkk> | エア−スライド式モ−ルドパウダ供給装置 |
Non-Patent Citations (1)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 011, no. 028 (M - 557) 27 January 1987 (1987-01-27) * |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20220135369A (ko) * | 2021-03-30 | 2022-10-07 | 현대제철 주식회사 | 파우더 공급 장치 |
| CN119016695A (zh) * | 2024-10-29 | 2024-11-26 | 洛阳科丰冶金新材料有限公司 | 一种分层熔渣炉 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0913217B1 (de) | 2002-05-08 |
| DE69805263T2 (de) | 2002-11-14 |
| ATE217223T1 (de) | 2002-05-15 |
| FR2769526A1 (fr) | 1999-04-16 |
| FR2769526B1 (fr) | 1999-12-03 |
| DE69805263D1 (de) | 2002-06-13 |
| ES2173559T3 (es) | 2002-10-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0521794B1 (de) | Vorrichtung zur Lagerung und Förderung von Eiskugeln, ohne Verschmelzung derselben, von ihrem Herstellungsort bis zu ihrem Verwendungsort wo sie gegen eine Zielfläche geschleudert werden | |
| FR2525134A1 (fr) | Dispositif de transfert de metal en fusion | |
| EP0269180A2 (de) | Vorrichtung zum Giessen eines pastenartigen Metalles | |
| FR3046095A1 (fr) | Machine de fabrication additive et procede de fabrication additive mettant en oeuvre une telle machine | |
| EP0913217B1 (de) | Vorrichtung zum Verteilen von Schlackenpulver und Stranggiessanlage mit einer derartigen Verteilungsvorrichtung | |
| EP2618949A1 (de) | Vorrichtung und verfahren zum waschen der innenflächen einer kammer | |
| WO2020161266A1 (fr) | Bec de remplissage a depression | |
| EP2229259A1 (de) | Form zum aluminothermischen direktgiess-schweissen | |
| FR2690364A1 (fr) | Procédé et appareil de coulée d'une bande de métal. | |
| FR2659593A1 (fr) | Dispositif pour la fabrication automatique de produits en beton moule necessitant un demoulage par retournement. | |
| BE1008394A6 (fr) | Dispositif de raccordement et d'echange d'un tube de coulee sur un recipient contenant un metal en fusion. | |
| EP0384870B1 (de) | Kernschiessmaschine | |
| EP1132163A1 (de) | Gerillter feuerfester Formkörper für metallurgischen Guss, Zusammensetzung feuerfester Formkörper, Gussvorrichtung und Verfahren zur Wiederherstellung der Oberfläche eines feuerfesten Formkörpers | |
| EP0067760A1 (de) | Einrichtung zum Verteilen, Orientieren und Positionieren von Achsen zu einer automatischen Maschine | |
| EP0242347A2 (de) | Vorrichtung zum Giessen einer flüssig-festen Mischung | |
| EP0327526B1 (de) | Vorrichtung zum Kühlen eines Metalls während des Giessens | |
| WO1995015234A1 (fr) | Dispositif d'alimentation pour le depot par simple gravite d'un materiau granuleux sur la surface d'un metal liquide coule en continu | |
| FR2642679A3 (fr) | Dispositif d'elimination des inclusions non metalliques dans un repartiteur de coulee continue de l'acier | |
| FR2700495A1 (fr) | Procédé et dispositif pour la préparation de fûts métalliques usagés en vue de faciliter leur manutention et leur recyclage. | |
| BE1004046A3 (fr) | Dispositif de dosage et de transport d'une masse pulverulente. | |
| EP1142660A1 (de) | Gerillter feuerfester Formkörper für metallurgischen Guss, Zusammensetzung feuerfester Formkörper und Gussvorrichtung der eine solche Zusammensetzung umfasst | |
| FR2572969A1 (fr) | Dispositif reglable de generation d'une vague de soudure pour machine de soudage a la vague | |
| FR3050447A1 (fr) | Dispositif de distribution regulee de composants | |
| EP3885190B1 (de) | Halbrunder kübel mit schubboden, der durch eine öffnung in einem stützrahmen der rückwand entleert wird | |
| EP0234978A1 (de) | Verteiler für zylindrische Röhrchen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB IE IT LI LU NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 19990710 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH DE DK ES FI FR GB IE IT LI LU NL PT SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20011024 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB IE IT LI LU NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020508 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020508 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020508 |
|
| REF | Corresponds to: |
Ref document number: 217223 Country of ref document: AT Date of ref document: 20020515 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| REF | Corresponds to: |
Ref document number: 69805263 Country of ref document: DE Date of ref document: 20020613 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020808 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020808 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020808 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20020721 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2173559 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D Ref document number: 0913217E Country of ref document: IE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CJ |
|
| 26N | No opposition filed |
Effective date: 20030211 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20071119 Year of fee payment: 10 Ref country code: ES Payment date: 20071022 Year of fee payment: 10 Ref country code: DE Payment date: 20071010 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20071011 Year of fee payment: 10 Ref country code: IT Payment date: 20071020 Year of fee payment: 10 Ref country code: AT Payment date: 20071017 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20071105 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20071019 Year of fee payment: 10 Ref country code: FR Payment date: 20071030 Year of fee payment: 10 |
|
| BERE | Be: lapsed |
Owner name: SOC. D'ETUDES ET DE REALISATIONS TECHNIQUES *SERT Effective date: 20081031 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20081014 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20090630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081014 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090501 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081014 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081031 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081031 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081014 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20081015 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081015 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20081014 |