EP0918581B1 - Hitzeschild - Google Patents
Hitzeschild Download PDFInfo
- Publication number
- EP0918581B1 EP0918581B1 EP97932924A EP97932924A EP0918581B1 EP 0918581 B1 EP0918581 B1 EP 0918581B1 EP 97932924 A EP97932924 A EP 97932924A EP 97932924 A EP97932924 A EP 97932924A EP 0918581 B1 EP0918581 B1 EP 0918581B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- heat shield
- shield panel
- sheet
- troughs
- ridges
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 229910052751 metal Inorganic materials 0.000 claims description 8
- 239000002184 metal Substances 0.000 claims description 8
- 239000004411 aluminium Substances 0.000 claims description 3
- 229910052782 aluminium Inorganic materials 0.000 claims description 3
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 3
- 229910045601 alloy Inorganic materials 0.000 claims description 2
- 239000000956 alloy Substances 0.000 claims description 2
- 238000000034 method Methods 0.000 description 8
- 238000004519 manufacturing process Methods 0.000 description 2
- 238000007493 shaping process Methods 0.000 description 2
- 229910000838 Al alloy Inorganic materials 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D13/00—Corrugating sheet metal, rods or profiles; Bending sheet metal, rods or profiles into wave form
- B21D13/10—Corrugating sheet metal, rods or profiles; Bending sheet metal, rods or profiles into wave form into a peculiar profiling shape
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D13/00—Corrugating sheet metal, rods or profiles; Bending sheet metal, rods or profiles into wave form
- B21D13/04—Corrugating sheet metal, rods or profiles; Bending sheet metal, rods or profiles into wave form by rolling
-
- E—FIXED CONSTRUCTIONS
- E04—BUILDING
- E04C—STRUCTURAL ELEMENTS; BUILDING MATERIALS
- E04C2/00—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels
- E04C2/02—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels characterised by specified materials
- E04C2/08—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels characterised by specified materials of metal, e.g. sheet metal
-
- E—FIXED CONSTRUCTIONS
- E04—BUILDING
- E04C—STRUCTURAL ELEMENTS; BUILDING MATERIALS
- E04C2/00—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels
- E04C2/30—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels characterised by the shape or structure
- E04C2/32—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels characterised by the shape or structure formed of corrugated or otherwise indented sheet-like material; composed of such layers with or without layers of flat sheet-like material
- E04C2/326—Building elements of relatively thin form for the construction of parts of buildings, e.g. sheet materials, slabs, or panels characterised by the shape or structure formed of corrugated or otherwise indented sheet-like material; composed of such layers with or without layers of flat sheet-like material with corrugations, incisions or reliefs in more than one direction of the element
Definitions
- This invention is concerned with a heat shield panel which comprises at least one sheet of metal.
- sheets of metal can be strengthened by shaping them into corrugations, thereby enabling thinner sheets to be used for certain applications.
- corrugated roofing sheets are widely used.
- the heat shield panel according to the invention has parallel upstanding ridges with troughs between them, these troughs having reentrant side walls. It is found that the panel has increased stiffness in all directions in the plane of the panel and can be bent into complex shapes. A method for manufacturing such a panel does not require expensive tooling. All that is required is one or two sets (depending on whether the same set is used for both corrugating operations) of corrugating rollers.
- Such corrugating rollers are well-known as they are used to corrugate metal sheets for, eg, roofing and to corrugate cardboard. Such rollers have sinusoidal ridges extending along their surfaces.
- a set of rollers comprises an upper and a lower roller whose ridges mesh with one another and press a sheet into corrugations as it passes through the nip between the rollers.
- said angle between the corrugating directions can be as low as 10°, it is preferred that said angle is at least 30°, eg 45°, and, most preferably, said angle is substantially 90°.
- the corrugating may be carried out by passing the sheet between two sets of corrugating rollers which are arranged to produce similar corrugations, ie the depth and spacing of the ridges on the corrugating rollers may be the same for both corrugating operations. Indeed, the same rollers could be used for both corrugating operations. However, it is possible to vary the corrugation depth and/or spacing between the corrugating operations, eg to vary the stiffness of the panel in different directions or to produce uniform stiffness.
- Said corrugations extending in the first direction may be generally sinusoidal, when viewed in transverse cross-section. It is, however, possible to use corrugations with other cross-sections.
- a heat shield panel according to the invention has a very complex shape, it can be manufactured very simply.
- the variation in height of the ridges is substantially sinusoidal.
- the troughs must conform to the width and height variations of the ridges.
- said troughs vary in depth along their length with the greatest depth occurring at the narrowest points of the troughs.
- the lowest points of the ridges may be lower than the highest points of the troughs, but, of course, such lowest and highest points are displaced from one another longitudinally of the ridges or troughs.
- the ridges may each have a crest which is substantially flat in a direction transverse to the length of the ridge.
- a heat shield panel according to a preferred embodiment of the invention may be formed from, eg, aluminium or an alloy thereof or steel.
- the sheets may have a thickness of at least 125 microns. Thicknesses of 0.3 to 1mm have been found to be appropriate but, clearly, depending on the metal involved, there is a limit to the thickness of sheet which can be formed into a panel according to the invention.
- the illustrative method which is not part of the invention as claimed, forms the heat shield panel 10 by shaping a sheet of metal 12, the sheet being made of aluminium alloy and being 0.3mm in thickness. At the beginning of the illustrative method, the sheet 12 is planar.
- the illustrative method firstly, comprises corrugating the sheet 12 with corrugations which extend parallel to one another in a first direction. These corrugations are of conventional form, being sinusoidal in transverse cross-section, and extend parallel to one another in the first direction across the sheet 12. This stage of the illustrative method is carried out by passing the sheet 12 between corrugating rollers of conventional type.
- the illustrative method comprises corrugating the already corrugated sheet 12 with corrugations which extend parallel to one another in a second direction, said second direction being inclined at an angle of 90° to said first direction. This is carried out by passing said sheet 12 between similar corrugating rollers to those used in the first corrugating operation. However, in the second corrugating operation, the direction of travel of the sheet 12 relative to the rollers is at 90° to its direction of travel relative to the corrugating rollers in the first corrugating operation.
- the illustrative heat shield panel 10 formed by the illustrative method is shown in the drawings.
- the sheet 12 is formed into a plurality of generally parallel upstanding ridges 20 separated by troughs 22.
- the longitudinal direction of the ridges 20 represents the longitudinal direction of the corrugations formed by the first corrugating operation, ie said first direction, but these corrugations have been deformed by the second corrugating operation, preformed at 90° to the first corrugating operation in said second direction.
- the shape of the ridges 20 and troughs 22 is complex and is described below.
- Figure 1 shows, in plan view, a portion of the upper surface of the heat shield panel 10.
- the lower surface of the sheet 10, not shown, has a similar appearance to said upper surface except that the lower surface is off-set by half the spacing between adjacent ridges 20.
- Each ridge 20 has a relatively broad crest. This crest varies in height along the ridge 20 (as shown in Figure 4) having peaks 20a and hollows 20b. As shown in Figure 2, the crest of the ridge 20 is dished downwardly at its peaks 20a but, as shown in Figure 3, the crest is substantially flat at its hollows 20b. As shown in Figures 1 to 3, the crest varies regularly in width along the ridge 20, having its greatest width at the hollows 20b and its smallest width at the peaks 20a. Figure 1 also illustrates that the narrowest points of the ridges 20 are spaced from one another along lines extending normally to the longitudinal direction of the ridges.
- the troughs 22 each have a relatively broad bottom which corresponds to the shape of the crests of the ridges 20.
- each bottom has broad peaks 22a which are substantially flat in a direction transverse to the length of the trough 22 (see Figures 2 and 3), and narrow hollows 22b which are dished upwardly.
- Figure 4 where the trough bottom of the lower side of the sheet 12 is represented by the lower side of the Figure, it can be seen how the bottom varies in height along the trough 22. The bottom also varies regularly in width along the trough 20 (as shown in Figure 1).
- the troughs 22 have side walls 24 (which also form the side walls of the ridges 20). These side walls 24 are reentrant so that the troughs 22 are narrower at their mouths between the crests of the ridges than at their bottoms. Each wall 24 follows the undulations of the trough 22 and meets the crest of one of the ridges 20 and the bottom of one of the troughs 22 at an angle which is less than 90°.
- the heat shield panel 10 derives stiffness from its shape and can be bent both about lines extending longitudinally of the ridges 20 and (less easily) about lines extending transversely thereof.
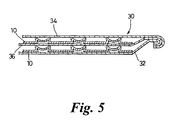
- FIG. 5 shows further embodiment of a heat shield panel 30 which comprises a shallow box formed by a bottom sheet 32 and a top sheet 34. Side walls of the box are formed by upwardly extending edges of the sheet 32. The top sheet 34 is turned over the edges of the bottom sheet 34 to join the sheets 32 and 34 together to close the box.
- the sheets 32 and 34 are formed of aluminium.
- the heat shield panel 30 also comprises two panels 10 as described in relation to Figures 1 to 4 and shown in Figure 6.
- the shield 30 also comprises a layer of thermally insulating paper 36 which is disposed between the two panels 10.
- the paper 36 may, for example be formed from the material marketed under the trade name "Fiberfrax 970".
- One of these panels 10 rests on the upper surface of the bottom sheet 32 with the paper 36 on top of it and the other panel 10 is on top of the paper 36 and beneath the lower surface of the sheets 34.
- the heat shield panel 30 can be utilised with either the lower surface of the sheet 32 or the upper surface of the sheet 34 facing a source of heat.
- the heat shield panel 30 has air trapped in it as the ridges 20 hold the sheets 32 and 34 apart. Modifications of the heat shield panel 30 can omit the paper 36 or may have only one panel 10 or more than two panels 10.
- the sheets 32 and 34 prevent dirt from accumulating in the folds of the panels 10.
- Figure 6 illustrates the appearance of the illustrative heat shield panel 10 as scanned by a computer.
- the figure shows the ridges 20 and the troughs 22 and also the peaks 20a and 22a and the hollows 20b and 22b.
Landscapes
- Engineering & Computer Science (AREA)
- Architecture (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Mechanical Engineering (AREA)
- Building Environments (AREA)
- Panels For Use In Building Construction (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
- Shielding Devices Or Components To Electric Or Magnetic Fields (AREA)
Claims (4)
- Hitzeschildpaneel bzw. -platte bzw. -tafel (10;30), welches mindestens eine Metallplatte bzw. -blech (12) umfasst, dadurch gekennzeichnet, dass das Blech (10) in eine Vielzahl von im allgemeinen hochstehende Grate bzw. Wulste bzw. Riffel bzw. Rücken bzw. Firste bzw. Stege (20) geformt ist, welche durch Mulden bzw. Rücksprünge (22) getrennt sind, wobei die Mulden (22) einspringende Seitenwände (24) aufweisen, wobei sich jeder Steg (20) in der Breite entlang seiner Länge in einer regelmäßigen Weise verändert und sich in der Höhe entlang der Länge des Steges (20) verändert, wobei die größte Höhe an den schmälsten Punkten des Steges (20) auftritt, und wobei die Mulden (22) sich in ihrer Tiefe entlang ihrer Länge verändern, wobei die größte Tiefe an den schmälsten Punkten der Mulden (22) auftritt.
- Hitzeschildpaneel gemäß Anspruch 1, dadurch gekennzeichnet, dass die Veränderung in der Höhe der Stege (20) im wesentlichen Sinusform besitzt.
- Hitzeschildpaneel gemäß einem der Ansprüche 1 und 2, dadurch gekennzeichnet, dass das Paneel (10;30) aus Alumminium oder einer Legierung davon ausgebildet ist.
- Hitzeschildpaneel gemäß einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, dass das Metalblech (12) eine Dicke von 0,3 bis 1 mm aufweist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| GB9616882 | 1996-08-10 | ||
| GBGB9616882.8A GB9616882D0 (en) | 1996-08-10 | 1996-08-10 | Forming a panel |
| PCT/GB1997/001975 WO1998006517A1 (en) | 1996-08-10 | 1997-07-18 | Method of forming a metal sheet and panel comprising such a sheet |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0918581A1 EP0918581A1 (de) | 1999-06-02 |
| EP0918581B1 true EP0918581B1 (de) | 2000-06-14 |
Family
ID=10798350
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97932924A Expired - Lifetime EP0918581B1 (de) | 1996-08-10 | 1997-07-18 | Hitzeschild |
Country Status (8)
| Country | Link |
|---|---|
| EP (1) | EP0918581B1 (de) |
| JP (1) | JP3233364B2 (de) |
| AU (1) | AU3628997A (de) |
| BR (1) | BR9711118A (de) |
| DE (1) | DE69702317T2 (de) |
| ES (1) | ES2147012T3 (de) |
| GB (1) | GB9616882D0 (de) |
| WO (1) | WO1998006517A1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1779940A1 (de) * | 2005-10-27 | 2007-05-02 | Etablissements Primet | Verfahren zum Hertsellen von metallischen geflechteten Strukturen sowie durch das Verfahren hergestellte Strukture |
| DE102007017340B4 (de) * | 2007-04-12 | 2015-12-03 | Federal-Mogul Sealing Systems Gmbh | Schutzschild zur thermischen und akustischen Abschirmung von Bauteilen einer Verbrennungskraftmaschine |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7308629B2 (en) | 2004-12-07 | 2007-12-11 | Texas Instruments Incorporated | Addressable tap domain selection circuit with TDI/TDO external terminal |
| US6935997B2 (en) | 2000-09-14 | 2005-08-30 | Rutgers, The State University Of New Jersey | Patterning technology for folded sheet structures |
| DK200600137A (da) * | 2005-12-21 | 2007-06-22 | Petersen Peder Vejsig | Varmeveksler i tynde profilerede plader |
| JP5705402B2 (ja) * | 2008-02-08 | 2015-04-22 | ニチアス株式会社 | アルミニウム成形板の製造方法 |
| KR100958733B1 (ko) * | 2009-11-10 | 2010-05-18 | 주식회사 모팜 | 차열용 다층 롤포밍 시트 및 그 제조방법 |
| US8777825B1 (en) | 2010-10-12 | 2014-07-15 | Daniel Kling | Methods for designing boxes and other types of containers |
| JP2012167464A (ja) * | 2011-02-14 | 2012-09-06 | Inosho:Kk | 金属パネル |
| WO2013046326A1 (ja) * | 2011-09-27 | 2013-04-04 | 三和パッキング工業株式会社 | 多方向波付け材の製造方法、多方向波付け材、及び波付け材製造装置 |
| JP4970626B1 (ja) * | 2011-09-27 | 2012-07-11 | 三和パッキング工業株式会社 | 多方向波付け材の製造方法、多方向波付け材、及び波付け材製造装置 |
| US10399134B2 (en) | 2015-07-31 | 2019-09-03 | Nissan Motor Co., Ltd. | Metal plate and metal cover employing same |
| JP6291106B1 (ja) * | 2017-03-29 | 2018-03-14 | 三和パッキング工業株式会社 | 成形材及びその製造方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE46795C (de) * | H. bellach in Jena. W. G. Bahnhofstrafse | Verfahren und Walzwerk zur Herstellung von doppelt gewelltem Blech | ||
| DE240269C (de) * | 1910-08-10 | 1911-11-01 | ||
| FR990018A (fr) * | 1948-12-31 | 1951-09-17 | Mannesmann Roehren Werke Ag | Tôle ondulée et ses applications |
| FR59765E (fr) * | 1949-11-21 | 1954-07-19 | Mannesmann Roehren Werke Ag | Tôle ondulée et ses applications |
| US3217845A (en) * | 1961-02-06 | 1965-11-16 | Crown Zellerbach Corp | Rigidified corrugated structure |
-
1996
- 1996-08-10 GB GBGB9616882.8A patent/GB9616882D0/en active Pending
-
1997
- 1997-07-18 EP EP97932924A patent/EP0918581B1/de not_active Expired - Lifetime
- 1997-07-18 AU AU36289/97A patent/AU3628997A/en not_active Abandoned
- 1997-07-18 BR BR9711118-0A patent/BR9711118A/pt not_active IP Right Cessation
- 1997-07-18 JP JP50946798A patent/JP3233364B2/ja not_active Expired - Fee Related
- 1997-07-18 WO PCT/GB1997/001975 patent/WO1998006517A1/en not_active Ceased
- 1997-07-18 DE DE69702317T patent/DE69702317T2/de not_active Expired - Lifetime
- 1997-07-18 ES ES97932924T patent/ES2147012T3/es not_active Expired - Lifetime
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1779940A1 (de) * | 2005-10-27 | 2007-05-02 | Etablissements Primet | Verfahren zum Hertsellen von metallischen geflechteten Strukturen sowie durch das Verfahren hergestellte Strukture |
| FR2892649A1 (fr) * | 2005-10-27 | 2007-05-04 | Primet Sarl Ets | Procede de fabrication de structures en metal tresse et les produits obtenus selon le procede |
| DE102007017340B4 (de) * | 2007-04-12 | 2015-12-03 | Federal-Mogul Sealing Systems Gmbh | Schutzschild zur thermischen und akustischen Abschirmung von Bauteilen einer Verbrennungskraftmaschine |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0918581A1 (de) | 1999-06-02 |
| AU3628997A (en) | 1998-03-06 |
| BR9711118A (pt) | 1999-09-08 |
| DE69702317D1 (de) | 2000-07-20 |
| DE69702317T2 (de) | 2001-02-15 |
| WO1998006517A1 (en) | 1998-02-19 |
| JP3233364B2 (ja) | 2001-11-26 |
| JP2001504393A (ja) | 2001-04-03 |
| ES2147012T3 (es) | 2000-08-16 |
| GB9616882D0 (en) | 1996-09-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6139974A (en) | Forming a composite panel | |
| US4862666A (en) | Profiled sheet for building purposes | |
| EP0918581A1 (de) | Verfahren und herstellung einer metallplatte und paneelstruktur mit dieser platte | |
| US6183836B1 (en) | Folded-sheet honeycomb structure | |
| US9517501B2 (en) | Sheet forming tool and a method for the manufacture of a corrugated sheet | |
| US7024907B2 (en) | Method and device for manufacturing a structured packing corrugation, and corresponding fluid-treatment apparatus | |
| GB2316028A (en) | Forming a panel | |
| US5126183A (en) | Curved paneling including honeycomb core material having crimps in one edge | |
| US5064493A (en) | Method of producing curved honeycomb core material having crimps in one edge | |
| GB2316027A (en) | Forming a composite panel | |
| EP0680793B1 (de) | Verfahren und Vorrichtung zum Herstellen von einer Baustrukturform mit einem Flach versteiften Plattenteil | |
| KR880013629A (ko) | 경사파형의 금속박판을 제조하는 방법 | |
| JP3420351B2 (ja) | プレス成形用ブランク材及びブランクダイ | |
| GB2101507A (en) | Method and apparatus for bending corrugated sheet | |
| EP0380281A2 (de) | Anschlussprofil | |
| JPS6119349Y2 (de) | ||
| JPS6039823B2 (ja) | 彎曲状建築用板 | |
| EP0146352A2 (de) | Verfahren und Vorrichtung zum Biegen von Wellblech | |
| JPS6039821B2 (ja) | 彎曲状馳締建築用板 | |
| JPS63280148A (ja) | 彎曲状建築用板 | |
| JPS6016173Y2 (ja) | 彎曲状馳締建築用板 | |
| JPH0694705B2 (ja) | 二重折版材 | |
| JPS6039822B2 (ja) | 彎曲状馳締建築用板 | |
| JPH11293892A (ja) | 外装用折板 | |
| JPH08326243A (ja) | 角樋の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19990115 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT |
|
| RIC1 | Information provided on ipc code assigned before grant |
Free format text: 6B 21D 13/04 A, 6E 04C 2/34 B |
|
| RTI1 | Title (correction) |
Free format text: HEAT SHIELD PANEL |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19991103 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| ITF | It: translation for a ep patent filed | ||
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT |
|
| REF | Corresponds to: |
Ref document number: 69702317 Country of ref document: DE Date of ref document: 20000720 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2147012 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 69702317 Country of ref document: DE Representative=s name: MUELLER-BORE & PARTNER PATENTANWAELTE, EUROPEA, DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: FEDERAL-MOGUL CORPORATION Effective date: 20130225 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 69702317 Country of ref document: DE Representative=s name: MUELLER-BORE & PARTNER PATENTANWAELTE PARTG MB, DE Effective date: 20130118 Ref country code: DE Ref legal event code: R082 Ref document number: 69702317 Country of ref document: DE Representative=s name: MUELLER-BORE & PARTNER PATENTANWAELTE, EUROPEA, DE Effective date: 20130118 Ref country code: DE Ref legal event code: R081 Ref document number: 69702317 Country of ref document: DE Owner name: FEDERAL-MOGUL LLC (N. D. GES. D. STAATES DELAW, US Free format text: FORMER OWNER: FEDERAL-MOGUL TECHNOLOGY LTD., RUGBY, WARWICKSHIRE, GB Effective date: 20130118 Ref country code: DE Ref legal event code: R081 Ref document number: 69702317 Country of ref document: DE Owner name: FEDERAL-MOGUL CORPORATION (N.D.GES.D. STAATES , US Free format text: FORMER OWNER: FEDERAL-MOGUL TECHNOLOGY LTD., RUGBY, WARWICKSHIRE, GB Effective date: 20130118 Ref country code: DE Ref legal event code: R081 Ref document number: 69702317 Country of ref document: DE Owner name: FEDERAL-MOGUL CORPORATION (N.D.GES.D. STAATES , US Free format text: FORMER OWNER: FEDERAL-MOGUL TECHNOLOGY LTD., RUGBY, GB Effective date: 20130118 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Owner name: FEDERAL-MOGUL CORPORATION, US Effective date: 20130313 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20130321 AND 20130327 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20140624 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20140731 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20140624 Year of fee payment: 18 Ref country code: ES Payment date: 20140716 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20140717 Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69702317 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20150718 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150718 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150718 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160202 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20160331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150731 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20160826 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150719 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 69702317 Country of ref document: DE Representative=s name: MUELLER-BORE & PARTNER PATENTANWAELTE PARTG MB, DE Ref country code: DE Ref legal event code: R081 Ref document number: 69702317 Country of ref document: DE Owner name: FEDERAL-MOGUL LLC (N. D. GES. D. STAATES DELAW, US Free format text: FORMER OWNER: FEDERAL-MOGUL CORPORATION (N.D.GES.D. STAATES DELAWARE), SOUTHFIELD, MICH., US |