EP1225324B1 - Surface de glissement d'un cylindre - Google Patents
Surface de glissement d'un cylindre Download PDFInfo
- Publication number
- EP1225324B1 EP1225324B1 EP02000872A EP02000872A EP1225324B1 EP 1225324 B1 EP1225324 B1 EP 1225324B1 EP 02000872 A EP02000872 A EP 02000872A EP 02000872 A EP02000872 A EP 02000872A EP 1225324 B1 EP1225324 B1 EP 1225324B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- running surface
- cylindrical
- wear layer
- partial
- cylindrical running
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000576 coating method Methods 0.000 claims description 11
- 238000000034 method Methods 0.000 claims description 8
- 239000011248 coating agent Substances 0.000 claims description 7
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims description 5
- 229910045601 alloy Inorganic materials 0.000 claims description 5
- 239000000956 alloy Substances 0.000 claims description 5
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 3
- 239000010949 copper Substances 0.000 claims description 3
- 230000003247 decreasing effect Effects 0.000 claims description 3
- 229910052742 iron Inorganic materials 0.000 claims description 3
- 229910001092 metal group alloy Inorganic materials 0.000 claims description 3
- 229910000838 Al alloy Inorganic materials 0.000 claims description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims description 2
- 229910052799 carbon Inorganic materials 0.000 claims description 2
- 238000002485 combustion reaction Methods 0.000 claims description 2
- 229910052802 copper Inorganic materials 0.000 claims description 2
- 229910052750 molybdenum Inorganic materials 0.000 claims description 2
- 229910052759 nickel Inorganic materials 0.000 claims description 2
- 229910052720 vanadium Inorganic materials 0.000 claims description 2
- 238000004519 manufacturing process Methods 0.000 claims 2
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims 1
- 229910000570 Cupronickel Inorganic materials 0.000 claims 1
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 claims 1
- 229910052782 aluminium Inorganic materials 0.000 claims 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims 1
- YOCUPQPZWBBYIX-UHFFFAOYSA-N copper nickel Chemical compound [Ni].[Cu] YOCUPQPZWBBYIX-UHFFFAOYSA-N 0.000 claims 1
- 230000005672 electromagnetic field Effects 0.000 claims 1
- WPBNNNQJVZRUHP-UHFFFAOYSA-L manganese(2+);methyl n-[[2-(methoxycarbonylcarbamothioylamino)phenyl]carbamothioyl]carbamate;n-[2-(sulfidocarbothioylamino)ethyl]carbamodithioate Chemical compound [Mn+2].[S-]C(=S)NCCNC([S-])=S.COC(=O)NC(=S)NC1=CC=CC=C1NC(=S)NC(=O)OC WPBNNNQJVZRUHP-UHFFFAOYSA-L 0.000 claims 1
- 229910052751 metal Inorganic materials 0.000 claims 1
- 239000002184 metal Substances 0.000 claims 1
- 239000011733 molybdenum Substances 0.000 claims 1
- LEONUFNNVUYDNQ-UHFFFAOYSA-N vanadium atom Chemical compound [V] LEONUFNNVUYDNQ-UHFFFAOYSA-N 0.000 claims 1
- 238000007750 plasma spraying Methods 0.000 description 5
- KEUKAQNPUBYCIC-UHFFFAOYSA-N ethaneperoxoic acid;hydrogen peroxide Chemical compound OO.CC(=O)OO KEUKAQNPUBYCIC-UHFFFAOYSA-N 0.000 description 3
- 238000010285 flame spraying Methods 0.000 description 3
- 238000003754 machining Methods 0.000 description 3
- 239000000654 additive Substances 0.000 description 2
- 238000005422 blasting Methods 0.000 description 2
- 210000000078 claw Anatomy 0.000 description 2
- 238000005507 spraying Methods 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 229910000881 Cu alloy Inorganic materials 0.000 description 1
- 229910000990 Ni alloy Inorganic materials 0.000 description 1
- 230000001133 acceleration Effects 0.000 description 1
- 230000001464 adherent effect Effects 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 238000009792 diffusion process Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- -1 etc. Substances 0.000 description 1
- 229910001234 light alloy Inorganic materials 0.000 description 1
- 229910052748 manganese Inorganic materials 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 238000003801 milling Methods 0.000 description 1
- 238000007788 roughening Methods 0.000 description 1
- 229910052710 silicon Inorganic materials 0.000 description 1
- 238000009987 spinning Methods 0.000 description 1
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F1/00—Cylinders; Cylinder heads
- F02F1/18—Other cylinders
- F02F1/20—Other cylinders characterised by constructional features providing for lubrication
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
- C23C4/14—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying for coating elongate material
- C23C4/16—Wires; Tubes
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02B—INTERNAL-COMBUSTION PISTON ENGINES; COMBUSTION ENGINES IN GENERAL
- F02B77/00—Component parts, details or accessories, not otherwise provided for
- F02B77/02—Surface coverings of combustion-gas-swept parts
Definitions
- the invention relates to a cylindrical running surface, for example a cylinder liner or a cylinder bore, made of a light metal alloy with a defined Verkrall Quilt a not yet coated cylindrical tread on which a wear layer is adherent applied.
- Such a cylindrical tread is for example from the article by Hans Rininger "flame-sprayed plain bearings" from " The Machine Market “(1954, No. 7, page 6 ) known.
- sawtooth punctures or threads are introduced with longitudinal grooves in the cylindrical tread to ensure a torsion-resistant adhesion.
- this type of pretreatment has proved to be unsuitable.
- a wear layer of an Fe-based alloy with the light metal alloy Additives such as C, Mn, Mo, V, etc., an Al-based alloy with additives such as Si, Fe, Cu, Ni, etc., or a copper / nickel alloy is applied.
- the wear layer is preferably applied by welding, plasma spraying, flame spraying or high-speed jet spraying.
- the light alloy to be coated is roughened by a blasting process (see, for example, US Pat GB-A-408 067 ).
- this type of pretreatment is very complicated due to the beam systems to be used and creates only an undefined surface structure that causes an uneven stress introduction into the wear layer, with the result that not sufficient adhesion of the wear layer is guaranteed in all load cases.
- the present invention is therefore based on the object to provide a remedy for the above-described problems.
- This Verkrall Scheme first leads to a defined increase in the adhesive surface of the tread to be coated. In addition, it comes in the subsequent coating process in the tips to a higher energy load, resulting in part to a reproducible diffusion compensation of the wear layer with the base material. Also, at the tips of the Verkrall Design to melting, which further improve the adhesion of the wear layer.
- the distance to the surface to be coated is so small that no maximum acceleration can be achieved in the coating medium, because of the low kinetic energy, the adhesion is reduced.
- optimum adhesion is achieved when it hits the surface to be coated vertically.
- the angle of incidence of the media jet is significantly less than 90 °, resulting in low adhesion of the coating medium in this zone.
- the macroscopic surface structure produced in such a targeted manner can be formed in the form of preferably grooves extending in the circumferential direction or else by helical thread-like profiles. Furthermore, the adhesion in the radial and / or axial direction can be improved by undercuts.
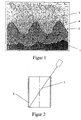
- FIG. 1 shows a longitudinal section through an inventively designed cylindrical tread.
- the cylindrical tread 1 consists of a known aluminum alloy.
- a Verkrall Design 2 in the present embodiment, a threaded profile were rotated in a known manner.
- the Verkrall Designen 2 invention can also be introduced in various other ways, such as spinning, cutting, milling, etc. in the cylindrical tread 1.
- the light undercuts 4 shown in the present embodiment can be attached to the Verkrall Modellen 2 by a subsequent forming process.
- FIG. 2 A schematic representation of the machining process for applying one of the wear layer 3 through the media jet 5 shows FIG. 2 ,
- the Verkrall Siemens 2 ensures that the angle of incidence of the media beam 5 is nearly 90 °. It shows FIG. 3 a first embodiment of the Verkrall Design 2, which ensures this defined angle of incidence.
- the alignment of the partial flanks 6 is constant over the entire cylindrical tread 1, which results in that the media jet 5 is moved translationally along the longitudinal axis of the cylindrical tread 1 during the coating process (see dotted lines).
- FIG. 4 shows a Verkrall Cook 2, the partial edges 6 in the longitudinal direction of the cylindrical tread 1 have a steadily decreasing angle of attack a.
- a Verkrall Quilt 2 can be prepared in a known manner, for example by a CNC machine.
- the media jet 5 then needs to perform as shown only a rotational movement, which in turn leads to a simplification of the machining process.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Plasma & Fusion (AREA)
- Physics & Mathematics (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- General Engineering & Computer Science (AREA)
- Combustion & Propulsion (AREA)
- Coating By Spraying Or Casting (AREA)
- Cylinder Crankcases Of Internal Combustion Engines (AREA)
- Physical Vapour Deposition (AREA)
Claims (6)
- Surface de glissement cylindrique pour le carter de vilebrequin d'un moteur à combustion interne, réalisée d'un alliage de métal léger avec des structures d'accrochage (2) radiales, chaque flanc partiel (6) de ladite structure d'accrochage (2) étant formé de manière à ce que les flancs partiels (6) soient inclinés par rapport à un axe longitudinal de la surface de glissement cylindrique (1) de sorte que l'on forme un profilé ressemblant à un filetage, et une couche anti-usure (3) métallique déposée d'une manière fermement adhérente sur ladite surface de glissement (1), caractérisée en ce que la surface de glissement est formée d'un alliage d'aluminium et la couche anti-usure (3) est formée- d'un alliage à base de fer avec l'addition de carbone, manganèse, molybdène et/ou vanadium,- d'un alliage à base d'aluminium avec l'addition de fer, cuivre ou nickel, ou- d'un alliage cuivre-nickel,et les flancs partiels (6) des structures d'accrochage (2) présentent un angle d'inclinaison α continûment décroissant dans la direction longitudinale de la surface de glissement (1) cylindrique.
- Surface de glissement cylindrique selon la revendication 1, caractérisée en ce que la structure de surface comprend des contre-dépouilles.
- Surface de glissement cylindrique selon l'une des revendications 1 et 2, caractérisée en ce que une structure d'accrochage définie est formée dans la surface de glissement selon la direction axiale.
- Procédé de fabrication d'une surface de glissement (1) cylindrique selon l'une des revendications 1 à 3, dans lequel une structure d'accrochage (2) en forme d'un profilé ressemblant à un filetage est formée dans la surface de glissement (1) de l'alésage d'un cylindre, et dans lequel une couche anti-usure (3) est ensuite appliquée sur ladite surface de glissement, caractérisé en ce que les flancs partiels (6) de la structure d'accrochage (2) sont formés dans la direction longitudinale de ladite surface de glissement (1) cylindrique avec un angle d'inclinaison α continûment décroissant.
- Procédé de fabrication d'une surface de glissement cylindrique selon la revendication 4, caractérisé en ce que la couche anti-usure (3) est appliquée par moyen d'un jet de médium d'une buse de déposition, ladite buse de déposition étant orientée à un flanc partiel (6) de la structure d'accrochage (2) sous un angle de jet de 90°.
- Procédé selon la revendication 4 ou 5, caractérisé en ce que le jet de médium est focalisé par des champs électromagnétiques.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP09167884.7A EP2112359B2 (fr) | 2001-01-20 | 2002-01-15 | Surface de glissement d'un cylindre |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10102654 | 2001-01-20 | ||
| DE10102654 | 2001-01-20 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP09167884.7A Division EP2112359B2 (fr) | 2001-01-20 | 2002-01-15 | Surface de glissement d'un cylindre |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1225324A2 EP1225324A2 (fr) | 2002-07-24 |
| EP1225324A3 EP1225324A3 (fr) | 2003-03-26 |
| EP1225324B1 true EP1225324B1 (fr) | 2009-10-14 |
Family
ID=7671293
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02000872A Expired - Lifetime EP1225324B1 (fr) | 2001-01-20 | 2002-01-15 | Surface de glissement d'un cylindre |
| EP09167884.7A Expired - Lifetime EP2112359B2 (fr) | 2001-01-20 | 2002-01-15 | Surface de glissement d'un cylindre |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP09167884.7A Expired - Lifetime EP2112359B2 (fr) | 2001-01-20 | 2002-01-15 | Surface de glissement d'un cylindre |
Country Status (3)
| Country | Link |
|---|---|
| EP (2) | EP1225324B1 (fr) |
| DE (1) | DE50213911D1 (fr) |
| ES (2) | ES2411477T5 (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102010016745A1 (de) * | 2010-05-03 | 2011-11-03 | Dr. Ing. H.C. F. Porsche Aktiengesellschaft | Verfahren zur strukturierten Vorbehandlung einer Lauffläche |
| EP2307162B1 (fr) | 2008-08-05 | 2017-08-30 | Martinrea Honsel Germany GmbH | Procédé et outil pour produire une surface présentant une rugosité prédéfinie |
| US9863030B2 (en) | 2015-03-02 | 2018-01-09 | GM Global Technology Operations LLC | Stress relief of mechanically roughened cylinder bores for reduced cracking tendency |
| DE102016116815A1 (de) | 2016-09-08 | 2018-03-08 | Dr. Ing. H.C. F. Porsche Aktiengesellschaft | Verfahren zur Beschichtung eines Zylinders einer Verbrennungskraftmaschine und Zylinder für eine Verbrennungskraftmaschine |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102006004769B4 (de) | 2006-02-02 | 2022-05-25 | Mercedes-Benz Group AG | Oberflächenkonditionierung für thermische Spritzschichten |
| DE102007023418B4 (de) | 2007-05-18 | 2010-09-09 | Daimler Ag | Verfahren zum Aufrauen von Oberflächen für die spätere Aufbringung von Spritzschichten, entspechend aufgeraute Bauteile sowie beschichtete Metallbauteile |
| DE102008019933A1 (de) * | 2008-04-21 | 2009-10-22 | Ford Global Technologies, LLC, Dearborn | Vorrichtung und Verfahren zum Vorbereiten einer Oberfläche aus Metall für das Aufbringen einer thermisch gespritzten Schicht |
| DE102008022225A1 (de) | 2008-05-06 | 2009-11-12 | Daimler Ag | Verfahren zum Behandeln einer Oberfläche |
| DE102010064350A1 (de) | 2010-12-29 | 2012-07-05 | Robert Bosch Gmbh | Bremsscheibe und Verfahren zur Behandlung der Oberfläche einer Bremsscheibe |
| US8956700B2 (en) | 2011-10-19 | 2015-02-17 | General Electric Company | Method for adhering a coating to a substrate structure |
| DE102012021859B4 (de) | 2012-11-07 | 2018-10-18 | Daimler Ag | Verfahren zum thermischen Beschichten von Zylinderlaufflächen |
| DE102013011726A1 (de) | 2013-07-12 | 2015-01-29 | Bayerische Motorenwerke Aktiengesellschaft | Verfahren zum Bearbeiten einer Lauffläche eines Zylinders eines Verbrennungsmotors |
| DE102015112540A1 (de) | 2015-07-30 | 2017-02-16 | Bayerische Motoren Werke Aktiengesellschaft | Verfahren und Vorrichtung zum Beschichten einer Oberfläche |
| JP6441295B2 (ja) * | 2016-12-26 | 2018-12-19 | 本田技研工業株式会社 | 接合構造体及びその製造方法 |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB408067A (en) * | 1932-12-16 | 1934-04-05 | Heinrich Schluepmann | Improvements relating to a process for improving the wearing qualities of mechanicaland constructional parts of light metal and for reconditioning worn and damaged light metal parts |
| US2314902A (en) * | 1940-04-16 | 1943-03-30 | Metallizing Engineering Compan | Method for causing sprayed metal to adhere to metal surfaces |
| FR1354895A (fr) * | 1963-01-17 | 1964-03-13 | Sarl Rech S Etudes Production | Procédé de métallisation au pistolet de pièces en béryllium |
| US5380564A (en) * | 1992-04-28 | 1995-01-10 | Progressive Blasting Systems, Inc. | High pressure water jet method of blasting low density metallic surfaces |
| WO1996033837A1 (fr) * | 1995-04-25 | 1996-10-31 | Mdc Max Dätwyler Bleienbach Ag | Procede permettant de preparer la surface d'une piece comportant un materiau support metallique, et piece munie d'un materiau support metallique |
| EP0858519B1 (fr) * | 1995-10-31 | 2000-05-10 | Volkswagen Aktiengesellschaft | Procede de production d'une surface de frottement sur une piece metallique |
| US5622753A (en) * | 1996-04-08 | 1997-04-22 | Ford Motor Company | Method of preparing and coating aluminum bore surfaces |
| DE19614328A1 (de) * | 1996-04-11 | 1997-10-16 | Gehring Gmbh & Co Maschf | Verfahren zum Beschichten und/oder spanabhebenden Bearbeiten von vorbehandelten Werkstück-Oberflächen |
| US5691004A (en) * | 1996-07-11 | 1997-11-25 | Ford Global Technologies, Inc. | Method of treating light metal cylinder bore walls to receive thermal sprayed metal coatings |
| JP3798496B2 (ja) * | 1997-02-25 | 2006-07-19 | トヨタ自動車株式会社 | シリンダブロックのボア面の加工装置 |
-
2002
- 2002-01-15 EP EP02000872A patent/EP1225324B1/fr not_active Expired - Lifetime
- 2002-01-15 DE DE50213911T patent/DE50213911D1/de not_active Expired - Lifetime
- 2002-01-15 ES ES09167884T patent/ES2411477T5/es not_active Expired - Lifetime
- 2002-01-15 ES ES02000872T patent/ES2334770T3/es not_active Expired - Lifetime
- 2002-01-15 EP EP09167884.7A patent/EP2112359B2/fr not_active Expired - Lifetime
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2307162B1 (fr) | 2008-08-05 | 2017-08-30 | Martinrea Honsel Germany GmbH | Procédé et outil pour produire une surface présentant une rugosité prédéfinie |
| DE102010016745A1 (de) * | 2010-05-03 | 2011-11-03 | Dr. Ing. H.C. F. Porsche Aktiengesellschaft | Verfahren zur strukturierten Vorbehandlung einer Lauffläche |
| US9863030B2 (en) | 2015-03-02 | 2018-01-09 | GM Global Technology Operations LLC | Stress relief of mechanically roughened cylinder bores for reduced cracking tendency |
| DE102016116815A1 (de) | 2016-09-08 | 2018-03-08 | Dr. Ing. H.C. F. Porsche Aktiengesellschaft | Verfahren zur Beschichtung eines Zylinders einer Verbrennungskraftmaschine und Zylinder für eine Verbrennungskraftmaschine |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2112359B2 (fr) | 2021-10-06 |
| EP1225324A2 (fr) | 2002-07-24 |
| ES2411477T5 (es) | 2022-03-24 |
| EP2112359A1 (fr) | 2009-10-28 |
| EP2112359B1 (fr) | 2013-04-03 |
| EP1225324A3 (fr) | 2003-03-26 |
| ES2334770T3 (es) | 2010-03-16 |
| DE50213911D1 (de) | 2009-11-26 |
| ES2411477T3 (es) | 2013-07-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2112359B1 (fr) | Surface de glissement d'un cylindre | |
| EP1719572B1 (fr) | Procédé pour souder une couronne avec une boîte d'engrenage | |
| DE10014078C5 (de) | Verfahren zur Herstellung eines Schweißbolzens | |
| EP3325685B1 (fr) | Procédé pour recouvrir une surface de glissement de cylindre d'un bloc-cylindres, bloc-cylindres avec une surface de glissement de cylindre recouverte et moteur | |
| EP0683862A1 (fr) | Soupape a commande electromagnetique | |
| WO1995014851A1 (fr) | Arbre a cames creux en une seule piece et son procede de fabrication | |
| DE102021128374B4 (de) | Verfahren zur Herstellung einer Bremsscheibe und Bremsscheibe | |
| EP4217619B1 (fr) | Procédé de production d'élément de palier lisse, et élément, palier lisse et transmission d'éolienne | |
| DE102016100470A1 (de) | Baugruppe mit mindestens zwei Bauteilen einer Abgasanlage und Verfahren zum Fügen | |
| DE10312475B4 (de) | Nockenwelle | |
| WO2020239164A1 (fr) | Écrou profilé d'un mécanisme de vis-écrou, en particulier vis-écrou à billes d'un mécanisme de vis-écrou à billes et procédé pour la fabrication de celui-ci | |
| DE102018103326A1 (de) | Verbindungselement | |
| EP3601629B1 (fr) | Segment de piston comprenant une couche de rodage grenaillée et procédé pour sa fabrication | |
| EP1715080B1 (fr) | Procédé pour le revêtement de l'intérieur d'un tube d'arme | |
| EP2785491B1 (fr) | Procédé pour réparer une aube directrice variable | |
| DE102010041840A1 (de) | Verfahren zur Herstellung einer Ventilationsbohrung in einem Lagerstuhl eines Kurbelgehäuses einer Hubkolben-Brennkraftmaschine | |
| DE102008012761B4 (de) | Bauelement einer Wälzlagerung und Verfehren zum Herstellen des Bauelements | |
| DE102014220337A1 (de) | Verfahren zur Herstellung eines Verbindungselements sowie Verbindungselement und CFK-Bauteil mit einem derartigen Verbindungselement | |
| DE102019120812A1 (de) | Verfahren zum Herstellen einer Gewindemutter eines Gewindetriebes, insbesondere Kugelgewindemutter eines Kugelgewindetriebes | |
| DE102018103325A1 (de) | Gewindefurchende Schraube und Herstellung derselben | |
| DE102014216790A1 (de) | Verfahren zur Herstellung eines Verbindungselements sowie Verbindungselement und CFK-Bauteil mit einem derartigen Verbindungselement | |
| DE102020120861A1 (de) | Verfahren zur Erzeugung einer Schicht, Fertigungssystem und Bauteil | |
| DE10236929A1 (de) | Beschichtungsverfahren für eine Rolle oder einen Zylinder | |
| EP3933067A1 (fr) | Procédé de fabrication d'un revêtement, revêtement, composant doté d'un revêtement | |
| DE102005019500B4 (de) | Schraubendruckfeder für Ölabstreifkolbenringe |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20020115 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: 7F 02F 1/20 B Ipc: 7F 02F 1/00 A Ipc: 7C 23C 4/02 B Ipc: 7F 02B 77/02 B |
|
| AKX | Designation fees paid |
Designated state(s): DE ES FR GB IT |
|
| 17Q | First examination report despatched |
Effective date: 20050714 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: KS ALUMINIUM-TECHNOLOGIE GMBH |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 50213911 Country of ref document: DE Date of ref document: 20091126 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2334770 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20100715 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 50213911 Country of ref document: DE Representative=s name: PATENTANWAELTE TER SMITTEN EBERLEIN RUETTEN PA, DE Ref country code: DE Ref legal event code: R081 Ref document number: 50213911 Country of ref document: DE Owner name: KS HUAYU ALUTECH GMBH, DE Free format text: FORMER OWNER: KS ALUMINIUM-TECHNOLOGIE AG, 74172 NECKARSULM, DE Ref country code: DE Ref legal event code: R082 Ref document number: 50213911 Country of ref document: DE Representative=s name: PATENTANWAELTE TER SMITTEN EBERLEIN-VAN HOOF R, DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 50213911 Country of ref document: DE Representative=s name: TERPATENT PATENTANWAELTE TER SMITTEN EBERLEIN-, DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20210120 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20210217 Year of fee payment: 20 Ref country code: GB Payment date: 20210122 Year of fee payment: 20 Ref country code: DE Payment date: 20210120 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20210129 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 50213911 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20220114 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20220426 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20220114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20220116 |