EP1634817A2 - Article à surface étiquetée et dispositif pour étiqueter un article - Google Patents
Article à surface étiquetée et dispositif pour étiqueter un article Download PDFInfo
- Publication number
- EP1634817A2 EP1634817A2 EP05019595A EP05019595A EP1634817A2 EP 1634817 A2 EP1634817 A2 EP 1634817A2 EP 05019595 A EP05019595 A EP 05019595A EP 05019595 A EP05019595 A EP 05019595A EP 1634817 A2 EP1634817 A2 EP 1634817A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- label
- article
- edge
- article according
- radially inwardly
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D23/00—Details of bottles or jars not otherwise provided for
- B65D23/08—Coverings or external coatings
- B65D23/0842—Sheets or tubes applied around the bottle with or without subsequent folding operations
- B65D23/0878—Shrunk on the bottle
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C3/00—Labelling other than flat surfaces
- B65C3/06—Affixing labels to short rigid containers
- B65C3/08—Affixing labels to short rigid containers to container bodies
- B65C3/14—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical
- B65C3/16—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical by rolling the labels onto cylindrical containers, e.g. bottles
- B65C3/163—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical by rolling the labels onto cylindrical containers, e.g. bottles where the label is of the wrap-around type
- B65C3/166—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical by rolling the labels onto cylindrical containers, e.g. bottles where the label is of the wrap-around type the label being shrunken after application
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C9/00—Details of labelling machines or apparatus
- B65C9/0015—Preparing the labels or articles, e.g. smoothing, removing air bubbles
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/12—Surface bonding means and/or assembly means with cutting, punching, piercing, severing or tearing
Definitions
- the invention relates to an article with a labeled lateral surface according to the preamble of claim 1 or 9 and an apparatus for labeling such an article according to the preamble of claim 10 or 12.
- a generic article is known for example from WO 95/01912.
- the article disclosed therein is a container having upper and lower cylindrical surfaces and an intermediate concave peripheral groove. Adjoining the upper cylindrical region of the lateral surface is a conically tapered jacket section which, together with the cylindrical lateral surfaces and the groove, is covered by a heat-shrinkable wrap-around label with overlapping end sections.
- a rectangular label blank which is separated, for example, from a label roll, adhered in the region of its label leading edge to the cylindrical shell sections, completely wound around the vessel to form an overlap connection between the label edges and applied by means of a shrink treatment to the described vessel contour.
- the problem is in particular the shrinkage treatment, especially in the region of the concave radially inwardly shaped Nutzone.
- the invention has for its object to improve the labeling of articles with a radial indicate an inwardly formed region, in particular a region formed inside a lateral surface.
- the air outlet openings may be formed as a barely perceptible to the naked eye perforation in the label.
- z. B. concave groove is also an approximately over the entire circumference of the label extending perforation line particularly advantageous to ensure a uniform air discharge in the shrinkage treatment.
- the perforation line is preferably arranged centrally to the groove.
- the adhesive bond at the Etikettendraggings- or label leading edge can be temporary nature, only upright during the winding of the label on the article an adhesive bond obtained after the completion of the overlap connection between the beginning of the label and this overlapping label end edge is no longer needed. This optional measure also facilitates label removal in conjunction with a later recycling process.
- the overlap connection between the initial label and the overlapping label end edge must be of lasting quality in order to withstand the shrinkage treatment after winding, which is usually triggered by heating.
- a hot melt curable by ultraviolet irradiation is particularly advantageous. If necessary, this can also be used for attaching the initial label edge to the article, in particular if a permanent attachment of the label, even after the shrinking treatment, is desired.
- This type of attachment with UV-curable hot glue at the label start edge and / or label end edge is also in a Rundumetikettierung of articles without a radially inwardly formed, ie concave area of advantage, eg in bottles, cups or the like.
- cylindrical and / or convex shell sections see US 4,923,557 or EP 0 675 806 B1). These items may be rigid or compliant when labeling, depending on the material (glass, metal, plastic, cardboard).
- a second Leimwerk can be applied to produce adhesive zones in the region of the label edge lower cost adhesive, while the application of UV-curable adhesives near the label end edge can be done by a separate Glue.
- the article to be labeled is a bottle made of plastic, glass or metal, which is intended for example for filling with drinks, food or the like.
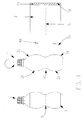
- FIG. 1 shows a bottle 1 labeled with a wrap-around label on the left hand, while the bottle 1 'shown in the center of the illustration shows the contour of the same bottle in the label-free state.
- Shown on the right hand side is a rectangular label blank 3, which is preferably provided by separating from a label tape.
- the lateral surface of the bottle 1 has an upper shell portion 2a, to which a tapered shoulder portion 2d in the direction of the bottle mouth followed. Further, the lateral surface has a lower shell portion 2b, followed by a in the direction of the bottle bottom tapered formed skirt portion 2e followed.
- the shell sections 2a and 2b may be cylindrical, ie have an extension along the axis of the bottle, or areas with a convex, convex surface with a maximum diameter.
- a radially inwardly formed portion 2c which extends in the illustrated embodiment over the entire circumference of the bottle 1 'and is concave.
- the bottle 1 'thus has a rotationally symmetrical outer contour to the bottle longitudinal axis.
- the wrap-around label 3 which consists of a shrinkable material, has a length extending from the label leading edge 3a to the label trailing edge 3b, which is greater than the maximum bottle circumference in the region of the upper and lower jacket sections 2a and 2b, so that the label trailing edge 3b after a complete Winding the label 3 on the bottle 1 'overlaps the label leading edge 3a in the circumferential direction.
- an adhesive zone 4b preferably extending over the entire label height, which may for example be in the form of a continuous hot glue strip.
- Hot glue for use, which is curable by UV irradiation.
- adhesive zones 4a which are preferably assigned to the upper and lower shell portion 2a, 2b of the bottle in terms of height on the label.
- a UV-curable hot glue can be used.
- a lower quality adhesive, in particular a conventional hot glue can be sufficient for this purpose.
- the shrinkable wrap-around label 3 has air outlet openings 5 which, in terms of height, are assigned approximately radially to the radially inward-shaped region 2c of the bottle 1 'and, for example, in the form of a perforation line running parallel to the label longitudinal edges.
- These air outlet openings may be formed as small holes or elongated slots in the label material, which are barely perceptible from the outside with the naked eye.
- the wrap-around label 3 is attached at least temporarily with the adhesive zones 4a and completely wound by subsequent rotation of the bottle 1 'about its vertical axis to overlap the front and rear edge of the label. After this winding process, the wrap-around label 3 not only covers the radially inward-shaped portion 2c but also portions of the skirt portions 2d and 2e.
- the permanent crosslinking of the adhesive takes place when using a curable hot glue, even before a shrink treatment of the label 3 for application to the bottle contour is started.
- the shrinking process is carried out by a heat treatment, for. B. by exposure to hot air, steam or infrared radiation.
- the label material contracts in the radial direction to the bottle casing surface, wherein the radially trapped region 2c between the lateral surface of the bottle and the back of the wrap-around label 3 trapped air can escape through the aforementioned air outlet openings 5 to the outside, so that a bubble-free application of the label material is ensured to the bottle contour.
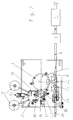
- FIG. 2 shows a schematic top view of a labeling machine which is suitable for the above-described labeling, which enables a continuously high-performance application of wrap-around labels 3 on bottles 1 'continuously fed in a single-lane series.
- the bottles have a feed conveyor 24, an inlet star wheel 25 with upstream Einteilschnecke 23, a guide arc 22, a carousel 6 with a plurality of uniformly spaced on a common pitch circle turntables 7, a discharge star wheel 8 and a discharge conveyor 9, which by a UV Tunnel 10 and a shrink tunnel 11 passes.
- the bottles are moving through the machine transport elements speed and position synchronous with each other continuously drivable.
- a labeling unit 12 for applying wrap-around labels 3 made of heat-shrinkable plastic film.
- the labeling unit 12 has two label roll receptacles 14 with an intermediate splicing station 15, a cutting unit 16, at least one gluing station 17, preferably a further gluing station 26, and a vacuum cylinder 18 for transferring a pre-cut label 3 glued to its leading and trailing edge a passing bottle 1 '.
- the labeling has a seen in the tape running direction between the splicing station 15 and the cutting unit 16 perforating 20, which consists for example of a equipped with needles perforating and a counter roll.
- the plastic film strip is fed to the cutting unit 16 by one of the two label tape rolls in a controlled strip take-off in cooperation with a print image or a marking-recognizing sensor so that a rectangular label blank having a length corresponding to the cylindrical shell circumference of the bottle 1 (with oversize) separated in the correct position to the printed image is passed to the vacuum cylinder 18, which then passes the wrap-around label 3 with the back facing outward on the glue roller of the gluing station 17 and possibly also on the glue roller of a further gluing station 26.
- the wrap-around label 3 receives in the region of its trailing edge 3b a glue application of UV-curable hot glue, which is preferably applied according to the form shown in Fig. 1, and possibly also in the leading edge 3a, but this one by the second Glue roller 26 can be applied conventional applicator glue.
- the label leading edge 3a is then brought to the lateral surfaces 2a and 2b of the bottle 1 ', adhered to the associated glue zones 4a and in the further course by a rotation of the bottle 1' caused by the turntable 7 fully wound around its vertical axis, the label trailing edge 3b after completion the rotation overlaps the label leading edge 3a and is adhered to the glue zone 4b on the outside thereof.
- the described process takes place during a continuous forward movement of the carousel 6.
- the labeled bottle 1 After passing through the labeling unit 12 and after completion of the winding process, the labeled bottle 1 reaches the outlet starwheel 8 in the further course and is transferred to the outlet conveyor 9.
- the outlet conveyor 9 transports the bottle 1 first through the UV tunnel 10, which brings about intense crosslinking and curing of the hot glue by UV irradiation, before the thermal loading of the shrinkable plastic label in the shrink tunnel 11 begins. Due to the UV treatment, the hot glue is temperature-resistant. A bursting of the fürlappungsverklebung during the shrinking treatment is reliably prevented in this way.
- the shrink treatment can be designed so that the upper and lower edge of the label before the middle label area is subjected to heat. It is possibly a local heat treatment for shrinking with appropriately positioned nozzles or heat radiators conceivable so that the voltage applied during winding of a label already on the lateral surface label areas need not be shrunk.
- the described innovation is also applicable to articles having a plurality of radially inwardly formed regions in the lateral surface.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Labeling Devices (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE202004013947U DE202004013947U1 (de) | 2004-09-08 | 2004-09-08 | Artikel mit einer etikettierten Mantelfläche und Vorrichtung zum Etikettieren eines Artikels |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1634817A2 true EP1634817A2 (fr) | 2006-03-15 |
| EP1634817A3 EP1634817A3 (fr) | 2006-09-13 |
| EP1634817B1 EP1634817B1 (fr) | 2008-10-29 |
Family
ID=34202625
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05019595A Expired - Lifetime EP1634817B1 (fr) | 2004-09-08 | 2005-09-08 | Article à surface étiquetée et dispositif pour étiqueter un article |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US20060048417A1 (fr) |
| EP (1) | EP1634817B1 (fr) |
| AT (1) | ATE412581T1 (fr) |
| DE (2) | DE202004013947U1 (fr) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102007014870A1 (de) * | 2007-03-26 | 2008-10-02 | Khs Ag | Verfahren zum Herstellen von Flaschen oder dergleichen Behälter aus Kunststoff |
| EP2186734A1 (fr) | 2008-11-14 | 2010-05-19 | Krones AG | Etiquette thermorétractable ainsi que procédé et appareil d'étiquetage de récipients |
| EP2287080A2 (fr) | 2009-08-21 | 2011-02-23 | Krones AG | Dispositif et procédé d'étiquetage de récipients dotés de types d'étiquettes différents |
| EP2394918A1 (fr) | 2010-06-08 | 2011-12-14 | Henkel AG & Co. KGaA | Procédé de collage de colles durcissables aux UV |
| DE102018209902A1 (de) | 2018-06-19 | 2019-12-19 | Krones Aktiengesellschaft | Verfahren zur Etikettierung von Leerflaschen aus Kunststoff und Etikettiermaschine |
Families Citing this family (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007015245A2 (fr) * | 2005-08-04 | 2007-02-08 | Polysack Plastic Industries Ltd | Film polymere retractable thermoplastique |
| EP1955952B1 (fr) | 2007-02-06 | 2016-05-04 | Krones Ag | Dispositif pour l'application d'étiquettes enveloppantes sur des objets |
| US8282754B2 (en) * | 2007-04-05 | 2012-10-09 | Avery Dennison Corporation | Pressure sensitive shrink label |
| DE102009031479A1 (de) * | 2009-07-01 | 2011-01-05 | Krones Ag | Vorrichtung zum Anbringen von Etikettenstreifen an Behältnissen |
| DE102009035269A1 (de) * | 2009-07-29 | 2011-02-03 | Krones Ag | Schneideinrichtung und Schneidverfahren zum Schneiden von Etiketten sowie Etikettiervorrichtung |
| BR122014017821A2 (pt) | 2010-01-28 | 2019-07-09 | Avery Dennison Corporation | Sistema para aplicação de rótulos em artigos |
| JP5672089B2 (ja) | 2011-03-15 | 2015-02-18 | オムロン株式会社 | 表示シートを備える機器の組立方法および表示シートを備える機器 |
| JP2014019492A (ja) * | 2012-07-23 | 2014-02-03 | Fuji Seal International Inc | ラベル付き容器 |
| JP5974287B2 (ja) * | 2012-08-22 | 2016-08-23 | 株式会社フジシール | シュリンクラベル付き容器及びシュリンクラベル |
| CA2911335C (fr) * | 2013-05-06 | 2022-03-15 | Compagnie Gervais Danone | Bouteille destinee a contenir une boisson, procede de fabrication d'une bouteille destinee a contenir une boisson et procede de conception d'une illustration |
| PL411535A1 (pl) * | 2015-03-10 | 2016-09-12 | Aleuro Converting Trade Spółka Z Ograniczoną Odpowiedzialnością | Sposób etykietowania rulonu folii spożywczej, urządzenie perforacyjne maszyny etykietującej oraz etykieta rulonu folii spożywczej |
| DE102015204821A1 (de) * | 2015-03-17 | 2016-09-22 | Krones Aktiengesellschaft | Vorrichtung und Verfahren zum Perforieren eines Folienschlauchs |
| JP2018120082A (ja) * | 2017-01-25 | 2018-08-02 | 株式会社トービ | シュリンクラベルおよびその製造方法 |
| CN109353628B (zh) * | 2018-12-11 | 2024-05-14 | 常熟利星光电科技有限公司 | 一种电源线双标签同步贴标装置 |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4923557A (en) | 1988-08-01 | 1990-05-08 | Trine Manufacturing Co., Inc. | Apparatus and method for applying a heat shrink film to a container |
| WO1995001912A1 (fr) | 1993-07-09 | 1995-01-19 | B & H Manufacturing Co., Inc. | Etiquetage de recipients presentant des rainures profondes |
| EP0675806B1 (fr) | 1992-12-18 | 2001-02-28 | B & H MANUFACTURING COMPANY, INC. | Procede d'etiquetage d'articles presentant des surfaces convexes |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4704173A (en) * | 1982-05-27 | 1987-11-03 | Wolfgang Hoffman | System for applying heat shrink film to containers and other articles and heat shrinking the same |
| US4574020A (en) * | 1983-11-28 | 1986-03-04 | Owens-Illinois, Inc. | Apparatus and method for wrapping a plastic label around a container |
| US4844760A (en) * | 1986-09-23 | 1989-07-04 | Trine Manufacturing Co., Inc. | Apparatus and method for applying |
| US4976798A (en) * | 1990-01-12 | 1990-12-11 | Shibuya America Corporation | Method of applying a plastic wrap to a contoured container |
| US5639529A (en) * | 1993-02-02 | 1997-06-17 | Moore Business Forms, Inc. | Permanent placed, easy removable label, for bottles and cans |
| JPH11507312A (ja) * | 1995-06-07 | 1999-06-29 | ビー アンド エイチ マニュファクチュアリング カンパニー インコーポレイテッド | 触知可能なしるしと伸びるラベルを含むラベルを物品に付けるためのコンピュータ制御式ラベリングマシン |
| WO1997001484A1 (fr) * | 1995-06-28 | 1997-01-16 | B & H Manufacturing Company, Inc. | Application d'etiquettes elastiques |
| US5897722A (en) * | 1996-07-12 | 1999-04-27 | B & H Manufacturing Company, Inc. | Process for applying labels with delayed adhesive activation |
| DE19750429A1 (de) * | 1997-11-14 | 1999-05-20 | Gerro Plast Gmbh | Verfahren zum Aufbringen einer schrumpfartigen Hülse aus folienartigem Schaumstoff auf eine Flasche oder dergleichen und Flasche oder dergleichen mit einer solchen Hülse |
| EP1116667B1 (fr) * | 1998-04-09 | 2005-11-16 | Asahi Breweries, Ltd. | Recipient a etiquette integrale retrecissable |
| DE19859063A1 (de) * | 1998-12-22 | 2000-06-29 | Frank Berrenbaum | Dekoratives Rundumetikett für Getränkeflaschen |
| US6649259B1 (en) * | 2000-02-29 | 2003-11-18 | National Starch And Chemical Investment Holding Corporation | Adhesives for thermally shrinkable films or labels |
| US6486229B1 (en) * | 2000-03-02 | 2002-11-26 | National Starch And Chemical Investment Holding Corporation | Radiation curable hot melt adhesive |
| JP4243085B2 (ja) * | 2002-10-07 | 2009-03-25 | 株式会社フジシールインターナショナル | 切取り線付き熱収縮性フィルム、その切取り線形成方法及び連続フィルム体 |
-
2004
- 2004-09-08 DE DE202004013947U patent/DE202004013947U1/de not_active Expired - Lifetime
-
2005
- 2005-08-18 US US11/207,397 patent/US20060048417A1/en not_active Abandoned
- 2005-09-08 DE DE502005005789T patent/DE502005005789D1/de not_active Expired - Lifetime
- 2005-09-08 AT AT05019595T patent/ATE412581T1/de not_active IP Right Cessation
- 2005-09-08 EP EP05019595A patent/EP1634817B1/fr not_active Expired - Lifetime
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4923557A (en) | 1988-08-01 | 1990-05-08 | Trine Manufacturing Co., Inc. | Apparatus and method for applying a heat shrink film to a container |
| EP0675806B1 (fr) | 1992-12-18 | 2001-02-28 | B & H MANUFACTURING COMPANY, INC. | Procede d'etiquetage d'articles presentant des surfaces convexes |
| WO1995001912A1 (fr) | 1993-07-09 | 1995-01-19 | B & H Manufacturing Co., Inc. | Etiquetage de recipients presentant des rainures profondes |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102007014870A1 (de) * | 2007-03-26 | 2008-10-02 | Khs Ag | Verfahren zum Herstellen von Flaschen oder dergleichen Behälter aus Kunststoff |
| EP2186734A1 (fr) | 2008-11-14 | 2010-05-19 | Krones AG | Etiquette thermorétractable ainsi que procédé et appareil d'étiquetage de récipients |
| EP2287080A2 (fr) | 2009-08-21 | 2011-02-23 | Krones AG | Dispositif et procédé d'étiquetage de récipients dotés de types d'étiquettes différents |
| DE102009043880A1 (de) | 2009-08-21 | 2011-02-24 | Krones Ag | Einrichtung und Verfahren zum Etikettieren von Behältern mit unterschiedlichen Etikettentypen |
| US8627870B2 (en) | 2009-08-21 | 2014-01-14 | Krones Ag | Apparatus and method for labeling containers with different types of labels |
| EP2394918A1 (fr) | 2010-06-08 | 2011-12-14 | Henkel AG & Co. KGaA | Procédé de collage de colles durcissables aux UV |
| DE102018209902A1 (de) | 2018-06-19 | 2019-12-19 | Krones Aktiengesellschaft | Verfahren zur Etikettierung von Leerflaschen aus Kunststoff und Etikettiermaschine |
| EP3584184A1 (fr) | 2018-06-19 | 2019-12-25 | Krones AG | Procédé d'étiquetage des bouteilles vides de matière plastique et étiqueteuse |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE412581T1 (de) | 2008-11-15 |
| EP1634817B1 (fr) | 2008-10-29 |
| US20060048417A1 (en) | 2006-03-09 |
| DE502005005789D1 (de) | 2008-12-11 |
| EP1634817A3 (fr) | 2006-09-13 |
| DE202004013947U1 (de) | 2005-02-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1634817B1 (fr) | Article à surface étiquetée et dispositif pour étiqueter un article | |
| EP2287080B1 (fr) | Dispositif et procédé d'étiquetage de récipients dotés de types d'étiquettes différents | |
| EP2785596B1 (fr) | Dispositif de formation d'unités de conditionnement | |
| EP0525729B1 (fr) | Procédé et appareil pour l'application sur des récipients, d'étiquettes en matière scellable, et récipients étiquettés ainsi obtenus | |
| DE69329976T3 (de) | Verfahren zum etikettieren von gegenständen mit konvexen oberflächen | |
| DE3442995C2 (fr) | ||
| DE102011106759B3 (de) | Verfahren zur Herstellung von Gebinden | |
| EP0559005B1 (fr) | Méthode et appareil pour l'application d'une étiquette circulaire sur un récipient | |
| DE3123637C2 (de) | Vorrichtung zur Aufbringung von Kunststoffhüllen auf Behälter | |
| DE19630690A1 (de) | Flasche o. dgl. mit einem den Umfang umschließenden Etikett, Verfahren und Vorrichtung zur Erzeugung dieser Flasche | |
| DE69100355T2 (de) | Verfahren und Vorrichtung zur Heisssiegelung von Etiketten auf Behältern. | |
| EP2801535B1 (fr) | Dispositif d'étiquetage de récipient et de mise en place de gaines thermorétractables sur des récipients et procédé correspondant | |
| DE68905233T2 (de) | Maschine mit verlängerten Spannfuttern zum Anbringen von Schrumpfetiketten. | |
| WO2013004340A1 (fr) | Procédé de réalisation d'emballages multiples à partir de récipients | |
| DE3637465A1 (de) | Verfahren und vorrichtung zur aufbringung eines kunststoffetikettes auf einen behaelter | |
| WO2013113464A1 (fr) | Dispositif ovale de traitement de récipients | |
| DE3637466A1 (de) | Verfahren und vorrichtung zur aufbringung eines loesungsmittels auf kunststoffetiketten | |
| DE69712040T2 (de) | Verfahren und vorrichtung zum etikettieren von behältern | |
| EP3099580B1 (fr) | Procédé et dispositif pour former des unités d'emballage | |
| DE69808319T2 (de) | Verfahren und vorrichtung zur etikettierung von behältern mit durch pressluft unterstütztem transfer der etiketten | |
| DE69623624T2 (de) | Verfahren zum aufbringen von dehnbaren etiketten | |
| DE102004047595A1 (de) | Verfahren und Vorrichtung zum Ausstatten von Gefäßen | |
| EP2186734B1 (fr) | Etiquette thermorétractable ainsi que procédé et appareil d'étiquetage de récipients | |
| DE19531839A1 (de) | Verfahren und Vorrichtung zum Ausstatten von Gegenständen | |
| EP3129297B1 (fr) | Procédé et dispositif pour attacher des etiquettes aux emballages |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| 17P | Request for examination filed |
Effective date: 20060315 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| 17Q | First examination report despatched |
Effective date: 20061108 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502005005789 Country of ref document: DE Date of ref document: 20081211 Kind code of ref document: P |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20081029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090209 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090129 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090228 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090330 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090129 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| 26 | Opposition filed |
Opponent name: KHS AG Effective date: 20090729 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| R26 | Opposition filed (corrected) |
Opponent name: KHS AG Effective date: 20090729 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| BERE | Be: lapsed |
Owner name: KRONES A.G. Effective date: 20090930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090930 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20090908 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090930 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090130 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090908 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| APBM | Appeal reference recorded |
Free format text: ORIGINAL CODE: EPIDOSNREFNO |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20081029 |
|
| APBQ | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3O |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: KHS GMBH Effective date: 20090729 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R100 Ref document number: 502005005789 Country of ref document: DE |
|
| APBU | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9O |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20150212 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20240730 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20240812 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 502005005789 Country of ref document: DE |