EP1880948B1 - Caisse de transport et dispositif de moulage par injection pour la fabrication d'une telle caisse de transport - Google Patents
Caisse de transport et dispositif de moulage par injection pour la fabrication d'une telle caisse de transport Download PDFInfo
- Publication number
- EP1880948B1 EP1880948B1 EP07011940A EP07011940A EP1880948B1 EP 1880948 B1 EP1880948 B1 EP 1880948B1 EP 07011940 A EP07011940 A EP 07011940A EP 07011940 A EP07011940 A EP 07011940A EP 1880948 B1 EP1880948 B1 EP 1880948B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- transport case
- shell
- main shell
- cover shell
- height
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000001746 injection moulding Methods 0.000 title description 4
- 238000004519 manufacturing process Methods 0.000 title description 3
- 239000004033 plastic Substances 0.000 claims description 35
- 229920003023 plastic Polymers 0.000 claims description 35
- 238000005192 partition Methods 0.000 claims description 4
- 230000000295 complement effect Effects 0.000 claims 3
- 239000002991 molded plastic Substances 0.000 claims 1
- 230000002093 peripheral effect Effects 0.000 claims 1
- 239000000463 material Substances 0.000 description 23
- 238000002347 injection Methods 0.000 description 14
- 239000007924 injection Substances 0.000 description 14
- 238000000034 method Methods 0.000 description 10
- 238000000465 moulding Methods 0.000 description 9
- 238000005507 spraying Methods 0.000 description 5
- 230000015572 biosynthetic process Effects 0.000 description 3
- 238000011161 development Methods 0.000 description 3
- 230000018109 developmental process Effects 0.000 description 3
- 238000009825 accumulation Methods 0.000 description 2
- 230000002787 reinforcement Effects 0.000 description 2
- 101100441413 Caenorhabditis elegans cup-15 gene Proteins 0.000 description 1
- 238000010521 absorption reaction Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 230000003287 optical effect Effects 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 230000001105 regulatory effect Effects 0.000 description 1
- 238000007711 solidification Methods 0.000 description 1
- 230000008023 solidification Effects 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000000007 visual effect Effects 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D1/00—Rigid or semi-rigid containers having bodies formed in one piece, e.g. by casting metallic material, by moulding plastics, by blowing vitreous material, by throwing ceramic material, by moulding pulped fibrous material or by deep-drawing operations performed on sheet material
- B65D1/22—Boxes or like containers with side walls of substantial depth for enclosing contents
- B65D1/24—Boxes or like containers with side walls of substantial depth for enclosing contents with moulded compartments or partitions
- B65D1/243—Crates for bottles or like containers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/03—Injection moulding apparatus
- B29C45/04—Injection moulding apparatus using movable moulds or mould halves
- B29C45/0441—Injection moulding apparatus using movable moulds or mould halves involving a rotational movement
- B29C45/045—Injection moulding apparatus using movable moulds or mould halves involving a rotational movement mounted on the circumference of a rotating support having a rotating axis perpendicular to the mould opening, closing or clamping direction
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/03—Injection moulding apparatus
- B29C45/04—Injection moulding apparatus using movable moulds or mould halves
- B29C45/06—Injection moulding apparatus using movable moulds or mould halves mounted on a turntable, i.e. on a rotating support having a rotating axis parallel to the mould opening, closing or clamping direction
- B29C45/062—Injection moulding apparatus using movable moulds or mould halves mounted on a turntable, i.e. on a rotating support having a rotating axis parallel to the mould opening, closing or clamping direction carrying mould halves co-operating with fixed mould halves
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/16—Making multilayered or multicoloured articles
- B29C45/1615—The materials being injected at different moulding stations
- B29C45/162—The materials being injected at different moulding stations using means, e.g. mould parts, for transferring an injected part between moulding stations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/16—Making multilayered or multicoloured articles
- B29C45/1615—The materials being injected at different moulding stations
- B29C45/1628—The materials being injected at different moulding stations using a mould carrier rotatable about an axis perpendicular to the opening and closing axis of the moulding stations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/16—Making multilayered or multicoloured articles
- B29C45/1657—Making multilayered or multicoloured articles using means for adhering or bonding the layers or parts to each other
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/17—Component parts, details or accessories; Auxiliary operations
- B29C45/76—Measuring, controlling or regulating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D1/00—Rigid or semi-rigid containers having bodies formed in one piece, e.g. by casting metallic material, by moulding plastics, by blowing vitreous material, by throwing ceramic material, by moulding pulped fibrous material or by deep-drawing operations performed on sheet material
- B65D1/40—Details of walls
- B65D1/42—Reinforcing or strengthening parts or members
- B65D1/48—Reinforcements of dissimilar materials, e.g. metal frames in plastic walls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2945/00—Indexing scheme relating to injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould
- B29C2945/76—Measuring, controlling or regulating
- B29C2945/76003—Measured parameter
- B29C2945/7604—Temperature
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2945/00—Indexing scheme relating to injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould
- B29C2945/76—Measuring, controlling or regulating
- B29C2945/76177—Location of measurement
- B29C2945/76254—Mould
- B29C2945/76257—Mould cavity
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2945/00—Indexing scheme relating to injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould
- B29C2945/76—Measuring, controlling or regulating
- B29C2945/76494—Controlled parameter
- B29C2945/76551—Time
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2945/00—Indexing scheme relating to injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould
- B29C2945/76—Measuring, controlling or regulating
- B29C2945/76655—Location of control
- B29C2945/76702—Closure or clamping device
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29L—INDEXING SCHEME ASSOCIATED WITH SUBCLASS B29C, RELATING TO PARTICULAR ARTICLES
- B29L2031/00—Other particular articles
- B29L2031/712—Containers; Packaging elements or accessories, Packages
- B29L2031/7134—Crates, e.g. for bottles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24012—Materials
- B65D2501/24019—Mainly plastics
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/2405—Construction
- B65D2501/24063—Construction of the walls
- B65D2501/24082—Plain
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/2405—Construction
- B65D2501/24146—Connection between walls or of walls with bottom
- B65D2501/24152—Integral
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24197—Arrangements for locating the bottles
- B65D2501/24203—Construction of locating arrangements
- B65D2501/2421—Partitions
- B65D2501/24216—Partitions forming square or rectangular cells
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24197—Arrangements for locating the bottles
- B65D2501/24343—Position pattern
- B65D2501/2435—Columns and rows
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24363—Handles
- B65D2501/24541—Hand holes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/2477—Parts reinforced
- B65D2501/24777—Side walls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24789—Means used for reinforcing
- B65D2501/24821—Reinforcing elements made from a material different to the one of the part being reinforced
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24828—Location of the reinforcing means
- B65D2501/2484—Outside the crate
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24828—Location of the reinforcing means
- B65D2501/24847—Oriented mainly vertically
Definitions
- the invention relates to a transport box made of plastic injection molding, in particular bottle crate, according to the preamble of claim 1.
- Transport containers especially crates
- Transport containers have been further developed in recent years due to market requirements, particularly in the field of handling and visual appearance.
- the originally relatively sharp-edged handles have been further developed to ergonomically favorable and comfortable for the customer, rounded handles
- the handles are further improved in recent times by molded enclosures with grip friendly material, which has been significantly improved in particular the comfort.
- the originally single-colored and simply printed transport boxes for example, by creating largely smooth side walls and use of high-quality printed, intimately associated with the container body film elements, so-called insert labels or labels attractive sales packaging has been further developed.
- US 2003/0014912 A1 is a rotationally symmetrical plastic container with a bottom and with a frusto-conical lateral surface forming side wall known.
- the bottom and the side wall are Moschalig formed by a base shell and applied to this and thermally connected to this cover shell.
- the plastic container has on a bottom opposite to the bottom, a filler opening comprehensive edge area, a bead-shaped reinforcement, which is formed by a formation of interlocking interlocking, radially encircling, spaced at a pitch distance staggered ribs of the base and the cover shell.
- the box-shaped container consists of a bottom and four vertically aligned side walls of a plastic injection molded part. Outstanding from the bottom is centrally arranged in the container a molded on the ground carrying handle and have the side walls approximately rectangular handle openings. Especially in the area of the handle openings is a bivalve Provision is made, according to which a preferably different to the first plastic material different plastic material is sprayed on the sprayed in a first injection process container from the plastic in a subsequent second injection process in areas. In the bivalve region ribs or webs are provided on the first spray shell, whereby a tooth-like engagement of the two plastic materials and thus an intimate connection is achieved.
- Out DE 102 39 319 A1 is a two-component plastic container, in particular bottle crate, with a bottom and / or container walls, which are formed at least from a first plastic, known, wherein at the bottom and / or the container walls, at least one area bivalves of different plastics is formed with each other are connected cohesively and / or positively.
- the second plastic is provided in the region of handle parts of the container in order to achieve a pleasant gripping behavior.
- Out DE 102 39 319 A1 is a two-component plastic container, in particular bottle crate known, with a bottom and container walls made of a first plastic, in which at the bottom or the container walls, an area is formed from a second plastic, wherein the first and second plastic material-locking and / or positively connected rigidly, Furthermore, the second plastic on the first plastic is molded or injected.
- the advantageous properties of two different plastics in a transport box can be combined, for example, handle parts with rubber-like surface for easier handling or color design options by using two differently colored plastics.
- the object of the invention is to provide a transport box, consisting of a base shell and an at least partially applied to the base shell cover shell, which is designed for deformation-free removal of a high stacking load.
- Possibilities are advantageous developments, as described in claims 2 and 3, whereby a high load capacity is achieved by stacking forces without changing the size, since the reinforcement zones in the rounded corner, without the general dimensions for width and length of the transport box are changed.
- a wandaussteifung is achieved to prevent buckling under pressure load.
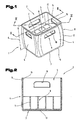
- a transport box 1 in particular bottle crate 2, preferably made of plastic injection, with by a bottom 3 and substantially planar in each case at a right angle arranged side walls 4 bounded interior 5 shown.
- the interior 5 is subdivided in a subregion of a height 6 by partitions 7 in receiving compartments 8.
- partitions 7 In the side walls 4 handle openings 8 forming breakthroughs 10 are arranged.
- a connection region 12 of adjacent side walls 4 forming a corner region 11 is, viewed in a plane parallel to a contact surface 13, rounded.
- the bottom 3 and the side walls 4 and preferably the partitions 7 form a one-piece injection molding a base shell 4 on at least partially on a surface facing away from the interior 5 surface 15, for example in the corner region 11 forming connecting portion 12 a cover shell 16 from a to a first Plastic material of the base shell 14 second plastic material with the same or the first plastic material different properties, eg in a different color, with different hardness or strength, etc., applied, which is thermally connected to the base shell 14 in particular by a spray-on, by process measures as described in detail later.
- cover 16 can also be used in essential areas of the transport box 1, e.g. the entire outer surfaces of the side walls 4 and the corner portions 11 may be provided on the base shell 14.
- corner region 11 forming connecting portion 12 between the adjacent, arranged in rectangular planes to each other side walls 4 is shown, which is rounded and a consideration in the bottom 3 parallel cross-sectional planes rounding radius 17 of an outline contour 18 on the height 6 of the transport box 1 different values having.
- the Rundüngsradius 17 in the region of the bottom 3 and an upper edge 19 of the transport box 1 is greater than in an area therebetween, in particular in the half of the height 6.
- a ratio between the maximum radius of curvature 17 in the area the bottom 3 and the top edge 19 of the transport box 1 to a minimum radius of curvature 20 in the half of the height 6 has a value at least greater than 1.5, preferably 2.5.
- an inner contour 21 of the base shell 14 delimiting the inner space 5 has a radius of curvature 22 which is unchanged over the entire height 6.
- This design with the different rounding radii 17, 20 for the outer contour contour 18 of the cover shell 16 allows bulging of the corner region 11 and give the transport box 1 a barrel-shaped appearance, without exceeding the bottom 3 by a length 26 and a width 27 footprint 13 exceeded becomes.
- the injection processes, as described later, are regulated in time so that there is a thermal connection between the base shell 14 and the cover shell 16.
- the Figure 5 is the formation of the corner region 11 with the rib-shaped elevations 30, which are mitgeformt in a first injection process on the base shell 14 in a first cavity between a core tool 31 and mold parts 32 of an injection mold 34, shown.
- the elevation 30 aligned on both sides of an approximately diagonal leading division plane 35 perpendicular to inner surfaces 36 of the mold parts 32 and extend, as already described above, at least over a portion of the height of the transport box.
- the core tool 31 is surrounded with the molded thereon base shell 14, preferably in a second injection station, with a second cavity forming mold parts 37, 38 and the cover shell 16 is sprayed onto the base shell 14, wherein the same and with the elevations 30 of Basic shell 14 form interlocking interlocking 30 elevations.
- each of the mold parts 32, 33, 37, 38 in the direction perpendicular to the outer surface 29 direction - according to arrow 39 - adjustable.
- a cross-section approximately crescent-shaped and over the height of the transport box 1 and the side walls 4 extending predominantly hollow chamber 40 is provided which reaches through the arrangement of a core tool 31 becomes.
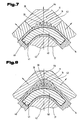
- FIGS. 7 and 8 another embodiment of the corner portion 11 is shown with the formed on the base shell 14 and the cover shell 16, rib-shaped elevations 30 which are aligned with respect to a diagonal plane 42 parallel thereto.
- a first injection molding tool is required with the core tool 31, as previously described, which also has the mandrel 41 for the hollow chamber 40, wherein at least for the injection process of the base shell 14 in the corner region another molding 43 is required for the Entformvorgang in the direction of the diagonal plane 42 - according to arrow 44 - is adjustable.
- corner region 11 or the connection region 12 between the adjacent side walls 4 instead of, as previously shown rounded and described, may also be designed for example in a 45 ° bevel.
- a connecting surface resulting from this beveling can, for example, be roof-surface-shaped over the height of the transport box in order, for example, to achieve a greater diagonal width than in the floor area and in the edge area of the transport box.
- this outer surface may extend over the height, e.g. wavy, jagged, or be formed with respect to the inner contour line 21 convex or concave.
- FIGS. 9 and 10 is another embodiment of the transport box 1, consisting of the base shell 14 and the at least on this partially, for example in the region of a side wall 4, applied cover shell 16 shown.
- a bulge over at least a portion of the height 6 of the transport box 1 is provided for example in the region of the side wall 4 by the formation of the elevations 30 on the base shell 14 and the cover shell 16.
- Such a design is indeed in terms of the associated loss of space when juxtaposing such transport boxes 1, eg on a transport pallet, only for special operations of the transport box 1 is used.
- elevations 30 may be formed by different shapes instead of the rib shape shown, for example, in cross and transverse webs on the base shell 14 or cover shell 16 and wherein counter-formed in remaining spaces of the elevations 30 and forming a positive connection Elevations 30 are formed or injected.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Ceramic Engineering (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
- Containers Having Bodies Formed In One Piece (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Stackable Containers (AREA)
- Rigid Containers With Two Or More Constituent Elements (AREA)
- Details Of Rigid Or Semi-Rigid Containers (AREA)
- Vending Machines For Individual Products (AREA)
Claims (21)
- Caisse de transport (1) en moulage par injection de matériau synthétique, en particulier caisse pour bouteilles, avec un espace intérieur (5) divisé par des parois de séparation (7) en cases de réception (8), avec une coque de base (14) réalisant un fond (3) et des parois latérales (4) en un premier matériau synthétique et avec une coque de recouvrement (16) disposée au moins par zones sur une surface extérieure de la coque de base (14), en particulier reliée thermiquement à celle-ci par projection en un deuxième matériau synthétique, caractérisée en ce qu'au moins des parois latérales avoisinantes dans une zone de liaison (12), orientées perpendiculairement les unes aux autres, la coque de base (14) et la coque de recouvrement (16) présentent des surélévations (30) venant en prise de denture, reliées en une pièce avec la coque de base (14) et la coque de recouvrement (16), en ce que la zone de liaison (12) formant la zone de coin (11) est arrondie, où un rayon de courbure (17) de la zone de liaison (12), vu dans des plans en section transversale parallèles au fond présente sur la hauteur (6) de la caisse de transport (1) des valeurs différentes, et le rayon de courbure (20) à peu près à mi-hauteur (6) est plus petit que dans la zone du fond (3) et/ou une arête supérieure (19) de la caisse de transport (1).
- Caisse de transport (1) selon la revendication 1, caractérisée en ce que le rapport entre le rayon de courbure maximal (17) dans la zone du fond (3) et/ou l'arête supérieure (19) de la caisse de transport (1) au rayon de courbure minimal (20) à peu près à mi-hauteur (6) présente une valeur supérieure à 1, en particulier supérieure à 2,5.
- Caisse de transport (1) selon la revendication 1 ou 2, caractérisée en ce qu'une dimension diagonale extérieure (22) des contours extérieurs opposés est plus grande au milieu de la hauteur (6) que dans la zone du fond (3) et/ou de l'arête supérieure (19).
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la zone de liaison (12) est formée par une partie de paroi de la coque de base (14) et/ou de la couche de recouvrement (16) qui s'étend à des plans formés sur des surfaces (28, 29) de parois latérales (4) avoisinantes, orientées perpendiculairement les unes aux autres, selon un angle de 45°C.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que des lignes de contour extérieures de la coque de recouvrement (16) s'opposant diagonalement, s'étendant sur la hauteur (6), sont courbées d'une manière concave diamétralement opposée.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que les lignes de contour extérieures sont courbées d'une manière convexe diamétralement opposée.
- Caisse de transport selon l'une des revendications précédentes, caractérisée en ce que les lignes de contour extérieures sont ondulées d'une manière diamétralement opposée.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que des lignes de contour intérieures diagonalement opposées de la coque de base sont à peu près parallèles les unes aux autres et sont disposées perpendiculairement à un plan formé par la face d'appui (13).
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce qu'il est réalisé dans la zone de coin (11) dans la coque de base (14) une chambre creuse (40) s'étendant en direction de la hauteur (6).
- Caisse de transport (1) selon la revendication 16, caractérisée en ce que la chambre creuse (40) est délimitée par une partie de paroi intérieure et une partie de paroi extérieure espacée de celle-ci de la coque de base (14).
- Caisse de transport (1) selon la revendication 16 ou 17, caractérisée en ce qu'une forme en section transversale de la chambre creuse (40) est courbée en forme de croissant.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que les élévations (30) de la coque de base (14) ou de la coque de recouvrement (16) sont formées par une grille à barrettes.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que les élévations (30) de la coque de base (14) ou de la coque de recouvrement (16) sont formées par des prolongements s'engageant dans des creux de la grille à barrettes.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce qu'une hauteur de barrette est égale sur une longueur de barrette.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce qu'une hauteur de barrette est différente sur une longueur de barrette.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de recouvrement (16) recouvre la coque de base (14) au moins par zones à des zones de bord, par exemple, dans la zone d'une arête supérieure (19) et/ou d'un bord d'ouverture de prise.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de recouvrement (16) est disposée au moins à une section de paroi de la coque de base (14).
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de recouvrement (16) forme une enveloppe extérieure de la coque de base (14).
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de recouvrement (16) est disposée sur la coque de base (14) en entourant au moins une zone de coin (12).
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de base (14) est de préférence en PE.
- Caisse de transport (1) selon l'une des revendications précédentes, caractérisée en ce que la coque de recouvrement (16) est réalisée de préférence en PE.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT0104506A AT503830B1 (de) | 2006-06-21 | 2006-06-21 | Transportkasten und spritzvorrichtung für einen transportkasten |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1880948A2 EP1880948A2 (fr) | 2008-01-23 |
| EP1880948A3 EP1880948A3 (fr) | 2008-07-30 |
| EP1880948B1 true EP1880948B1 (fr) | 2010-05-26 |
Family
ID=38440170
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP07011940A Active EP1880948B1 (fr) | 2006-06-21 | 2007-06-19 | Caisse de transport et dispositif de moulage par injection pour la fabrication d'une telle caisse de transport |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1880948B1 (fr) |
| AT (2) | AT503830B1 (fr) |
| DE (1) | DE502007003905D1 (fr) |
Families Citing this family (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL2007073C2 (en) * | 2011-07-08 | 2013-01-09 | Soederhuizen Stenen B V | Crate comprising a rib structure with c-shaped corner ribs. |
| DE102014104294A1 (de) * | 2014-03-27 | 2015-10-01 | Dr. Ing. H.C. F. Porsche Aktiengesellschaft | Verfahren zur Herstellung eines Strukturbauteils eines Kraftfahrzeugs |
| US12108853B2 (en) | 2019-01-06 | 2024-10-08 | Yeti Coolers, Llc | Luggage system |
| AU201717615S (en) | 2017-06-12 | 2018-01-15 | Yeti Coolers | Container |
| CN116729803B (zh) | 2017-06-12 | 2026-06-09 | 野醍冷却器有限责任公司 | 容器和闩锁组件 |
| US11976498B2 (en) | 2017-06-12 | 2024-05-07 | Yeti Coolers, Llc | Container and latching system |
| US11685573B2 (en) | 2017-06-12 | 2023-06-27 | Yeti Coolers, Llc | Carry strap for container |
| USD904829S1 (en) | 2018-12-11 | 2020-12-15 | Yeti Coolers, Llc | Container accessories |
| USD907445S1 (en) | 2018-12-11 | 2021-01-12 | Yeti Coolers, Llc | Container accessories |
| JP7303313B2 (ja) | 2019-01-06 | 2023-07-04 | イエティ クーラーズ エルエルシー | 荷物システム |
| US12225993B2 (en) | 2019-01-06 | 2025-02-18 | Yeti Coolers, Llc | Luggage system |
| USD963344S1 (en) | 2020-06-30 | 2022-09-13 | Yeti Coolers, Llc | Luggage |
| USD954436S1 (en) | 2020-06-30 | 2022-06-14 | Yeti Coolers, Llc | Luggage |
| USD961926S1 (en) | 2020-06-30 | 2022-08-30 | Yeti Coolers, Llc | Luggage |
| USD951643S1 (en) | 2020-06-30 | 2022-05-17 | Yeti Coolers, Llc | Luggage |
| USD985937S1 (en) | 2020-12-16 | 2023-05-16 | Yeti Coolers, Llc | Container |
| USD960648S1 (en) | 2020-12-16 | 2022-08-16 | Yeti Coolers, Llc | Container accessory |
| USD994438S1 (en) | 2020-12-16 | 2023-08-08 | Yeti Coolers, Llc | Container |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0260698B2 (fr) * | 1986-09-18 | 1996-10-30 | Schoeller-Plast AG | Poignée d'un réceptacle, en particulier pour casier à bouteilles |
| US4935184A (en) | 1988-02-05 | 1990-06-19 | Primtec | Stabilized injection molding when using a common mold part with separate complimentary mold parts |
| DE4480340C2 (de) * | 1993-12-29 | 1997-10-23 | Kobe Steel Ltd | Zwei-Lagen-Schaum-Spritzgießmaschine |
| DE19639486B4 (de) * | 1996-09-26 | 2005-10-20 | Schaefer Gmbh Fritz | Behälter aus Kunststoff |
| US6823624B2 (en) * | 2001-07-17 | 2004-11-30 | S.I.T., Inc. | Plastic article with protuberance |
| DE10208845A1 (de) * | 2002-03-03 | 2003-09-11 | Oberland Engineering Gmbh | Verfahren zum Herstellen eines Kastens und danach hergestellter Kasten |
| DE10239319B4 (de) | 2002-08-27 | 2007-04-19 | Schoeller Wavin Systems Services Gmbh | Zweikomponenten Kunstoffbehälter |
| DE10252648A1 (de) | 2002-09-09 | 2004-05-27 | Theysohn Formenbau Gmbh | Behältnis sowie Anlage und Verfahren zum Ausbilden dieses |
| GB2394218A (en) * | 2002-10-17 | 2004-04-21 | D W Plastics Nv | Container having a handle |
| WO2004039557A1 (fr) * | 2002-10-31 | 2004-05-13 | Sumitomo Heavy Industries, Ltd. | Machine a former et son procede de commande |
| US7156652B2 (en) * | 2003-10-03 | 2007-01-02 | Daiwa Kasei Industry Co., Ltd. | Motor-driven injection molding apparatus |
-
2006
- 2006-06-21 AT AT0104506A patent/AT503830B1/de not_active IP Right Cessation
-
2007
- 2007-06-19 DE DE502007003905T patent/DE502007003905D1/de active Active
- 2007-06-19 AT AT07011940T patent/ATE469039T1/de active
- 2007-06-19 EP EP07011940A patent/EP1880948B1/fr active Active
Also Published As
| Publication number | Publication date |
|---|---|
| EP1880948A3 (fr) | 2008-07-30 |
| EP1880948A2 (fr) | 2008-01-23 |
| ATE469039T1 (de) | 2010-06-15 |
| AT503830B1 (de) | 2008-09-15 |
| AT503830A1 (de) | 2008-01-15 |
| DE502007003905D1 (de) | 2010-07-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1880948A2 (fr) | Caisse de transport et dispositif de moulage par injection pour la fabrication d'une telle caisse de transport | |
| DE60114202T2 (de) | Kunststoffbehälter mit runden schultern | |
| EP1882636B1 (fr) | Récipient en plastique et procédé de fabrication | |
| DE69419392T2 (de) | Zusammenlegbarer Behälter | |
| DE69321363T2 (de) | Flaschenkastenanordnung | |
| DE2123472C3 (de) | Durch Anspritzen eines flexiblen Flachmaterials in einer Spritzgießform hergestellter Behalter | |
| EP0673334A1 (fr) | Unite empilable d'emballage. | |
| DE3872256T2 (de) | Behaelteradapter. | |
| DE102007018358B4 (de) | Relief-Overmolding | |
| EP0575394B1 (fr) | Disposition de bacs | |
| DE102006005873B4 (de) | Wandflächenteil und Transportbehälter | |
| EP2322441B1 (fr) | Récipient de transport et de stockage empilable en plastique | |
| EP0374774B1 (fr) | Casiers à bouteilles avec des éléments horizontaux servant de poignées | |
| DE102007020277A1 (de) | Mehrteilige Palette | |
| DE3444477A1 (de) | Kastenfoermiger behaelter | |
| EP3024051B1 (fr) | Boîtier d'élément d'accumulateur | |
| DE4429945A1 (de) | Stapelbarer Transportbehälter | |
| WO2002004301A1 (fr) | Recipient d'emballage | |
| EP2987742B1 (fr) | Recipient empilable ayant une structure de transfert de charge | |
| CH683087A5 (de) | Lager- und Transportbehälter aus Kunststoff. | |
| EP1149023B1 (fr) | Fut a bondes | |
| EP3543158A1 (fr) | Conteneur de transport | |
| DE29613553U1 (de) | Flexibler Behälter aus thermoplastischem Kunststoff | |
| DE102019113936A1 (de) | Getränkekasten für das Einstellen von Flaschen | |
| DE2717298C3 (de) | Verfahren zum Herstellen eines Verbunddeckels |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| 17P | Request for examination filed |
Effective date: 20090124 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AXX | Extension fees paid |
Extension state: MK Payment date: 20090124 Extension state: BA Payment date: 20090124 Extension state: AL Payment date: 20090124 Extension state: RS Payment date: 20090124 Extension state: HR Payment date: 20090124 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502007003905 Country of ref document: DE Date of ref document: 20100708 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20100526 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20100526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100926 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100630 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100927 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100827 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| 26N | No opposition filed |
Effective date: 20110301 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502007003905 Country of ref document: DE Effective date: 20110228 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100726 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20110619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100619 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20101127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100526 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20130628 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 469039 Country of ref document: AT Kind code of ref document: T Effective date: 20120619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100826 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20130628 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20100906 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120619 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502007003905 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502007003905 Country of ref document: DE Effective date: 20150101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140630 |