EP2185424B1 - Verfahren und maschine zum schneiden und verschliessen von schachteln und zum einsatz von polsterbeuteln - Google Patents
Verfahren und maschine zum schneiden und verschliessen von schachteln und zum einsatz von polsterbeuteln Download PDFInfo
- Publication number
- EP2185424B1 EP2185424B1 EP08839140A EP08839140A EP2185424B1 EP 2185424 B1 EP2185424 B1 EP 2185424B1 EP 08839140 A EP08839140 A EP 08839140A EP 08839140 A EP08839140 A EP 08839140A EP 2185424 B1 EP2185424 B1 EP 2185424B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- box
- bag
- height
- void
- bags
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000005520 cutting process Methods 0.000 title claims abstract description 21
- 238000000034 method Methods 0.000 title claims description 21
- 239000000463 material Substances 0.000 claims description 6
- 238000007789 sealing Methods 0.000 claims 2
- 238000003780 insertion Methods 0.000 claims 1
- 230000037431 insertion Effects 0.000 claims 1
- 238000003466 welding Methods 0.000 description 14
- 238000005259 measurement Methods 0.000 description 6
- 238000002360 preparation method Methods 0.000 description 6
- 230000015572 biosynthetic process Effects 0.000 description 5
- 230000006978 adaptation Effects 0.000 description 4
- 238000004806 packaging method and process Methods 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 3
- 239000000109 continuous material Substances 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000009826 distribution Methods 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 238000012423 maintenance Methods 0.000 description 2
- 239000002699 waste material Substances 0.000 description 2
- 208000031872 Body Remains Diseases 0.000 description 1
- 241001415961 Gaviidae Species 0.000 description 1
- 240000008042 Zea mays Species 0.000 description 1
- 230000002411 adverse Effects 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000003287 optical effect Effects 0.000 description 1
- 210000000056 organ Anatomy 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 239000000523 sample Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 210000003462 vein Anatomy 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D81/00—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents
- B65D81/02—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents specially adapted to protect contents from mechanical damage
- B65D81/05—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents specially adapted to protect contents from mechanical damage maintaining contents at spaced relation from package walls, or from other contents
- B65D81/051—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents specially adapted to protect contents from mechanical damage maintaining contents at spaced relation from package walls, or from other contents using pillow-like elements filled with cushioning material, e.g. elastic foam, fabric
- B65D81/052—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents specially adapted to protect contents from mechanical damage maintaining contents at spaced relation from package walls, or from other contents using pillow-like elements filled with cushioning material, e.g. elastic foam, fabric filled with fluid, e.g. inflatable elements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
- B65B5/02—Machines characterised by incorporation of means for making the containers or receptacles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B55/00—Preserving, protecting or purifying packages or package contents in association with packaging
- B65B55/20—Embedding contents in shock-absorbing media, e.g. plastic foam, granular material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/001—Arrangements to enable adjustments related to the product to be packaged
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/003—Arrangements to enable adjustments related to the packaging material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/02—Arrangements to enable adjustments to be made while the machine is running
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/02—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for perforating, scoring, slitting, or applying code or date marks on material prior to packaging
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B7/00—Closing containers or receptacles after filling
- B65B7/16—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons
- B65B7/20—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons by folding-down preformed flaps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B7/00—Closing containers or receptacles after filling
- B65B7/16—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons
- B65B7/28—Closing semi-rigid or rigid containers or receptacles not deformed by, or not taking-up shape of, contents, e.g. boxes or cartons by applying separate preformed closures, e.g. lids, covers
- B65B7/2842—Securing closures on containers
- B65B7/285—Securing closures on containers by deformation of the closure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B2210/00—Specific aspects of the packaging machine
- B65B2210/04—Customised on demand packaging by determining a specific characteristic, e.g. shape or height, of articles or material to be packaged and selecting, creating or adapting a packaging accordingly, e.g. making a carton starting from web material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/52—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation using roller-ways or endless conveyors
Definitions
- the present invention relates generally to the production and filling of packaging usually cardboard, here more simply referred to as "boxes", which is adapted to the height and volume of the products filling in each case the box.
- This invention relates more particularly to the field of the preparation of orders and shipments of products, nature and variable amount so that the products grouped in a box can occupy volumes and various heights.
- a first solution described in the patent FR 2,710,580 in the name of the Applicant, consists of cutting a cardboard box before filling, so as to eliminate the surplus of cardboard made useless according to the more or less reduced height of the contents of the box. It is thus formed a waste cardboard, more or less important, which must be evacuated.
- each box along its four vertical edges, from its top and on a partial height which corresponds to the difference between the initial height of the box and the height products filling this box, so as to release flaps which will then be folded just above said products.
- the reduction of the height of the body for its adaptation to the height of its contents would be combined, and the filling of the residual free spaces (already minimized) around the packaged products and above these products, by one or more bags of padding inflated or inflatable, bags whose volume or number are thus also minimized.
- the volume of the dunnage bag, deposited in the box could be such that the upper part of the bag coincides substantially with the marking height of the sidewalls in view of their folding, while providing however a height initially slightly higher for the upper part of the bag, so that after closing the box, a slight compression of the bag ensuring a good maintenance of the packaged products.
- the inflation means of the bags are located on the side of the body, facing the mouth of the bag which passes through a side face of the body.
- the position of these inflation means hinders the advance of the boxes on the conveyor, and as a result additional devices are to be provided to clear the inflation means to the passage of the boxes.
- the present invention aims to solve all of the above problems by a solution that allows a direct adaptation of the inflation of the bags to the free volume to be filled, so as to avoid measurements and / or calculations, while remaining compatible with cardboard boxes of a common type, and without the position of the inflation means obstructing the advance of the boxes on a conveyor.
- the subject of the invention is a method for producing a carton packaging, of the cashbox type, of variable volume adapted to the height of the packaged products in each case, the method providing for the cutting of the box along of its vertical edges, from its top and on a partial height, as well as the formation of fold lines at a suitable height, on the sides of the box, to delimit the upper flaps, the flaps being folded over the contents of the box previously filled, at least one inflated or inflatable cushioning bag being placed in the box, around and / or above the packaged products, after the formation of the fold lines which delimit the upper flaps, and before the folding of these flaps above the contents of the box, this method being essentially characterized by the fact that to adjust the degree of inflation of the sacking bag (s) to the existing free volume around and / or beyond After the bags have been introduced into the box but before the closure of the box by folding the flaps, each bag of packing is introduced inside the box in the non-inflated state, and this bag of wedging is inflated inside the body, in
- the wedging bag can here have a variable length, depending on the difference in height remaining between the top of the body and the highest product, especially if the inflation of the bag is made at a constant level above the body ; more simply, the bag can have a constant length, adapted to the size of the body, especially if the inflation of the bag is made at a variable level inside the body.
- the wedging bag adapts directly to the volume to be filled, which makes it possible to overcome uncertainties of volume calculation, which may adversely affect the proper wedging of the products in the box.
- the invention also relates to a combined machine for implementing the previously defined method, that is to say a machine for cutting and closing crates, with inflated or inflatable bags laying, the machine comprising a conveyor on which advance the boxes previously filled and successively encountered along the conveyor: a product height detection station inside each box, a cutting station crates along their vertical edges, on a certain height , a box flank marking station for forming the fold lines, a flap folding station above the contents of the box, and a closing cap placement station on the top of the boxes, the machine further comprising between the flank marking station and the flap folding station, a station for preparing and placing inside the crates inflatable cushioning bags, the preparation and setting station.
- chock bags comprising means for unwinding a continuous material film or sheath, wherein the chock bags are formed and separated by welding and cutting, means for inflating and closing each bag, and means laying of each bag inside a box, these laying means comprising a rigid plate adapted to be lowered inside each box, substantially at the fold lines formed in each case, this to achieve a inflating the bags corresponding to the volume to be filled and the position that will take the flaps, after folding, or to partially deflate the bags and adapt to the volume to be filled and the position that will take the flaps, after folding.
- the means for inflating the chock bags can be maintained at a constant height above the top of the boxes, as well as the means for closing, in particular by welding, inflated chocking bags.
- the means for inflating the chock bags, as well as the means for closing, in particular by welding, inflated chock bags are located at variable height and able to be introduced inside the boxes; in the latter case, said means may be associated with the means for laying bags.
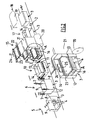
- a first station 5, encountered by the crates 3 at their entry into the machine, comprises optical organs "vision”, or alternatively one or more mechanical probes that detect the height of the products 4 inside each box 3.
- a second station 6 comprises cutting tools 7 which cut the boxes 3 along their four vertical edges 8. More particularly, the tools 7 make on the edges 8 of each box 3 a vertical section which extends over a certain height, from the top 9 of the body 3, interrupting this section above the product 4 the highest.
- a third station 10 carries out, by means of specific tools 11, a horizontal marking of the four sides 12 of the boxes 3, to form fold lines 13. More particularly, the marking is carried out on each box 3 at the same level as the lower end of the slots, made at the second station 6 along the vertical edges 8 of the box 3.
- a fourth station 15, of which a detail A is also shown in an enlarged manner, follows the marking station 10 and constitutes a station for the preparation and placement of inflated or inflatable stowing bags 16, as described in detail below.
- a fifth station 17 folds the flaps 14 along the lines 13, above the contents of each box 3, that is to say above the products 4 packed in the box and of the sacking bags 16 introduced into this box 3 at the previous station for holding said products in place 4.
- a sixth and last station 18 ensures the installation of a cardboard cap 19 on the top of each box 3, so above folded flaps 14, to achieve the closure of the body 3.
- a head storage magazine is associated laterally with the latter station 18. The boxes 3 filled, and closed at the station 18, are finally discharged at the downstream end of the conveyor 2.
- the station 15 for preparing and setting up dunnage bags 16 comprises a lateral unwinder for a reel 20 of continuous material made of film or sheath 21.
- This station 15 comprises means for pulling and guiding the material 21, causing the above each box 3 arriving at the post.
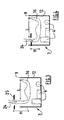
- the cutting means 22 are associated with means for laying the bags, in the form of a rigid plate 23 adapted to be lowered inside each box 3, as well as inflation means in the form of a nozzle 24. and welding means in the form of a pair of welding jaws 25 - see figure 3 .
- the inflation nozzle 24 and the welding jaws 25 are held at a constant height above the top 9 of the boxes 3.
- the bag 16 is then inflated with air, using the nozzle 24, then it is closed by welding by means of the jaws 25.
- the bag 16 is thus inflated to the maximum that allows the position of the plate rigid 23, this bag 16 then filling all the free space between the products 4 and the rigid plate 23.
- the figures 2 and 4 relate to a variant in which the inflation means, comprising the nozzle 24 and the welding jaws 25, are carried by the rigid plate 23 and can thus be descended, with this plate 23, inside each box 3.
- the wedging bag 16 here has a constant length "L + H", L being the fixed horizontal length portion of the bag 16 inside the body 3, and H being the difference in height, also fixed, between the top of the products 4 and the corresponding level at which the nozzle 24 and the jaws 25 are brought.
- this variant in which the inflation and welding means of the wedging bags 16 are "embedded" in the tooling of these bags, is particularly suitable in the case where the bags 16 detached are already welded in part, before inflation, only a rather short area is left un-welded on one side during the preparation of the bag; thus the welding means such as the welding jaws 25 are of reduced length and can be easily placed on the laying tool and introduced inside the boxes 3.
- the figure 5 illustrates another embodiment of the method of the invention, in which the wedging bags 16 are inflated to a predefined maximum degree, before being put into place in the boxes 3.
- each bag 16 is detached by the cutting means 22, then the bag 16 is inflated with air at its maximum by means of a nozzle. Then, the inflated cushioning bag 16 is lowered and placed inside the corresponding box 3, above the products 4, as illustrated in particular by the enlarged detail A of the figure 5 .
- the bag 16 considered can be pinched at its center by a tab 26 formed on its upper face along a center line.
- the wedging bag 16 is pierced at its upper lug 26, while the rigid plate 23 is applied to the bag 16 by being positioned at the marks previously made on the sides 12 of the body 3. L Excess air then escapes from the bag 16, then this bag 16 is welded again, and closed again, at the level of the tab 26.
- the inflation of each bag 16 is adapted in each case to the volume remaining to be filled. inside the box 3, around the products 4 and above them, without a measurement or a preliminary calculation of the available volume is necessary.
- inflated bags 16 are used before they are put in place, or inflatable bags which are inflated only after they have been placed in boxes 3, the method and the machine of the invention make it possible in all cases to optimize the packaging of products 4 of various heights, adapting and minimizing the volume and in particular the height of each box 3, and adapting and also minimizing the volume of the bag 16 necessary for setting products 4.
- the method of the invention is applicable not only by marking on each side of the boxes a fold line whose level corresponds exactly to the height of the products placed in the boxes, but also following "Bearings" of predefined height and approaching the height of the products which allows an automatic palletization of crates, with constitution of layers of uniform height.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Container Filling Or Packaging Operations (AREA)
- Making Paper Articles (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
- Control And Other Processes For Unpacking Of Materials (AREA)
Claims (6)
- Verfahren zur Herstellung einer Verpackung aus Pappe in der Art einer Schachtel mit variablem Volumen, die an die Höhe der in jedem Fall verpackten Produkte (4) angepasst ist, wobei das Verfahren das Schneiden der Schachtel (3) entlang ihrer vertikalen Kanten (8) von ihrem höchsten Punkt (9) und über eine teilweise Höhe vorsieht sowie die Ausbildung von Faltlinien(13) in einer entsprechenden Höhe über die Seiten (12) der Schachtel, um obere Umschlagklappen (14) zu begrenzen, wobei die Umschlagklappen (14) über dem Inhalt der zuvor gefüllten Schachtel (3) gefaltet werden, wobei nach der Ausbildung der Faltlinien (13), die die oberen Umschlagklappen (14) begrenzen, und vor dem Falten dieser Umschlagklappen (14) über dem Inhalt der Schachtel (3) mindestens ein aufgeblasener oder aufblasbarer Polsterbeutel (16) in der Schachtel (3) um und/oder über den verpackten Produkten (4) platziert wird, dadurch gekennzeichnet, dass, um den Grad des Aufblasens des oder der Polsterbeutel (16) gemäß dem vorhandenen freien Volumen um und/oder über den verpackten Produkten (4) nach Einlegen des oder der Beutel (16) in die Schachtel (3), aber vor dem Verschließen dieser Schachtel (3) durch Falten der Umschlagklappen (14) anzupassen, jeder Polsterbeutel (16) in nicht aufgeblasenem Zustand in die Schachtel (3) gelegt wird, und dass der Beutel (16) in der Schachtel (3) in einem Volumen aufgeblasen wird, das der Höhe nach durch Einlegen eines starren Elements in der Art einer Platte (23) in die Schachtel (3) begrenzt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der Polsterbeutel (16) eine variable Länge (L+H), die Funktion der verbleibenden Höhendifferenz zwischen dem höchsten Punkt (9) der Schachtel (3) und dem höchsten Produkt (4) ist, wobei das Aufblasen des Beutels (16) insbesondere auf einem konstanten Niveau über der Schachtel (3) durchgeführt wird.
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass der Polsterbeutel (16) eine konstante Länge (L+H) hat, die an das Format der Schachtel (3) angepasst ist, wobei das Aufblasen des Beutels (16) auf einem variablen Niveau in der Schachtel (3) durchgeführt wird.
- Kombinierte Maschine zum Schneiden und Verschließen von Schachteln mit Einsetzen von aufgeblasenen oder aufblasbaren Polsterbeuteln für die Umsetzung des Verfahrens nach einem der Ansprüche 1 bis 3, wobei die Maschine ein Förderband (2) umfasst, auf dem sich die zuvor gefüllten Schachteln (3) fortbewegten und nacheinander entlang des Förderbands (2) absolvieren: eine Arbeitsstation (5) zur Detektion der Höhe der Produkte (4) in jeder Schachtel (3), eine Arbeitsstation (6) zum Schneiden der Schachteln (3) entlang ihrer vertikalen Kanten (8) über eine bestimmte Höhe, eine Arbeitsstation (10) zur Markierung der Seiten (12) der Schachteln (3) zwecks Ausbildung der Faltlinien (13), eine Arbeitsstation (17) zum Falten der Umschlagklappen (14) über dem Inhalt der Schachtel (3) und eine Arbeitsstation (18) zum Einlegen von Verschlussdeckeln (19) auf dem höchsten Punkt der Schachteln (3), wobei die Maschine außerdem zwischen der Arbeitsstation (10) zur Markierung der Seiten (12) und der Arbeitsstation (17) zum Falten der Umschlagklappen (14) eine Arbeitsstation (15) zur Vorbereitung und Platzierung aufblasbarer Polsterbeutel (16) in die Schachteln (3) umfasst, wobei die Arbeitsstation (15) zur Vorbereitung und Platzierung der Polsterbeutel (16) Abrollmittel (20) eines kontinuierlichen Folien- oder Hüllenmaterial (21) umfasst, aus dem die Polsterbeutel (16) ausgebildet und durch Schweißen oder Schneiden abgetrennt werden, Aufblas- (24) und Verschlussmittel (25) jedes Beutels (16) und Einlegemittel (23) jedes Beutels (16) in eine Schachtel (3), wobei diese Einlegemittel eine starre Platte (23) umfassen, die imstande ist, in jede Schachtel (3) etwa auf das Niveau der in jedem Fall ausgebildeten Faltlinien (13) abgesenkt zu werden, um ein Aufblasen der Beutel (16) entsprechend dem auszufüllenden Volumen und der Position, die die Umschlagklappen (14) nach dem Falten hinnehmen werden, durchzuführen, oder um die Beutel (16) teilweise zu entleeren und sie an das auszufüllende Volumen und an die Position, die die Umschlagklappen (14) nach dem Falten einnehmen werden, anzupassen.
- Maschine nach Anspruch 4, dadurch gekennzeichnet, dass die Aufblasmittel (24) der Polsterbeutel (16) in einer konstanten Höhe über dem höchsten Punkt der Schachteln (3) gehalten werden, ebenso wie die Mittel zum Verschließen (25), vor allem durch Schweißen, der Polsterbeutel (16).
- Maschine nach Anspruch 4, dadurch gekennzeichet, dass sich die Aufblasmittel (24) der Polsterbeutel (15), ebenso wie die Verschlussmittel (25) der aufgeblasenen Polsterbeutel {16}, ihn variabler Höhe befinden und imstande sind, in die Schachteln (3) eingeführt zu werden, wobei die Mittel (24, 25) mit den Einlegemitteln (23) der Schachteln (16) kombinierbar sind.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL08839140T PL2185424T3 (pl) | 2007-08-02 | 2008-07-31 | Sposób i maszyna kombinowana do cięcia i zamykania kartonów z umieszczaniem toreb stabilizujących |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0705666A FR2919520B1 (fr) | 2007-08-02 | 2007-08-02 | Procede et machine combinee de coupe et de fermeture de caisses avec pose de sacs de calage |
| PCT/FR2008/001144 WO2009050350A2 (fr) | 2007-08-02 | 2008-07-31 | Procédé et machine combinée de coupe et de fermeture de caisses avec pose de sacs de calage |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2185424A2 EP2185424A2 (de) | 2010-05-19 |
| EP2185424B1 true EP2185424B1 (de) | 2011-07-13 |
Family
ID=39092834
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08839140A Not-in-force EP2185424B1 (de) | 2007-08-02 | 2008-07-31 | Verfahren und maschine zum schneiden und verschliessen von schachteln und zum einsatz von polsterbeuteln |
Country Status (10)
| Country | Link |
|---|---|
| US (1) | US7823367B2 (de) |
| EP (1) | EP2185424B1 (de) |
| CN (1) | CN101801794B (de) |
| AT (1) | ATE516211T1 (de) |
| CA (1) | CA2694995C (de) |
| ES (1) | ES2369227T3 (de) |
| FR (1) | FR2919520B1 (de) |
| PL (1) | PL2185424T3 (de) |
| RU (1) | RU2468978C2 (de) |
| WO (1) | WO2009050350A2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021089302A1 (de) | 2019-11-05 | 2021-05-14 | Opitz Packaging Systems Gmbh | Verfahren zum automatischen rillen einer faltkiste mit eingesetztem packgut |
Families Citing this family (36)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT1395019B1 (it) * | 2009-07-23 | 2012-09-05 | Progetto C S R L | Metodo per la definizione di contenitori scatolari attorno a gruppi di articoli |
| US8672180B2 (en) | 2011-07-29 | 2014-03-18 | Sealed Air Corporation | Dispensing bin for multiple materials |
| US20130168441A1 (en) * | 2011-12-30 | 2013-07-04 | 3M Innovative Properties Company | Article and methods for preparing an object for sterilization |
| US9821925B2 (en) | 2012-01-18 | 2017-11-21 | Rengo Co., Ltd. | Method and device for assembling height-adjustable box |
| DE102012004208B4 (de) * | 2012-03-06 | 2016-04-21 | Opitz Maschinentechnik Gmbh | Verfahren und Verschlussmaschine zum automatischen Verschließen einer Faltkiste mit Verpackungsgütern |
| DE102012102117A1 (de) * | 2012-03-13 | 2013-09-19 | Phoenix Contact Gmbh & Co. Kg | Verpackungsanlage und Verfahren zum Verpacken von Versandgut |
| GB201210170D0 (en) * | 2012-06-08 | 2012-07-25 | Linkx Systems Ltd | Container sizing method and system |
| FI124705B (fi) * | 2012-07-12 | 2014-12-15 | Jomet Oy | Laitteisto pakkauslaatikon korkeuden säätämiseksi ja laatikon sulkemiseksi |
| ES2770623T3 (es) * | 2012-09-18 | 2020-07-02 | Ranpak Corp | Método de distribución de material de estiba |
| ITBO20130388A1 (it) * | 2013-07-23 | 2015-01-24 | Gd Spa | Unita' e metodo di incarto per la piegatura di uno sbozzato in una macchina impacchettatrice. |
| ITMO20130257A1 (it) * | 2013-09-20 | 2015-03-21 | System Spa | Dispositivo per definire un volume di articoli da imballare e macchina e relativo metodo di confezionamento |
| DE102014101268B4 (de) * | 2014-02-03 | 2016-09-29 | SSI Schäfer PEEM GmbH | Packverfahren und Pack-Arbeitsplatz |
| FR3017858B1 (fr) * | 2014-02-24 | 2016-03-18 | B & Equipment | Procede et machine pour fermer des boites a section carree ou rectangulaire en reduisant leur hauteur a celle de leur contenu. |
| DE102014103355A1 (de) * | 2014-03-12 | 2015-09-17 | Mondi Consumer Packaging Technologies Gmbh | Verfahren zum Verpacken von Stückgut in einer Umverpackung, Stückgut-Verpackungsanordnung sowie Fluidpolsterkissen |
| US10850906B2 (en) | 2015-03-04 | 2020-12-01 | Storopack, Inc. | Air cushion machine and method |
| GB201504880D0 (en) * | 2015-03-23 | 2015-05-06 | Linkx Systems Ltd | Container sizing |
| AU2016241566B2 (en) * | 2015-04-01 | 2021-01-21 | C.M.C. S.P.A. | System and method for forming a custom-sized package |
| US10759133B2 (en) * | 2015-06-15 | 2020-09-01 | International Boxes S.R.L. | Machine for automatically manufacturing customized packaging items |
| JP6062505B1 (ja) | 2015-07-23 | 2017-01-18 | Ckd株式会社 | シール装置、ブリスタ包装機及びブリスタパックの製造方法 |
| ITUA20163733A1 (it) * | 2016-05-24 | 2017-11-24 | F L Auto Srl | Stazione di piegatura per la piegatura di un cartone di imballaggio e macchina per l’imballaggio di un articolo all’interno di una scatola di cartone ottenuta dal cartone di imballaggio |
| EP3284687B1 (de) * | 2016-08-16 | 2020-11-04 | Quadient Technologies France | System und verfahren zum automatischen verpacken von artikeln unterschiedlicher grösse und anzahl für den versand |
| EP3354581B1 (de) * | 2017-01-31 | 2021-05-19 | Quadient Technologies France | System und verfahren zur automatischen verpackung unterschiedlicher versandsätze |
| JP7164620B2 (ja) * | 2017-11-27 | 2022-11-01 | ランパク コーポレーション | 配送用の箱の高さを最適化するためのシステム及び方法 |
| EP3749581B1 (de) * | 2018-02-07 | 2022-03-30 | Ranpak Corp. | Automatische polsterformvorrichtung und verfahren |
| CN109353590B (zh) * | 2018-11-20 | 2024-02-09 | 圣奥科技股份有限公司 | 一种办公家具板材的包装线 |
| JP7265121B2 (ja) * | 2019-01-11 | 2023-04-26 | 裕子 大村 | 段ボール箱の折り曲げ装置 |
| CN112591174B (zh) * | 2020-11-27 | 2022-06-24 | 兰剑智能科技股份有限公司 | 一种全自动纸箱包装机 |
| CN113086307A (zh) * | 2021-03-31 | 2021-07-09 | 张桂莲 | 一种手机壳包装设备 |
| US20230124423A1 (en) * | 2021-10-15 | 2023-04-20 | Cornerstone Automation Systems, Llc | Automated container resizing apparatus, a system including the apparatus, and a method of resizing a container |
| FR3136226B1 (fr) * | 2022-06-01 | 2024-07-19 | Durrenberg | Procédé de réduction d’une hauteur initiale d’un emballage, tel qu’une caisse américaine, en fonction de son contenu et dispositif pour mettre en œuvre un tel procédé |
| CN119677676A (zh) * | 2022-09-08 | 2025-03-21 | Abb瑞士股份有限公司 | 包装系统和用于包装对象的方法 |
| IT202300000447A1 (it) * | 2023-01-16 | 2024-07-16 | Ima Spa | Apparecchiatura e procedimento di lavorazione di una scatola contenente uno o più oggetti da confezionare. |
| FR3148010B1 (fr) | 2023-04-19 | 2025-06-13 | Durrenberg | Procédé et machine d’emballage pour la fermeture par une coiffe d'une caisse de forme parallélépipédique rectangle ouverte sur le dessus |
| CN116552017B (zh) * | 2023-07-10 | 2023-09-15 | 湖南省康普通信技术有限责任公司 | 一种基于光信号测距实现的非接触式仿形包装方法及设备 |
| CN118953799B (zh) * | 2024-10-16 | 2025-01-24 | 四川菊乐食品股份有限公司 | 一种产品箱自动成型装箱装置 |
| FR3161904A1 (fr) | 2025-05-05 | 2025-11-07 | Durrenberg | Procédé et machine d’emballage pour la fermeture par une coiffe d'une caisse de forme parallélépipédique rectangle ouverte sur le dessus |
Family Cites Families (33)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3313467A (en) * | 1965-04-27 | 1967-04-11 | Juel U Anderskow | Corrugated carton box |
| US3598303A (en) * | 1969-02-20 | 1971-08-10 | George W Folz | Variable sized box form |
| DE2440885C3 (de) * | 1974-08-27 | 1980-06-19 | Focke & Pfuhl, 2810 Verden | Vorrichtung zum Einhüllen von Gegenständen wechselnder Höhe |
| US3953956A (en) * | 1974-11-29 | 1976-05-04 | Hayssen Manufacturing Company | Apparatus for forming flaps on a carton |
| FR2385606A1 (fr) | 1977-03-29 | 1978-10-27 | Asnieres Prony Ste Civile Immo | Perfectionnements apportes a un procede d'elaboration d'emballage aux fins de transport, en particulier de marchandises sensibles aux chocs et/ou aux vibrations, ainsi que les emballages s'y rapportant |
| FR2456677A1 (fr) * | 1979-05-14 | 1980-12-12 | Jaffre Felicien | Procede de calage d'objets ou de produits dans un emballage |
| CH648800A5 (de) * | 1980-12-03 | 1985-04-15 | Involvo Ag | Sammelpackmaschine. |
| DE3233471C2 (de) * | 1982-09-09 | 1998-09-17 | Focke & Co | Vorrichtung zum Prägen von Faltlinien in einem Faltkarton |
| NL8600036A (nl) | 1985-04-19 | 1986-11-17 | Hiroshi Yamashiro | Schokbreker en werkwijze en apparaat voor het vervaardigen daarvan. |
| GB2178694B (en) | 1985-06-06 | 1990-01-31 | Hiroshi Yamashiro | Dunnage shock absorber and method and apparatus for making same |
| FR2606367A1 (fr) | 1986-11-12 | 1988-05-13 | Guy Letard | Procede d'encaissage de produits de hauteur variable |
| FR2612885A1 (fr) | 1987-01-22 | 1988-09-30 | Chandellier Antoine | Caisse dite " americaine " a hauteur variable et dispositif mecanique pour sa fabrication |
| DE3813309A1 (de) * | 1987-04-21 | 1989-08-03 | Avon Cosmetics Gmbh | Verfahren zur transportsicheren verpackung von kommissionen, hierdurch erreichte verpackungseinheit sowie eine anordnung zum verpacken |
| NL8901162A (nl) * | 1989-05-09 | 1990-12-03 | Texim Electronics B V | Werkwijze voor het immobiliseren van los in een alzijdig gesloten verpakking geplaatste artikelen, en verpakking volgens deze werkwijze. |
| US5016753A (en) * | 1989-07-28 | 1991-05-21 | Henderson Donald M | Telescoping packaging system |
| RU2129976C1 (ru) * | 1992-03-16 | 1999-05-10 | Интепак Текнолоджиз Инк. | Упаковочный узел (варианты) |
| US5454407A (en) * | 1992-09-24 | 1995-10-03 | Diba Industries Inc. | Pneumatic wand apparatus and method |
| FR2710580B1 (fr) * | 1993-09-29 | 1995-11-03 | Savoye Nouvelle Sa | Maintien d'une charge dans un emballage et dispositif de coupe d'emballage. |
| US5552003A (en) * | 1994-10-04 | 1996-09-03 | Hoover; Gregory A. | Method for producing inflated dunnage |
| US6676009B1 (en) * | 1997-09-30 | 2004-01-13 | Harold J. Rose | Container having a plurality of selectable volumes |
| US6119929A (en) * | 1997-09-30 | 2000-09-19 | Rose; Harold J. | Container having a plurality of selectable volumes |
| US6253919B1 (en) * | 1998-04-13 | 2001-07-03 | Sealed Air Corporation | Inflatable packing material |
| US6536183B1 (en) * | 1998-12-21 | 2003-03-25 | Free-Flow Packaging International, Inc. | Air-filled packing cushion delivery system |
| CN2518385Y (zh) * | 2002-03-11 | 2002-10-30 | 史丽 | 多功能组合安全旅游包 |
| DE60306407C9 (de) * | 2002-11-01 | 2021-09-09 | Ranpak Corp. | Verpackungssystem mit messen vom polster-füllmaterial |
| US6996955B2 (en) * | 2003-09-12 | 2006-02-14 | Sealed Air Corporation (Us) | System for conveying packaging cushions |
| CA2556975A1 (en) | 2004-02-04 | 2005-08-25 | Inflatable Packaging, Inc. | Packaging system with inflatable cushion |
| CN101035712B (zh) * | 2004-08-04 | 2013-01-02 | 兰帕克公司 | 包装系统和方法 |
| US8020358B2 (en) | 2004-11-02 | 2011-09-20 | Sealed Air Corporation (Us) | Apparatus and method for forming inflated containers |
| JP4301172B2 (ja) * | 2005-01-31 | 2009-07-22 | 村田機械株式会社 | 流体注入装置 |
| EP1922254B1 (de) * | 2005-08-19 | 2010-03-17 | Ranpak Corp. | Verpackungssystem und verfahren zur erfassung von geschlossenen behältern |
| FR2898072B1 (fr) * | 2006-03-06 | 2009-06-05 | Savoye Sa | Procede et dispositif pour la realisation d'un emballage en carton de volume variable |
| US7814733B2 (en) * | 2006-04-10 | 2010-10-19 | Ranpak Corp. | Packaging system with volume measurement |
-
2007
- 2007-08-02 FR FR0705666A patent/FR2919520B1/fr not_active Expired - Fee Related
- 2007-11-28 US US11/987,258 patent/US7823367B2/en active Active
-
2008
- 2008-07-31 CA CA2694995A patent/CA2694995C/fr not_active Expired - Fee Related
- 2008-07-31 EP EP08839140A patent/EP2185424B1/de not_active Not-in-force
- 2008-07-31 ES ES08839140T patent/ES2369227T3/es active Active
- 2008-07-31 PL PL08839140T patent/PL2185424T3/pl unknown
- 2008-07-31 CN CN2008801007744A patent/CN101801794B/zh not_active Expired - Fee Related
- 2008-07-31 AT AT08839140T patent/ATE516211T1/de active
- 2008-07-31 WO PCT/FR2008/001144 patent/WO2009050350A2/fr not_active Ceased
- 2008-07-31 RU RU2010107452/13A patent/RU2468978C2/ru active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021089302A1 (de) | 2019-11-05 | 2021-05-14 | Opitz Packaging Systems Gmbh | Verfahren zum automatischen rillen einer faltkiste mit eingesetztem packgut |
Also Published As
| Publication number | Publication date |
|---|---|
| RU2010107452A (ru) | 2011-09-10 |
| CN101801794B (zh) | 2012-05-30 |
| ATE516211T1 (de) | 2011-07-15 |
| EP2185424A2 (de) | 2010-05-19 |
| CA2694995A1 (fr) | 2009-04-23 |
| CN101801794A (zh) | 2010-08-11 |
| WO2009050350A3 (fr) | 2009-07-23 |
| US20090031676A1 (en) | 2009-02-05 |
| RU2468978C2 (ru) | 2012-12-10 |
| FR2919520A1 (fr) | 2009-02-06 |
| CA2694995C (fr) | 2015-12-22 |
| US7823367B2 (en) | 2010-11-02 |
| FR2919520B1 (fr) | 2011-01-07 |
| ES2369227T3 (es) | 2011-11-28 |
| PL2185424T3 (pl) | 2011-12-30 |
| WO2009050350A2 (fr) | 2009-04-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2694995C (fr) | Procede et machine combinee de coupe et de fermeture de caisses avec pose de sacs de calage | |
| EP2258627B1 (de) | Verpackungsvorrichtung und Verfahren zum Verpacken geschichteter weicher Hygieneprodukte in einen Kunststoffbeutel | |
| EP1671883B1 (de) | Vorrichtung und Verfahren zum Verpacken von Reifen | |
| EP2412636B1 (de) | Anlage zur Verpackung von Warenlosen | |
| US20100310198A1 (en) | Plastic bag for stacked soft hygienic products | |
| US20160251097A1 (en) | Process and apparatus for packaging potato crisps, as well as the package obtained | |
| WO1990003263A1 (fr) | Procede et dispositif pour ameliorer la rigidite d'un conteneur en matiere synthetique | |
| US4069349A (en) | Process for vacuum packaging of roasted, ground coffee | |
| EP1832413B1 (de) | Verfahren und Vorrichtung zur Herstellung von Kartonverpackungen mit variablem Volumen | |
| FR2855147A1 (fr) | Procede et unite pour emballer des groupes de produits | |
| EP3797968B1 (de) | Vorrichtung zum thermoformen, folienverschliessen und schneiden von behähltern von unterschiedlichen grössen | |
| FR2483881A3 (fr) | Appareil et procede pour le remplissage d'un recipient flexible | |
| EP1851113B1 (de) | Verfahren und anlage zur verpackung von gefuellten flexiblen beuteln | |
| CH614671A5 (en) | Method and machine for packaging a particulate product | |
| FR2524419A1 (fr) | Procede d'emballages dans des cartons, sans soulever le produit a emballer, et machine pour la mise en oeuvre de ce procede | |
| FR3101858A1 (fr) | Dispositif et procédé de formage de conteneur par pliage | |
| FR2877642A1 (fr) | Dispositif de transfert de sacs | |
| BE710298A (de) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20100217 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| 17Q | First examination report despatched |
Effective date: 20100812 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: FOULON, JOEL Inventor name: BOIGUES, MICHEL |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: FRENCH |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602008008280 Country of ref document: DE Effective date: 20110908 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2369227 Country of ref document: ES Kind code of ref document: T3 Effective date: 20111128 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: T2 Effective date: 20110713 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20110402346 Country of ref document: GR Effective date: 20111117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111113 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111114 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E012328 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: NO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110731 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 |
|
| 26N | No opposition filed |
Effective date: 20120416 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602008008280 Country of ref document: DE Effective date: 20120416 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: RE |
|
| PGRI | Patent reinstated in contracting state [announced from national office to epo] |
Ref country code: NO Effective date: 20121126 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110731 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20130618 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110713 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BG Payment date: 20130628 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: HU Payment date: 20130702 Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: ML Ref document number: 20110402346 Country of ref document: GR Effective date: 20150204 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150331 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150204 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ICB INGENIEURS CONSEILS EN BREVETS SA, CH Ref country code: CH Ref legal event code: PUE Owner name: SAVOYE, FR Free format text: FORMER OWNER: SAVOYE, FR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602008008280 Country of ref document: DE Representative=s name: PATENT- UND RECHTSANWAELTE LOESENBECK, SPECHT,, DE Ref country code: DE Ref legal event code: R081 Ref document number: 602008008280 Country of ref document: DE Owner name: A-SIS SOCIETE PAR ACTION SIMPLIFIEE, FR Free format text: FORMER OWNER: SAVOYE, DIJON, FR |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: CHAD Owner name: SAVOYE S.A.S.U., FR Ref country code: NO Ref legal event code: CREP Representative=s name: BRYN AARFLOT AS, STORTINGSGATA 8, 0161 OSLO, NORGE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20210416 Year of fee payment: 14 Ref country code: NL Payment date: 20210519 Year of fee payment: 14 Ref country code: NO Payment date: 20210624 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 516211 Country of ref document: AT Kind code of ref document: T Owner name: SAVOYE, FR Effective date: 20210708 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20210512 Year of fee payment: 14 Ref country code: CH Payment date: 20210611 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20210621 Year of fee payment: 14 Ref country code: IT Payment date: 20210707 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20210812 Year of fee payment: 14 Ref country code: BE Payment date: 20210726 Year of fee payment: 14 Ref country code: DE Payment date: 20210519 Year of fee payment: 14 Ref country code: SE Payment date: 20210721 Year of fee payment: 14 Ref country code: PL Payment date: 20210701 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: PD Owner name: A-SIS; FR Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT Effective date: 20210208 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: HC Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CHANGE OF OWNER(S) NAME Effective date: 20210407 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602008008280 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: MMEP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20220801 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 516211 Country of ref document: AT Kind code of ref document: T Effective date: 20220731 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20220731 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20220731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220801 Ref country code: NO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230201 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220801 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230525 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20230901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220731 |