EP2208551B1 - Procédé de fabrication d'une pièce de tôle préformée complexe - Google Patents
Procédé de fabrication d'une pièce de tôle préformée complexe Download PDFInfo
- Publication number
- EP2208551B1 EP2208551B1 EP09015648.0A EP09015648A EP2208551B1 EP 2208551 B1 EP2208551 B1 EP 2208551B1 EP 09015648 A EP09015648 A EP 09015648A EP 2208551 B1 EP2208551 B1 EP 2208551B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheet metal
- forming
- die
- tool
- contour
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 239000002184 metal Substances 0.000 title claims description 73
- 238000004519 manufacturing process Methods 0.000 title claims description 6
- 238000000034 method Methods 0.000 claims description 35
- 238000005452 bending Methods 0.000 claims description 20
- 239000007769 metal material Substances 0.000 claims description 9
- 238000003825 pressing Methods 0.000 claims description 8
- 230000015572 biosynthetic process Effects 0.000 claims description 4
- 238000005520 cutting process Methods 0.000 claims description 3
- 230000000717 retained effect Effects 0.000 claims description 2
- 238000009434 installation Methods 0.000 claims 1
- 238000007493 shaping process Methods 0.000 description 20
- 239000000463 material Substances 0.000 description 19
- 238000011161 development Methods 0.000 description 12
- 230000018109 developmental process Effects 0.000 description 12
- 238000005482 strain hardening Methods 0.000 description 6
- 230000006835 compression Effects 0.000 description 3
- 238000007906 compression Methods 0.000 description 3
- 238000000465 moulding Methods 0.000 description 3
- 230000000052 comparative effect Effects 0.000 description 2
- 238000012938 design process Methods 0.000 description 2
- 230000009466 transformation Effects 0.000 description 2
- 238000004140 cleaning Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 238000007688 edging Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 239000000314 lubricant Substances 0.000 description 1
- 239000011159 matrix material Substances 0.000 description 1
- 238000010422 painting Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 230000000284 resting effect Effects 0.000 description 1
- 238000004904 shortening Methods 0.000 description 1
- 230000000087 stabilizing effect Effects 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
- 238000009966 trimming Methods 0.000 description 1
- 238000011144 upstream manufacturing Methods 0.000 description 1
Images
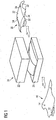

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D22/00—Shaping without cutting, by stamping, spinning, or deep-drawing
- B21D22/02—Stamping using rigid devices or tools
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D53/00—Making other particular articles
- B21D53/88—Making other particular articles other parts for vehicles, e.g. cowlings, mudguards
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D19/00—Flanging or other edge treatment, e.g. of tubes
- B21D19/08—Flanging or other edge treatment, e.g. of tubes by single or successive action of pressing tools, e.g. vice jaws
Definitions
- the invention relates to a method for producing a complex sheet metal part, as well as a complex sheet metal part produced by this method, (see, eg DE-A-19524235 ).
- a complex sheet metal part is understood in the context of this invention, due to its spatial shape or shape only consuming writable sheet metal part.
- a complex sheet-metal shaped part can be composed or formed from many individual, even curved, surface sections. Due to its complex shape, such a complex sheet metal part according to the current state of the art can only be produced in a complex manner.
- the complex sheet metal parts are simply shaped sheet metal parts opposite, which can be easily described and produced in a simple manner, for example. By simple bending operations or the like.
- Body parts for motor vehicles in particular body panels and structural parts, are often complex sheet metal parts.
- An object of the invention is to provide a comparatively favorable possibility to be able to provide complex sheet-metal shaped parts with a high quality level.
- more than two free-form surfaces and a plurality of contour lines are formed.
- a plurality of free-form surfaces is formed.
- at least one free-form surface is formed, which is delimited at least in sections by at least one contour line.
- ruled surface can be understood to mean a surface or a surface section which can be described in a mathematically simple manner. Ruled surfaces can in particular be planes, one-dimensionally curved surfaces with constant radii of curvature, lateral surfaces of cylinders, cones and the like.
- free-form surface can be understood to mean a complex, preferably multi-curved surface which, in particular, can not be mathematically described by simple geometric basic forms such as straight line, circle and conic section.
- a free-form surface can, for example, have complex concave and / or convex sections.
- a ruled surface and a free-form surface are characterized in particular by the fact that they have only a slight change in shape (comparative shape change). In the case of work hardening sheet metal materials, this change in shape is particularly so small that no appreciable cold work hardening occurs during forming.
- a "contour line” is understood to mean a bending line or a bending edge.
- Such a contour line is defined essentially by its spatial course, its bending angle and / or its bending radius.
- a contour line preferably has a curved and in particular a spatially multiply curved course.
- the bend radius and / or the bend angle may vary along the course.
- the bending contour can deviate from a circle segment.
- the bending angle is chosen so that a crack-free forming is guaranteed.
- the bending radius is at least partially selected so that when forming a cold work hardening sheet material, a work hardening occurs.
- the output board essentially corresponds to a precise development of the ready-to-install sheet metal part. This implies that during the forming no stretching or compression of the sheet material takes place, so that the starting sheet thickness is maintained in an advantageous manner over the entire sheet metal part. An exception form the areas of the contour lines, in which in particular a bending shortening can occur, which can be considered in the development of the sheet metal part quite well, which is indicated by the wording "essentially".
- the blank determination is preferably carried out by means of CAD systems.
- the invention is based on the idea of designing a complex sheet metal part such that it comprises free-form surfaces which are separated from one another by means of at least one contour line or subdivided by means of this contour line.
- the free-form surfaces are defined here by the spatial progression of an adjacent contour line or of all contiguous contour lines. That The spatial shape or the shape of the adjacent surfaces or surface sections is predetermined or determined by the spatial progression of a contour line.
- the 3D geometry determination for the sheet metal part is about to divide the overall geometry into individual free-form surfaces and based on the spatial shape of these individual surfaces or surface sections suitable gradients for the contour lines, and to define suitable bending angle and / or bending radii , whereby the reverse sequence is possible.
- the shape of the sheet metal part must also be developable in the plane, as explained above.
- the invention has many advantages.
- the forming takes place essentially in only one main forming stage, for which only one forming tool and only one forming press are required. Due to the resulting low investment costs, the invention is therefore particularly suitable for small quantities and small batches. However, this does not preclude the fact that the Hauptumformwork follow other Umformworkn or may be upstream.
- the sheet metal parts produced by the process according to the invention to a high level of quality, which is quite close to the quality of deep-drawn metal parts, although in the production of sheet metal parts according to the invention explicitly no deep-drawing process is performed. But that does not contradict that the method according to the invention can be combined with a deep drawing process. Furthermore arise for the design process of the sheet metal part new degrees of freedom.
- a front flap with integrated side walls or a complete floor assembly for a motor vehicle which is usually realized in the art by a plurality of sheet metal parts joined together and thus is correspondingly complex and costly.
- the forming takes place between a substantially rigid lower and a substantially rigid upper tool part, which are arranged in a forming press, wherein at least one of these tool parts has at least one closed shaping tool contour.
- all tool parts that are directly involved in forming have a closed shaping tool contour.
- the tool parts can also be referred to as upper tool and lower tool. These can each be constructed in several parts. By using rigid tool parts, the quality of the produced sheet metal parts can be improved.
- a bend (of the sheet metal material) takes place with a small bending radius.
- the term "small” here refers in particular to the relationship between the bending radius and the starting sheet thickness. Preferably, this ratio is in the range between 5 and 10 and in particular in the range between 2 and 5.
- the inventive method advantageously offers the possibility of defined formation of small radii and very small radii despite large depths of form, and this in particular even at high forming speeds.
- the application can be done, for example, by means of the upper tool to a shaping tool contour in the lower tool, or vice versa.
- the use of lubricant can thus largely be dispensed with; in addition, sheet metal materials with coated, pretreated and / or ready-to-install surfaces, in particular painted surfaces, can be used. Also, a hold-down is not required, so that a Ziehflansch deleted and sheet material is saved.
- a pressing operation is carried out, in which at least one contour line (of the sheet metal part) is finally formed or pronounced.
- This pressing operation is preferably carried out in the same forming tool and with high pressing forces, which are a multiple of the previous forming forces.
- At least one free-form surface of the sheet metal part is provided with a structuring of rigidity at least in sections during a pressing operation.
- Such structuring may be, for example, an embossed honeycomb structure or the like.
- the positioning of the output board in the forming tool takes place by means of at least one locking device.
- a locking device may, for example, be a simple locking pin or locking bolt.
- a suction device may be included in the forming tool.
- openings in the sheet metal part are formed by pre-apertures in the output board.
- Such openings may be bores, contoured recesses and the like. Starting from their position in the sheet metal part takes place through the plane Processing their positioning on the output board. This makes it possible to dispense with subsequent expensive cutting tools.
- the final formation of at least one contour line (of the sheet metal part) or a folding or edging by means of a separately movable tool part of the same Umformtechnikmaschines done in a similar manner undercuts on the sheet metal part can be produced.
- the separate tool part can be actuated, for example, by means of an auxiliary ram or a die cushion of the forming press.
- a complex shaped sheet metal part according to the invention is produced by the process according to the invention. This comprises at least two free-form surfaces, which are delimited from one another by at least one contour line, wherein the F formiform surfaces have a relatively small change in shape over their entire extent and a rigidity of the sheet metal part results to a significant extent from the at least one contour line.
- the rigidity can be, for example, the overall stiffness (for example, relevant to the crash case), the torsional stiffness or the average buckling stiffness.
- the rigidity of the sheet metal part results in particular from the prevailing stresses in the free-form surfaces, from a possible structuring of these surfaces, from the bending resistance of all contour lines, from the stress distribution of the upper side of the sheet to the underside of sheet metal in particular in the region of these contour lines and from a work hardening along these contour lines.
- the rigidity of the sheet metal part is to result in a substantial proportion from at least one contour line and preferably from the totality of all contour lines insofar as the free-form surfaces are stabilized by the adjacent contour lines.
- a contour line in particular also prevents an elastic return of an adjacent free-form surface.
- the complex sheet-metal shaped part according to the invention has, in the region of at least one contour line, at least in sections, a locally high change in shape (comparative shape change).
- the change in shape is preferably so great that a clear work hardening occurs in the sheet material, as already explained above in connection with the term "contour line”.
- Fig. 1 shows the inventive method for producing a complex sheet metal part in a schematic overview. The sequence of the process takes place according to the illustration from bottom left to top right, which is symbolized by the arrows.
- the method comprises first providing a finished trimmed output board 10 made of a sheet metal material.
- the contour of the output board 10 essentially corresponds to a precise development of the product to be produced Sheet metal part.
- the output board 10 comprises pre-punched openings in the form of contoured recesses 12 and holes 14.
- the output board 10 is positioned in a forming tool 20 with an upper tool 22 and a lower tool 25.
- the forming tool 20 is installed in a forming press, not shown.
- a contour line 34 is a spatially extending bending line or bending edge.
- the illustrated sheet metal part 30 is an example of a front flap of a motor vehicle. The transformation from the output board 10 to the sheet metal part 30 takes place in only one forming stage (Hauptumformcut). After this transformation, no trimming of the sheet metal part 30 is required.
- the sheet metal part 30 is as it were ready to install, subject to any cleaning and / or painting or the like.
- the forming of the output board 10 to the sheet metal part 30 by the forming tool 20 is shown schematically in the Fig. 2a and 2b shown.
- Fig. 2a shows the inserted between upper tool 22 and lower tool 25 output board 10. This is smaller in size than the shaping tool contours 23 and 26 of the upper tool 22 and the lower tool 25.
- the output board 10 is formed.
- the reshaping takes place in such a way that the sheet material of the output board 10 successively and / or in sections starting from at least one eg. Highest contact point to the closed forming tool contours 23 and / or 26, wherein in the following a relative movement between the adjacent sheet material and the forming tool 20 is largely avoided.
- the output sheet thickness of the output board 10 is maintained over the entire sheet metal molding 30. Consequently also have the introduced into the output board 10 openings 12 and 14 in the finished molded sheet metal part 30 their exact position and geometry, as in Fig. 1 indicated.
- Fig. 2b shows the closed forming tool 20.
- the output board 10 has been here converted in the manner described above to the sheet metal molding 30.
- a pressing operation can be carried out with high pressing forces in order to finally form at least one contour line 34 and / or to provide at least one free-form surface 32 with a stabilizing and rigidity-increasing structuring.
- This structuring is introduced by the shaping tool contours 23 and / or 26 in the sheet metal molding 30.
- Fig. 3a shows the output board 10 in a plan view, which when forming after the Fig. 2 is used. Shown here are the forming during forming contour lines 34th Fig. 3b shows the produced sheet metal part 30 in a perspective view with the freeform surfaces 32, which are delimited by the contour lines 34 to each other.
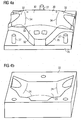
- Fig. 4a shows the lower tool 25 of the forming tool 20 in a perspective view. This includes a closed shaping tool contour 26 and three tool guides 27 for the upper tool 22. Also shown is a resting on the tool contour 26 finished molded sheet metal part 30, which in the manner described above from the output board 10 by successive and / or sectional application of the sheet material was made to the shaping tool contour 26 and can be removed from the forming tool 20 in the state shown.
- Fig. 4b shows that to Fig. 4a corresponding, turned upper tool 22 in a perspective view.
- This comprises a shaping tool contour 23, which is formed as a negative contour to the shaping tool contour 26 of the lower tool 25 with an offset.
- the application of the sheet material to the tool contour 26 of the lower tool 25 by means of the shaping tool contour 23 in the upper tool 22 (or vice versa), without a Relative movement between the sheet material and the shaping tool contours 23 and 26 is given.
- the shaping tool contours 23 and 26 comprise corresponding shaping sections, which are shown schematically in the upper tool 22 shown and designated by the reference numeral 24 and which the sheet material during closing and in particular compression of the forming tool 20 against corresponding shaping sections of the shaping tool contour 26 in Press lower tool 25 (or vice versa) to thereby form a contour line 34 exactly.
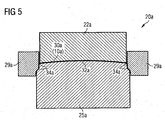
- Fig. 5 shows an alternative or supplementary possibility for forming at least one contour line.
- the same components are designated by the same reference numerals but with the addition "a”.
- the forming tool 20a comprises, in addition to the upper tool 22a and the lower tool 25a, a tool part 29a which is movable separately and parallel to the upper tool 22a.
- free-form surfaces 32a are formed between the shaping tool contours of the upper tool 22a and the lower tool 25a.
- a formation of contour lines 34a, by the tool part 29a is moved downward as shown, wherein initially a folding or stopping the sheet material down.
- the separate tool part 29a can be moved by the auxiliary ram of a forming press.
- a separate tool part can also be moved from below, for example by means of the drawing cushion of the forming press.
- undercut can also be produced on the sheet-metal shaped part 30a, for example by means of a laterally displaceable separate tool part.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Shaping Metal By Deep-Drawing, Or The Like (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
Claims (12)
- Procédé de fabrication d'une pièce préformée en tôle (30) complexe et prête au montage après la mise en forme, en un matériau en tôle comprenant les étapes consistant à :- découper une platine de départ plane (10) dont les contours correspondent essentiellement à la projection dans un plan exacte de la pièce préformée en tôle prête à être montée,- positionner la platine de départ (10) dans un outil de mise en forme (20) qui comprend au moins deux parties d'outil axialement mobile l'une par rapport à l'autre, et- déplacer axialement de ces parties d'outil l'une par rapport à l'autre, la mise en forme de la platine de départ (10) pour obtenir une pièce préformée en tôle (30) prête à être montée étant effectuée de façon à former au moins deux surfaces de forme libre (32) qui sont délimitées l'une par rapport à l'autre au moins par segments par au moins une ligne de contour (34), lors de la mise en forme, aucun écrasement ou refoulement du matériau en tôle ne se produisant de sorte que l'épaisseur de tôle de platine de départ (10) soit maintenue sur la totalité de la pièce en tôle préformée (30).
- Procédé conforme à la revendication 1,
caractérisé en ce que
la mise en forme est effectuée entre une partie d'outil inférieure rigide (22) et une partie d'outil supérieure rigide (25) qui sont montées dans une presse de mise en forme, au moins l'une de ces parties d'outil (22, 25) comprenant au moins un contour d'outil de mise en forme fermé (23, 26). - Procédé conforme à la revendication 1 ou 2,
caractérisé en ce que
lors de la mise en forme il se produit le long d'une ligne de contour (34) au moins par segments une courbure avec un faible rayon de courbure. - Procédé conforme à la revendication 2 ou 3,
caractérisé en ce que
lors de la mise en forme, le matériau en tôle s'applique successivement et/ou par segments contre le contour d'outil de mise en forme fermé (23, 26) d'au moins une partie d'outil (22, 25), et, ensuite, un mouvement relatif entre le matériau en tôle en appui et la partie d'outil (22, 25) est largement évité. - Procédé conforme à l'une quelconque des revendications précédentes,
caractérisé en ce que
à la fin de la mise en forme on effectue un processus de moulage lors duquel en particulier au moins une ligne de contour (34) est finalement formée. - Procédé conforme à la revendication 5,
caractérisé en ce que
au moins une surface de forme libre (32) est équipée lors du processus de moulage, au moins par segments, d'au moins une structuration augmentant la rigidité. - Procédé conforme à l'une des revendications précédentes,
caractérisé en ce que
le positionnement de la platine de départ (10) dans l'outil de mise en forme (20) s'effectue au moyen d'au moins un dispositif d'arrêt. - Procédé conforme à l'une des revendications précédentes,
caractérisé en ce que
des ouvertures dans la pièce préformée en tôle sont formées par des ouvertures prépercées (12, 14) situées dans la platine de départ (10). - Procédé conforme à l'une des revendications précédentes,
caractérisé en ce que
la formation finale d'au moins une ligne de contour (34) ou d'un biseau est effectuée au moyen d'une partie d'outil mobile séparée (29a) du même outil de mise en forme (20a). - Pièce préformée en tôle complexe (30) obtenue par la mise en oeuvre du procédé conforme à l'une quelconque des revendications précédentes,
caractérisée en ce que
cette pièce comprend au moins deux surfaces de forme libre (32) qui sont délimitées l'une par rapport à l'autre au moins par segments par au moins une ligne de contour (34),
les surfaces de forme libre (32) comportent sur la totalité de leur extension une modification de forme relativement faible, et la rigidité de la pièce préformée en tôle (30) résulte pour une partie importante de la présence de la ligne de contour (34). - Pièce préformée en tôle complexe (30) conforme à la revendication 10,
caractérisée en ce qu'
elle comporte dans la zone d'au moins une ligne de contour (34) au moins par segments une modification de forme en hauteur locale. - Utilisation d'une pièce préformée en tôle complexe (30) conforme à l'une des revendications 10 et 11,
en tant qu'élément de carrosserie dans un véhicule.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102009005261A DE102009005261A1 (de) | 2009-01-20 | 2009-01-20 | Verfahren zur Herstellung eines komplexen Blechformteils |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP2208551A2 EP2208551A2 (fr) | 2010-07-21 |
| EP2208551A3 EP2208551A3 (fr) | 2013-07-31 |
| EP2208551B1 true EP2208551B1 (fr) | 2016-04-06 |
Family
ID=42144900
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP09015648.0A Active EP2208551B1 (fr) | 2009-01-20 | 2009-12-17 | Procédé de fabrication d'une pièce de tôle préformée complexe |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2208551B1 (fr) |
| DE (1) | DE102009005261A1 (fr) |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102343405A (zh) * | 2011-06-28 | 2012-02-08 | 天津汽车模具股份有限公司 | 一种用于汽车外板覆盖件冲压的定位方法 |
| GB201217221D0 (en) | 2012-09-26 | 2012-11-07 | Jaguar Cars | Panel bending method |
| DE102013011951A1 (de) * | 2013-07-18 | 2015-01-22 | GM Global Technology Operations LLC (n. d. Ges. d. Staates Delaware) | Verfahren zum Fertigen von Kraftfahrzeug-Karosserieteilen |
| RU2732552C2 (ru) * | 2015-05-05 | 2020-09-21 | Пса Отомобиль Са | Упрощенный способ изготовления детали, деталь, полученная при помощи такого способа изготовления, и способ выбора между упрощенным и не упрощенным способом изготовления |
| FR3050666B1 (fr) * | 2016-05-02 | 2018-10-19 | Peugeot Citroen Automobiles Sa | Procede de realisation simplifie d’une piece, piece obtenue par un tel procede de realisation et procede de selection entre un procede de realisation simplifie ou non simplifie |
| FR3035805B1 (fr) * | 2015-05-05 | 2017-12-01 | Peugeot Citroen Automobiles Sa | Procede de realisation d’une piece comportant une etape de formage et piece de structure de vehicule formee par un tel procede |
| FR3036299B1 (fr) * | 2015-05-18 | 2017-05-19 | Peugeot Citroen Automobiles Sa | Mise a forme d’embouti semi-ouvert |
| CN114603060A (zh) * | 2022-02-17 | 2022-06-10 | 四川国腾设备制造有限公司 | 一种飞机发动机机罩的生产方法 |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4212188A (en) | 1979-01-18 | 1980-07-15 | The Boeing Company | Apparatus for forming sheet metal |
| JP3398240B2 (ja) * | 1994-12-21 | 2003-04-21 | ダイハツ工業株式会社 | 板金のプレス方法 |
| DE19524235A1 (de) * | 1995-07-04 | 1997-01-16 | Volkswagen Ag | Verfahren zur Herstellung eines Formteils |
| JP4550249B2 (ja) * | 2000-09-28 | 2010-09-22 | 本田技研工業株式会社 | 車体パネルの製造方法 |
| JP2002102947A (ja) * | 2000-09-28 | 2002-04-09 | Honda Motor Co Ltd | 車体パネルの成形方法 |
| DE10065142A1 (de) | 2000-12-23 | 2002-07-04 | Simone Rubbert | Verfahren zur Verformung von flachen Körpern in unregelmäßig, mehrdimensional gekrümmte Gegenstände |
| SE530228C2 (sv) * | 2006-08-25 | 2008-04-01 | Gestamp Hardtech Ab | Sätt att varmforma och härda en plåtdetalj, samt en B-stolpe till ett fordon |
| GB2444574B (en) | 2007-06-13 | 2008-11-12 | Gregory Epps | Bending sheet material |
-
2009
- 2009-01-20 DE DE102009005261A patent/DE102009005261A1/de not_active Withdrawn
- 2009-12-17 EP EP09015648.0A patent/EP2208551B1/fr active Active
Also Published As
| Publication number | Publication date |
|---|---|
| EP2208551A3 (fr) | 2013-07-31 |
| EP2208551A2 (fr) | 2010-07-21 |
| DE102009005261A1 (de) | 2010-07-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2512702B1 (fr) | Procédé et dispositif de fabrication d'un élément en demi-coque | |
| EP0707535B1 (fr) | Procede et dispositif utilises pour realiser une piece | |
| DE102011115219B4 (de) | Verfahren und Vorrichtung zur Herstellung eines Blechformteils unter Vermeidung von Nachlaufkanten | |
| EP2208551A2 (fr) | Procédé de fabrication d'une pièce de tôle préformée complexe | |
| EP3401032B1 (fr) | Outil composite et procédé de fabrication d'un élément en tôle | |
| EP2108467B1 (fr) | Procédé de fabrication de demi-coques de dimensions très précises | |
| EP0288705A2 (fr) | Procédé de fabrication de pièces compliquées en tôle et dispositif pour réaliser le procédé | |
| EP1097758B1 (fr) | Méthode de formage d' une large tôle, en particulier une partie de carrosserie d'un véhicule | |
| DE102013019634A1 (de) | Herstellung eines Blechformteils mit lokalem elektromagnetischen Umformen des Blechmaterials zur Erzeugung einer Blechformteilkante | |
| DE19842750B4 (de) | Verfahren und Herstellung von tiefgezogenen Hohlteilen und Ziehwerkzeug | |
| DE10215912C1 (de) | Verfahren und Prägewerkzeug zur Herstellung eines Karosserie-Bauteils aus einem wölbstrukturierten Blech | |
| DE102007056358A1 (de) | Umformwerkzeug sowie Verfahren zur Herstellung eines solchen Umformwerkzeugs | |
| DE69909485T2 (de) | Vorrichtung und verfahren zum formen von flachen gegenständen | |
| EP1029611B1 (fr) | Dispositif pour la fabrication de produits creux courbes contre-dépouillés par hydroformage | |
| DE102013011951A1 (de) | Verfahren zum Fertigen von Kraftfahrzeug-Karosserieteilen | |
| DE102006025522B4 (de) | Verfahren und Vorrichtung zur Herstellung strukturierter, geschlossener Hohlprofile | |
| EP2490835A1 (fr) | Procédé et dispositif pour façonner des pièces planes | |
| DE102004054120B4 (de) | Verfahren zum Umformen einer großflächigen Blechplatine zu einem Formteil, wie einem Außenhautteil einer Kraftfahrzeugkarosserie | |
| EP0339060B1 (fr) | Outil de moulage par compression pour la fabrication de plaques moulees a couches multiples | |
| DE10016803B4 (de) | Verfahren zum Herstellen von Bauteilen | |
| EP3478426B1 (fr) | Procédé de fabrication de baguettes enjoliveuses et baguettes enjoliveuses fabriquées en utilisant le procédé | |
| DE102004058013B3 (de) | Verfahren zum Herstellen einer Tragwerkstruktur mit einem integral prolfilartigen Versteifungselement für ein Flugzeug | |
| WO2012045292A1 (fr) | Procédé et dispositif d'emboutissage de tôles | |
| DE102020202004A1 (de) | Verfahren zum Herstellen von umgeformten Blechteilen und Vorrichtung | |
| DE10120880B4 (de) | Verfahren zur Herstellung von Tiefziehteilen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA RS |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA RS |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B21D 22/02 20060101AFI20130624BHEP Ipc: B21D 53/88 20060101ALI20130624BHEP Ipc: B62D 25/00 20060101ALI20130624BHEP |
|
| 17P | Request for examination filed |
Effective date: 20140121 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: BAYERISCHE MOTOREN WERKE AKTIENGESELLSCHAFT |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B21D 53/88 20060101ALI20151103BHEP Ipc: B21D 22/02 20060101AFI20151103BHEP Ipc: B62D 25/00 20060101ALI20151103BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20151124 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 787178 Country of ref document: AT Kind code of ref document: T Effective date: 20160415 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502009012372 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D Ref country code: NL Ref legal event code: MP Effective date: 20160406 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160806 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160706 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160707 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160808 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502009012372 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| 26N | No opposition filed |
Effective date: 20170110 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161217 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161217 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20161231 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 787178 Country of ref document: AT Kind code of ref document: T Effective date: 20161217 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20091217 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161217 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160406 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230502 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20241209 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20241218 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20241218 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20241216 Year of fee payment: 16 |