EP3055476B1 - Profilé composite, bande de renforcement pour profilé composite et procédé permettant de produire un profilé composite - Google Patents
Profilé composite, bande de renforcement pour profilé composite et procédé permettant de produire un profilé composite Download PDFInfo
- Publication number
- EP3055476B1 EP3055476B1 EP14799352.1A EP14799352A EP3055476B1 EP 3055476 B1 EP3055476 B1 EP 3055476B1 EP 14799352 A EP14799352 A EP 14799352A EP 3055476 B1 EP3055476 B1 EP 3055476B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- composite profile
- reinforcement
- reinforcement strips
- profile
- composite
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- E—FIXED CONSTRUCTIONS
- E06—DOORS, WINDOWS, SHUTTERS, OR ROLLER BLINDS IN GENERAL; LADDERS
- E06B—FIXED OR MOVABLE CLOSURES FOR OPENINGS IN BUILDINGS, VEHICLES, FENCES OR LIKE ENCLOSURES IN GENERAL, e.g. DOORS, WINDOWS, BLINDS, GATES
- E06B3/00—Window sashes, door leaves, or like elements for closing wall or like openings; Layout of fixed or moving closures, e.g. windows in wall or like openings; Features of rigidly-mounted outer frames relating to the mounting of wing frames
- E06B3/04—Wing frames not characterised by the manner of movement
- E06B3/06—Single frames
- E06B3/08—Constructions depending on the use of specified materials
- E06B3/20—Constructions depending on the use of specified materials of plastics
- E06B3/22—Hollow frames
- E06B3/221—Hollow frames with the frame member having local reinforcements in some parts of its cross-section or with a filled cavity
Definitions
- the invention relates to a composite profile with the features of claim 1 and a method for producing a composite profile with the features of claim 11.
- Extruded plastic profiles are widely used today in the area of windows, doors or other components. In the case of larger components in particular, the plastic profiles have a considerable length, so that in particular the dimensional stability is of great importance.
- the profiles that form the frame and the sash are stressed primarily by the weight of the insulating glass panes and by the wind pressure. These forces are transferred into the building structure via the profiles.
- the profiles must not deform too much, with the deflection in particular being viewed critically. In order to keep this deflection low, a minimum bending stiffness of the profiles depending on the window size is required. Since the beginning of the use of plastic windows, the plastic profiles have been reinforced by inserting so-called U-reinforcing bars.
- an extruded plastic hollow profile strip for window frames is known in which a reinforcing element made of synthetic resin-bonded reinforcing fibers is arranged in at least one profile wall and can be angled during extrusion of the plastic hollow profile.
- At least two reinforcement tapes are arranged inside the composite profile.
- the at least two reinforcing tapes are at least partially formed from thermoplastic with embedded endless glass and / or mineral fibers and / or other reinforcing fibers.
- At least one of the reinforcing tapes has at least one section that is angled parallel to the longitudinal axis of the composite profile. Furthermore, the distance between the at least two reinforcement bands and the inside of the respectively adjacent outer wall of the composite profile in the region of the non-angled section corresponds to 0.1 to 3 times the wall thickness of the outer wall.
- Such a composite profile has a combination of features that together result in a dimensionally stable composite profile.
- the choice of the distance ensures that the reinforcement strips are not too close to the surface, but also not too far inside the composite profile.
- the angle between the at least one angled section and the non-angled section of the at least two reinforcing bands is more than 10 ° and less than 150 °, in particular between 20 ° and 90 °.
- the bend in the reinforcement band increases the bending stiffness of the band itself.
- the distance between the at least two reinforcing bands and the inside of the respectively assigned outer wall of the composite profile is between 0.1 and 10 mm, in particular between 0.5 and 3 mm. This dimension ensures that the reinforcement tapes are not too close below the outer surface of the composite profile, which experience has shown could impair the surface quality.
- the upper limit of the distance also prevents the reinforcing strips from being too close to the center of gravity axis line of the composite profile. The greater the distance of the stiffening bands from the center of gravity axis line, the greater the section modulus of the entire composite profile.
- At least one of the at least two reinforcement tapes has a proportion of 30 to 70 vol.% Glass fibers and / or mineral fibers and / or other reinforcement fibers, embedded in a thermoplastic matrix, in particular in PET .
- this matrix softens, so that the reinforcing fibers can dodge laterally when the weld seam is formed and the associated shortening in the area of the end faces, and can also penetrate into one another at the end, so that the reinforcing strips themselves also weld to a certain extent.
- At least one spacer is provided to produce the defined distance between the at least two reinforcing bands and the inside of the composite profile. This applies in particular if at least one spacer is arranged in the longitudinal direction of the composite profile on one of the at least two reinforcement bands, in particular in one piece on the reinforcement band and / or is formed from plastic of the composite profile, in particular as a web and is arranged on the wall of the composite profile and / or as separate part is formed. There are therefore several options for arranging spacers between the reinforcing strips and the composite profile.
- a profile in particular a linear profile and / or a knurling, is provided on at least one edge on each of the at least two reinforcing strips to create a frictional and / or positive connection with the Extrusion plastic profile is arranged.
- the shear forces that occur when the composite profile is curved can thus be transmitted efficiently.
- connection between the reinforcement strips and the plastic of the composite profile can additionally or alternatively be improved if the at least two reinforcement strips have a connection layer on the surface for producing a material connection to the extrusion plastic profile by welding.
- the connection layer can have a proportion of PVC.
- At least one bend and / or profiling of an edge takes place by thermal deformation on at least one of the at least two reinforcement bands inline during the extrusion process prior to insertion into an extrusion nozzle, at least one of the at least two reinforcement bands being arranged in the composite profile in such a way that the distance between the at least two reinforcement bands and the inside of the respectively adjacent outer wall of the composite profile in the region of the non-angled section corresponds to 0.1 to 3 times the wall thickness of the outer wall.
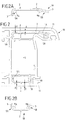
- a first embodiment of a composite profile 10 made of plastic is shown.
- This composite profile 10 which is designed as a hollow profile, is produced by extrusion in a manner known per se, some special features of the manufacturing process for some embodiments being shown below.
- Such a composite profile 10 is used, for example, to enclose an insulating glass pane 15 as a frame.
- the composite profile 10 has two reinforcement bands 1A, 1B, which are shown in FIGS 1A and 1B are shown separately.
- the reinforcing tapes 1A, 1B are formed at least partially, but in particular completely, from a thermoplastic with embedded endless glass and / or mineral fibers and / or other reinforcing fibers.
- the reinforcing tapes 1A, 1B can have a proportion of 30 to 70% by volume of reinforcing fibers embedded in a thermoplastic matrix, in particular in PET.
- Such reinforcing tapes 1A, 1B have a high mechanical strength with low weight, which is particularly advantageous compared to metallic reinforcements. In alternative embodiments, more than two reinforcement bands 1A, 1B can also be used.
- the reinforcing strips 1A, 1B have angled sections 5A, 5B and a non-angled section which, when assembled, is arranged essentially parallel to an outer wall 11 of the composite profile 10.
- a second angled section 5B is arranged on the opposite edge of the first reinforcing band 1A. This forms an angle ⁇ B of approximately 170 ° with the non-angled section of the first reinforcement band 1A.
- the angled sections 5A, 5B are of different sizes in this embodiment.
- the angles ⁇ A , ⁇ B can be more than 10 ° and less than 150 °, these angles, as in Fig. 1 shown, are measured on the side facing away from the outer wall 11.
- reinforcement tapes 1A, 1B are shown, each having two angled sections 5A, 5B. In alternative embodiments, there may be only one angled section or more than two angled sections.
- the reinforcement bands 1A, 1B are arranged at a relatively small distance A from the outer walls 11 of the composite profile 10.
- the distance A is between 0.1 and 3 times the respectively adjacent outer wall 11.
- the distance A is determined between the inside of the outer wall 11 and the non-angled section of the reinforcing tape 1A, 1B. This non-angled section of the reinforcement band 1A, 1B lies essentially parallel to the inside of the outer wall 11.
- the distance A between the at least two reinforcement bands 1A, 1B and the inside of the outer wall 11 of the composite profile 10 is between 0.2 and 10 mm, in particular between 0.5 and 3 mm.
- the spacing A selected in this way ensures that the flatness of the outer wall 11 is not impaired by the reinforcement band and, likewise, the reinforcement band 1A, 1B is not too far inside the composite profile 10.
- the reinforcement bands 1A, 1B have the greatest effect if they are positioned as far as possible from the center of gravity axis line S of the composite profile 10. The aim is therefore to attach the reinforcement tapes 1A, 1B as far as possible outside, that is, in the case of a window profile, far away from the glass plane.
- the extrusion process in the composite profile 10 creates considerable internal stresses due to the different changes in length during cooling.
- the reinforcement tapes 1A, 1B are subjected to pressure, the plastic (eg PVC) of the composite profile 10 under tension.
- the entire composite profile 10 is straight when the internal tensions cancel each other out or compensate.
- the internal stresses on a cutting surface are forced to zero, which leads to deformations.
- a window profile that has considerable asymmetries, this leads to a "tilting" of the rollover inwards (ie in the direction of the glass plane of the insulating glass 15) in the range up to approximately 1 mm, which can lead to a malfunction after the corners are welded together to form a window frame.
- the angled reinforcement profiles 1A, 1B themselves have a higher rigidity, which acts against tipping, and on the other hand, the angled sections 5A, 5B are positioned more centrally on the central plane of the rollover area, so that the tensile stresses in the PVC are also present in this partial area of the composite profile 10 behave approximately symmetrically after the separation process.
- the two reinforcing bands 1A, 1B each have spacers 2 on the sides which are oriented toward the outer sides 11 of the composite profile 10. These ensure that the distance A between the reinforcing tape 1A, 1B and the inside of the outer wall 11 is maintained in a defined manner.
- the outer wall of the composite profile 10 has short webs as spacers 2, which prevent the reinforcing profile 1A, 1B from abutting the outer wall over a large area and that a distance A is maintained in a defined manner.
- the spacers 2 are made here in one piece with the plastic of the composite profile 10.
- the spacers 2 prevent direct contact with the visible surface (i.e. the visible surface of a window profile, essentially parallel to the glass surface, i.e. in the installed state of a window on the room side or on the facade side); or at least largely avoided.
- this visible surface would have slight waves, which are visually disturbing and, particularly when viewed at a flat angle, cause strongly distorted mirror images. This prevents unevenness of the reinforcement bands 1A, 1B from becoming apparent.
- minimal fluctuations in the thickness of the outer wall of the composite profile 10 could not be displaced inwards because the surface of the reinforcing profile would have a dominant effect in the event of direct contact.
- the spacers 2 can additionally or alternatively also be arranged on the reinforcement band 1A, 1B (see Fig. 2 ).
- the spacers 2 can each be applied in one piece to the reinforcing strips 1A, 1B or, for example, by extrusion. It is also possible that the Spacers 2 are arranged as a separate part between the reinforcing bands 1A, 1B and the plastic of the composite profile 10.
- Profiles 3 are arranged on the edges of the reinforcing strips 1A, 1B in order to enable the reinforcing strips 1A, 1B to have a shear-resistant fit in the plastic part of the composite profile 10.
- the profiles can also be arranged on only one edge of the reinforcing strips 1A, 1B.
- the profiling 3 can e.g. be designed as knurling and / or as a line structure.
- the profiling 3 can be introduced in the course of the assembly process of the reinforcement tape, for example by embossing in connection with heating and / or milling or pressing takes place in the cold state.
- a frictional and / or positive connection between the reinforcement bands 1A, 1B and the plastic profile can thus be achieved.
- connection of the reinforcement bands 1A, 1B to the plastic part of the composite profile 10 can be increased if at least part of the surface of at least one of the reinforcement bands 1A, 1B has a connecting layer with which a material connection to the plastic part of the composite profile 10 can be produced. This can e.g. by a targeted application of a PVC layer to one of the reinforcement tapes 1A, 1B.
- FIG. 3 A semifinished product 6 is shown, which can serve as the starting product for reinforcing tapes 1A, 1B with molded connection layer 5.
- This semifinished product essentially has continuous glass fibers which are embedded in a thermoplastic matrix, the width of this semifinished product being significantly greater than the width of an individual reinforcing band 1A, 1B, for example 500 mm.
- a thin connecting layer 5 is made from a plastic in an inline process on both outer surfaces, which has a high bond strength both with the matrix of the composite material and with the plastic of the composite profile 10 and with the latter is weldable, for example made of PVC.
- connection layer 5 can also form the spacers 2. The required widths for the individual reinforcement bands 1A, 1B are then separated from this semifinished product 6 and these are then fed to the further assembly process.
- FIG. 2A and 2B A second embodiment of a composite profile is shown, which essentially corresponds to the first embodiment, so that reference can be made to the above description.
- the reinforcement bands 1A, 1B themselves have the spacers 2, which are integrally formed on the reinforcement band.
- At least one of the reinforcing tapes 1A, 1B e.g. can be unwound from a roll, the bending of the at least one section 5A, 5B and / or the profiling 3 of the edge region taking place inline during the extrusion process of the composite profile 10.
- the raw material for the reinforcement tapes 1A, 1B is e.g. unrolled from a roll and it passes through a heating tunnel.
- the profiling 3 is then applied in the edge regions 3 of the reinforcement band 1A, 1B and the angled section 5A, 5B is bent.
- the reinforcing band 5A, 5B which is still largely hot, is then fed to the extrusion die and then extrusion-coated with the plastic profile of the composite profile 10.
- the flat raw material for the reinforcement tapes 1A, 1B can be on rolls stored wound up and transported to customers. Forming can then be carried out on site, as described above. In the case of reinforcing tapes which are already angled (ie folded), a relatively large winding radius is required, which is also manageable. This means that suitable reinforcing tapes with the required contour and edge shape can also be produced in a separate manufacturing or assembly process, regardless of the extrusion process of the composite profile.
Landscapes
- Engineering & Computer Science (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
- Laminated Bodies (AREA)
Claims (11)
- Profilé composite en matière synthétique, conçu comme un profilé creux pourvu d'au moins deux bandes de renforcement disposées à l'intérieur,
les au moins deux bandes de renforcement (1A, 1B) étant au moins partiellement formées à partir de matière thermoplastique dans laquelle sont incorporées des fibres de verre et/ou minérales sans fin et/ou d'autres fibres de renforcement et au moins une des bandes de renforcement (1A, 1B) comportant au moins une portion coudée (5A, 5B) parallèle à l'axe longitudinal du profilé composite (10),
caractérisé en ce que
la distance (A) entre les au moins deux bandes de renforcement (1A, 1B) et le côté intérieur de la paroi extérieure (11) respectivement adjacente du profilé composite (10) dans la région de la portion noncoudée est de 0,1 à 3 fois l'épaisseur de paroi (D) de la paroi extérieure (11). - Profilé composite selon la revendication 1, caractérisé en ce que l'angle (αA, αB) compris entre l'au moins une portion coudée (5A, 5B) et la portion noncoudée des au moins deux bandes de renforcement (1A, 1B) est de plus de 10° et de moins de 150°, notamment est compris entre 20° et 90°.
- Profilé composite selon la revendication 1 ou 2, caractérisé en ce que la distance (A) entre les au moins deux bandes de renforcement (1A, 1B) et le côté intérieur de la paroi extérieure (11) respectivement associée du profilé composite (10) est comprise entre 0,1 et 10 mm, en particulier entre 0,5 et 3 mm.
- Profilé composite selon l'une au moins des revendications précédentes, caractérisé en ce que l'une au moins des au moins deux bandes de renforcement (1A, 1B) comporte un pourcentage allant de 30 à 70 % en volume de fibres de verre et/ou de fibres minérales et/ou d'autres fibres de renforcement, incorporées dans une matrice thermoplastique, en particulier en PET.
- Profilé composite selon l'une au moins des revendications précédentes, caractérisé par au moins un élément d'espacement (2) destiné à établir la distance définie (A) entre les au moins deux bandes de renforcement (1A, 1B) et le côté intérieur du profilé composite (10).
- Profilé composite selon la revendication 5, caractérisé en ce qu'au moins un élément d'espacement (2) est disposé sur l'une des au moins deux bandes de renforcement (1A, 1B) dans la direction longitudinale du profilé composite (10), notamment est formé d'une seule pièce sur la bande de renforcement (1A, 1B) et/ou sur le profilé en matière synthétique du profilé composite (10), en particulier sous la forme d'une nervure, est disposé sur la paroi du profil composite (10) et/ou est conçu comme une pièce séparée.
- Profilé composite selon l'une au moins des revendications précédentes, caractérisé en ce que sur au moins un bord de chacune des au moins deux bandes de renforcement (1A, 1B) un profilage (3), notamment un profilage linéaire et/ou un moletage pour créer une liaison à friction et/ou à complémentarité de formes avec le profilé en matière synthétique d'extrusion (10) est disposé.
- Profilé composite selon l'une au moins des revendications précédentes, caractérisé en ce que les au moins deux bandes de renforcement (1A, 1B) comportent sur la surface une couche de liaison (4) destinée à créer une liaison de matière avec le profilé en matière synthétique d'extrusion (10) par soudage.
- Profilé composite selon la revendication 8, caractérisé en ce que la couche de liaison (4) comporte un pourcentage de PVC.
- Profilé composite selon l'une au moins des revendications précédentes, caractérisé en ce que les au moins deux bandes de renforcement (1A, 1B) sont disposées de façon à augmenter le couple de résistance dans la région extérieure du profilé de matière synthétique (10), notamment à une distance du centre de gravité de la ligne axiale (S) de plus de 0,7 fois la distance (H) du bord extérieur à la ligne axiale barycentrique (S).
- Procédé de fabrication d'un profilé composite selon l'une au moins des revendications 1 à 10,
caractérisé en ce que
au moins un coude et/ou un profilage (3) d'un bord de l'une au moins des au moins deux bandes de renforcement (1A, 1B) est réalisé en ligne avec un procédé d'extrusion ou au moins un coude et/ou un profilage sur l'une au moins des au moins deux bandes de renforcement (1A, 1B) avant l'insertion dans une buse d'extrusion, cela étant dû à une déformation thermique, l'une au moins des au moins deux bandes de renforcement (1A, 1B) étant disposée dans le profilé composite de telle sorte que la distance (A) entre les au moins deux bandes de renforcement (1A, 1B) et le côté intérieur de la paroi extérieure (11) respectivement adjacente du profilé composite (10) dans la région de la portion noncoudée soit de 0,1 à 3 fois l'épaisseur de paroi (D) de la paroi extérieure (11).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL14799352T PL3055476T3 (pl) | 2013-10-07 | 2014-10-06 | Profil łączony, taśma wzmacniająca dla profilu łączonego, sposób do wytwarzania profilu łączonego |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102013220211.3A DE102013220211A1 (de) | 2013-10-07 | 2013-10-07 | Verbundprofil, Verstärkungsband für ein Verbundprofil und ein Verfahren zurHerstellung eines Verbundprofils |
| PCT/EP2014/071339 WO2015052130A1 (fr) | 2013-10-07 | 2014-10-06 | Profilé composite, bande de renforcement pour profilé composite et procédé permettant de produire un profilé composite |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3055476A1 EP3055476A1 (fr) | 2016-08-17 |
| EP3055476B1 true EP3055476B1 (fr) | 2020-06-24 |
Family
ID=51903874
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP14799352.1A Active EP3055476B1 (fr) | 2013-10-07 | 2014-10-06 | Profilé composite, bande de renforcement pour profilé composite et procédé permettant de produire un profilé composite |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP3055476B1 (fr) |
| CN (1) | CN105637163A (fr) |
| DE (1) | DE102013220211A1 (fr) |
| EA (1) | EA032396B1 (fr) |
| ES (1) | ES2814999T3 (fr) |
| PL (1) | PL3055476T3 (fr) |
| WO (1) | WO2015052130A1 (fr) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3558620A1 (fr) * | 2016-12-23 | 2019-10-30 | LANXESS Deutschland GmbH | Technologie de composites profilés creux |
| DE202017107427U1 (de) | 2017-12-06 | 2019-03-07 | Rehau Ag + Co | Hohlkammerprofil, insbesondere Fenster- oder Türprofil |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3136863A1 (de) * | 1981-04-15 | 1982-11-04 | Schock & Co Gmbh, 7060 Schorndorf | Extrudierte kunststoff-hohlprofilleiste fuer fensterrahmen, aus derartigen profilleisten hergestellter fensterrahmen und verfahren zur herstellung eines solchen fensterrahmens |
| DE29912375U1 (de) * | 1999-07-15 | 1999-09-09 | SCHÜCO International KG., 33609 Bielefeld | Kunststoffhohlprofil mit eingelagerten Bändern oder Streifen aus faserverstärktem Kunststoff, vorzugsweise Rahmenprofil für Fenster oder Türen |
| DE19933099A1 (de) | 1999-07-15 | 2001-01-18 | Schueco Int Kg | Kunststoffhohlprofil mit eingelagerter Metallverstärkung, vorzugsweise Rahmenprofil für Fenster oder Türen |
| EP1196677B2 (fr) * | 1999-07-15 | 2010-08-11 | SCHÜCO International GmbH & Co. | Profile creux en matiere plastique |
| DE102007015318A1 (de) | 2007-03-30 | 2008-10-02 | Rehau Ag + Co. | Verfahren zur Herstellung von verstärkten thermoplastischen Kunststoffcomposites und zugehörige Vorrichtung zur Durchführung, sowie derart hergestellte Composites |
| DE102007039009A1 (de) * | 2007-08-17 | 2009-02-19 | Rehau Ag + Co | Rahmen-Baugruppe sowie Kunststoff-Profilrahmen hierfür |
| DE102008008343A1 (de) * | 2008-02-08 | 2009-08-13 | Aluplast Gmbh | Profil für Fenster- oder Türrahmen |
| CN202249430U (zh) * | 2011-08-18 | 2012-05-30 | 芜湖海螺型材科技股份有限公司 | 一种隐形扇窗结构 |
| CN203201394U (zh) * | 2013-04-11 | 2013-09-18 | 浙江瑞明节能门窗股份有限公司 | 一种多腔体型材塑钢门窗 |
-
2013
- 2013-10-07 DE DE102013220211.3A patent/DE102013220211A1/de not_active Ceased
-
2014
- 2014-10-06 EP EP14799352.1A patent/EP3055476B1/fr active Active
- 2014-10-06 WO PCT/EP2014/071339 patent/WO2015052130A1/fr not_active Ceased
- 2014-10-06 EA EA201690694A patent/EA032396B1/ru not_active IP Right Cessation
- 2014-10-06 ES ES14799352T patent/ES2814999T3/es active Active
- 2014-10-06 PL PL14799352T patent/PL3055476T3/pl unknown
- 2014-10-06 CN CN201480055366.7A patent/CN105637163A/zh active Pending
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| EA032396B1 (ru) | 2019-05-31 |
| EA201690694A1 (ru) | 2016-07-29 |
| CN105637163A (zh) | 2016-06-01 |
| PL3055476T3 (pl) | 2021-01-11 |
| ES2814999T3 (es) | 2021-03-29 |
| DE102013220211A1 (de) | 2015-04-09 |
| WO2015052130A1 (fr) | 2015-04-16 |
| EP3055476A1 (fr) | 2016-08-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69703252T2 (de) | Verfahren zur Herstellung eines isolierenden Abstandhalters zum Erzeugen einer wärmedämmenden Brücke | |
| EP2870313B1 (fr) | Entretoise destinée à des vitrages isolants | |
| EP3140485B1 (fr) | Profilé composite pour portes, fenêtres ou éléments de façade | |
| EP0153758A2 (fr) | Barre composée, en particulier pour châssis de fenêtre, châssis de porte et volets à rouleau | |
| EP2476853B1 (fr) | Profil composite pour fenêtres, portes et façades et son procédé de fabrication | |
| EP2236720A1 (fr) | Elément de profilé pour fenêtres ou portes | |
| DE102012101668A1 (de) | Verfahren zur Erstellung eines Hohlkammerprofils | |
| EP2527580A1 (fr) | Insert d'isolation pour un cadre formé de profilés | |
| EP2576949B1 (fr) | Profile a rupture de pont thermique | |
| EP2163719B1 (fr) | Profilé composite et procédé de fabrication d'un profilé composite | |
| EP2582901B1 (fr) | Profilé composite et procédé de production d'un élément de renforcement pour le profilé composite | |
| DE102011117170B4 (de) | Wärmegedämmtes Profil | |
| DE102015007611A1 (de) | Isolierelement | |
| WO2015052130A1 (fr) | Profilé composite, bande de renforcement pour profilé composite et procédé permettant de produire un profilé composite | |
| EP3015635B1 (fr) | Profile composite pour des portes, fenetres ou elements de façade | |
| EP0684352A1 (fr) | Plaque multicouche entretoisée en matière thermoplastique | |
| DE2622905B2 (de) | Rolladenstab | |
| DE20121281U1 (de) | Bauelement und Verwendung eines Trägers | |
| EP3219895B1 (fr) | Système de porte coulissante et vantail coulissant d'un système de porte coulissant | |
| EP0721041A1 (fr) | Armature profilée pour espagnolette ainsi que le demi-produit et sa fabrication | |
| DE102008064784B3 (de) | Verbundprofil | |
| EP3048232B1 (fr) | Profilé métallique, profilé composite avec un tel profilé métallique ainsi que procédé de fabrication du profilé métallique | |
| DE102011122924B4 (de) | Isoliersteg und wärmegedämmtes Profil | |
| DE102009036925A1 (de) | Verfahren zur Herstellung einer Gewebeprofilleiste | |
| EP4585783A1 (fr) | Procédé de fabrication d'un profilé composite et profilé composite |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20160504 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20200115 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502014014371 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1284062 Country of ref document: AT Kind code of ref document: T Effective date: 20200715 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200924 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200925 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200924 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20200624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201026 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20201024 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502014014371 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2814999 Country of ref document: ES Kind code of ref document: T3 Effective date: 20210329 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| 26N | No opposition filed |
Effective date: 20210325 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201006 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201006 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200624 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R081 Ref document number: 502014014371 Country of ref document: DE Owner name: EXELLIQ AUSTRIA GMBH, AT Free format text: FORMER OWNER: GREINER TOOL. TEC GMBH, NUSSBACH, AT |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: PD Owner name: EXELLIQ AUSTRIA GMBH; AT Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT; FORMER OWNER NAME: EXELLIQ HOLDING GMBH Effective date: 20240111 Ref country code: BE Ref legal event code: HC Owner name: EXELLIQ HOLDING GMBH; AT Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CHANGE OF OWNER(S) NAME; FORMER OWNER NAME: GREINER TOOL.TEC GMBH Effective date: 20240111 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20240201 AND 20240207 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 1284062 Country of ref document: AT Kind code of ref document: T Owner name: EXELLIQ AUSTRIA GMBH, AT Effective date: 20240603 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: EXELLIQ AUSTRIA GMBH Effective date: 20241112 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20250822 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250918 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20251024 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20251021 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251031 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20251029 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20251022 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20251114 Year of fee payment: 12 |