EP4015681A1 - Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil - Google Patents
Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil Download PDFInfo
- Publication number
- EP4015681A1 EP4015681A1 EP20215332.6A EP20215332A EP4015681A1 EP 4015681 A1 EP4015681 A1 EP 4015681A1 EP 20215332 A EP20215332 A EP 20215332A EP 4015681 A1 EP4015681 A1 EP 4015681A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cleaning
- yarn
- forming element
- spinning
- air
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H1/00—Spinning or twisting machines in which the product is wound-up continuously
- D01H1/11—Spinning by false-twisting
- D01H1/115—Spinning by false-twisting using pneumatic means
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H4/00—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques
- D01H4/02—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques imparting twist by a fluid, e.g. air vortex
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H11/00—Arrangements for confining or removing dust, fly or the like
- D01H11/005—Arrangements for confining or removing dust, fly or the like with blowing and/or suction devices
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H11/00—Arrangements for confining or removing dust, fly or the like
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H2700/00—Spinning or twisting machines; Drafting devices
- D01H2700/21—Piecing or cleaning in spinning mules
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H4/00—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques
- D01H4/04—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques imparting twist by contact of fibres with a running surface
- D01H4/22—Cleaning of running surfaces
Definitions
- the invention relates to a spinning position of an air-jet spinning machine and a method for cleaning a yarn-forming element of an air-jet spinning nozzle.
- a drafting sliver is drawn in a defined manner according to the yarn count to be achieved by means of a multi-roller drafting system and then fed to an air spinning nozzle.
- the outer fibers of the sliver are wound around an internal fiber core by means of a turbulent air flow generated by air nozzles in the area of an inlet opening of a yarn-forming element of the air spinning nozzle, resulting in an air-yarn-specific yarn structure of a parallel yarn core and twisted fibers lying at a certain angle, whereby the wrapping fibers are crucial for the desired strength of the yarn.
- the air spinning process can be carried out with fibers made of different materials, whereby both natural fibers, such as cotton and/or animal wool, and synthetic fibers, such as polyester, and mixtures of natural and synthetic fibers can be used.
- synthetic fibers such as polyester
- polymer residues, polyester fiber fragments and/or finishing agents are often deposited on a surface of a spinning cone of the yarn-forming element.
- deposits significantly disrupt the air-jet spinning process and significantly reduce the spinning result and thus the yarn quality.
- yarn breakages can occur during the spinning process due to the increased friction between the surfaces of the air spinning nozzle and the fibers.
- the air nozzles and other components of the air spinning nozzle can become clogged with deposits, so that the yarn obtained has a lower yarn strength and yarn quality.
- the invention is therefore based on the object of providing a spinning position of an air-jet spinning machine and a method for cleaning a yarn-forming element of an air-jet spinning nozzle which enable particularly long and trouble-free operation with consistent quality and strength of the yarn produced.
- the spinning position of an air-jet spinning machine has an air-spinning nozzle with a yarn-forming element arranged within a turbulence chamber for producing a yarn from a fiber sliver fed to the air-spinning nozzle, wherein the air-spinning nozzle can be converted from a closed state for yarn formation into an open state in which the yarn-forming element can be cleaned.
- At least one cleaning nozzle for cleaning the yarn-forming element when the air spinning nozzle is open is assigned to the spinning station or is arranged on the spinning station, with the cleaning nozzle being designed, in particular positioned and/or aligned or positionable and/or alignable in such a way that at least in the open State of the air spinning nozzle, the yarn formation element can be acted upon by the cleaning nozzle with a cleaning medium.
- the air-spinning nozzle having a whirl chamber is first opened to make the yarn-forming element arranged in the whirl chamber accessible, then and/or at the same time the yarn-forming element and/or a cleaning nozzle is moved into a cleaning position and finally the yarn-forming element with at least one cleaning medium applied.
- the inventors have recognized that regular cleaning of the yarn-forming element enables long and trouble-free operation with consistent quality and strength of the yarn produced, with such cleaning being possible in a particularly simple manner and without a disruptive effect on the other components of the air-jet spinning machine if the Air spinneret is in an open position, for example in the course of a spinning interruption after a thread breakage or a planned cut of the yarn.
- the invention advantageously allows an increase in strength and greater cleanliness spun yarns.
- An air spinneret is first understood to be any spinneret which, by means of at least one air stream, swirls fibers, in particular twisted fibers, around an internal fiber core to form a thread or yarn.
- the process of yarn formation takes place in the area of a turbulence chamber of the air spinning nozzle, in which at least one yarn-forming element is arranged.
- the air-jet spinning nozzle is surrounded by a spinning station, each spinning station serving to produce a yarn from a sliver fed to the air-jet spinning nozzle.
- the air spinning nozzle has an inlet for the sliver, the internal whirl chamber, one or more yarn forming or spinning elements arranged at least in sections in the whirl chamber, and an outlet for the yarn produced inside the whirl chamber.
- the air spinning nozzle preferably has a plurality of air nozzles opening into the turbulence chamber, which are particularly preferably in fluid communication with at least one air supply line, wherein during spinning operation of the spinning station, in which the yarn is produced by means of the air spinning nozzle, compressed air provided by the air supply line via the air nozzles in flows into the vortex chamber to generate a vortex air flow within the vortex chamber for air-spinning the supplied sliver into a yarn.
- a yarn or a thread within the meaning of the invention is a fiber structure in which at least some of the fibers are wound around an internal fiber core.
- a yarn can also be a roving or a roving for further processing, for example by means of a ring spinning machine.
- the sliver and thus the yarn produced from it is preferably formed at least partially, particularly preferably completely, from synthetic fibers or man-made fibers, for example from polyester or from polyethersulfone.
- the sliver is basically the fibrous material fed to the air spinning process, which is preferably provided as a coherent sliver or composite of fibers to be spun. All the fibers can be formed from the same material or the sliver can contain fibers that are chemically different from one another. In principle, however, the fibers in the sliver are not yet spun together.
- the Garn Strukturselement can be both an independent component, as well as a section of a Be a structural unit or a functional unit that is directly involved in the air spinning process.
- the yarn formation element can be formed in one piece or in several pieces.
- the yarn-forming element preferably has a spinning cone or part of a spinning cone, and the yarn-forming element very particularly preferably forms the spinning cone.
- the yarn-forming element comes into direct contact, at least in sections, with the fibers to be spun to produce the yarn and with the spun yarn.
- the air spinning nozzle can be switched from a closed state of the air spinning nozzle, in which the turbulence chamber is preferably formed by the air spinning nozzle and the yarn-forming element arranged in the turbulence chamber is surrounded by the turbulence chamber, to an open state in which the turbulence chamber is preferably opposite to the outer environment of the air spinning nozzle is opened and the yarn forming element is exposed for cleaning, for which purpose preferably at least a first component of the air spinning nozzle, which more preferably comprises the yarn forming element, can be moved relative to a further component of the air spinning nozzle.
- the first and the second component of the air spinning nozzle have, in particular, wall sections which at least partially delimit the turbulence chamber in the closed state of the air spinning nozzle.
- the first component of the air spinning nozzle which particularly preferably comprises the yarn-forming element, is particularly preferably moved, in particular shifted and/or pivoted, relative to the second component of the air spinning nozzle, which is preferably arranged stationary at the spinning station.
- the closed state of the air spinning nozzle is intended for yarn formation, while in the open state of the air spinning nozzle the yarn forming element is at least partially and particularly preferably completely accessible for cleaning.
- the opening of the air spinning nozzle and the movement of the yarn-forming element and/or preferably the cleaning nozzle can take place either completely one after the other or at least partially at the same time. It is also conceivable that when the air spinning nozzle is opened, the yarn-forming element is moved into a cleaning position at the same time or immediately thereafter, in which case a movement of the cleaning nozzle into a cleaning position is not necessary, but is preferably also possible.
- the cleaning position is that position of the yarn-forming element and/or the cleaning nozzle in which the yarn-forming element is cleaned by at least one cleaning medium by means of the cleaning nozzle.
- the cleaning position of the cleaning nozzle is preferably outside of the vortex chamber and/or opposite a surface of the yarn-forming element.
- the cleaning position is provided for operating the cleaning nozzle, with the cleaning nozzle preferably being operated exclusively in the cleaning position.
- no further component of the air spinning nozzle, the spinning position and/or the air spinning machine is preferably arranged in an impingement path between an outer surface of the yarn-forming element and the at least one cleaning nozzle, particularly preferably all cleaning nozzles.
- the cleaning by means of the cleaning nozzle can take place in any manner, with the method for cleaning preferably comprising a defined cleaning cycle, which in particular is made up of a number of cleaning steps.
- cleaning preferably means removing dirt from the yarn-forming element, in particular deposits of fibers, finishes and/or polymers.
- the dirt is particularly preferably removed from the outer surface of the yarn-forming element and/or at least part of a thread withdrawal channel inside the yarn-forming element.
- a cleaning nozzle for dispensing a cleaning medium and for feeding the cleaning medium to the yarn-forming element is provided according to the invention.
- the cleaning nozzle is arranged at the spinning station and/or directed towards the spinning station.
- At least one cleaning nozzle is preferably assigned to two spinning positions, more preferably to a single spinning position.
- the cleaning nozzle can preferably be arranged in the area of two adjacent spinning stations in such a way that the cleaning nozzle can apply a cleaning medium to the respective yarn-forming element of these two spinning stations. More preferably, a cleaning nozzle is arranged at each spinning station.
- the cleaning nozzle is preferably a nozzle for cleaning the yarn-forming element by means of a liquid and/or a gas.
- the cleaning medium can be either a gas or a liquid.
- any mixtures of gases and liquids, in particular aerosols, foams and/or emulsions, are also conceivable as the cleaning medium.
- more than one cleaning nozzle can also be arranged in the area of a yarn-forming element, with preferably several cleaning nozzles in the cleaning position directed at different surface sections of the yarn-forming element and/or from different directions at the yarn-forming element or are adjustable.
- the cleaning nozzle is also preferably formed in order to apply the cleaning medium to at least one surface section of the yarn-forming element by means of atomizer technology.
- the cleaning nozzle particularly preferably has a liquid atomizer, and the cleaning nozzle is very particularly preferably designed as a liquid atomizer.
- the cleaning nozzle is designed, in particular positioned and/or aligned or positionable and/or alignable, in such a way that the yarn-forming element can be acted upon by the cleaning medium in the cleaning position.
- the application of cleaning medium is understood to mean that a cleaning medium is guided onto at least a part or a section of the surface of the yarn-forming element.
- the supply of at least one cleaning medium to the cleaning nozzle preferably takes place via at least one cleaning medium line, which can be formed both as a pure liquid line and as a pure gas line or alternatively as a mixed line. Furthermore, in particular, the supply of gases and liquids as a cleaning medium can take place via different lines or lines that are separate from one another.
- An activation and/or dosing unit is preferably arranged in the supply direction of the at least one cleaning medium and especially for each individual cleaning medium in front of the cleaning nozzle, which is particularly preferably formed as a valve and/or as an adjustable throttle in order to regulate the quantity or the flow of the Being able to regulate the cleaning medium supplied to the yarn formation element in a defined manner.
- At least one cleaning nozzle is arranged outside the turbulence chamber and/or stationary on or in the area of the spinning position, whereby a particularly simple structure can be achieved and the air spinning process is not disturbed by the cleaning nozzle.
- At least one, in particular one further, cleaning nozzle can be moved outside the vortex chamber and/or by means of a pivoting device between a rest position and a cleaning position for cleaning the yarn-forming element, thereby enabling the spinning position to operate particularly smoothly.
- the movement between the rest position and the cleaning position is preferably a displacement, in particular an extension, and/or a folding over or pivoting.
- an advantageous embodiment of the spinning station with several cleaning nozzles is conceivable, with all cleaning nozzles preferably being stationary or movable or preferably at least one stationary cleaning nozzle and at least one movable cleaning nozzle for cleaning a yarn-forming element.
- the cleaning nozzle can be positioned and aligned, in particular by means of the pivoting device, in such a way that the yarn-forming element in the cleaning position can be exposed to the cleaning medium frontally and/or laterally, at least over part of the surface, as a result of which cleaning of the yarn-forming element is achieved in a particularly simple manner can be.
- frontally means in particular in a direction along a yarn withdrawal channel and/or in the direction of a tip of the yarn-forming element.
- Laterally means in particular from one side orthogonal to a yarn withdrawal channel arranged centrally in the yarn formation element and/or aligned towards a part of a preferably conical side surface of the yarn formation element.
- the cleaning nozzle can be rotated at least in sections, preferably completely around the yarn-forming element, in particular by means of the pivoting device, in order to be able to apply the cleaning medium to the entire surface of the yarn-forming element, in particular a spinning cone surface, during rotation .
- the cleaning nozzle can be rotated perpendicularly to a central longitudinal axis or a yarn draw-off channel of the yarn-forming element, or at a constant or variable angle, with rotation along a circular path or along a section of a circle being preferred becomes.
- a preferred embodiment of the method for cleaning a yarn-forming element provides that the cleaning nozzle for cleaning the yarn-forming element is moved by means of a pivoting device from a rest position to a cleaning position and/or from the cleaning position to the rest position after cleaning. In principle, this movement into the cleaning position can take place at any time. It is conceivable that the yarn-forming element is moved into the cleaning position by initiating the process of opening the air spinning nozzle, during the opening of the air spinning nozzle and/or after the opening of the air spinning nozzle. However, it is preferable for the yarn-forming element to be moved into the cleaning position in such a way that the cleaning nozzle is in the cleaning position before or at the end of the opening process, as a result of which particularly time-efficient cleaning is possible.
- a preferred embodiment of the method for cleaning a yarn-forming element provides that a yarn-forming element is cleaned in the course of a spinning interruption, for example after at least one or each thread breakage, after at least one or each cut of the yarn, during removal of a take-up package wound up by means of the air-spun yarn and/or or during a change of a sliver can from which the sliver is fed to the spinning station. Cleaning after a thread breakage makes it possible, in particular, for contamination as a possible reason for a thread breakage to be eliminated before the air-jet spinning process is resumed.
- Cleaning after the yarn has been cut, while the take-up bobbin is being removed or a new empty tube is being inserted in the winding device and during a sliver can change ensures consistently high yarn quality and strength, as does cleaning after a yarn breakage.
- cleaning can also be carried out periodically with defined identical or mutually different interval sections, in particular based on the operating time of the spinning position, the number of thread breaks, the number of cuts of the yarn, the number of take-up bobbins removed or the number of empty tubes used, the number of Spinning can changes, generally the number of spinning interruptions or spinning stops, are carried out in order to ensure regular cleaning ensure or avoid longer periods without being able to clean.
- cleaning can take place before the spinning station is put into operation after a defined downtime and/or before the spinning station is shut down in preparation for a defined downtime. This also ensures that when the spinning process is resumed, these disruptive deposits in the air spinning nozzle are minimized or eliminated as far as possible.
- a preferred embodiment of the method for cleaning a yarn-forming element provides that the yarn-forming element is cleaned by means of a cleaning liquid, in particular by means of an aqueous cleaning liquid, an aerosol, a foam, an emulsion or a gas as the cleaning medium.
- a suitable selection of the cleaning medium allows cleaning and, in particular, additional treatment of the surface of the yarn-forming element as required.
- a defined layer with a defined effect can be applied to the surface of the yarn-forming element in particular by means of an aerosol, foam or an emulsion, which can have an advantageous effect on the spinning process.
- the yarn-forming element can be provided with an anti-stick layer which at least reduces, at best prevents, adhesion of particles to the yarn-forming element for a certain period of time. As a result, cleaning cycles of the yarn-forming element can be lengthened.
- a cleaning liquid is any liquid which has a liquid content of preferably at least 90%, particularly preferably at least 95% and very particularly preferably at least 98%.
- the liquid can particularly preferably be water.
- the cleaning medium can likewise preferably contain at least one cleaning and/or surface-active substance, in particular at least one surfactant.
- a cleaning liquid, an aerosol, a foam or an emulsion to remove deposits and subsequently, in a second cleaning step, a gas stream is directed onto the yarn-forming element in order to remove the moisture from the surface of the yarn-forming element and/or to dry it, with such preferred cleaning particularly preferably being carried out using the same cleaning nozzle can.
- cleaning by means of a gas flow can be carried out both by a continuous gas flow and by one or more gas blasts or pulses.
- an advantageous embodiment of the method for cleaning a yarn-forming element is also conceivable, in which the yarn-forming element is cleaned first by means of a gas stream to remove loose particles from the surface, then by means of a cleaning liquid, an aerosol, a foam or an emulsion to loosen adhering particles and preferably finally again by means of a gas flow for the final cleaning and/or drying of the surface of the yarn-forming element.
- the second gas stream can also be dispensed with if necessary in order to keep the surface of the yarn-forming element moist and thereby achieve greater strength of the yarn produced by means of the yarn-forming element due to an increased force acting on the surface of the yarn-forming element.
- the spinning station can be included in a working station of the air-jet spinning machine.
- a work station is any position on the air-jet spinning machine at which an air-spun spun thread or yarn is produced by means of the spinning station from a fiber sliver fed to the spinning station and is wound up via a winding device downstream of the spinning station in the yarn path for winding a package, in particular a cross-wound bobbin .
- the sliver can be fed in via a central sliver store assigned to the air-jet spinning machine or via a sliver store assigned to the individual spinning station, such as a sliver can in particular, in which a defined quantity of sliver is stored so that it can be removed from the sliver can.
- the work station can have further sliver or thread treatment devices for the defined and needs-based treatment of the sliver or thread.
- the workplace can have sensors for monitoring the sliver feed and/or the sliver parameters as well as or alternatively for monitoring the yarn take-off, the yarn feed to the winding device, the yarn parameters, for cleaning up yarn defects and/or for piecing after a sliver or yarn break or after a sliver can change or a take-up package removal.
- sensors or other devices in the area of the drafting system can be assigned to the work station, by means of which the sliver can be defined and drawn as required and/or provided with additional fibers, in particular made of a different fiber material, a so-called core yarn.
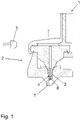
- a first in the figures 1 and 2 The illustrated embodiment of a spinning station 1 of an air-jet spinning machine has an air-spinning nozzle 2 in which a spinning cone is arranged as a yarn-forming element 4 within a turbulence chamber 3 .
- a sliver is first drafted using a multi-roller drafting system and the resulting stretched sliver is subsequently fed to the air spinning nozzle 2 via a sliver inlet 7 .
- the sliver is, after introduction via the sliver inlet 7, about a sliver transport direction extending in a previously known manner in the direction of the yarn-forming element 4, approximately up to the outlet of the latter Needle 8 out.
- a well-known pair of tweezers can be arranged according to a further preferred embodiment.
- the outer fibers of the sliver are wound around an internal fiber core by means of a turbulent air flow generated by air spinning nozzles 2 in the area of an inlet opening of the air spinning nozzle 2, so that an air-yarn-specific yarn structure of a parallel yarn core and winding fibers lying at a certain angle result, which are decisive for the desired strength of the yarn.
- a stationary cleaning nozzle 5 is arranged outside the vortex chamber 3 in the area of the spinning position 1, whereby this does not influence the air spinning process in the closed air spinning nozzle 2 due to its arrangement (see Fig figure 1 ).
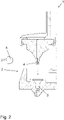
- the yarn forming element 4 is moved into a cleaning position when the air spinning nozzle 2 opens, in which an outlet opening of the stationary cleaning nozzle 5 is aligned with a side surface of the yarn forming element 4. so that the surface of the yarn-forming element 4 can be cleaned by means of the cleaning nozzle 5 (see figure 2 ).
- At least one aqueous cleaning liquid is atomized by means of the cleaning nozzle 5 and directed as a spray onto the yarn-forming element 4 so that the deposits adhering to the surface of the yarn-forming element 4 can be removed.
- a cleaning preferably takes place by means of a cleaning cycle that can be carried out once or repeated several times.
- a first possible cleaning cycle provides that first a cleaning liquid for removing deposits is sprayed onto the surface of the yarn-forming element 4 by means of the cleaning nozzle 5 and then also by means of the Cleaning nozzle 5, a compressed air pulse is directed onto the surface of the yarn-forming element 4 in order to remove the mixture of the cleaning liquid and the loosened adhesions and to dry the surface of the yarn-forming element 4.
- a foam is applied via the cleaning nozzle 5 to the surface of the yarn-forming element 4, with the foam being mixed with a non-stick liquid.
- the yarn-forming element 4 with the anti-adhesion liquid applied thereto is dried by means of the subsequent pulse of compressed air.
- a pulse of compressed air is first directed at the surface of the yarn-forming element 4 in order to remove loose buildup. This is followed by cleaning using a cleaning medium such as the cleaning liquid in order to remove the buildup that has not been loosened by the compressed air. Finally, the mixture of the cleaning liquid and the loosened adhesions is preferably also removed and the surface of the yarn-forming element 4 is dried by means of renewed application of compressed air.
- the same cleaning nozzle 5 is preferably used for all cleaning steps.
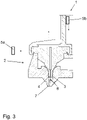
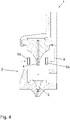
- a second, in the Figures 3 and 4 The illustrated embodiment of a spinning station 1 of an air-jet spinning machine differs significantly from the first embodiment in that instead of a stationary cleaning nozzle 5, two movable cleaning nozzles 5a, 5b are provided.
- a first cleaning nozzle 5a is arranged to be linearly displaceable in the direction of a side surface of the yarn-forming element 4, this cleaning nozzle 5a also being linearly in a cleaning position is shifted and thus at least one cleaning medium, in particular a cleaning liquid, an aerosol, a foam, an emulsion or a gas, can be applied to the yarn-forming element 4 in the immediate vicinity of the surface of the yarn-forming element 4 .
- this cleaning nozzle 5a can also at least partially surround the Yarn formation element 4 can be pivoted around so that a cleaning fluid can be applied along the circumference of the surface of the yarn formation element 4 .
- the second cleaning nozzle 5b can be moved both linearly and by means of a pivoting device 6 (in figure 4 shown only schematically by an arrow) on the surface of the Garn avoirselements 4 pivotally arranged.
- the second cleaning nozzle 5b is already linearly displaced during the opening of the air spinning nozzle 2 and the associated positioning of the yarn-forming element 4 in a cleaning position.
- the cleaning nozzle 5b is then pivoted by means of the pivoting device 6 in the direction of the surface of the yarn-forming element 4, so that cleaning can take place by means of both cleaning nozzles 5a, 5b.
- cleaning can be carried out with all cleaning nozzles 5 at the same time, or the cleaning nozzles 5a, 5b can be used for cleaning one after the other.
- both cleaning nozzles do not use the same cleaning medium at the same time or immediately one after the other, but instead a cleaning cycle that is independent of the other cleaning nozzles 5b, 5a can also be carried out using each cleaning nozzle 5a, 5b.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Textile Engineering (AREA)
- Spinning Or Twisting Of Yarns (AREA)
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP20215332.6A EP4015681B1 (fr) | 2020-12-18 | 2020-12-18 | Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil |
| US17/554,174 US11834759B2 (en) | 2020-12-18 | 2021-12-17 | Spinning position with a cleaning nozzle and method of cleaning a yarn forming element |
| BR102021025617-6A BR102021025617A2 (pt) | 2020-12-18 | 2021-12-17 | Posto de fiação com um bico de limpeza e método para a limpeza de um elemento de formação de fio |
| CN202111550502.8A CN114645345A (zh) | 2020-12-18 | 2021-12-17 | 具有清洁喷嘴的纺纱位置和用于清洁纱线形成件的方法 |
| JP2021205367A JP7853753B2 (ja) | 2020-12-18 | 2021-12-17 | クリーニングノズルを備えた紡績ユニットおよび糸形成エレメントをクリーニングする方法 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP20215332.6A EP4015681B1 (fr) | 2020-12-18 | 2020-12-18 | Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4015681A1 true EP4015681A1 (fr) | 2022-06-22 |
| EP4015681B1 EP4015681B1 (fr) | 2025-01-29 |
Family
ID=73855702
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20215332.6A Active EP4015681B1 (fr) | 2020-12-18 | 2020-12-18 | Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US11834759B2 (fr) |
| EP (1) | EP4015681B1 (fr) |
| JP (1) | JP7853753B2 (fr) |
| CN (1) | CN114645345A (fr) |
| BR (1) | BR102021025617A2 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11834759B2 (en) | 2020-12-18 | 2023-12-05 | Saurer Intelligent Technology AG | Spinning position with a cleaning nozzle and method of cleaning a yarn forming element |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP4012083A1 (fr) * | 2020-12-09 | 2022-06-15 | Saurer Intelligent Technology AG | Élément à filer d'une filière à jet d'air pour un métier à filer à jet d'air |
| DE102020133359A1 (de) | 2020-12-14 | 2022-06-15 | Saurer Spinning Solutions Gmbh & Co. Kg | Multifunktionsdüse für eine Spinnmaschine |
| DE102022114064A1 (de) | 2022-06-03 | 2023-12-14 | Saurer Spinning Solutions Gmbh & Co. Kg | Fadenabzugsdüse sowie Offenend-Spinnvorrichtung mit einer Fadenabzugsdüse |
| CN115156169B (zh) * | 2022-07-06 | 2023-07-28 | 杭州临港化纤有限公司 | 一种假捻盘的清洗工艺 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011038210A (ja) * | 2009-08-11 | 2011-02-24 | Murata Machinery Ltd | 空気紡績装置及びこの空気紡績装置を備える紡績機 |
| EP3048191A1 (fr) * | 2015-01-21 | 2016-07-27 | Maschinenfabrik Rieter Ag | Filiere d'un metier a tisser a jet d'air et son procede d'ouverture |
| CH713499A2 (de) * | 2017-02-28 | 2018-08-31 | Rieter Ag Maschf | Luftspinnmaschine zur Herstellung eines Garns aus einem strangförmigen Faserverband. |
| DE102017113257A1 (de) * | 2017-06-16 | 2018-12-20 | Maschinenfabrik Rieter Ag | Arbeitsstelle einer Luftspinnmaschine sowie Verfahren zum Öffnen einer Spinndüse |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4107911A (en) * | 1976-06-18 | 1978-08-22 | Murata Kikai Kabushiki Kaisha | Pneumatic spinning apparatus |
| JPS5932606Y2 (ja) * | 1981-10-13 | 1984-09-12 | 村田機械株式会社 | 空気式紡績装置における空気ノズル先端部の空気の整流板 |
| CH683697A5 (de) * | 1990-07-20 | 1994-04-29 | Rieter Ag Maschf | Vorrichtung zum automatischen Ansetzen oder Anspinnen eines Fadens und Verfahren zu ihrem Betrieb. |
| US5177950A (en) * | 1990-12-06 | 1993-01-12 | Fowler Jr Floyd N | Flexible whirl-cleaning nozzle |
| JPH0625923A (ja) * | 1992-04-30 | 1994-02-01 | Murata Mach Ltd | 風綿清掃台車 |
| EP0646192B1 (fr) * | 1993-04-16 | 1996-11-13 | Luwa AG | Installation permettant d'influer sur les conditions d'environnement de processus de traitement textiles |
| JP2009155749A (ja) | 2007-12-26 | 2009-07-16 | Murata Mach Ltd | 紡績機 |
| DE102012100674A1 (de) * | 2012-01-27 | 2013-08-01 | Maschinenfabrik Rieter Ag | Luftspinnmaschine mit einem Reinigungsorgan sowie Verfahren zum Reinigen der Wirbelkammer einer Luftspinnmaschine |
| JP2015101805A (ja) * | 2013-11-25 | 2015-06-04 | 村田機械株式会社 | 空気紡績装置及び紡績機 |
| CH709466A1 (de) | 2014-04-03 | 2015-10-15 | Rieter Ag Maschf | Spinnstelle einer Luftspinnmaschine sowie Verfahren zum Betrieb einer Luftspinnmaschine. |
| CH709749A1 (de) * | 2014-06-12 | 2015-12-15 | Rieter Ag Maschf | Luftspinnmaschine sowie Verfahren zum Betrieb einer solchen. |
| JP2019026980A (ja) * | 2017-08-02 | 2019-02-21 | 村田機械株式会社 | 空気紡績機 |
| DE102018130826A1 (de) * | 2018-12-04 | 2020-06-04 | Maschinenfabrik Rieter Ag | Spinndüse sowie Verfahren zum Reinigen derselben |
| EP4015681B1 (fr) | 2020-12-18 | 2025-01-29 | Saurer Intelligent Technology AG | Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil |
-
2020
- 2020-12-18 EP EP20215332.6A patent/EP4015681B1/fr active Active
-
2021
- 2021-12-17 US US17/554,174 patent/US11834759B2/en active Active
- 2021-12-17 BR BR102021025617-6A patent/BR102021025617A2/pt not_active Application Discontinuation
- 2021-12-17 JP JP2021205367A patent/JP7853753B2/ja active Active
- 2021-12-17 CN CN202111550502.8A patent/CN114645345A/zh active Pending
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011038210A (ja) * | 2009-08-11 | 2011-02-24 | Murata Machinery Ltd | 空気紡績装置及びこの空気紡績装置を備える紡績機 |
| EP3048191A1 (fr) * | 2015-01-21 | 2016-07-27 | Maschinenfabrik Rieter Ag | Filiere d'un metier a tisser a jet d'air et son procede d'ouverture |
| CH713499A2 (de) * | 2017-02-28 | 2018-08-31 | Rieter Ag Maschf | Luftspinnmaschine zur Herstellung eines Garns aus einem strangförmigen Faserverband. |
| DE102017113257A1 (de) * | 2017-06-16 | 2018-12-20 | Maschinenfabrik Rieter Ag | Arbeitsstelle einer Luftspinnmaschine sowie Verfahren zum Öffnen einer Spinndüse |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11834759B2 (en) | 2020-12-18 | 2023-12-05 | Saurer Intelligent Technology AG | Spinning position with a cleaning nozzle and method of cleaning a yarn forming element |
Also Published As
| Publication number | Publication date |
|---|---|
| BR102021025617A2 (pt) | 2022-06-28 |
| EP4015681B1 (fr) | 2025-01-29 |
| JP2022097468A (ja) | 2022-06-30 |
| US11834759B2 (en) | 2023-12-05 |
| CN114645345A (zh) | 2022-06-21 |
| JP7853753B2 (ja) | 2026-04-30 |
| US20220195634A1 (en) | 2022-06-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4015681B1 (fr) | Poste de filage doté d'une buse de nettoyage et procédé de nettoyage d'un élément de formation de fil | |
| EP2955256B1 (fr) | Metier a filer a jet d'air et procede de fonctionnement d'un tel metier a filer a jet d'air | |
| EP2767624B1 (fr) | Poste de filage d'un métier à tisser à jet d'air | |
| EP2767625B1 (fr) | Poste de filage d'un métier à filer | |
| DE19580019C1 (de) | Verfahren und Vorrichtung zur Herstellung eines Mischgarnes sowie Mischgarn | |
| DE19501545A1 (de) | Verfahren zum Andrehen von Garn in einer Spinnmaschine | |
| EP3148913B1 (fr) | Procédé permettant de faire fonctionner une machine textile et machine textile servant à produire une mèche | |
| EP3276057B1 (fr) | Unité guide-fil, métier à filer à bout ouvert et procédé de fonctionnement d'un poste de filage | |
| EP2329066B1 (fr) | Groupe de filature a buse d'air comprenant un composant en forme de broche | |
| WO2011006580A1 (fr) | Elément pour dispositif de filature à tuyère à air | |
| EP2944713B1 (fr) | Poste de filage pour une machine de filage à jet d'air et utilisation de celle-ci | |
| DE2722319A1 (de) | Verfahren und vorrichtung zum herstellen von garnen | |
| CH628095A5 (de) | Verfahren zum direkten spinnen eines garnes aus einem faserband, und vorrichtung zur durchfuehrung des verfahrens. | |
| EP1786961A1 (fr) | Dispositif de filature a jet d'air | |
| DE3331629C2 (de) | Verfahren zum Spinnzwirnen in einem Offenend-Spinnrotor und Vorrichtung zum Durchführen dieses Verfahrens | |
| EP0162367B1 (fr) | Procédé et dispositif pour la préparation de l'extrémité de fil pour la remise en route d'une machine à bout libéré | |
| DE69704028T2 (de) | Verfahren, vorrichtung und anlage zur behandlung von garnen mit fortlaufender verschiebung | |
| EP4015680B1 (fr) | Poste de filage d'un métier à filer à jet d'air et procédé de nettoyage d'un élément de formation de fil | |
| EP4259867B1 (fr) | Buse multifonctionnelle destinée à un métier à filer | |
| DE3430369A1 (de) | Verfahren und vorrichtung zur herstellung eines verbaenderten gesponnenen garnes | |
| CH707560A1 (de) | Spinnstelle einer Luftdüsenspinnmaschine. | |
| WO2021122669A1 (fr) | Procédé permettant d'agencer un brin de fibres sur un dispositif de filage d'un poste de filage | |
| LU501576B1 (de) | Luftspinnvorrichtung sowie Verfahren zur Oberflächenbehandlung innerhalb einer Luftspinnvorrichtung | |
| LU102753B1 (de) | Faserband-Streckwerk mit Additivzuführung | |
| DE4013689A1 (de) | Verfahren und vorrichtung zum verspinnen von stapelfasern zu einem garn |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20221222 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20240816 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SAURER INTELLIGENT TECHNOLOGY AG |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502020010312 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250429 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250429 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250529 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250529 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250129 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502020010312 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251210 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: U11 Free format text: ST27 STATUS EVENT CODE: U-0-0-U10-U11 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260101 |
|
| 26N | No opposition filed |
Effective date: 20251030 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20251205 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251222 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251231 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20260101 Year of fee payment: 6 |