EP4328376B1 - Formeur à tamis oblique - Google Patents
Formeur à tamis oblique Download PDFInfo
- Publication number
- EP4328376B1 EP4328376B1 EP23188826.4A EP23188826A EP4328376B1 EP 4328376 B1 EP4328376 B1 EP 4328376B1 EP 23188826 A EP23188826 A EP 23188826A EP 4328376 B1 EP4328376 B1 EP 4328376B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- wire
- horizontally extending
- former
- substantially horizontally
- web
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F1/00—Wet end of machines for making continuous webs of paper
- D21F1/48—Suction apparatus
- D21F1/50—Suction boxes with rolls
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F9/00—Complete machines for making continuous webs of paper
- D21F9/02—Complete machines for making continuous webs of paper of the Fourdrinier type
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H13/00—Pulp or paper, comprising synthetic cellulose or non-cellulose fibres or web-forming material
- D21H13/10—Organic non-cellulose fibres
- D21H13/20—Organic non-cellulose fibres from macromolecular compounds obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds
- D21H13/26—Polyamides; Polyimides
Definitions
- the present invention relates to an inclined wire former for producing a fibrous web, in particular a long-fiber paper or wet-laid nonwoven web, from at least one fibrous suspension, with a wire which runs over a circumferential region of a breast roll and then runs at least partially at an angle to the horizontal in the wire running direction before being deflected into a substantially horizontal direction at a deflection point, wherein in this inclined section of the wire at least one headbox applies at least a portion of the at least one fibrous suspension to the top of the wire, and at least one dewatering element is arranged on the bottom side for dewatering the at least a portion of the at least one fibrous suspension applied to the wire, wherein the headbox comprises a front wall which, together with the wire, defines an outlet gap for the at least one fibrous suspension.
- the invention further relates to the use of such an inclined wire former for producing a long fiber paper or wet-laid nonwoven web, in particular a battery separator paper web or an aramid paper web or a capacitor paper web.
- Such an inclined screen former is known, for example, from the German patent application DE 10 2004 047 518 A1 and is manufactured and marketed by the applicant under the name "hydroformer.” It is primarily used for the production of long-fiber papers and wet-laid nonwovens. This type of sheet formation utilizes fibers and fiber blends of various materials with a length of 1 to 40 mm.
- Some long-fiber paper or wet-laid nonwoven webs such as battery separator paper webs, aramid paper webs, or capacitor paper webs, have very high quality requirements. As a rule, they should have the lowest possible basis weight while being free of so-called "pinholes," i.e., small holes. This requires very good formation. Fiber agglomerations must be prevented, and the web should have as uniform a thickness and a cross-sectional area profile as possible. In this area, there is still potential for further improvement in the existing inclined wire formers.
- the problem is solved by a generic fourdrinier former as described above, in which the front wall of the headbox extends in the direction of wire travel beyond the deflection point of the wire, so that the outlet gap is arranged above the substantially horizontally extending section of the wire.
- the inventors are credited with recognizing that the quality of a long-fiber paper or wet-laid nonwoven web produced on a conventional inclined wire former is negatively affected by the fact that a portion of the fiber suspension exiting the outlet gap flows back along the inclined section of the wire due to gravity. By arranging the outlet gap above the essentially horizontally extending section of the wire, such backflow can be reliably prevented.
- substantially horizontally extending portion of the screen means that this portion of the screen either extends exactly horizontally or has only a small angle to the horizontal, namely an angle of less than 20°, preferably less than 10°, more preferably less than 5°. In any case, the angle to the horizontal of the "essentially horizontally extending section of the sieve" is smaller in magnitude than the angle to the horizontal of the inclined sieve section.
- the present invention is a special combination of an inclined wire former and a fourdrinier wire former, wherein the fiber suspension is applied to the wire by the special former largely in the region of the inclined wire section and only to a small extent in the substantially horizontally extending wire section.
- the at least one dewatering element arranged under the inclined section of the screen extends in the direction of screen travel beyond the deflection point of the screen, so that it ends below the substantially horizontally extending section of the screen. This ensures that dewatering by the at least one dewatering element through the screen also takes place in all areas where fiber suspension is applied to the screen.
- the front wall of the headbox has a curve or a kink or the like in the area of the wire deflection point, so that the distance between the front wall of the headbox and the wire tapers, preferably continuously, in the direction of wire travel. Due to the distance tapering in the direction of wire travel, the flow velocity of the fiber suspension to be applied to the wire can be kept approximately constant.
- a fixing suction device is arranged under the essentially horizontally extending sieve section, by means of which the The position of the waterline of the at least one fiber suspension on the essentially horizontally extending screen section can be determined.
- the fibers still possess turbulence energy from the headbox and can thus, while still in motion, be deposited in the sheet structures.
- the watery state in this sheet formation area is clearly illustrated by the side view of the essentially horizontally extending screen section, where a shiny, reflective surface can be seen. This phenomenon breaks off almost abruptly at the so-called "waterline,” and the surface subsequently appears relatively matte in the direction of screen travel.
- the position of the waterline can be adjusted using the fixing suction cup.
- At least one further dewatering element in particular a suction box, can be arranged downstream of the fixing suction device below the essentially horizontally extending screen section, by means of which the fibrous web can be further dewatered.
- the aim is to achieve a predetermined dry content of the fibrous web before it is removed from the screen.
- At least one steam blow box can be arranged above the essentially horizontally extending screen section.
- the steam can reduce the viscosity of the water in the fibrous web, which promotes dehumidification of the fibrous web, for example, by means of suction boxes arranged below the screen.
- At least one upper wire can be arranged above the essentially horizontally extending wire section for this purpose. This allows the fibrous web to be dewatered both downwards through the wire and upwards through the upper wire. This not only shortens the required dewatering distance but also improves the surface of the fibrous web.
- the fabric can have a low air permeability of less than 0.193 m3 /s (410 CFM) and/or a high retention value of more than 100 FSI. This allows even low-consistency fibrous webs to be reliably produced and transported.
- the essentially horizontally extending section of the screen is at least partially surrounded laterally by edge limiters.
- a further aspect of the present invention relates to the use of a previously described inclined wire former according to the invention for producing a long-fiber paper or wet-laid nonwoven web, in particular a battery separator paper web, an aramid paper web, or a capacitor paper web.
- the advantages of the inclined wire former according to the invention are particularly evident for these webs with their high quality requirements.
- the inclined screen former according to the invention is preferably operated such that the water line of the at least one fiber suspension is positioned on the substantially horizontally extending screen section. This prevents the fiber suspension from flowing back.
- the consistency of the at least one fiber suspension can be less than 0.3%, preferably less than 0.02%. Low consistency is particularly advantageous for battery separator paper webs, aramid paper webs, or capacitor paper webs. The same applies if the long-fiber paper or wet-laid nonwoven web has a basis weight of less than 20 g/ m2 .
- FIG 1 shows a schematic of an inclined wire former 10' known from the prior art with a headbox 20' and a wire 30'.
- the wire 30' designed as an endless wire loop, moves clockwise over a series of rollers.
- One of these rollers is designed as a breast roll 32'.
- the wire 30' moves upwards from the breast roll 32' at an angle oblique to the horizontal direction.
- the headbox 20' applies a fiber suspension to the top of the wire 30'.
- a dewatering element 40' is arranged on the bottom of the inclined wire section.
- the headbox 20' has a front wall 22', which, together with the wire 30', defines an outlet gap 24' for the fiber suspension.
- Behind the dewatering element 40' is a suction fixation device 50', by means of which the water line of the fiber suspension can be adjusted.
- Both the outlet gap 24' and the dewatering element 40' and the suction fixation device 50' are arranged here in the inclined region of the wire 30'. Only then is the wire 30' deflected in a substantially horizontal direction by means of a first deflection roller 34'. In the wire travel direction, in an area between the first deflection roller 34' and a second deflection roller 36', in which the wire 30' moves substantially horizontally, further dewatering elements 60' are arranged below the wire 30' to further dewater the fiber web.
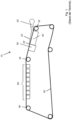
- FIG. 2 now schematically shows an embodiment of an inclined screen former 10 according to the invention. Similar or identical components as those shown in Figure 1 shown and described above, are provided with the same reference numerals, but without a prime. In the following, we will primarily focus on the differences between the two embodiments and otherwise refer to the explanations above regarding Figure 1 referred to.
- the inclined wire former 10 is particularly characterized in that the outlet gap 24 is already arranged above the essentially horizontally extending section of the wire 30.
- the front wall 22 of the headbox 20 extends over a deflection point at which the wire 30 transitions from an inclined wire section into the essentially horizontally extending wire section. This reliably prevents part of the fiber suspension emerging from the outlet gap from flowing back onto the wire 30, which is detrimental to the quality of the fibrous web to be produced.
- the front wall 22 is curved in the region of the deflection point such that its distance from the wire 30 tapers, preferably continuously, in the direction of wire travel.
- the dewatering element 40 located below the screen 30, also extends beyond the deflection point to below the essentially horizontally extending screen section. Since the upper side of the dewatering element 40 is curved, it guides the screen 30 and defines the deflection point. A deflection roller is therefore unnecessary here.
- the fixing suction device 50 which follows the dewatering element 40 in the direction of the screen travel, is thus arranged here below the substantially horizontally extending section of the screen 30. Consequently, the waterline of the fiber suspension emerging from the outlet gap 24 is also located on the substantially horizontally extending section of the screen 30.
- the screen 30 is preferably laterally supported by Figure 2 not shown, which prevent the fiber suspension from running down the side of the screen 30.
- a steam blow box 70 and/or an upper screen 80 can be arranged above the substantially horizontal screen section.
- the dehumidification of the fibrous web can be carried out efficiently downstream of the waterline, or the overall length of the inclined wire former 10 can be reduced, which is required to transfer the fibrous web with a predetermined dry content to a section of the production machine following the inclined wire former 10.
- further dewatering elements 60 are arranged in the area of the steam blow box 70 and/or the upper wire 80 below the wire.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Paper (AREA)
Claims (13)
- Appareil de formage (10) à tamis incliné pour la fabrication d'une bande de matière fibreuse, en particulier d'une bande de papier à fibres longues ou d'une bande de non-tissé humide, à partir d'au moins une suspension de matière fibreuse, comprenant un tamis (30) qui passe sur une zone périphérique d'un rouleau de tête (32) et s'étend ensuite dans la direction du tamis au moins par endroits en formant un angle oblique par rapport à l'horizontale, avant d'être déviée dans une direction essentiellement horizontale en un point de déviation ; dans cette partie oblique du tamis (30), au moins une caisse de tête (20) dépose au moins une partie de la suspension de matière fibreuse sur la face supérieure du tamis (30) ; et au moins un élément d'égouttage (40) est agencé sur le côté inférieur pour égoutter ladite au moins une partie de ladite au moins une suspension de matière fibreuse appliquée sur le tamis (30), la caisse de tête (20) comprenant une paroi avant (22) qui définit, conjointement avec le tamis (30), une fente de sortie (24) pour ladite au moins une suspension de matière fibreuse,
caractérisé en ce que la paroi avant (22) de la caisse de tête (20) s'étend dans le sens de circulation du tamis au-delà du point de déviation du tamis (30), de sorte que la fente de sortie (24) est agencée au-dessus de la partie du tamis (30) s'étendant essentiellement horizontalement. - Appareil de formage (10) à tamis incliné selon la revendication 1,
caractérisé en ce que ledit au moins un élément d'égouttage (40) agencé sur le côté inférieur de la partie inclinée du tamis (30) s'étend au-delà du point de déviation du tamis (30) dans le sens de circulation du tamis, de sorte qu'il se termine sous la partie sensiblement horizontale du tamis (30). - Appareil de formage (10) à tamis incliné selon la revendication 1 ou la revendication 2,
caractérisé en ce que la paroi avant (22) de la caisse de tête (20) comprend une courbure ou un pli dans la zone du point de déviation du tamis (30), de sorte que la distance entre la paroi avant (22) de la caisse de tête (20) et le tamis (30) se rétrécit dans le sens de circulation du tamis, de préférence de manière continue. - Appareil de formage (10) à tamis incliné selon l'une des revendications précédentes,
caractérisé en ce qu'un dispositif d'aspiration de fixation (50) est en outre agencé sous la partie du tamis s'étendant sensiblement horizontalement, au moyen duquel la position de la ligne d'eau de ladite au moins une suspension de matière fibreuse est apte à être déterminée sur la partie du tamis s'étendant sensiblement horizontalement. - Appareil de formage (10) à tamis incliné selon la revendication 4,
caractérisé en ce qu'au moins un autre élément d'égouttage (60), en particulier un caisson d'aspiration, est agencé en dessous de la partie de tamis s'étendant sensiblement horizontalement, à la suite du dispositif d'aspiration de fixation (50), au moyen duquel la bande de matière fibreuse est apte à être égouttée de façon supplémentaire. - Appareil de formage (10) à tamis incliné selon l'une des revendications précédentes,
caractérisé en ce qu'au moins un caisson de soufflage de vapeur (70) est agencé au-dessus de la partie de tamis s'étendant sensiblement horizontalement. - Appareil de formage (10) à tamis incliné selon l'une des revendications précédentes,
caractérisé en ce que ledit au moins un tamis supérieur (80) est agencé au-dessus de la partie de tamis s'étendant sensiblement horizontalement. - Appareil de formage (10) à tamis incliné selon l'une des revendications précédentes,
caractérisé en ce que le tamis (30) présente une faible perméabilité à l'air, de moins de 0,193m3/s et/ou un indice de rétention FSI (fiber support index) élevé, de plus de 100. - Appareil de formage (10) à tamis incliné selon l'une des revendications précédentes,
caractérisé en ce que la partie du tamis (30) s'étendant essentiellement horizontalement est entourée latéralement, au moins partiellement, par des limitateurs de bord. - Utilisation d'un appareil de formage (10) à tamis incliné selon l'une des revendications précédentes pour la fabrication d'une bande de papier à fibres longues ou d'une nappe non tissée par voie humide, en particulier d'une bande de papier séparateur de batterie ou d'une bande de papier aramide ou d'une bande de papier condensateur.
- Utilisation selon la revendication 10,
caractérisée en ce que l'appareil de formage (10) à tamis incliné est utilisé de telle sorte que la ligne d'eau de ladite suspension de matière fibreuse au moins se règle sur la partie de tamis s'étendant sensiblement horizontalement. - Utilisation selon la revendication 10 ou la revendication 11,
caractérisée en ce que la densité de ladite suspension de matière fibreuse est inférieure à 0,3%, de préférence inférieure à 0,02%. - Utilisation selon l'une des revendications 10 à 12, caractérisée en ce que la bande de papier à fibres longues ou de non-tissé par voie humide comprend un grammage inférieur à 20g/m2.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102022121105.3A DE102022121105A1 (de) | 2022-08-22 | 2022-08-22 | Schrägsiebformer |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4328376A1 EP4328376A1 (fr) | 2024-02-28 |
| EP4328376B1 true EP4328376B1 (fr) | 2025-05-21 |
Family
ID=87553848
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23188826.4A Active EP4328376B1 (fr) | 2022-08-22 | 2023-08-01 | Formeur à tamis oblique |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20240060238A1 (fr) |
| EP (1) | EP4328376B1 (fr) |
| CN (1) | CN117604802B (fr) |
| DE (1) | DE102022121105A1 (fr) |
| FI (1) | FI4328376T3 (fr) |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3147115A1 (de) * | 1981-11-27 | 1983-06-01 | Hermann Wangner Gmbh & Co Kg, 7410 Reutlingen | Spiralgliederband und verfahren zu dessen herstellung |
| WO1992001113A1 (fr) * | 1990-07-05 | 1992-01-23 | A. Ahlstrom Corporation | Procede et appareil de fabrication d'un materiau filtrant multicouche |
| JPH05502066A (ja) * | 1990-07-05 | 1993-04-15 | エイ.アフルストロム コーポレーション | 多層フィルター材の製造方法および装置 |
| JP3064134B2 (ja) * | 1993-01-14 | 2000-07-12 | 三菱重工業株式会社 | 多層紙形成装置 |
| US20020029860A1 (en) * | 1998-01-16 | 2002-03-14 | Liberty Diversified Industries | Moisture barrier paper and process for making the same |
| DE102004047518A1 (de) | 2004-09-28 | 2006-03-30 | Voith Paper Patent Gmbh | Verfahren und Schrägsiebformer einer Maschine zur Herstellung einer Faserstoffbahn aus mindestens einer Faserstoffsuspension |
| DE102008000435A1 (de) * | 2008-02-28 | 2009-09-03 | Voith Patent Gmbh | Schrägsiebformer einer Maschine zur Herstellung einer Faserstoffbahn aus mindestens einer Faserstoffsuspension |
| US8236082B2 (en) * | 2009-06-19 | 2012-08-07 | Hollingsworth & Vose Company | Flutable fiber webs with high dust holding capacity |
| EP2664708B1 (fr) * | 2011-01-12 | 2017-04-12 | Seiko Epson Corporation | Système et processus de recyclage de papier |
| FI126055B (en) * | 2012-05-14 | 2016-06-15 | Upm Kymmene Corp | A method of making a film from fibril pulp and a fibril pulp film |
| DE102014107725A1 (de) * | 2014-06-02 | 2015-12-03 | TRüTZSCHLER GMBH & CO. KG | Verfahren zur Herstellung eines strukturierbaren mehrschichtigen Vlieses und mehrschichtiges Vlies |
| FI127630B (en) * | 2014-12-17 | 2018-10-31 | Valmet Technologies Inc | Forming section of a fiber web machine and a secondary forming unit for a multiply forming section of a fiber web machine |
-
2022
- 2022-08-22 DE DE102022121105.3A patent/DE102022121105A1/de active Pending
-
2023
- 2023-08-01 FI FIEP23188826.4T patent/FI4328376T3/fi active
- 2023-08-01 EP EP23188826.4A patent/EP4328376B1/fr active Active
- 2023-08-18 CN CN202311047428.7A patent/CN117604802B/zh active Active
- 2023-08-22 US US18/453,449 patent/US20240060238A1/en active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| CN117604802B (zh) | 2026-05-12 |
| DE102022121105A1 (de) | 2024-02-22 |
| CN117604802A (zh) | 2024-02-27 |
| EP4328376A1 (fr) | 2024-02-28 |
| US20240060238A1 (en) | 2024-02-22 |
| FI4328376T3 (fi) | 2025-08-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0489094B2 (fr) | Dispositif pour la fabrication du papier comprenant deux toiles | |
| DE69308904T2 (de) | Blattbildungspartie für eine Papiermaschine | |
| DE69707256T2 (de) | DOPPELSIEBFORMER MIT ROLLE UND KLINGE FüR EINE PAPIERMASCHINE | |
| EP2739780B1 (fr) | Système de formation de feuille pour une machine de fabrication d'une bande de matière fibreuse à deux couches ou plus | |
| EP1233105A2 (fr) | Section de formage à deux toiles | |
| AT16049U1 (de) | Siebpartie, insbesondere eine umgebaute siebpartie | |
| DE69713104T2 (de) | Doppelsiebformer für eine papiermaschine | |
| DE112007000307T5 (de) | Bahnbildungspartie einer Papier-oder Pappemaschine | |
| DE102010030707A1 (de) | Blattbildungssystem für eine Maschine zur Herstellung einer zumindest einschichtigen Faserstoffbahn | |
| EP4328376A1 (fr) | Formeur à tamis oblique | |
| DE102004047518A1 (de) | Verfahren und Schrägsiebformer einer Maschine zur Herstellung einer Faserstoffbahn aus mindestens einer Faserstoffsuspension | |
| EP1098035B1 (fr) | Section de formage à deux toiles | |
| DE69923084T2 (de) | Doppelsiebformer | |
| DE9105797U1 (de) | Doppelsiebpartie einer Papier- oder Kartonmaschine | |
| DE1461179A1 (de) | Siebpartie einer Langsiebpapiermaschine mit Blattbildung unter Luftabschluss | |
| EP1953296B1 (fr) | Procédé de fabrication d'une bande de matière fibreuse et section de formage à deux toiles pour la mise en oeuvre du procédé | |
| AT507448B1 (de) | Blattbildungspartie | |
| EP1659211B1 (fr) | Système de formation d'une machine pour fabriquer une bande fibreuse | |
| EP1586702B1 (fr) | Section de formage à deux toiles pour machine de fabrication d'une bande de matériau fibreux | |
| WO2010012676A2 (fr) | Dispositif de formage à double tamis pour une machine de production d'une bande de matière fibreuse | |
| EP2072677B1 (fr) | Partie humide à deux toiles pour une machine destinée à la fabrication d'une bande de matière fibreuse à partir d'au moins une suspension de matière fibreuse | |
| DE102021113491A1 (de) | Formierpartie einer Faserbahn-Herstellungslinie | |
| DE102004051255A1 (de) | Blattbildungssystem | |
| DE202004021817U1 (de) | Blattbildungssystem | |
| DE202007003440U1 (de) | Former |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20240828 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20250121 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502023001027 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: FGE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250922 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20250822 Year of fee payment: 3 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250820 Year of fee payment: 3 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250821 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250822 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250828 Year of fee payment: 3 Ref country code: AT Payment date: 20251020 Year of fee payment: 3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502023001027 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250801 |
|
| 26N | No opposition filed |
Effective date: 20260224 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250801 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250521 |