EP4575004A1 - Verfahren zur herstellung von reduziertem eisen - Google Patents
Verfahren zur herstellung von reduziertem eisen Download PDFInfo
- Publication number
- EP4575004A1 EP4575004A1 EP23865056.8A EP23865056A EP4575004A1 EP 4575004 A1 EP4575004 A1 EP 4575004A1 EP 23865056 A EP23865056 A EP 23865056A EP 4575004 A1 EP4575004 A1 EP 4575004A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- pellets
- iron ore
- iron
- reduced iron
- clustering
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images




Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21B—MANUFACTURE OF IRON OR STEEL
- C21B13/00—Making spongy iron or liquid steel, by direct processes
- C21B13/008—Use of special additives or fluxing agents
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21B—MANUFACTURE OF IRON OR STEEL
- C21B3/00—General features in the manufacture of pig-iron
- C21B3/02—General features in the manufacture of pig-iron by applying additives, e.g. fluxing agents
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21B—MANUFACTURE OF IRON OR STEEL
- C21B11/00—Making pig-iron other than in blast furnaces
- C21B11/10—Making pig-iron other than in blast furnaces in electric furnaces
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21B—MANUFACTURE OF IRON OR STEEL
- C21B13/00—Making spongy iron or liquid steel, by direct processes
- C21B13/12—Making spongy iron or liquid steel, by direct processes in electric furnaces
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B1/00—Preliminary treatment of ores or scrap
- C22B1/14—Agglomerating; Briquetting; Binding; Granulating
- C22B1/16—Sintering; Agglomerating
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B1/00—Preliminary treatment of ores or scrap
- C22B1/14—Agglomerating; Briquetting; Binding; Granulating
- C22B1/24—Binding; Briquetting ; Granulating
- C22B1/2406—Binding; Briquetting ; Granulating pelletizing
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B1/00—Preliminary treatment of ores or scrap
- C22B1/14—Agglomerating; Briquetting; Binding; Granulating
- C22B1/24—Binding; Briquetting ; Granulating
- C22B1/242—Binding; Briquetting ; Granulating with binders
- C22B1/243—Binding; Briquetting ; Granulating with binders inorganic
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22B—PRODUCTION AND REFINING OF METALS; PRETREATMENT OF RAW MATERIALS
- C22B1/00—Preliminary treatment of ores or scrap
- C22B1/14—Agglomerating; Briquetting; Binding; Granulating
- C22B1/24—Binding; Briquetting ; Granulating
- C22B1/242—Binding; Briquetting ; Granulating with binders
- C22B1/244—Binding; Briquetting ; Granulating with binders organic
- C22B1/245—Binding; Briquetting ; Granulating with binders organic with carbonaceous material for the production of coked agglomerates
Definitions
- This present disclosure relates to a method of producing reduced iron, including a process of direct reduction of iron ore pellets in a vertical shaft furnace.
- Patent Literature (PTL) 1 describes pellets in which "the surface of the raw material iron ore is coated with cement”. Further, Non-Patent Literature (NPL) 1 states that "pellets having higher iron grade have higher shrinkage and are more likely to form clusters”.
- NPL 1 Dentaro Kaneko, et al., "Clustering Phenomena during Iron Oxide Reduction in Shaft Furnace", Tetsu-to-Hagane, Vol. 64 (1978), Issue 6, p. 681-690 .
- the inventors have conducted extensive studies and found that when SiO 2 , Al 2 O 3 , CaO, and MgO content of reduced iron pellets, FeO content of residual iron oxide in the reduced iron pellets, and M.Fe. content of metallic iron in the reduced iron pellets satisfy the following Expression (1), clustering of iron ore pellets can be suppressed. (SiO 2 + Al 2 O 3 + CaO + MgO + FeO)/M.Fe ⁇ 0.15 ... (1)
- the method of producing reduced iron can suppress clustering of iron ore pellets.
- SiO 2 , Al 2 O 3 , CaO, and MgO are SiO 2 , Al 2 O 3 , CaO, and MgO content, in mass%, of the reduced iron pellets
- FeO is residual iron oxide content, in mass%, of the reduced iron pellets
- M.Fe is metallic iron content, in mass%, of the reduced iron pellets.
- the raw material of iron ore pellets is typically iron ore powder, binder, and auxiliary material.
- high-grade iron ore, medium-grade iron ore, and low-grade iron ore are defined as follows, according to the total Fe content (T.Fe), Al 2 O 3 content, and SiO 2 content of the iron ore.
- a portion of the composition that volatilizes due to heating in the component analysis of iron ore is measured as a volatile portion (ignition loss), but T.Fe is the content of the composition of the iron ore including the volatile portion (content of the iron ore before volatilization), while SiO 2 and Al 2 O 3 are the content of the composition of the iron ore without the volatile portion (content of the iron ore after volatilization).
- the raw material of the iron ore powder includes iron ore having a composition in which total Fe content is 63 mass% or less and the sum of SiO 2 and Al 2 O 3 is 4 mass% or more, that is, medium-grade iron ore or low-grade iron ore.
- the clustering index can be suitably adjusted by using medium-grade iron ore or low-grade iron ore.
- there is no upper limit to the ratio of medium-grade iron ore or low-grade iron ore used in the raw material of the iron ore powder and all raw material of the iron ore powder may be one or both of medium-grade iron ore and low-grade iron ore.
- the iron ore pellets preferably include one or more types of binder.
- Bentonite is a preferred binder for the iron ore pellets, but any known or optional binder may be used, including organic and inorganic binders that provide similar effects.
- the iron ore pellets may be mixed with quicklime, limestone (CaCO 3 ), dolomite (CaMg(CO 3 ) 2 ), or the like, as auxiliary material. Adjustment of basicity of the iron ore pellets (adjustment of CaO content) is made by the auxiliary material. The basicity of the iron ore pellets is calculated by the weight ratio of CaO/SiO 2 in the iron ore pellets. By adjusting CaO/SiO 2 to lower values, the iron content, or hematite (Fe 2 O 3 ) content, of the iron ore pellets can be increased.
- the basicity of the iron ore pellets is preferably 0.6 or less, from the viewpoint of obtaining suitable strength. Further, the slag ratio can be suitably suppressed when the basicity is 0.6 or less.
- a lower limit of the basicity of the iron ore pellets is not particularly limited, but is generally 0.1 or more.
- the raw material described above is used to produce the iron ore pellets typically through the processes of grinding, mixing, granulation, and firing.
- Raw material that has been finely ground by a grinder such as a ball mill is mixed using a high-speed agitator mixer or the like, processed into pellet form using a pelletizer, drum mixer, or the like, and fired using an electric furnace, rotary kiln, or the like.
- Crushing strength of the iron ore pellets is preferably more than 250 kg.
- firing conditions are preferably set to a firing temperature (furnace temperature) of 1200 °C to 1350 °C and a hold time at the firing temperature of 10 min to 25 min.
- Particle size of the iron ore pellets is not particularly limited. Particle size of the iron ore pellets is preferably 10 mm to 12.5 mm.
- Reducing gas is not particularly limited, and may be, for example, a mixed gas containing, in vol%, 55 % H 2 and 35 % CO, with the balance being CO 2 and CH 4 , or a mixed gas containing 75 % H 2 and 20 % CO, with the balance being CO 2 and N 2 .
- Temperature of the reducing gas is preferably determined based on the clustering index to make clustering less likely.
- the temperature of the reducing gas is preferably 900 °C or more.
- the temperature of the reducing gas is more preferably 950 °C or more.
- the temperature of the reducing gas is even more preferably 1000 °C or more.
- Reduction efficiency is suitable when the temperature of the reducing gas is 900 °C or more.
- an upper limit of the temperature of the reducing gas at which clustering is unlikely to occur may be determined based on the clustering index, and therefore the temperature of the reducing gas is preferably set to be equal to or less than the determined upper limit.
- the percentage of T.Fe (total iron content) reduced to M.Fe (metallic iron) in the pellets after reduction is called the metallization rate.
- unreduced iron is mainly FeO.
- the metallization rate is therefore preferably 88 % or more.
- the metallization rate is therefore preferably 96 % or less.
- the slag ratio can be suitably controlled and clustering can be suppressed.
- the metallization rate is typically determined by the operating conditions of the reduction process (amount of reducing gas, temperature, hold time, and the like) and the apparatus used.
- SiO 2 , Al 2 O 3 , CaO, and MgO are SiO 2 , Al 2 O 3 , CaO, and MgO content, in mass%, of the reduced iron pellets
- FeO is residual iron oxide content, in mass%, of the reduced iron pellets
- M.Fe is metallic iron content, in mass%, of the reduced iron pellets.
- the content of various oxides and M.Fe. is the content when the volatile portion of the iron ore is not included.
- the clustering index is 0.15 or more.
- the clustering index is preferably 0.2 or more. When the clustering index is less than 0.15, clustering cannot be suppressed. Further, the clustering index is preferably 0.4 or less. The clustering index is more preferably 0.3 or less. When the clustering index is 0.4 or less, the amount of slag is suitable and efficient reduction can be carried out.
- the reduced iron pellets satisfy Expression (1), it is preferable to intentionally set one or both of (A) the SiO 2 , Al 2 O 3 , CaO, and MgO content of the iron ore pellets and (B) the metallization rate in the reduction process.
- the metallization rate in the reduction process is often set as an operating condition without consideration of the clustering index.
- the metallization rate is preset, it is more preferable to intentionally set (A) the SiO 2 , Al 2 O 3 , CaO, and MgO content of the iron ore pellets so that the reduced iron pellets satisfy Expression (1).
- the setting of (A) the SiO 2 , Al 2 O 3 , CaO, and MgO content of the iron ore pellets is preferably performed by setting one or both of (A-1) the composition of the iron ore powder and (A-2) the type and content of the binder and the auxiliary material in the iron ore pellet production process.
- A-2) The type and content of the binder and the auxiliary material are often set according to the properties (strength, basicity, and the like) required of the iron ore pellets, without consideration of the clustering index.
- the clustering index is preferably set to 0.15 or more by mixing iron ore containing a large amount of gangue without changing the basicity of the iron ore pellets.
- Iron ore, binder, and auxiliary material were prepared as raw material for iron ore pellets.
- Table 1 lists the chemical compositions of the iron ores used in Experiment Examples 1 to 5.
- Bentonite containing 3 % CaO, 60 % SiO 2 , 15 % Al 2 O 3 , and 3 % MgO was prepared as the binder.
- Limestone containing 53 % CaO, 1 % or less SiO 2 , 1 % or less Al 2 O 3 , and 1 % MgO was prepared as the auxiliary material.
- Table 1 (mass%) Ore Composition including volatile portion Composition without volatile portion T.Fe FeO SiO 2 CaO Al 2 O 3 MgO Ig.loss (volatile portion) T.Fe FeO SiO 2 CaO Al 2 O 3 MgO SiO 2 + Al 2 O 3 Ore A (low-grade) 56.38 0.34 5.34 0.16 3.12 0.20 10.23 62.80 0.38 5.95 0.18 3.48 0.22 9.4 Ore B (low-grade) 61.33 0.55 3.80 0.03 2.04 0.08 6.38 65.51 0.59 4.06 0.03 2.18 0.09 6.2 Ore C (medium-grade) 62.55 0.40 3.40 0.06 1.72 0.32 4.68 65.62 0.42 3.57 0.06 1.80 0.34 5.4 Ore D (high-grade) 63.74 0.82 1.24 0.01 1.83 0.04 5.56 67.49 0.87 1.31 0.01 1.94 0.04 3.3 Ore E (high-grade) 66.39 0.99 3.37 0.10 0.43
- the iron ore pellets were produced by changing the mix ratio of the five types of iron ore listed in Table 1, as well as the limestone and bentonite content. First, iron ore was ground in a ball mill to obtain iron ore powder. In each case, the mix ratio of the five types of iron ores listed in Table 1 was changed to obtain varied values of T.Fe in the reduced iron pellets, and a total of 2000 g of mixed iron ore powder was prepared. Further, limestone was added to the mixed iron ore powder at an addition rate set so that the basicity of the iron ore pellets was 0.2 or 1.1. Typically, a basicity of 0.2 is referred to as acidic and a basicity of 1.1 is referred to as basic, and these terms are indicated in FIG. 2 and FIG.
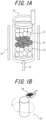
- FIG. 1A is a schematic diagram of the load softening reduction test apparatus.
- a carbon crucible 10 having a diameter of 100 mm was filled with alumina balls 12, 500 g of iron ore pellets 14, and alumina balls 12, in this order.
- FIG. 1B is a schematic diagram of the I-type rotational test machine.
- the clustered reduced iron pellets 20 were placed in the I-type rotational test machine 22 and crushed by rotating at 30 rpm for 5 min.
- the crushed sample was taken out and sorted through a 15 mm sieve.
- the weight of the sample remaining on the sieve was measured and the clustering rate CR (%) was calculated from the following formula. The higher the clustering rate, the more likely clustering would occur in a shaft furnace in actual production of reduced iron.
- CR Ws / W * 100
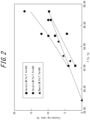
- FIG. 2 illustrates the relationship between T.Fe of reduced iron pellets and clustering rate of the reduced iron pellets obtained.
- the T.Fe was lowered by adding limestone.
- the trend of increasing clustering rate with increasing T.Fe of the reduced iron pellets was confirmed, but the effects of the metallization rate and the basicity of the iron ore pellets were also strongly evident.
- the clustering rate varied from 5 % to 13 % depending on the basicity. This indicates that a conventional method of suppressing clustering using T.Fe (iron grade) as an index, as described in NPL 1, may have difficulty suppressing clustering, depending on the type of iron ore and the metallization rate.
- FIG. 3 illustrates the relationship between the clustering index of reduced iron pellets that is a focus of the present disclosure and clustering rate of reduced iron pellets. Regardless of the metallization rate or the basicity, the reduced iron pellets that had a clustering index of 0.15 or more had a clustering rate of 9.5 % or less, which was a level of sufficient clustering suppression. This indicates that when reduced iron pellets are evaluated by the clustering index, as in the present disclosure, the clustering rate can be evaluated regardless of the metallization rate and the basicity.
- Iron ore pellets were produced in the same way as in Experiment Example 1 above, with further changes to the five iron ore blend mix ratios listed in Table 1 and to the basicity of the iron ore pellets to increase the number of test cases.
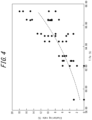
- the clustering rate evaluation tests were conducted on the obtained iron ore pellets, and the results are illustrated in FIG. 4 and FIG. 5 .
- the metallization rate of the reduced iron pellets was changed by changing the hold time in the clustering rate evaluation test. From FIG. 4 , it can be seen that the clustering rate varied even more when the T.Fe (iron grade) of the reduced iron pellets was used as an index.
- FIG. 5 illustrates that even when the number of test cases was increased, the reduced iron pellets that had a clustering index of 0.15 or more had a clustering rate of 9.5 % or less, which was a level of sufficient clustering suppression.
- Iron ore pellets were produced from low-grade iron ore "Ore A", medium-grade iron ore "Ore C", and high-grade iron ore “Ore D", respectively.
- each iron ore was ground in a ball mill to obtain iron ore powder.
- 2000 g of each iron ore powder was prepared, and limestone was added to the iron ore powder at an addition rate set so that the basicity of the iron ore pellets was 0.2.
- bentonite was added at 1.0 wt% relative to the iron ore powder amount, and iron ore pellets were produced in the same way as in Experiment Example 1.
- Clustering rate evaluation tests were performed on the obtained iron ore pellets, and the metallization rate of the reduced iron pellets was changed by changing the hold time.
- the hold time was 360 min for 92 % metallization, and for each 2 % increase in metallization, the hold time was extended by 20 min until 100 % metallization.
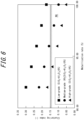
- FIG. 6 illustrates the relationship between the metallization rate and the clustering index obtained in the present experiment example. Even for iron ore pellets produced from the same raw material, the clustering index decreased as the metallization rate was increased. This may be because a higher metallization rate decreases the amount of unreduced FeO in the reduced iron pellets, which decreases the slag ratio and makes clustering more likely to occur.
- FIG. 6 illustrates that when low-grade iron ore or medium-grade iron ore is used, a clustering index of 0.15 or more can be achieved with a metallization rate of 96 % or less. Accordingly, the metallization rate is preferably 96 % or less. On the other hand, a lower metallization rate is undesirable because of the loss of reducibility. From this perspective, the metallization rate is preferably 88 % or more. Further, FIG. 6 illustrates that achieving a clustering index of 0.15 or more when only high-grade iron ore is used as raw material is difficult.
- FIG. 7 illustrates the relationship between the mix ratio of low/medium-grade iron ore in the iron ore pellets and the clustering index of the reduced iron pellets. It was found that the clustering index was higher with higher percentages of low/medium-grade iron ore, and that the clustering index could be 0.15 or more at a mix ratio of 40 mass%, both with low-grade iron ore and with medium-grade iron ore.
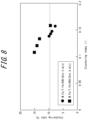
- FIG. 8 illustrates that clustering rate can be controlled by controlling the clustering index.
- Iron ore pellets having different clustering index values were produced by changing the mix ratio of the five types of iron ore listed in Table 1.
- a furnace temperature upper limit at which operation was possible without clustering occurring in a vertical shaft furnace was determined.
- the gas temperature was increased by 50 °C, a new sample was charged, and the same test was repeated.
- the test was terminated and the temperature before clustering occurred was set as the furnace temperature upper limit.
- FIG. 9 illustrates the relationship between the clustering index and the furnace temperature upper limit. It can be seen that the furnace temperature upper limit increases linearly with an increase in the clustering index. Accordingly, it can be seen that the clustering index can be used to suppress clustering and increase the temperature in a shaft furnace more than in a conventional case. Thus, the effects of the present disclosure are clear.
- the present disclosure provides a method of producing reduced iron that can suppress clustering of iron ore pellets.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Organic Chemistry (AREA)
- Metallurgy (AREA)
- Materials Engineering (AREA)
- Geochemistry & Mineralogy (AREA)
- Geology (AREA)
- Life Sciences & Earth Sciences (AREA)
- Mechanical Engineering (AREA)
- General Life Sciences & Earth Sciences (AREA)
- Environmental & Geological Engineering (AREA)
- Inorganic Chemistry (AREA)
- Manufacture And Refinement Of Metals (AREA)
- Manufacture Of Iron (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022148511 | 2022-09-16 | ||
| PCT/JP2023/025631 WO2024057694A1 (ja) | 2022-09-16 | 2023-07-11 | 還元鉄の製造方法 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4575004A1 true EP4575004A1 (de) | 2025-06-25 |
| EP4575004A4 EP4575004A4 (de) | 2025-10-15 |
Family
ID=90274605
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23865056.8A Pending EP4575004A4 (de) | 2022-09-16 | 2023-07-11 | Verfahren zur herstellung von reduziertem eisen |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20260071287A1 (de) |
| EP (1) | EP4575004A4 (de) |
| JP (1) | JP7477064B1 (de) |
| CN (1) | CN119866381A (de) |
| AU (1) | AU2023341035B2 (de) |
| CA (1) | CA3262920A1 (de) |
| WO (1) | WO2024057694A1 (de) |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1758171B2 (de) * | 1968-04-17 | 1976-09-02 | Metallgesellschaft Ag, 6000 Frankfurt | Verfahren zur herstellung von eisenschwammpellets |
| JPS55113818A (en) * | 1979-02-23 | 1980-09-02 | Kobe Steel Ltd | Shaft furnace for iron ore high temperature reduction |
| JPS589936A (ja) * | 1981-07-10 | 1983-01-20 | Nippon Kokan Kk <Nkk> | 塊成鉱製造法 |
| JP2002363624A (ja) * | 2001-06-13 | 2002-12-18 | Mitsubishi Heavy Ind Ltd | 還元鉄製造方法及び装置 |
| US7896963B2 (en) * | 2003-09-23 | 2011-03-01 | Hanqing Liu | Self-reducing, cold-bonded pellets |
| US11530464B2 (en) * | 2015-04-24 | 2022-12-20 | Sabic Global Technologies B.V. | Composite iron pellets and methods of making same |
| CN117480268A (zh) * | 2021-06-18 | 2024-01-30 | 杰富意钢铁株式会社 | 块矿的评价方法及块矿 |
-
2023
- 2023-07-11 JP JP2024504904A patent/JP7477064B1/ja active Active
- 2023-07-11 CN CN202380065580.XA patent/CN119866381A/zh active Pending
- 2023-07-11 WO PCT/JP2023/025631 patent/WO2024057694A1/ja not_active Ceased
- 2023-07-11 US US19/107,575 patent/US20260071287A1/en active Pending
- 2023-07-11 AU AU2023341035A patent/AU2023341035B2/en active Active
- 2023-07-11 CA CA3262920A patent/CA3262920A1/en active Pending
- 2023-07-11 EP EP23865056.8A patent/EP4575004A4/de active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| CA3262920A1 (en) | 2025-06-09 |
| AU2023341035B2 (en) | 2026-07-23 |
| JPWO2024057694A1 (de) | 2024-03-21 |
| JP7477064B1 (ja) | 2024-05-01 |
| EP4575004A4 (de) | 2025-10-15 |
| AU2023341035A1 (en) | 2025-02-13 |
| US20260071287A1 (en) | 2026-03-12 |
| WO2024057694A1 (ja) | 2024-03-21 |
| CN119866381A (zh) | 2025-04-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN100465306C (zh) | 改善高炉炉渣粘度的烧结矿及其制备方法 | |
| CN102242251A (zh) | 一种碱性钒钛球团矿及其制备方法 | |
| CN115404339B (zh) | 一种开发利用鲕状高磷铁矿的方法 | |
| CN113136486A (zh) | 一种加入低镍高铁镍矿的球团生产方法及配方 | |
| CN113774216A (zh) | 一种用红土镍矿作为球团粘结剂的球团的制备方法 | |
| AU2013236700A1 (en) | Method for adjusting precursor powder for sintered ore, and precursor powder for sintered ore | |
| CN115874048A (zh) | 一种强化粗粒磁铁精矿球团质量的方法 | |
| US20260071287A1 (en) | Method of producing reduced iron | |
| CN116377214B (zh) | 一种改善烧结转鼓强度的烧结混料方法 | |
| KR102458931B1 (ko) | 소결광 제조방법 | |
| CN117144121A (zh) | 一种褐铁矿与镜铁矿联合抑制烧结脆化的方法 | |
| EP4317464A1 (de) | Rohstoffpartikel zur herstellung von agglomeraten, verfahren zur herstellung von rohstoffpartikeln zur herstellung von agglomeraten, agglomerat, verfahren zur herstellung von agglomeraten und verfahren zur herstellung von reduziertem eisen | |
| Umadevi et al. | EFFECT OF OLIVINE AS MgO-BEARING FLUX ON LOW-AND HIGHALUMINA IRON ORE PELLETS | |
| CN101989479A (zh) | 一种烧结锶铁氧体永磁材料的制造方法 | |
| JP3252646B2 (ja) | 焼結鉱の製造方法 | |
| JPH10195549A (ja) | 焼結鉱の製造方法 | |
| EP4575003A1 (de) | Verfahren zur herstellung von heissem metall unter verwendung eines feststoffreduktionsofens und eines tauchbogenofens | |
| CN119287106B (zh) | 一种kr脱硫渣资源化利用工艺 | |
| CN1621541A (zh) | 一种高品位铁矿石直接干法制备球团矿的方法 | |
| CN116622982B (zh) | 降低球团矿膨胀率的方法 | |
| EP4556584A1 (de) | Nicht gebrannte pellets zur reduktion und verfahren zur herstellung davon | |
| JP4661077B2 (ja) | 焼結鉱の製造方法 | |
| EP4575020A1 (de) | Eisenerzpelletherstellungsverfahren | |
| CN114836616B (zh) | 铁矿粉球团矿及其制备方法 | |
| JPH09272925A (ja) | 高温性状と冷間強度の優れた焼結鉱の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20250319 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20250911 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C21B 13/02 20060101AFI20250905BHEP Ipc: C22B 1/16 20060101ALI20250905BHEP Ipc: C21B 11/10 20060101ALI20250905BHEP Ipc: C21B 13/12 20060101ALI20250905BHEP Ipc: C22B 1/24 20060101ALI20250905BHEP Ipc: C21B 3/02 20060101ALN20250905BHEP Ipc: C22B 1/243 20060101ALN20250905BHEP Ipc: C22B 1/245 20060101ALN20250905BHEP |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) |