EP4575665A1 - Verfahren zur herstellung von spiralfedern einer uhr - Google Patents
Verfahren zur herstellung von spiralfedern einer uhr Download PDFInfo
- Publication number
- EP4575665A1 EP4575665A1 EP23217974.7A EP23217974A EP4575665A1 EP 4575665 A1 EP4575665 A1 EP 4575665A1 EP 23217974 A EP23217974 A EP 23217974A EP 4575665 A1 EP4575665 A1 EP 4575665A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- watch
- stiffness
- batch
- balance springs
- average
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images
Classifications
-
- G—PHYSICS
- G04—HOROLOGY
- G04D—APPARATUS OR TOOLS SPECIALLY DESIGNED FOR MAKING OR MAINTAINING CLOCKS OR WATCHES
- G04D3/00—Watchmakers' or watch-repairers' machines or tools for working materials
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B17/00—Mechanisms for stabilising frequency
- G04B17/04—Oscillators acting by spring tension
- G04B17/06—Oscillators with hairsprings, e.g. balance
- G04B17/066—Manufacture of the spiral spring
-
- G—PHYSICS
- G04—HOROLOGY
- G04D—APPARATUS OR TOOLS SPECIALLY DESIGNED FOR MAKING OR MAINTAINING CLOCKS OR WATCHES
- G04D3/00—Watchmakers' or watch-repairers' machines or tools for working materials
- G04D3/0069—Watchmakers' or watch-repairers' machines or tools for working materials for working with non-mechanical means, e.g. chemical, electrochemical, metallising, vapourising; with electron beams, laser beams
-
- G—PHYSICS
- G04—HOROLOGY
- G04D—APPARATUS OR TOOLS SPECIALLY DESIGNED FOR MAKING OR MAINTAINING CLOCKS OR WATCHES
- G04D7/00—Measuring, counting, calibrating, testing or regulating apparatus
- G04D7/10—Measuring, counting, calibrating, testing or regulating apparatus for hairsprings of balances
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49579—Watch or clock making
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49609—Spring making
Definitions
- the manufacturing method comprises the following steps: a) a hairspring is formed in dimensions greater than the dimensions necessary to obtain a hairspring of a predetermined stiffness, b) the stiffness of the hairspring formed during step a) is determined by measuring the frequency of the hairspring coupled with a balance wheel having a predetermined inertia, c) the thickness of material to be removed to obtain the hairspring of a predetermined stiffness is calculated and d) the formed hairspring is removed in step a) the calculated material thickness, steps b), c) and d) can be repeated to further improve the dimensional quality.
- the manufacturing method comprises the following steps: a) a hairspring is formed in dimensions smaller than the dimensions necessary to obtain a hairspring of a predetermined stiffness, b) the stiffness of the hairspring formed during step a) is determined by measuring the frequency of the hairspring coupled with a balance wheel having a predetermined inertia, c) the missing material thickness is calculated to obtain the hairspring of a predetermined stiffness and d) the hairspring formed during step a) is modified to compensate for the missing material thickness, it being possible for steps b), c) and d) to be repeated to further improve the dimensional quality.
- Such methods can be improved in particular in order to limit the contamination of the wafer which can be generated during the measurement step which they implement.
- An aim of the present invention is to propose a method for manufacturing a batch of watch balance springs making it possible to meet the aforementioned needs.
- Another goal is to improve the precision of the manufacturing of the batch of watch hairsprings whose stiffnesses have an average within a predetermined range.
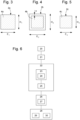
- FIG. 6 shows a schematic representation of the manufacturing process of a batch or set of 2a watch hairsprings whose stiffnesses have an average within a predetermined range. Such a process aims to ensure very high dimensional precision of the hairsprings 2a manufactured and, incidentally, to guarantee a more precise stiffness of these 2a hairsprings.
- each hairspring 2b, 2c comprises a collet intended to be secured to a pivoting shaft.
- This watch hairspring 2b, 2c also comprises an elastically flexible strand connected by one end to the collet and wound in a spiral so as to form several consecutive turns, the last of which is extended by an attachment segment intended to be attached to a fixed balance bridge, for example by means of a stud.
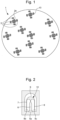
- Such a method comprises a step 20 of forming in the plate 1 the watch balance springs 2b, 2c according to dimensions E, E3, H2, H3 different from the dimensions E1, H1 necessary to obtain the batch of watch balance springs 2a whose stiffnesses have the average included in the predetermined range.
- the spirals 2b, 2c are formed in the wafer 1 of material. These spirals 2b, 2c are preferably formed simultaneously in this wafer 1.
- the formation of these spirals 2a, 2c in the wafer 1 can be carried out by etching, for example by deep reactive ion etching, by laser etching, by chemical etching or by etching using a focused ion beam. It will be noted that these spirals 2b, 2c preferably have similar geometries.
- These watch hairsprings 2b, 2c formed in this plate 1 have blades having sections 4b, 4c of dimensions E2, H2, E3, H3 - characterized by a height H1, H2, H3 and a thickness E1, E2, E3 of this section 4a, 4b, 4c when such a blade is of polygonal shape - which are different from the dimensions E1, H1 necessary to obtain the batch of watch hairsprings 2a whose stiffnesses have the average included in the predetermined range.
- the blade of each hairspring 2b, 2c can have a section 4b, 4c whose dimensions E2, H2, E3, H3 are greater than or less than the necessary dimensions E1, H1 of the section 4a of the blade of the manufactured 2a hairspring which makes it possible to obtain a stiffness in the average included in the predetermined range.
- the wafer 1 is preferably made of doped or undoped silicon.
- This silicon can be monocrystalline, polycrystalline or amorphous silicon.
- this silicon can be of orientation ⁇ 1,1,1 ⁇ , ⁇ -1,1,1 ⁇ , ⁇ 1,-1,1 ⁇ , ⁇ -1,-1,1 ⁇ for which the Young model of silicon is the most important.
- this wafer 1 can be made of quartz, glass, ceramic, metal or alloy.
- the method also comprises a step 21 of forming in the wafer 1, systems for indicating a reference stiffness 3, for determining the stiffnesses of the watch balance springs 2a whose average is included in the predetermined range.
- This step 21 is carried out in the same plate 1 comprising the watch hairsprings 2b, 2c formed and this, preferably simultaneously with the step 20 of forming these hairsprings 2b, 2c.
- a system 3 is formed in the plate 1 for each hairspring 2b, 2c of the batch of watch hairsprings formed.
- This system 3 is made up of at least one oscillating element 10 which is arranged in the immediate vicinity of the corresponding hairspring 2b, 2c.
- the oscillating element 10 of each system 3 is preferably formed by etching. It will be noted that there may be in this plate 1 as many systems 3 as there are hairsprings 2b, 2c and the height of the oscillating element 10 is similar to that of the plate 1 and therefore to that of the hairsprings 2b, 2c. Alternatively, this plate 1 may include a minimum sample of system 3 making it possible to obtain a good representation of the stiffnesses on this plate 1.
- this system 3 preferably comprises a plurality of oscillating elements 10.
- Such an element 10 comprises at least one blade and can extend essentially in a rectilinear manner.
- This element 10 comprises an attachment end 5a and at least one free end 5b, 5c.
- This element 10 has a geometric shape and dimensions which are different from those of a hairspring of this plate 1, with the exception of course of the height as we have specified previously.
- Each oscillating element 10 is included in an opening 9 made in the plate 1. This opening 9 defines a space in which the oscillating element 10 can freely execute a controlled/controlled mechanical oscillation movement.
- this oscillating element 10 comprises an attachment end 5a and two free ends 5b, 5c.
- this oscillating element 10 comprises a rod/trunk 6 provided with the attachment end 5a.
- This rod 6 extends rectilinearly in the opening 9 and comprises in its extension two arms 7, 8 forming two flexible blades, or two flexible branches, which are folded along the rod 6. More precisely, such arms 7, 8 are arranged in the opening 9 while being located close to the stem 6 and are in this configuration essentially parallel to the latter.
- These two arms 7, 8 are connected to each other forming the letter “U” and each comprise a free end of the oscillating element 10. It will be noted that these arms 7, 8 may each have a thickness similar or substantially similar to that of the hairspring.
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Optics & Photonics (AREA)
- Plasma & Fusion (AREA)
- Micromachines (AREA)
- Springs (AREA)
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP23217974.7A EP4575665A1 (de) | 2023-12-19 | 2023-12-19 | Verfahren zur herstellung von spiralfedern einer uhr |
| US18/941,193 US12481248B2 (en) | 2023-12-19 | 2024-11-08 | Method for manufacturing horological balance springs |
| TW113143536A TWI910910B (zh) | 2023-12-19 | 2024-11-13 | 製造鐘錶遊絲之方法 |
| JP2024206421A JP7831727B2 (ja) | 2023-12-19 | 2024-11-27 | ヒゲゼンマイを製造する方法 |
| CN202411724580.9A CN120178646A (zh) | 2023-12-19 | 2024-11-28 | 钟表游丝的制造方法 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP23217974.7A EP4575665A1 (de) | 2023-12-19 | 2023-12-19 | Verfahren zur herstellung von spiralfedern einer uhr |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP4575665A1 true EP4575665A1 (de) | 2025-06-25 |
Family
ID=89224545
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23217974.7A Pending EP4575665A1 (de) | 2023-12-19 | 2023-12-19 | Verfahren zur herstellung von spiralfedern einer uhr |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US12481248B2 (de) |
| EP (1) | EP4575665A1 (de) |
| JP (1) | JP7831727B2 (de) |
| CN (1) | CN120178646A (de) |
| TW (1) | TWI910910B (de) |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3181938A1 (de) | 2015-12-18 | 2017-06-21 | CSEM Centre Suisse d'Electronique et de Microtechnique SA - Recherche et Développement | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch wegnahme von material |
| EP3181939A1 (de) | 2015-12-18 | 2017-06-21 | CSEM Centre Suisse d'Electronique et de Microtechnique SA - Recherche et Développement | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch zugabe von material |
| EP3982205A1 (de) * | 2020-10-06 | 2022-04-13 | Patek Philippe SA Genève | Verfahren zur herstellung einer uhrfeder mit einer präzisen steifigkeit |
| CH719668A2 (fr) * | 2022-05-06 | 2023-11-15 | Richemont Int Sa | Procédé de fabrication de composants horlogers. |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6843594B1 (en) * | 1997-08-28 | 2005-01-18 | Seiko Epson Corporation | Spring, power spring, hair spring, driving mechanism utilizing them, and timepiece |
| TWI796444B (zh) * | 2018-03-20 | 2023-03-21 | 瑞士商百達翡麗日內瓦股份有限公司 | 用於製造精確剛度之時計熱補償游絲的方法 |
| CH716605A1 (fr) | 2019-09-16 | 2021-03-31 | Richemont Int Sa | Procédé de fabrication d'une pluralité de résonateurs sur une plaquette. |
| CH716603A1 (fr) * | 2019-09-16 | 2021-03-31 | Sigatec Sa | Procédé de fabrication de spiraux horlogers. |
| EP4030243B1 (de) * | 2021-01-18 | 2024-09-25 | Richemont International S.A. | Verfahren zur kontrolle und zur herstellung von uhrwerk-spiralfedern |
-
2023
- 2023-12-19 EP EP23217974.7A patent/EP4575665A1/de active Pending
-
2024
- 2024-11-08 US US18/941,193 patent/US12481248B2/en active Active
- 2024-11-13 TW TW113143536A patent/TWI910910B/zh active
- 2024-11-27 JP JP2024206421A patent/JP7831727B2/ja active Active
- 2024-11-28 CN CN202411724580.9A patent/CN120178646A/zh active Pending
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3181938A1 (de) | 2015-12-18 | 2017-06-21 | CSEM Centre Suisse d'Electronique et de Microtechnique SA - Recherche et Développement | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch wegnahme von material |
| EP3181939A1 (de) | 2015-12-18 | 2017-06-21 | CSEM Centre Suisse d'Electronique et de Microtechnique SA - Recherche et Développement | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch zugabe von material |
| EP3982205A1 (de) * | 2020-10-06 | 2022-04-13 | Patek Philippe SA Genève | Verfahren zur herstellung einer uhrfeder mit einer präzisen steifigkeit |
| CH719668A2 (fr) * | 2022-05-06 | 2023-11-15 | Richemont Int Sa | Procédé de fabrication de composants horlogers. |
Also Published As
| Publication number | Publication date |
|---|---|
| US20250199476A1 (en) | 2025-06-19 |
| CN120178646A (zh) | 2025-06-20 |
| TWI910910B (zh) | 2026-01-01 |
| TW202528856A (zh) | 2025-07-16 |
| US12481248B2 (en) | 2025-11-25 |
| JP2025097923A (ja) | 2025-07-01 |
| JP7831727B2 (ja) | 2026-03-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4278234B1 (de) | Verfahren zur kontrolle und zur herstellung von uhrwerk-spiralfedern | |
| EP2175328B1 (de) | Uhrwerk umfassend einen flachen Spiralfeder | |
| EP3181938B1 (de) | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch wegnahme von material | |
| EP3181939B1 (de) | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch zugabe von material | |
| EP1519250B1 (de) | Spiralfeder-Unruh-Resonator mit Thermokompensation | |
| EP3982205B1 (de) | Verfahren zur herstellung einer uhrfeder mit einer präzisen steifigkeit | |
| EP3181940B1 (de) | Herstellungsverfahren einer spiralfeder mit einer vorbestimmten steifigkeit durch lokalisierte wegnahme von material | |
| CH710795A2 (fr) | Spiral en silicium. | |
| EP4558866B1 (de) | Verfahren zur kontrolle und herstellung von uhrwerk-spiralfedern | |
| CH719668A2 (fr) | Procédé de fabrication de composants horlogers. | |
| EP2869138B1 (de) | Spiralfeder für Regulierorgan einer mechanischen Armbanduhr, mit einer solchen Spiralfeder ausgestattetes Regulierorgan und Herstellungsverfahren einer solchen Spiralfeder | |
| EP4453665A1 (de) | Verfahren zum testen und herstellen von ausgleichsfedern für uhren | |
| EP4030242A1 (de) | Verfahren zur herstellung von uhrwerks-spiralfedern | |
| EP3865954B1 (de) | Herstellungsverfahren einer monoblock-vorrichtung mit federzungen aus silizium, für uhrwerk | |
| CH721422A2 (fr) | Procédé de fabrication d'un lot de ressorts spiraux d'horlogerie | |
| EP4273632B1 (de) | Verfahren zur herstellung von uhrenkomponenten | |
| EP4202576A1 (de) | Verfahren zur kontrolle und herstellung von uhrwerk-spiralfedern | |
| TWI910910B (zh) | 製造鐘錶遊絲之方法 | |
| EP4012511A1 (de) | Verfahren zum harmonischen stimmen mindestens eines klangs eines schlagwermechanismus einer armbanduhr | |
| EP3839642A1 (de) | Herstellungsverfahren von uhrenfedern und ätzmaske für ein solches verfahren | |
| EP4650882A1 (de) | Verfahren zur herstellung von uhren-spirux | |
| WO2025153445A1 (fr) | Procédé de contrôle d'éléments inertiels horlogers | |
| EP2017681A1 (de) | Breguet-Spiralfeder für Uhr und Verfahren zu deren Herstellung | |
| EP4614242A1 (de) | Herstellung und paarung von uhrenkomponenten | |
| EP4553586A1 (de) | Verfahren zur herstellung einer rückstellfeder mit genauer steifigkeit für einen uhrresonator |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20260102 |