JP5074246B2 - オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 - Google Patents
オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 Download PDFInfo
- Publication number
- JP5074246B2 JP5074246B2 JP2008061335A JP2008061335A JP5074246B2 JP 5074246 B2 JP5074246 B2 JP 5074246B2 JP 2008061335 A JP2008061335 A JP 2008061335A JP 2008061335 A JP2008061335 A JP 2008061335A JP 5074246 B2 JP5074246 B2 JP 5074246B2
- Authority
- JP
- Japan
- Prior art keywords
- moving
- side member
- continuous casting
- core
- fixed
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000009749 continuous casting Methods 0.000 title claims description 59
- 238000001816 cooling Methods 0.000 description 28
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 22
- 229910052802 copper Inorganic materials 0.000 description 22
- 239000010949 copper Substances 0.000 description 22
- 229910000831 Steel Inorganic materials 0.000 description 4
- 238000005266 casting Methods 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- 239000000498 cooling water Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
Images


Landscapes
- Continuous Casting (AREA)
Description
該連続鋳造鋳型を前記連続鋳造設備に固定する固定フレームをそれぞれ基部が貫通し、前記固定側長辺部材の背面側に先部が配置された固定側コア及び前記移動側長辺部材の背面側に先部が配置されると共に該移動側長辺部材の移動方向に沿って移動可能に設けられた移動側コアと、
前記固定側コア及び前記移動側コアの外周にそれぞれ隙間を設けて捲回された電磁ブレーキコイルと、
前記固定フレームに取付けられ、前記移動側コアを前記移動側長辺部材の移動方向に沿って移動させて、該移動側コアと該移動側長辺部材との距離を調整する駆動部とを有している。
これによって、作業空間を確保するために移動させた移動側コアの短辺部材交換後の位置決めを、簡素な構成で確実に、かつ精度よく実施できる。
これによって、移動側コアを大きく移動させて十分な作業空間を確保することができる。
これによって、ライナーの挿入を簡素な構成で確実に行うことができる。
また、電磁ブレーキを構成する部材の中で移動するのは移動側コアのみなので、電磁ブレーキの構造が簡素となり、製造コストの上昇を抑えることができる。
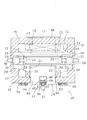
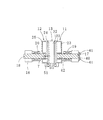
ここで、図1は本発明の一実施の形態に係る電磁ブレーキを搭載した連続鋳造鋳型の一部切り欠き平面図、図2は同電磁ブレーキを搭載した連続鋳造鋳型の正面図、図3は図2のA−A断面図、図4は同電磁ブレーキを搭載した連続鋳造鋳型において移動側コアを移動させその位置決めが行われた状態を示す説明図、図5は同電磁ブレーキを搭載した連続鋳造鋳型で移動側長辺部材を移動した状態を示す説明図である。
図4、図5に示すように、短辺部材13、14を交換する場合、先ず、コア移動用シリンダ21を操作して短辺部材13、14と別の短辺部材との幅の差分に相当する長さ、すなわち、ライナー52、53の厚みより大きい距離だけ移動側コア18を移動させる。次いで、移動側冷却箱解放シリンダ30、31を操作して、短辺部材13、14を取外して別の短辺部材に交換することができるように移動側長辺部材12を移動させる(なお、移動側コア18の移動量は移動側長辺部材12の移動量より大きい)。これによって、短辺部材13、14を別の短辺部材に交換する際の作業空間が確保される。
例えば、本実施の形態では、使用する短辺部材の種類を2種類としたが、3種類以上にすることもできる。この場合、最小幅の短辺部材で連続鋳造鋳型を形成した際の移動側コアの位置決めが移動側コアの鍔部を固定フレームに当接させたときに行われるようにしておき、ライナーの形状を階段状にして最小幅の短辺部材と残りの短辺部材との幅の差分に相当する高さの平坦部が、高さが高くなるにつれて先側から基側に向けて順次形成されるようにする。そして、鍔部と固定フレームの間に形成される隙間に挿入するライナーの挿入量を調整することで、短辺部材を交換した際の移動側コアの位置決めを行うことができる。また、鍔部とライナーを側面視して互いに当接する楔形状として、鍔部に当接するライナー位置を調整することで、短辺部材を交換した際の移動側コアの位置決めを行うようにすることもできる。
更に、移動側コア及びライナーの移動をそれぞれコア移動用シリンダ、ライナー移動用シリンダを用いて行ったが、ねじ送り機構を用いて移動することもできる。
Claims (4)
- 固定側長辺部材と、該固定側長辺部材に対向し該固定側長辺部材との間隔の調整が可能な移動側長辺部材と、該固定側長辺部材及び該移動側長辺部材で挟まれて対向する対となる短辺部材とを有し、前記固定側長辺部材及び前記移動側長辺部材を連続鋳造設備に取付けた状態で前記両短辺部材を交換する電磁ブレーキを搭載した連続鋳造鋳型であって、
該連続鋳造鋳型を前記連続鋳造設備に固定する固定フレームをそれぞれ基部が貫通し、前記固定側長辺部材の背面側に先部が配置された固定側コア及び前記移動側長辺部材の背面側に先部が配置されると共に該移動側長辺部材の移動方向に沿って移動可能に設けられた移動側コアと、
前記固定側コア及び前記移動側コアの外周にそれぞれ隙間を設けて捲回された電磁ブレーキコイルと、
前記固定フレームに取付けられ、前記移動側コアを前記移動側長辺部材の移動方向に沿って移動させて、該移動側コアと該移動側長辺部材との距離を調整する駆動部とを有することを特徴とする電磁ブレーキを搭載した連続鋳造鋳型。 - 請求項1記載の電磁ブレーキを搭載した連続鋳造鋳型において、前記移動側コアの基部に鍔部を設け、前記短辺部材と交換した短辺部材との幅の差分に相当する厚みのライナーを、前記固定フレームと該鍔部の間に形成された隙間に挿入して該移動側コアの位置決めを行うことを特徴とする電磁ブレーキを搭載した連続鋳造鋳型。
- 請求項2記載の電磁ブレーキを搭載した連続鋳造鋳型において、前記両短辺部材を交換する際に移動する前記移動側コアの移動量は、前記ライナーの厚みより大きいことを特徴とする電磁ブレーキを搭載した連続鋳造鋳型。
- 請求項2及び3のいずれか1項に記載の電磁ブレーキを搭載した連続鋳造鋳型において、前記ライナーは、前記鍔部に対向する前記固定フレームの面上に載置され、該固定フレームに取付けられた第2の駆動部を用いて該固定フレームと該鍔部との前記隙間に挿入されることを特徴とする電磁ブレーキを搭載した連続鋳造鋳型。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008061335A JP5074246B2 (ja) | 2008-03-11 | 2008-03-11 | オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008061335A JP5074246B2 (ja) | 2008-03-11 | 2008-03-11 | オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2009214143A JP2009214143A (ja) | 2009-09-24 |
| JP5074246B2 true JP5074246B2 (ja) | 2012-11-14 |
Family
ID=41186581
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2008061335A Active JP5074246B2 (ja) | 2008-03-11 | 2008-03-11 | オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP5074246B2 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP7124647B2 (ja) | 2018-11-02 | 2022-08-24 | 日本製鉄株式会社 | 電磁ブレーキ装置 |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5944211B2 (ja) * | 2012-04-19 | 2016-07-05 | スチールプランテック株式会社 | 連続鋳造設備のモールド可変装置 |
| GB2522873A (en) | 2014-02-07 | 2015-08-12 | Siemens Vai Metals Tech Gmbh | A method of forming tailored cast blanks |
| JP7138495B2 (ja) * | 2018-07-04 | 2022-09-16 | 日鉄エンジニアリング株式会社 | 連続鋳造鋳型 |
| CN113441694A (zh) * | 2021-05-20 | 2021-09-28 | 山东创新金属科技有限公司 | 一种用于铝合金电磁搅拌连续铸锭用的铸造平台 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2987906B2 (ja) * | 1990-09-05 | 1999-12-06 | 日本鋼管株式会社 | 連続鋳造機の組み立てモールド |
| JPH04327343A (ja) * | 1991-04-26 | 1992-11-16 | Kawasaki Steel Corp | 静磁場を印加した連続鋳造におけるモールド幅の変更方法及びその装置 |
| JP3025366B2 (ja) * | 1992-02-03 | 2000-03-27 | 住友重機械工業株式会社 | 連続鋳造機の鋳型ユニット、鋳型構造および鋳型ユニット組換え方法 |
| JP2004106042A (ja) * | 2002-09-20 | 2004-04-08 | Nippon Steel Corp | 連続鋳造用鋳型 |
| JP4404759B2 (ja) * | 2004-12-27 | 2010-01-27 | 新日鉄エンジニアリング株式会社 | 連続鋳造用鋳型 |
-
2008
- 2008-03-11 JP JP2008061335A patent/JP5074246B2/ja active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP7124647B2 (ja) | 2018-11-02 | 2022-08-24 | 日本製鉄株式会社 | 電磁ブレーキ装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2009214143A (ja) | 2009-09-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3046698B1 (en) | Caliper casting device, core and mold used in caliper casting device, caliper for disc brake, and manufacturing method thereof | |
| JP2009214143A (ja) | オンライン短辺交換を行う電磁ブレーキを搭載した連続鋳造鋳型 | |
| EP3046697B1 (en) | Mold used in caliper casting device, caliper casting device, method for manufacturing caliper | |
| JP6596163B2 (ja) | 鋳造機のロールギャップの測定装置 | |
| JP4950720B2 (ja) | 鋳造装置及び鋳造方法 | |
| CA2642355C (en) | Liquid-cooled permanent chill mold for the continuous casting of metals | |
| JP2019089075A (ja) | ダイカスト鋳造装置 | |
| JP2012166423A (ja) | トグルリンク式型締装置のリアプラテン | |
| JP2019005778A (ja) | ダイキャスト用チルベント | |
| JP2010131926A (ja) | 成型用金型および成型用金型の固定方法 | |
| JP4492014B2 (ja) | ダイカスト装置 | |
| JP7739950B2 (ja) | 金型構造 | |
| KR102163553B1 (ko) | 개선된 구조를 갖는 턴디쉬 슬라이드 게이트 장치 | |
| JP5944211B2 (ja) | 連続鋳造設備のモールド可変装置 | |
| JP2972098B2 (ja) | 水平振動鋳型の短辺自立機構 | |
| CN212577439U (zh) | 一种便于快速组装和拆卸的铸造模具 | |
| JP2918145B2 (ja) | 金型の位置決め機構 | |
| JP4404759B2 (ja) | 連続鋳造用鋳型 | |
| JPH11207435A (ja) | 金型の位置決め機構 | |
| JP4829619B2 (ja) | ダイカスト機 | |
| JPWO2012101824A1 (ja) | 鋳造用の消失模型および鋳造品 | |
| KR102265195B1 (ko) | 주조기용 더미장치 | |
| JP2000015417A (ja) | 横型締・縦射出装置 | |
| KR101924029B1 (ko) | 다이캐스팅 금형 | |
| JP4377366B2 (ja) | ツインモールド |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20100929 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20110519 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20120731 |
|
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20120823 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 5074246 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150831 Year of fee payment: 3 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150831 Year of fee payment: 3 |
|
| S533 | Written request for registration of change of name |
Free format text: JAPANESE INTERMEDIATE CODE: R313533 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150831 Year of fee payment: 3 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150831 Year of fee payment: 3 |
|
| S533 | Written request for registration of change of name |
Free format text: JAPANESE INTERMEDIATE CODE: R313533 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150831 Year of fee payment: 3 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| S533 | Written request for registration of change of name |
Free format text: JAPANESE INTERMEDIATE CODE: R313533 |
|
| S533 | Written request for registration of change of name |
Free format text: JAPANESE INTERMEDIATE CODE: R313533 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| S111 | Request for change of ownership or part of ownership |
Free format text: JAPANESE INTERMEDIATE CODE: R313115 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| S111 | Request for change of ownership or part of ownership |
Free format text: JAPANESE INTERMEDIATE CODE: R313111 |
|
| R360 | Written notification for declining of transfer of rights |
Free format text: JAPANESE INTERMEDIATE CODE: R360 |
|
| R360 | Written notification for declining of transfer of rights |
Free format text: JAPANESE INTERMEDIATE CODE: R360 |
|
| R371 | Transfer withdrawn |
Free format text: JAPANESE INTERMEDIATE CODE: R371 |
|
| S111 | Request for change of ownership or part of ownership |
Free format text: JAPANESE INTERMEDIATE CODE: R313111 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |