WO2020002813A1 - Procede de fabrication d'une piece en alliage d'aluminium - Google Patents
Procede de fabrication d'une piece en alliage d'aluminium Download PDFInfo
- Publication number
- WO2020002813A1 WO2020002813A1 PCT/FR2019/051545 FR2019051545W WO2020002813A1 WO 2020002813 A1 WO2020002813 A1 WO 2020002813A1 FR 2019051545 W FR2019051545 W FR 2019051545W WO 2020002813 A1 WO2020002813 A1 WO 2020002813A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- equal
- mass fraction
- less
- layer
- powder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/20—Direct sintering or melting
- B22F10/28—Powder bed fusion, e.g. selective laser melting [SLM] or electron beam melting [EBM]
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/60—Treatment of workpieces or articles after build-up
- B22F10/64—Treatment of workpieces or articles after build-up by thermal means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/24—After-treatment of workpieces or articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B33—ADDITIVE MANUFACTURING TECHNOLOGY
- B33Y—ADDITIVE MANUFACTURING, i.e. MANUFACTURING OF THREE-DIMENSIONAL [3D] OBJECTS BY ADDITIVE DEPOSITION, ADDITIVE AGGLOMERATION OR ADDITIVE LAYERING, e.g. BY 3D PRINTING, STEREOLITHOGRAPHY OR SELECTIVE LASER SINTERING
- B33Y70/00—Materials specially adapted for additive manufacturing
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C32/00—Non-ferrous alloys containing at least 5% by weight but less than 50% by weight of oxides, carbides, borides, nitrides, silicides or other metal compounds, e.g. oxynitrides, sulfides, whether added as such or formed in situ
- C22C32/0047—Non-ferrous alloys containing at least 5% by weight but less than 50% by weight of oxides, carbides, borides, nitrides, silicides or other metal compounds, e.g. oxynitrides, sulfides, whether added as such or formed in situ with carbides, nitrides, borides or silicides as the main non-metallic constituents
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/20—Direct sintering or melting
- B22F10/25—Direct deposition of metal particles, e.g. direct metal deposition [DMD] or laser engineered net shaping [LENS]
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/30—Process control
- B22F10/38—Process control to achieve specific product aspects, e.g. surface smoothness, density, porosity or hollow structures
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/60—Treatment of workpieces or articles after build-up
- B22F10/62—Treatment of workpieces or articles after build-up by chemical means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F10/00—Additive manufacturing of workpieces or articles from metallic powder
- B22F10/60—Treatment of workpieces or articles after build-up
- B22F10/66—Treatment of workpieces or articles after build-up by mechanical means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/24—After-treatment of workpieces or articles
- B22F2003/248—Thermal after-treatment
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/12—Both compacting and sintering
- B22F3/14—Both compacting and sintering simultaneously
- B22F3/15—Hot isostatic pressing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F7/00—Manufacture of composite layers, workpieces, or articles, comprising metallic powder, by sintering the powder, with or without compacting wherein at least one part is obtained by sintering or compression
- B22F7/008—Manufacture of composite layers, workpieces, or articles, comprising metallic powder, by sintering the powder, with or without compacting wherein at least one part is obtained by sintering or compression characterised by the composition
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F7/00—Manufacture of composite layers, workpieces, or articles, comprising metallic powder, by sintering the powder, with or without compacting wherein at least one part is obtained by sintering or compression
- B22F7/06—Manufacture of composite layers, workpieces, or articles, comprising metallic powder, by sintering the powder, with or without compacting wherein at least one part is obtained by sintering or compression of composite workpieces or articles from parts, e.g. to form tipped tools
- B22F7/08—Manufacture of composite layers, workpieces, or articles, comprising metallic powder, by sintering the powder, with or without compacting wherein at least one part is obtained by sintering or compression of composite workpieces or articles from parts, e.g. to form tipped tools with one or more parts not made from powder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B33—ADDITIVE MANUFACTURING TECHNOLOGY
- B33Y—ADDITIVE MANUFACTURING, i.e. MANUFACTURING OF THREE-DIMENSIONAL [3D] OBJECTS BY ADDITIVE DEPOSITION, ADDITIVE AGGLOMERATION OR ADDITIVE LAYERING, e.g. BY 3D PRINTING, STEREOLITHOGRAPHY OR SELECTIVE LASER SINTERING
- B33Y80/00—Products made by additive manufacturing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P10/00—Technologies related to metal processing
- Y02P10/25—Process efficiency
Definitions
- TITLE PROCESS FOR MANUFACTURING AN ALUMINUM ALLOY PART
- the technical field of the invention is a method of manufacturing an aluminum alloy part, using an additive manufacturing technique.
- additive manufacturing techniques have developed. They consist in shaping a part by adding material, which is the opposite of machining techniques, which aim to remove material.
- machining techniques which aim to remove material.
- additive manufacturing is defined, according to French standard XP E67-001, as a "set of processes for manufacturing, layer by layer, by adding material, a physical object from a digital object”.
- ASTM F2792 January 2012 also defines additive manufacturing.
- Different additive manufacturing methods are also defined and described in ISO / ASTM 17296-1.
- the use of additive manufacturing to produce an aluminum part, with low porosity, has been described in document W02015 / 006447.
- the application of successive layers is generally carried out by applying a so-called filler material, then melting or sintering the filler material using an energy source of the laser beam, electron beam type, plasma torch or electric arc.
- each added layer is of the order of a few tens or hundreds of microns.
- a means of additive manufacturing is the melting or sintering of a filler material taking the form of a powder. It can be fusion or sintering by an energy beam.
- selective laser sintering techniques selective laser sintering, SLS or direct metal laser sintering, DMLS
- SLS selective laser sintering
- DMLS direct metal laser sintering
- Another type of metal forming process includes selective laser melting (SLM) or electron beam melting (EBM), in which thermal energy from a laser or directed electron beam is used to selectively melt (rather than sinter) the metal powder so that it fuses as it cools and solidifies.
- LMD laser melting deposition
- Patent application WO2016 / 209652 describes a method for manufacturing aluminum with high mechanical resistance comprising: the preparation of an atomized aluminum powder having one or more approximate powder sizes desired and an approximate morphology; sintering the powder to form a product by additive manufacturing; dissolution; quenching; and the income from additively produced aluminum.
- Patent application US2017 / 0016096 describes a process for manufacturing a part by localized melting, in particular obtained by exposing a powder to an energy beam of electron beam or laser beam type, the powder consisting of 'an aluminum alloy whose copper content is between 5% and 6% by mass, the magnesium content being between 2.5% and 3.5% by mass.
- Patent application EP2796229 discloses a process for forming a metallic aluminum alloy reinforced by dispersion comprising the steps consisting in: obtaining, in powder form, an aluminum alloy composition which is capable of acquiring a dispersion-reinforced microstructure; directing a low energy density laser beam onto a part of the powder having the composition of the alloy; removing the laser beam from the portion of the powdered alloy composition; and cooling the portion of the powdered alloy composition at a speed greater than or equal to about 10 6 ° C per second, thereby forming the dispersion-reinforced aluminum metal alloy.
- the method is particularly suitable for an alloy having a composition according to the following formula: AI C ompFe a SibXc, in which X represents at least one element chosen from the group consisting of Mn, V, Cr, Mo, W, Nb and Ta; "A” ranges from 2.0 to 7.5 atom%; “B” ranges from 0.5 to 3.0 atom%; “C” ranges from 0.05 to 3.5 atom%; and the balance is aluminum and accidental impurities, provided that the ratio [Fe + Si] / Si is in the range of about 2.0: 1 to 5.0: 1.
- Patent application US2017 / 0211168 discloses a process for manufacturing a light and resistant alloy, performing at high temperature, comprising aluminum, silicon, and iron and / or nickel.
- Patent application EP3026135 describes a molding alloy comprising 87 to 99 parts by weight of aluminum and silicon, 0.25 to 0.4 parts by weight of copper and 0.15 to 0.35 parts by weight of a combination of at least two elements among Mg, Ni and Ti. This molding alloy is adapted to be sprayed with an inert gas to form a powder, the powder being used to form an object by additive manufacturing by laser, the object then undergoing a tempering treatment.
- Patent application US2016 / 0138400 describes alloys comprising from 3 to 12% by weight of iron, from 0.1 to 3% by weight of vanadium, from 0.1 to 3% by weight of silicon and from 1 to 6% by weight of copper, aluminum residue and impurities, suitable for additive manufacturing techniques.
- 4xxx alloys (mainly AllOSiMg, AI7SiMg and AI12SÎ) are the most mature aluminum alloys for the SLM application. These alloys offer a very good suitability for the SLM process but suffer from limited mechanical properties.
- the Scalmalloy ® (DE102007018123A1) developed by APWorks offers (with a post-production heat treatment of 4 hours at 325 ° C) good mechanical properties at room temperature.
- this solution suffers from a high cost in powder form linked to its high scandium content ( ⁇ 0.7% Sc) and the need for a specific atomization process.
- This solution also suffers from poor mechanical properties at high temperature, for example greater than 150 ° C.
- the mechanical properties of the aluminum parts obtained by additive manufacturing depend on the alloy forming the filler metal, and more precisely on its composition, on the parameters of the additive manufacturing process as well as on the heat treatments applied.
- the inventors have determined an alloy composition which, used in an additive manufacturing process, makes it possible to obtain parts having remarkable characteristics.
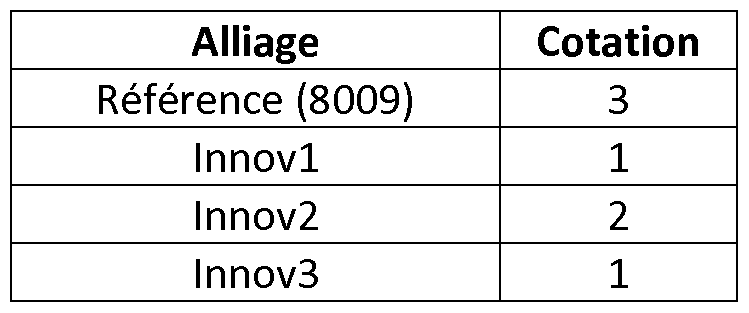
- the parts obtained according to the present invention have improved characteristics compared to the prior art (in particular an 8009 alloy), in particular in terms of surface quality, resistance to hot cracking, or even hot hardness (by example after 4h at 400 ° C).
- a first object of the invention is a method of manufacturing a part comprising the formation of successive solid metal layers, superimposed on each other, each layer describing a pattern defined from a digital model, each layer being formed by the deposition of a metal, called filler metal, the filler metal being subjected to an energy supply so as to melt and to constitute, by solidifying, said layer, in which the filler metal takes the form of a powder, the exposure of which to an energy beam results in a fusion followed by solidification so as to form a solid layer, the method being characterized in that the filler metal is an alloy of aluminum comprising at least the following alloying elements:
- Fe according to a mass fraction of 1% to 15%, preferably 2 to 10%;
- V according to a mass fraction of 0 to 5%, preferably 0.5 to 5%, more
- the alloy according to the present invention also comprises:
- impurities according to a mass fraction of less than 0.05% each (ie 500 ppm) and less than 0.15% in total;
- the alloy can also comprise at least one element chosen from: Mn, Ti, W, Nb, Ta, Y, Yb, Nd, Er, Cr, Zr, Hf, Sc, Ce and / or mischmetal, according to a mass fraction less than or equal to 5%, preferably less than or equal to 3% each, and less than or equal to 15%, preferably less than or equal to 12%, even more preferably less than or equal to 5% in total.
- the addition of Sc is avoided, the preferred mass fraction of Sc then being less than 0.05%, and preferably less than 0.01%.
- the alloy can also comprise at least one element chosen from: Sr, Ba, Sb, Bi, Ca, P, B, In and / or Sn, according to a mass fraction less than or equal to 1%, preferably less than or equal to 0.1%, even more preferably less than or equal to 700 ppm each, and less than or equal to 2%, preferably less than or equal to 1% in total.
- the addition of Bi is avoided, the preferred mass fraction of Bi then being less than 0.05%, and preferably less than 0.01%.
- the alloy can also comprise at least one element chosen from: Ag according to a mass fraction of 0.06 to 1%, Li according to a mass fraction of 0.06 to 1%, Cu according to a mass fraction of 0.06 at 5%, preferably from 0.1 to 2%, Zn according to a mass fraction of 0.06 to 1% and / or Mg according to a mass fraction of 0.06 to 1%.
- these elements can act on the resistance of the material by hardening precipitation or by their effect on the properties of the solid solution.
- the addition of Mg is not recommended and the Mg content is preferably kept below an impurity value of 0.05% by mass.
- the alloy can also comprise at least one compound for refining the grains and avoiding a coarse columnar microstructure, for example AITiC or AITÎB2 (for example in AT5B or AT3B form), in an amount less than or equal to 50 kg / ton, preferably less than or equal to 20 kg / tonne, even more preferably less than or equal to 12 kg / tonne each, and less than or equal to 50 kg / tonne, preferably less than or equal to 20 kg / tonne in total.
- AITiC or AITÎB2 for example in AT5B or AT3B form
- the process can comprise, following the formation of the layers: a dissolution followed by quenching and tempering, or
- a heat treatment typically at a temperature of at least 100 ° C and at most 400 ° C
- CIC hot isostatic compression
- the heat treatment can in particular allow a dimensioning of the residual stresses and / or an additional precipitation of hardening phases.
- CIC treatment can in particular make it possible to improve the elongation properties and the fatigue properties.
- Hot isostatic compression can be performed before, after or in place of the heat treatment.
- the hot isostatic compression is carried out at a temperature of 250 ° C to 550 ° C and preferably from 300 ° C to 450 ° C, at a pressure of 500 to 3000 bars and for a period of 0.5 to 10 hours.
- Heat treatment and / or hot isostatic compression makes it possible in particular to increase the hardness of the product obtained.
- suitable for alloys with structural hardening it is possible to carry out dissolution followed by quenching and tempering of the formed part and / or hot isostatic compression.
- the hot isostatic compression can in this case advantageously replace the dissolution.
- the process according to the invention is advantageous since it preferably does not require a solution treatment followed by quenching. Dissolution can have a detrimental effect on the mechanical resistance in certain cases by participating in a magnification of the dispersoids or of the fine intermetallic phases.
- the method according to the present invention also optionally comprises a machining treatment, and / or a chemical, electrochemical or mechanical surface treatment, and / or a tribofinishing. These treatments can be carried out in particular to reduce the roughness and / or improve the resistance to corrosion and / or improve the resistance to the initiation of fatigue cracks.
- a second object of the invention is a metal part, obtained by a method according to the first object of the invention.
- a third object of the invention is a powder comprising, preferably consisting of, an aluminum alloy comprising at least the following alloying elements:
- Fe according to a mass fraction of 1% to 15%, preferably 2 to 10%;
- V according to a mass fraction of 0 to 5%, preferably 0.5 to 5%, more
- the alloy according to the present invention also comprises:
- impurities according to a mass fraction of less than 0.05% each (ie 500 ppm) and less than 0.15% in total;
- the aluminum alloy of the powder according to the present invention can also comprise:
- Mg is not recommended and the Mg content is preferably kept below an impurity value of 0.05% by mass; and or
- At least one compound chosen to refine the grains and avoid a coarse columnar microstructure for example AITiC or AITÎB2 (for example in AT5B or AT3B form), in an amount less than or equal to 50 kg / tonne, preferably less than or equal at 20 kg / ton, even more preferably lower or equal to 12 kg / tonne each, and less than or equal to 50 kg / tonne, preferably less than or equal to 20 kg / tonne in total.
- Figure 1 is a diagram illustrating an additive manufacturing process of the SLM, or EBM type.
- Figure 2 shows a micrograph of a cross section of an All0Si0.3Mg sample after surface scanning with a laser, cut and polished with two Knoop impressions in the recast layer.
- Figure 1 generally describes an embodiment, in which the additive manufacturing method according to the invention is implemented.
- the filler material 25 is in the form of an alloy powder according to the invention.
- An energy source for example a laser source or an electron source 31, emits an energy beam for example a laser beam or an electron beam 32.
- the energy source is coupled to the filler material by an optical system or electromagnetic lenses 33, the movement of the beam can thus be determined as a function of a digital model M.
- the energy beam 32 follows a movement along the longitudinal plane XY, describing a pattern depending on the digital model M
- the powder 25 is deposited on a support 10. The interaction of the energy beam 32 with the powder 25 generates a selective melting of the latter, followed by solidification, resulting in the formation of a layer 20i ...
- SLM selective laser melting
- EBM electron beam melting
- the layer is obtained by selective laser sintering (selective laser sintering, SLS or direct metal laser sintering, DMLS), the layer of alloy powder according to the invention being selectively sintered according to the chosen digital model with thermal energy supplied by a laser beam.
- selective laser sintering selective laser sintering, SLS or direct metal laser sintering, DMLS
- the powder is sprayed and melted simultaneously by a generally laser beam. This process is known as laser melting deposition.
- Direct Energy Deposition Direct Energy Deposition
- Direct Metal deposition Direct Métal Déposition, DMD
- Direct Laser Déposition Direct Laser Déposition
- LDT laser deposition technology
- LENS metal deposition by laser
- LCT laser plating technology
- LCT Laser Freeform Manufacturing Technology
- the method according to the invention is used for the production of a hybrid part comprising a part 10 obtained by conventional methods of rolling and / or spinning and / or molding and / or forging optionally followed machining and an integral part 20 obtained by additive manufacturing.
- This embodiment can also be suitable for repairing parts obtained by conventional methods.
- the metal parts obtained by the process according to the invention are particularly advantageous because they have smooth surfaces and do not exhibit hot cracking.
- they have a hardness in the raw state of manufacture lower than that of a reference in 8009, and at the same time a hardness after a heat treatment greater than that of a reference in 8009.
- the hardness of the alloys according to the present invention decreases less between the raw state of manufacture and the state after a heat treatment.
- the lower hardness in the raw state of manufacture of the alloys according to the present invention compared to an alloy 8009 is considered to be advantageous for the suitability for the SLM process, by inducing a lower level of stresses during the SLM manufacture and thus lower sensitivity to hot cracking.
- the higher hardness after a heat treatment (for example 1 h at 400 ° C.) of the alloys according to the present invention compared to an alloy 8009 provides better thermal stability.
- the heat treatment could be a post isostatic hot compressions (CIC) post manufacturing SLM.
- CIC post isostatic hot compressions
- the Knoop hardness 10g in the raw state for manufacturing the metal parts obtained according to the present invention is preferably from 150 to 350 HK, more preferably from 200 to 340 HK.
- the Knoop hardness 10g of the metal parts obtained according to the present invention after a heat treatment of at least 100 ° C and at most 550 ° C and / or isostatic hot compression, is 150 to 300 HK, more preferably from 160 to 250 HK.
- the Knoop hardness measurement method is described in the examples below.
- average particle size 10 to 100 ⁇ m, preferably 20 to 60 ⁇ m;
- the sphericity of a powder can for example be determined using a morphogranulometer
- the flowability of a powder can for example be determined according to standard ASTM B213;
- the porosity preferably from 0 to 5%, more preferably from 0 to 2%, even more preferably from 0 to 1% by volume.
- the porosity can in particular be determined by scanning electron microscopy or by helium pycnometry (see standard ASTM B923);
- the powder according to the present invention can be obtained by conventional methods of atomization from an alloy according to the invention in liquid or solid form or, alternatively, the powder can be obtained by mixing primary powders before exposure to energy beam, the different compositions of the primary powders having an average composition corresponding to the composition of the alloy according to the invention.
- infusible, insoluble particles for example oxides or T1B2 particles or carbon particles
- primary powders These particles can be used to refine the microstructure. They can also be used to harden the alloy if they are nanometric in size. These particles can be present in a volume fraction of less than 30%, preferably less than 20%, more preferably less than 10%.
- the powder according to the present invention can be obtained for example by atomization by gas jet, plasma atomization, atomization by water jet, atomization by ultrasound, atomization by centrifugation, electrolysis and spheroidization, or grinding and spheroidization.
- the powder according to the present invention is obtained by atomization by gas jet.
- the gas jet atomization process begins with the casting of molten metal through a nozzle.
- the molten metal is then reached by jets of neutral gases, such as nitrogen or argon, and atomized into very small droplets which cool and solidify as they fall inside an atomization tower .
- the powders are then collected in a can.
- the gas jet atomization process has the advantage of producing a powder having a spherical shape, unlike water jet atomization which produces a powder having an irregular shape.
- Another advantage of atomization by gas jet is a good powder density, in particular thanks to the spherical shape and the distribution of particle size. Yet another advantage of this method is good reproducibility of the particle size distribution.
- the powder according to the present invention can be steamed, in particular in order to reduce its humidity.
- the powder can also be packaged and stored between its manufacture and its use.
- the powder according to the present invention can in particular be used in the following applications:
- direct metal sintering by laser Direct Métal Laser Sintering or DMLS in English
- Selective sintering by heating Selective Heat Sintering or SHS
- SLM Selective laser melting
- EBM Electro Beam Melting
- DED direct energy deposition
- DLD direct laser deposition
- LDT Laser Deposition Technology
- LFMT laser freeform manufacturing technology
- Induthem VC 650V to obtain ingots 130 mm high, 95 mm wide and 5 mm thick.
- the composition of the alloys, obtained by ICP, is given as a percentage by mass fraction in Table 1 below.
- the refining compound AT5B was added to the alloys Innovl and lnnov2, according to an amount of
- the alloys as described in table 1 above were tested by a rapid prototyping method. Samples were machined for scanning the surface with a laser, in the form of discs 5 mm thick and 27 mm in diameter, from the ingots obtained above. The discs were placed in an SLM machine and scans of the surface were performed with a laser following the same scanning strategy and process conditions representative of those used for the SLM process. It has in fact been found that it is possible in this way to assess the suitability of the alloys for the SLM process and in particular the surface quality, the sensitivity to hot cracking, the hardness in the raw state and the hardness. after heat treatment.
- the metal melts in a bath 10 to 350 ⁇ m thick. After the laser has passed, the metal cools quickly as in the SLM process. After the laser scanning, a thin surface layer 10 to 350 ⁇ m thick was melted and then solidified. The properties of the metal in this layer are close to the properties of the metal at the heart of a part manufactured by SLM, because the scanning parameters are judiciously chosen.
- the laser scanning of the surface of the different samples was carried out using a selective laser fusion machine PM100 from Phoenix Systems.
- the laser source had a power of 200 W, the manufacturing temperature was 200 ° C, the vector deviation was 50 ⁇ m and the diameter of the beam was 60 to 80 ⁇ m. Two different scanning speeds were tested for each sample: 600 mm / s and 900 mm / s.
- Hardness is an important property for alloys. Indeed, if the hardness in the layer remelted by scanning the surface with a laser is high, a part manufactured with the same alloy will potentially have a high breaking limit.
- the hardness was measured according to the Knoop scale with a load of 10 g after laser treatment (in the raw state) and after an additional heat treatment at 400 ° C for 4 h, allowing in particular to evaluate the suitability of the alloy for hardening during a heat treatment and the effect of a possible CIC treatment on the mechanical properties.
- the alloys according to the present invention showed a Knoop hardness 10 g in the raw state less than that of alloy 8009, but, after 4 h at 400 ° C., greater than that of alloy 8009 reference. Without being bound by theory, it is assumed that the higher hardness after 4 hours at 400 ° C is very probably associated with a slower coagulation kinetics of the dispersoids (better thermal stability).
- Ingots cast from the compositions described in Table 1 above were atomized by the UTBM (University of Technology of Belfort Montbéliard) to obtain a powder by atomization by gas jet (method described above).
- the particle size analysis of the powders obtained was carried out by laser diffraction using a Malvern Mastersizer 2000 granulometer according to standard ISO 13320.
- the curve describing the evolution of the volume fraction as a function of the diameter of the particles forming the powder described generally a distribution comparable to a Gaussian distribution. Dio, D 5 o and Dgo are generally called the 10%, 50% (median) and 90% of the distribution obtained, respectively.
- the porosity could be improved by optimizing the process, or even with a post-fabrication treatment of the CIC type (hot isostatic compression).
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Plasma & Fusion (AREA)
- Crystallography & Structural Chemistry (AREA)
- Powder Metallurgy (AREA)
Abstract
Description




Claims
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201980042797.2A CN112352061A (zh) | 2018-06-25 | 2019-06-24 | 制造铝合金零件的方法 |
| EP19742879.0A EP3810817B1 (fr) | 2018-06-25 | 2019-06-24 | Procede de fabrication d'une piece en alliage d'aluminium |
| JP2020569780A JP7386819B2 (ja) | 2018-06-25 | 2019-06-24 | アルミニウム合金からなる部品の製造方法 |
| CA3102419A CA3102419A1 (fr) | 2018-06-25 | 2019-06-24 | Procede de fabrication d'une piece en alliage d'aluminium |
| US17/253,393 US20210260661A1 (en) | 2018-06-25 | 2019-06-24 | Process for manufacturing an aluminium alloy part |
| KR1020207037117A KR20210023882A (ko) | 2018-06-25 | 2019-06-24 | 알루미늄 합금 부품 제조 방법 |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR1870745 | 2018-06-25 | ||
| FR1870745A FR3082763A1 (fr) | 2018-06-25 | 2018-06-25 | Procede de fabrication d une piece en alliage d aluminium |
| FR1871131 | 2018-10-05 | ||
| FR1871131A FR3082764B1 (fr) | 2018-06-25 | 2018-10-05 | Procede de fabrication d'une piece en alliage d'aluminium |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020002813A1 true WO2020002813A1 (fr) | 2020-01-02 |
Family
ID=67402959
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/FR2019/051545 Ceased WO2020002813A1 (fr) | 2018-06-25 | 2019-06-24 | Procede de fabrication d'une piece en alliage d'aluminium |
Country Status (1)
| Country | Link |
|---|---|
| WO (1) | WO2020002813A1 (fr) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113528901A (zh) * | 2021-07-20 | 2021-10-22 | 重庆增隆新材料科技有限公司 | 一种增材制造用耐热铝合金球形粉体材料及其制备方法 |
| CN114277272A (zh) * | 2021-12-27 | 2022-04-05 | 上海耀鸿科技股份有限公司 | 铝合金改性用复合稀土合金及其制备方法 |
| CN114395704A (zh) * | 2021-12-24 | 2022-04-26 | 安顺学院 | 一种利用热等静压技术提高铝合金铸件致密度的方法 |
| CN115443199A (zh) * | 2020-05-13 | 2022-12-06 | 肯联铝业技术中心 | 制造铝合金零件的方法 |
| CN115747579A (zh) * | 2022-10-25 | 2023-03-07 | 安徽中科春谷激光产业技术研究院有限公司 | 一种高强韧增材制造铝合金材料及其制备方法 |
Citations (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01149935A (ja) * | 1987-12-07 | 1989-06-13 | Furukawa Alum Co Ltd | 耐熱性アルミニウム合金粉末成形体及びその製造方法 |
| JPH01319644A (ja) * | 1988-06-18 | 1989-12-25 | Furukawa Alum Co Ltd | 耐熱性アルミニウム合金材及びその製造方法 |
| JPH03232949A (ja) * | 1990-02-07 | 1991-10-16 | Furukawa Alum Co Ltd | アルミニウム合金制振材料の製造方法 |
| JPH0813074A (ja) * | 1994-07-04 | 1996-01-16 | Toyota Motor Corp | アルミ基摺動部材 |
| JPH08143999A (ja) * | 1994-11-22 | 1996-06-04 | Mitsubishi Materials Corp | 高温強度および高温延性に優れたAl合金粉末熱間鍛造部材 |
| JPH116024A (ja) * | 1997-06-18 | 1999-01-12 | Sumitomo Metal Ind Ltd | 耐摩耗性に優れたアルミニウム合金複合材料 |
| JP2007039748A (ja) * | 2005-08-03 | 2007-02-15 | Kobe Steel Ltd | 耐熱性Al基合金 |
| JP2008261004A (ja) * | 2007-04-11 | 2008-10-30 | Sumitomo Denko Shoketsu Gokin Kk | アルミニウム合金 |
| DE102007018123A1 (de) | 2007-04-16 | 2008-10-30 | Eads Deutschland Gmbh | Verfahren zur Herstellung eines Strukturbauteils aus einer Aluminiumbasislegierung |
| EP2796229A1 (fr) | 2013-03-13 | 2014-10-29 | Honeywell International Inc. | Procédés pour former des alliages d'aluminium renforcés par dispersion |
| WO2015006447A1 (fr) | 2013-07-10 | 2015-01-15 | Alcoa Inc. | Procédés de production de produits forgés et d'autres produits travaillés |
| US20160138400A1 (en) | 2014-11-17 | 2016-05-19 | Alcoa Inc. | Aluminum alloys having iron, silicon, vanadium and copper |
| EP3026135A1 (fr) | 2014-11-21 | 2016-06-01 | Industrial Technology Research Institute | Matériau de moulage d'alliage et procédé de fabrication d'un objet en alliage |
| WO2016209652A1 (fr) | 2015-06-15 | 2016-12-29 | Northrop Grumman Systems Corporation | Aluminium à haute résistance fabriqué par impression tridimensionnelle par l'intermédiaire de procédés laser à lit de poudre |
| US20170016096A1 (en) | 2015-07-16 | 2017-01-19 | Hamilton Sundstrand Corporation | Method of manufacturing aluminum alloy articles |
| US20170211168A1 (en) | 2016-01-27 | 2017-07-27 | GM Global Technology Operations LLC | Rapidly solidified high-temperature aluminum iron silicon alloys |
| US20180080103A1 (en) * | 2016-09-19 | 2018-03-22 | Ut-Battelle, Llc | Additive manufacturing methods using aluminum-rare earth alloys and products made using such methods |
-
2019
- 2019-06-24 WO PCT/FR2019/051545 patent/WO2020002813A1/fr not_active Ceased
Patent Citations (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01149935A (ja) * | 1987-12-07 | 1989-06-13 | Furukawa Alum Co Ltd | 耐熱性アルミニウム合金粉末成形体及びその製造方法 |
| JPH01319644A (ja) * | 1988-06-18 | 1989-12-25 | Furukawa Alum Co Ltd | 耐熱性アルミニウム合金材及びその製造方法 |
| JPH03232949A (ja) * | 1990-02-07 | 1991-10-16 | Furukawa Alum Co Ltd | アルミニウム合金制振材料の製造方法 |
| JPH0813074A (ja) * | 1994-07-04 | 1996-01-16 | Toyota Motor Corp | アルミ基摺動部材 |
| JPH08143999A (ja) * | 1994-11-22 | 1996-06-04 | Mitsubishi Materials Corp | 高温強度および高温延性に優れたAl合金粉末熱間鍛造部材 |
| JPH116024A (ja) * | 1997-06-18 | 1999-01-12 | Sumitomo Metal Ind Ltd | 耐摩耗性に優れたアルミニウム合金複合材料 |
| JP2007039748A (ja) * | 2005-08-03 | 2007-02-15 | Kobe Steel Ltd | 耐熱性Al基合金 |
| JP2008261004A (ja) * | 2007-04-11 | 2008-10-30 | Sumitomo Denko Shoketsu Gokin Kk | アルミニウム合金 |
| DE102007018123A1 (de) | 2007-04-16 | 2008-10-30 | Eads Deutschland Gmbh | Verfahren zur Herstellung eines Strukturbauteils aus einer Aluminiumbasislegierung |
| EP2796229A1 (fr) | 2013-03-13 | 2014-10-29 | Honeywell International Inc. | Procédés pour former des alliages d'aluminium renforcés par dispersion |
| WO2015006447A1 (fr) | 2013-07-10 | 2015-01-15 | Alcoa Inc. | Procédés de production de produits forgés et d'autres produits travaillés |
| US20160138400A1 (en) | 2014-11-17 | 2016-05-19 | Alcoa Inc. | Aluminum alloys having iron, silicon, vanadium and copper |
| EP3026135A1 (fr) | 2014-11-21 | 2016-06-01 | Industrial Technology Research Institute | Matériau de moulage d'alliage et procédé de fabrication d'un objet en alliage |
| WO2016209652A1 (fr) | 2015-06-15 | 2016-12-29 | Northrop Grumman Systems Corporation | Aluminium à haute résistance fabriqué par impression tridimensionnelle par l'intermédiaire de procédés laser à lit de poudre |
| US20170016096A1 (en) | 2015-07-16 | 2017-01-19 | Hamilton Sundstrand Corporation | Method of manufacturing aluminum alloy articles |
| US20170211168A1 (en) | 2016-01-27 | 2017-07-27 | GM Global Technology Operations LLC | Rapidly solidified high-temperature aluminum iron silicon alloys |
| US20180080103A1 (en) * | 2016-09-19 | 2018-03-22 | Ut-Battelle, Llc | Additive manufacturing methods using aluminum-rare earth alloys and products made using such methods |
Non-Patent Citations (4)
| Title |
|---|
| "Characterization of AI-Fe-V-Si heat-resistant aluminum alloy components fabricated by selective laser melting", JOURNAL OF MATERIAL RESEARCH, vol. 30, no. 10, 28 May 2015 (2015-05-28) |
| "Microstructure and mechanical properties of AI-Fe-V-Si aluminum alloy produced by electron beam melting", MATERIALS SCIENCE&ENGINEERING A, vol. 659, 2016, pages 207 - 214 |
| A. L. GREER: "Grain refinement of alloys by inoculation of melts", ROYAL SOCIETY OF LONDON. PHILOSOPHICAL TRANSACTIONS A. MATHEMATICAL, PHYSICAL AND ENGINEERING SCIENCES, vol. 361, no. 1804, 28 January 2003 (2003-01-28), UK, pages 479 - 495, XP055571848, ISSN: 1471-2962, DOI: 10.1098/rsta.2002.1147 * |
| J Q WANG ET AL: "Effect of rare-earth elements on the microstructural characterization in rapidly quenched thermally strengthened aluminium alloys", JOURNAL OF MATERIALS SCIENCE, vol. 33, no. 2, 31 January 1998 (1998-01-31), Dordrecht, pages 497 - 505, XP055568035, ISSN: 0022-2461, DOI: 10.1023/A:1004352704113 * |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115443199A (zh) * | 2020-05-13 | 2022-12-06 | 肯联铝业技术中心 | 制造铝合金零件的方法 |
| CN113528901A (zh) * | 2021-07-20 | 2021-10-22 | 重庆增隆新材料科技有限公司 | 一种增材制造用耐热铝合金球形粉体材料及其制备方法 |
| CN113528901B (zh) * | 2021-07-20 | 2022-03-29 | 重庆增隆新材料科技有限公司 | 一种增材制造用耐热铝合金球形粉体材料及其制备方法 |
| CN114395704A (zh) * | 2021-12-24 | 2022-04-26 | 安顺学院 | 一种利用热等静压技术提高铝合金铸件致密度的方法 |
| CN114277272A (zh) * | 2021-12-27 | 2022-04-05 | 上海耀鸿科技股份有限公司 | 铝合金改性用复合稀土合金及其制备方法 |
| CN115747579A (zh) * | 2022-10-25 | 2023-03-07 | 安徽中科春谷激光产业技术研究院有限公司 | 一种高强韧增材制造铝合金材料及其制备方法 |
| CN115747579B (zh) * | 2022-10-25 | 2024-02-02 | 安徽中科春谷激光产业技术研究院有限公司 | 一种高强韧增材制造铝合金材料及其制备方法 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3860788B1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium et une poudre d'alliage d'aluminium | |
| EP3622095B1 (fr) | Piece en alliage d'aluminium et son procédé de fabrication | |
| FR3083479A1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium | |
| EP3860787B1 (fr) | Procédé de fabrication d'une pièce en alliage d'aluminium | |
| EP3810817B1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium | |
| EP3924124B1 (fr) | Procédé de fabrication d'une pièce en alliage d'aluminium | |
| FR3077524A1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium et de chrome | |
| WO2020152427A1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium, l'alliage comportant au moins du zirconium et du magnesium | |
| FR3083478A1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium | |
| EP4149703B1 (fr) | Procédé de fabrication d'une pièce en alliage d'aluminium | |
| WO2021156583A2 (fr) | Procédé de fabrication d'une pièce en alliage d'aluminium | |
| FR3139018A1 (fr) | Procédé de fabrication d'une pièce en alliage d'aluminium | |
| EP4536425A1 (fr) | Procede de fabrication d'une piece en alliage d'aluminium |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 19742879 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 3102419 Country of ref document: CA |
|
| ENP | Entry into the national phase |
Ref document number: 2020569780 Country of ref document: JP Kind code of ref document: A |
|
| ENP | Entry into the national phase |
Ref document number: 20207037117 Country of ref document: KR Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2019742879 Country of ref document: EP Effective date: 20210125 |
|
| WWG | Wipo information: grant in national office |
Ref document number: 2019742879 Country of ref document: EP |