EP0170539A1 - Verfahren und Vorrichtung zum Fertigen von kalibrierten Röhren aus Pappe mit sehr kleiner Oberflächenrauheit und hoher Ausmassstabilität - Google Patents
Verfahren und Vorrichtung zum Fertigen von kalibrierten Röhren aus Pappe mit sehr kleiner Oberflächenrauheit und hoher Ausmassstabilität Download PDFInfo
- Publication number
- EP0170539A1 EP0170539A1 EP85401079A EP85401079A EP0170539A1 EP 0170539 A1 EP0170539 A1 EP 0170539A1 EP 85401079 A EP85401079 A EP 85401079A EP 85401079 A EP85401079 A EP 85401079A EP 0170539 A1 EP0170539 A1 EP 0170539A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- sanding
- station
- coating
- sections
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 20
- 239000011111 cardboard Substances 0.000 title claims abstract description 13
- 239000011248 coating agent Substances 0.000 claims abstract description 35
- 238000000576 coating method Methods 0.000 claims abstract description 35
- 229920005989 resin Polymers 0.000 claims abstract description 22
- 239000011347 resin Substances 0.000 claims abstract description 22
- 238000007906 compression Methods 0.000 claims abstract description 15
- 230000006835 compression Effects 0.000 claims abstract description 15
- 229920001187 thermosetting polymer Polymers 0.000 claims abstract description 14
- 238000004804 winding Methods 0.000 claims abstract description 13
- 238000004519 manufacturing process Methods 0.000 claims abstract description 11
- 239000000463 material Substances 0.000 claims abstract description 11
- 238000005520 cutting process Methods 0.000 claims abstract description 10
- 238000005498 polishing Methods 0.000 claims abstract description 10
- 238000001035 drying Methods 0.000 claims abstract description 7
- 230000003746 surface roughness Effects 0.000 claims abstract description 5
- 238000005507 spraying Methods 0.000 claims description 9
- 239000003054 catalyst Substances 0.000 claims description 4
- 239000000428 dust Substances 0.000 claims description 3
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 3
- 238000001816 cooling Methods 0.000 claims 1
- 241001672694 Citrus reticulata Species 0.000 abstract 1
- 239000010408 film Substances 0.000 description 4
- 238000007792 addition Methods 0.000 description 3
- 239000007921 spray Substances 0.000 description 3
- KXGFMDJXCMQABM-UHFFFAOYSA-N 2-methoxy-6-methylphenol Chemical compound [CH]OC1=CC=CC([CH])=C1O KXGFMDJXCMQABM-UHFFFAOYSA-N 0.000 description 2
- 239000000123 paper Substances 0.000 description 2
- 239000005011 phenolic resin Substances 0.000 description 2
- 229920001568 phenolic resin Polymers 0.000 description 2
- 238000006116 polymerization reaction Methods 0.000 description 2
- 238000005096 rolling process Methods 0.000 description 2
- 239000012080 ambient air Substances 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 238000007731 hot pressing Methods 0.000 description 1
- 238000005470 impregnation Methods 0.000 description 1
- 239000002655 kraft paper Substances 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 239000011087 paperboard Substances 0.000 description 1
- 229920000728 polyester Polymers 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 239000004576 sand Substances 0.000 description 1
- 230000000087 stabilizing effect Effects 0.000 description 1
- 238000010025 steaming Methods 0.000 description 1
- 239000010409 thin film Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31C—MAKING WOUND ARTICLES, e.g. WOUND TUBES, OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31C3/00—Making tubes or pipes by feeding obliquely to the winding mandrel centre line
Definitions
- the invention relates to a method and a device for manufacturing a calibrated cardboard tube with very low surface roughness and high dimensional stability.
- This type of machine comprises a fixed cylindrical mandrel on which are wound in a helix one or more strips previously glued, with the exception of the first, and which make determined angles with the axis of said mandrel, the formed tube being driven. in rotation and simultaneously in longitudinal translation, by an endless belt making a dead turn around said formed tube.
- Each cardboard tube thus continuously produced is then cut during its formation into unitary tubes, in a cutting or cutting-off station.
- Patent FR 1563024 and its additions to the name of the applicant do not solve all of these problems.
- the aforementioned patent recommends a method of manufacturing a tube which is remarkable in that on a raw tube, made of in a conventional manner, there is wound up a glued strip of a compressible material of low density, such as felt cardboard, intended to form the penultimate fold, then a strip of dense material, intended to form the last fold, sand and coat the outer surface of said last ply with a thermosetting resin and, finally, after cutting and steaming, passing each section of tube through a heated die, so as to simultaneously obtain the calibration, by crushing from the front -last compressible fold, and polymerization of the resin coating.
- a compressible material of low density such as felt cardboard
- the sanding operation can be avoided by a preparation and a particular bonding of the last ply
- the second addition describes other hot compression means than the die described in the patent. main and further specifies a possibility of eliminating the external coating of resin using a last porous ply and bonded to the penultimate ply by means of a thermosetting resin.
- At least the penultimate ply is chamfered in parallel on its two longitudinal edges, so that the chamfers of two consecutive turns of this ply overlap.
- the edge of the last fold opposite to the direction of advancement of the tube is in a known manner chamfered so that this edge is covered by the straight edge of the next turn.
- the method according to the invention recommends a first narrow sanding of the outside surface of the raw tube, intended 4 to remove the edge formed by the clear edge of the last ply, followed by a second wider sanding intended to felect the material of said last ply.
- the last coating is carried out by a simultaneous double spraying, on the one hand of the resin and, on the other hand, of a catalyst.
- the invention also relates to a device for the implementation of this method comprising in particular a spiraling machine for the manufacture of continuous tubes, a station for sanding the tube, a resin coating station, a cutting station, a drying of the sections and a transverse compression station of said sections, a remarkable device in that it further comprises, downstream of the compression station, a station for coating the sections, followed by a flexible polishing or sanding station.
- the section coating station is preceded by a section sanding station.
- the tube sanding station has a first narrow sanding means for the tube, followed by another wider sanding means, while the tube coating station has at least two coating means per bath and / or spray.
- the invention obviously relates to a tube manufactured according to the above-mentioned process and / or by means of its implementation device.
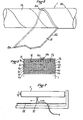
- FIG. 1 we can see a raw tube 1 which is manufactured in a known manner by a spiraling machine 2 intended to wind helically a plurality of strips glued around a mandrel 3, the raw tube being driven in translation according to arrow F and in rotation by an endless belt device 4.
- the spiring machine 2 is equipped with a cutting station 5 intended to form several sections of tube such as 1 1 in FIGS. 1,4 and 5,6.
- the first "folds" of the tube formed by the first coiled bands 6a to 6i are here with almost contiguous turns (Figure 3) while the antepenultimate band 7a and the penultimate band 7b intended to constitute the corresponding plies are chamfered on their two longitudinal edges so that the chamfers 7'a and 7'b ( Figure 3) of two consecutive turns of each of these plies overlap.
- One or more of the bands 6a to 6i could also be chamfered like the bands 7a and 7b.
- edge 8a of the strip 8 forming the last fold and which is opposite to the direction F of the advancement is chamfered on its face facing outwards so that this edge 8a is covered by the straight edge 8b of the next turn ( Figures 1 to 3).
- the first folds of the tube formed by the strips 6a to 6i are for example made of kraft cardboard while the last fold, the penultimate and the antepenultimate are made by Lar: respectively 8, 7b, 7a of a long fiber and dense material such as paper d 'impregnation, the strip 8 being slightly wider.
- the strips 7a and 7b are further impregnated, before winding, with a thermosetting resin, such as a phenolic resin, by means for example of devices provided on the reels on which said strips are stored and unwound.
- a thermosetting resin such as a phenolic resin
- the embodiment described comprises only two impregnated strips 7a and 7b, but preferably this number is higher.
- a sanding station 9 consisting of a first means 9a with a narrow sanding belt and a second means 9b with a wider sanding belt.
- the first means 9a is intended to eliminate the edge formed by the frank edge 8b of the outer ply while the means 9b is intended to felt the material of said last ply.
- the sanding station is followed by a coating station 10, constituted here by two tanks 10a and 10b filled with a mixture containing a phenolic resin.
- the number of tanks may of course be different, as may the nature of the coating station (spraying for example).
- each section is dried in depth before being worked in a die apparatus shown in FIG. 4.
- the apparatus of FIG. 4 comprises a frame 11 provided with a hydraulic cylinder 12 and coaxially a die 13.
- the rod 14 of the actuator 12 is provided with a head 15 intended to push one of the ends of each section of tube introduced into a cylindrical core 16 of the die 13;
- the cylindrical core 16 is surrounded by a sealed envelope 17 in which a heated fluid circulates, so that the temperature of the core 16 of the die corresponds to the polymerization temperature of the resin used in station 10 in FIG. 1.
- This sanding station includes a flexible abrasive belt 18, the tension of which is adjustable and which is applied to the working section arranged on motorized support rollers 19.
- the rollers 19 are also orientable with respect to the axis of the tube section so that they can impart to the latter a rotational movement and a translational movement.
- Sanding is usually done in a slow back and forth, so as to cross the steps.
- This sanding is to improve the bonding of the last coating while also improving the surface condition.
- a spray gun 21 is arranged for example on a rod 22 parallel to the axis of the sections and on which it is moved in translation so as to be able to come and go at a constant speed, so as to homogenize and regularize the coating.
- the gun 21 is supplied with a thermosetting resin, for example polyester.
- a catalyst is mixed with said resin and preferably, two guns or a two-headed gun are used so as to spray the resin and the catalyst at the same time.
- This spraying is generally done on a round trip of the gun (to cross the steps).
- the sections thus coated are then dried in ambient air or in an oven, each section being arranged in a vertical position.
- the buffing is carried out after closing the ends of the section and under spraying with water so as to cool the section and entrain the dust.
- the last coating makes it possible to obtain a surface of homogeneous and permanent hardness and low roughness, only thanks to the fact that the preliminary operations described above already make it possible to obtain a hard undercoat on a tube or section of tube. whose geometry is also stabilized as already specified.
Landscapes
- Making Paper Articles (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Laminated Bodies (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR8410498A FR2567069B1 (fr) | 1984-07-03 | 1984-07-03 | Procede et dispositif de fabrication d'un tube de carton calibre a tres faible rugosite de surface et haute stabilite dimensionnelle |
| FR8410498 | 1984-07-03 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0170539A1 true EP0170539A1 (de) | 1986-02-05 |
| EP0170539B1 EP0170539B1 (de) | 1987-12-16 |
Family
ID=9305722
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP85401079A Expired EP0170539B1 (de) | 1984-07-03 | 1985-05-31 | Verfahren und Vorrichtung zum Fertigen von kalibrierten Röhren aus Pappe mit sehr kleiner Oberflächenrauheit und hoher Ausmassstabilität |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US4645553A (de) |
| EP (1) | EP0170539B1 (de) |
| JP (1) | JPH0628930B2 (de) |
| DE (1) | DE3561187D1 (de) |
| ES (1) | ES8609032A1 (de) |
| FR (1) | FR2567069B1 (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2623439A1 (fr) * | 1987-11-19 | 1989-05-26 | Auxerroise Cartonnages | Procede de fabrication de tube en carton a roulage parallele ou spirale |
| EP0343601A3 (de) * | 1988-05-26 | 1991-12-18 | Mitsuya Tekko Co., Ltd. | Vorrichtung zum Herstellen von Rohren |
| CN102922779A (zh) * | 2012-11-16 | 2013-02-13 | 金红叶纸业集团有限公司 | 纸管成型装置 |
Families Citing this family (24)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2589384B1 (fr) * | 1985-10-30 | 1988-01-22 | Lhomme Sa | Dispositif de tronconnage de tubes |
| JP2620857B2 (ja) * | 1987-05-20 | 1997-06-18 | 光洋精工株式会社 | 磁気軸受装置における保護用ラジアル玉軸受 |
| DE3742027A1 (de) * | 1987-12-11 | 1989-06-22 | Varta Batterie | Isolationshuelse fuer galvanische primaerelemente |
| FI87898C (fi) * | 1988-04-25 | 1993-03-10 | Lhomme Sa | Anordning foer kapning av roer |
| US5393582A (en) * | 1993-06-04 | 1995-02-28 | Sonoco Products Company | Enhanced crush strength construction multi-grade paperboard tubes |
| US5799705A (en) * | 1995-10-25 | 1998-09-01 | Ameron International Corporation | Fire resistant pipe |
| JPH10512357A (ja) * | 1995-10-25 | 1998-11-24 | アメロン インターナショナル コーポレイション | 耐火性パイプ |
| FR2764277B1 (fr) * | 1997-06-06 | 1999-09-10 | Alain Boyer | Cylindre rotatif a faible inertie de masse |
| US6309717B1 (en) * | 1998-10-27 | 2001-10-30 | Sonoco Development, Inc. | Composite paperboard containers of optimized axial strength construction |
| US6889715B2 (en) * | 2002-11-27 | 2005-05-10 | Wellstream International Limited | Flexible tubular member with sealed tape layer |
| CN100341691C (zh) * | 2004-07-15 | 2007-10-10 | 杭州保力洁包装有限公司 | 一种纸管的制作方法 |
| US7824595B2 (en) * | 2004-08-13 | 2010-11-02 | Perma-Pipe, Inc. | Method and system for cast molding a fluid conduit |
| US7703480B1 (en) * | 2005-08-01 | 2010-04-27 | Hillerich & Bradsby Co. | Composite tubes and method of manufacturing same |
| US20080072988A1 (en) * | 2006-08-22 | 2008-03-27 | Perma-Pipe, Inc. | Glass Syntactic Polyurethane Insulated Product |
| ITFI20070230A1 (it) * | 2007-10-22 | 2009-04-23 | Perini Fabio Spa | "tubiera con un supporto magnetico per il mandrino avvolgitore" |
| US8153541B2 (en) * | 2008-06-17 | 2012-04-10 | Century, Inc. | Ceramic article |
| US20110057069A1 (en) * | 2009-09-09 | 2011-03-10 | Sonoco Development, Inc. | Coated Paperboard Core For Elastomeric Fiber Production |
| CH702191A1 (de) | 2009-11-04 | 2011-05-13 | Alstom Technology Ltd | Geschweisster Rotor. |
| US9283734B2 (en) | 2010-05-28 | 2016-03-15 | Gunite Corporation | Manufacturing apparatus and method of forming a preform |
| CN103506921A (zh) * | 2013-05-21 | 2014-01-15 | 吴江市美晟机械设备有限公司 | 纸管打磨机 |
| RU2657693C2 (ru) * | 2014-01-29 | 2018-06-14 | Футура С.П.А. | Оборудование и способ изготовления картонных трубок |
| CN104129101B (zh) * | 2014-07-11 | 2016-09-07 | 绍兴市天时纸业有限公司 | 一种全自动宝塔纸管机 |
| MX2019008279A (es) | 2017-03-02 | 2019-09-09 | Abzac Canada Inc | Sistema y metodo no destructivo y sin contacto en linea para detectar defectos en estructura de carton en movimiento. |
| CN107964831A (zh) * | 2017-12-05 | 2018-04-27 | 绍兴科恩士纸管有限公司 | 一种纸管的生产设备及其生产方法 |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3002433A (en) * | 1958-01-10 | 1961-10-03 | Sonoco Products Co | Spiral wound paper tube having seamless outer surface |
| CH359594A (de) * | 1958-05-19 | 1962-01-15 | Sonoco Products Co | Mehrschichtiges Papierrohr, Verfahren zu dessen Herstellung, und Verwendung des Papierrohres |
| US3170489A (en) * | 1961-01-27 | 1965-02-23 | Sonoco Products Co | Method of making plastic impregnated paper tubes and resulting product |
| FR1458458A (fr) * | 1965-01-22 | 1966-03-04 | Continental Can Co | Procédé et appareil pour fabriquer des boîtes à corps enroulé en hélice |
| US3300159A (en) * | 1963-07-24 | 1967-01-24 | Textile Paper Products Inc | Smooth-surfaced paper body and method of forming same |
| US3457130A (en) * | 1966-07-11 | 1969-07-22 | Owens Illinois Inc | Method and apparatus for forming a tubular article of wound plies of thermoplastic strip material |
| FR2302851A1 (fr) * | 1975-03-07 | 1976-10-01 | Spirapo | Procede de fabrication de tubes en papier et tubes realises par ledit procede |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2751936A (en) * | 1953-01-08 | 1956-06-26 | Sonoco Products Co | Textile carrier and means for forming same |
| US2785700A (en) * | 1955-09-27 | 1957-03-19 | Pennsylvania Papyrus Corp | Paper tube and method of making the same |
| DE1165914B (de) * | 1961-12-14 | 1964-03-19 | Siemens Ag | Schaltungsanordnung zur Bildung des Logarithmus einer Spannung |
| US3430543A (en) * | 1965-05-27 | 1969-03-04 | Sonoco Products Co | Method of making a wound multi-ply paper tube |
| US3451433A (en) * | 1967-05-24 | 1969-06-24 | Sonoco Products Co | Forming tube for glass fibers |
| US3813026A (en) * | 1968-02-07 | 1974-05-28 | Lhomme Sa | Accurately dimensioned smooth-surfaced multi-layer cardboard tubes and method of and apparatus for making the same |
| FR1563024A (de) * | 1968-02-07 | 1969-04-11 | ||
| US3545494A (en) * | 1968-09-30 | 1970-12-08 | Sonoco Products Co | Forming tube for glass fibers |
| FR2121993A6 (de) * | 1971-01-14 | 1972-08-25 | Lhomme Sa | |
| DE3150774C2 (de) * | 1981-12-22 | 1985-01-31 | Tanaka Shikan K.K., Yao, Osaka | Verfahren zum kontinuierlichen Herstellen eines Papierrohres mit glatter Oberfläche |
-
1984
- 1984-07-03 FR FR8410498A patent/FR2567069B1/fr not_active Expired
-
1985
- 1985-05-17 JP JP60104175A patent/JPH0628930B2/ja not_active Expired - Lifetime
- 1985-05-31 US US06/739,927 patent/US4645553A/en not_active Expired - Fee Related
- 1985-05-31 DE DE8585401079T patent/DE3561187D1/de not_active Expired
- 1985-05-31 EP EP85401079A patent/EP0170539B1/de not_active Expired
- 1985-06-19 ES ES544355A patent/ES8609032A1/es not_active Expired
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3002433A (en) * | 1958-01-10 | 1961-10-03 | Sonoco Products Co | Spiral wound paper tube having seamless outer surface |
| CH359594A (de) * | 1958-05-19 | 1962-01-15 | Sonoco Products Co | Mehrschichtiges Papierrohr, Verfahren zu dessen Herstellung, und Verwendung des Papierrohres |
| US3170489A (en) * | 1961-01-27 | 1965-02-23 | Sonoco Products Co | Method of making plastic impregnated paper tubes and resulting product |
| US3300159A (en) * | 1963-07-24 | 1967-01-24 | Textile Paper Products Inc | Smooth-surfaced paper body and method of forming same |
| FR1458458A (fr) * | 1965-01-22 | 1966-03-04 | Continental Can Co | Procédé et appareil pour fabriquer des boîtes à corps enroulé en hélice |
| US3457130A (en) * | 1966-07-11 | 1969-07-22 | Owens Illinois Inc | Method and apparatus for forming a tubular article of wound plies of thermoplastic strip material |
| FR2302851A1 (fr) * | 1975-03-07 | 1976-10-01 | Spirapo | Procede de fabrication de tubes en papier et tubes realises par ledit procede |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2623439A1 (fr) * | 1987-11-19 | 1989-05-26 | Auxerroise Cartonnages | Procede de fabrication de tube en carton a roulage parallele ou spirale |
| EP0343601A3 (de) * | 1988-05-26 | 1991-12-18 | Mitsuya Tekko Co., Ltd. | Vorrichtung zum Herstellen von Rohren |
| CN102922779A (zh) * | 2012-11-16 | 2013-02-13 | 金红叶纸业集团有限公司 | 纸管成型装置 |
| CN102922779B (zh) * | 2012-11-16 | 2015-04-01 | 金红叶纸业集团有限公司 | 纸管成型装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0170539B1 (de) | 1987-12-16 |
| JPH0628930B2 (ja) | 1994-04-20 |
| ES8609032A1 (es) | 1986-09-01 |
| FR2567069B1 (fr) | 1986-12-05 |
| US4645553A (en) | 1987-02-24 |
| JPS6120733A (ja) | 1986-01-29 |
| FR2567069A1 (fr) | 1986-01-10 |
| ES544355A0 (es) | 1986-09-01 |
| DE3561187D1 (en) | 1988-01-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0170539B1 (de) | Verfahren und Vorrichtung zum Fertigen von kalibrierten Röhren aus Pappe mit sehr kleiner Oberflächenrauheit und hoher Ausmassstabilität | |
| EP3492249A1 (de) | Verfahren und anlage zum wickeln eines vorimprägnierten stoffbands auf eine geneigte oberfläche | |
| FR2622506A1 (fr) | Procede et machine de fabrication de pieces tubulaires a partir d'au moins une bande de matiere souple, et pieces tubulaires ainsi obtenues | |
| EP0475886A1 (de) | Vorrichtung und Verfahren zum Öffnen einer Papierrolle und zum Verbinden von dem Ende einer Papierbahn an das Ende einer anderen Papierbahn | |
| EP0225235B1 (de) | Rohrschneidevorrichtung | |
| EP0878425B1 (de) | Maschine zum Wickeln von Folie, Verfahren zum Herstellen von Rollen aus vorgedehnter Folie und mit diesem Verfahren hergestellte Rollen | |
| EP0294290B1 (de) | Verfahren zum zusammendrückenden Aufwickeln | |
| EP0707941A1 (de) | Verfahren zum Herstellen von Rohren aus Verbundwerkstoff mit guten mechanischen und tribologischen Eigenschaften | |
| EP0402199B1 (de) | Elektro-Schweissmuffe sowie Verfahren und Vorrichtung zu deren Herstellung | |
| EP0546885B1 (de) | Zylinder für eine Stranggiessvorrichtung zum Giessen von Metallbändern, entsprechende Stranggiessvorrichtung und Verfahren zur Herstellung eines derartigen Zylinders | |
| FR2510032A1 (fr) | Procede et appareil pour fabriquer des articles par enroulement de filaments | |
| FR2539104A1 (fr) | Tube de carton spirale dechirable et son procede de fabrication | |
| EP1747158B1 (de) | Verfahren zur herstellung einer zentralen abwickelrolle und rolle | |
| FR2641492A1 (fr) | Procede de fabrication en continu de carton ondule tubulaire | |
| FR2693134A1 (fr) | Procédé pour réaliser un tube métallique gainé extérieurement. | |
| EP0773900B1 (de) | Trennvorrichtung, insbesondere für papier- oder kartonbahnen | |
| FR2774022A3 (fr) | Mandrin en carton pour l'industrie papetiere et son procede de fabrication | |
| EP0202983A1 (de) | Verfahren und Apparat zur Herstellung einer thermischen mehrschichtigen Isolierung rundum und entlang einer festen Durchfuhr und dazugehöriger Kryogenbehälter | |
| FR2651717A1 (fr) | Procede et dispositif de fabrication d'enveloppes en plastique verre-resine. | |
| FR2489747A1 (fr) | Tube de carton spirale et son procede de fabrication | |
| FR2481619A1 (fr) | Machine pour la production continue de tubes enroules en spirale a partir d'une tole en bande | |
| FR2497781A1 (fr) | Procede pour changer les bobines et les mandrins des machines d'enroulement sans axe | |
| FR2890385A1 (fr) | Machine de bobinage pour le stockage d'elements plats | |
| FR2655591A1 (fr) | Dispositif pour conserver l'aplat d'une bande de carton entre deux elements consecutifs d'une spiraleuse. | |
| CH452293A (fr) | Procédé et appareil pour la fabrication en continu d'un matériau isolant fibreux se présentant sous la forme d'un tube |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): BE CH DE GB IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19851212 |
|
| 17Q | First examination report despatched |
Effective date: 19860821 |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE CH DE GB IT LI LU NL SE |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| REF | Corresponds to: |
Ref document number: 3561187 Country of ref document: DE Date of ref document: 19880128 |
|
| R20 | Corrections of a patent specification |
Effective date: 19880212 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19930419 Year of fee payment: 9 Ref country code: BE Payment date: 19930419 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19930426 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 19930429 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19930518 Year of fee payment: 9 |
|
| ITTA | It: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19930531 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19930709 Year of fee payment: 9 |
|
| EPTA | Lu: last paid annual fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19940531 Ref country code: LI Effective date: 19940531 Ref country code: GB Effective date: 19940531 Ref country code: CH Effective date: 19940531 Ref country code: BE Effective date: 19940531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19940601 |
|
| BERE | Be: lapsed |
Owner name: S.A. LHOMME SA Effective date: 19940531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19941201 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19940531 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 85401079.0 Effective date: 19950110 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19950201 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 85401079.0 |