EP0262324A1 - Verfahren zum Schnellabschrecken im Wirbelbett - Google Patents
Verfahren zum Schnellabschrecken im Wirbelbett Download PDFInfo
- Publication number
- EP0262324A1 EP0262324A1 EP87110765A EP87110765A EP0262324A1 EP 0262324 A1 EP0262324 A1 EP 0262324A1 EP 87110765 A EP87110765 A EP 87110765A EP 87110765 A EP87110765 A EP 87110765A EP 0262324 A1 EP0262324 A1 EP 0262324A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bed
- temperature
- article
- conductivity gas
- fluidized
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000010791 quenching Methods 0.000 title claims abstract description 94
- 238000000034 method Methods 0.000 title claims abstract description 73
- 230000008569 process Effects 0.000 title claims abstract description 65
- 230000000171 quenching effect Effects 0.000 title claims abstract description 51
- 239000002245 particle Substances 0.000 claims abstract description 25
- 239000007789 gas Substances 0.000 claims description 82
- 229910000851 Alloy steel Inorganic materials 0.000 claims description 41
- 229910045601 alloy Inorganic materials 0.000 claims description 21
- 239000000956 alloy Substances 0.000 claims description 21
- 238000005243 fluidization Methods 0.000 claims description 15
- 239000007787 solid Substances 0.000 claims description 13
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 10
- 229910052782 aluminium Inorganic materials 0.000 claims description 9
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 9
- 230000015572 biosynthetic process Effects 0.000 claims description 9
- 239000001307 helium Substances 0.000 claims description 8
- 229910052734 helium Inorganic materials 0.000 claims description 8
- SWQJXJOGLNCZEY-UHFFFAOYSA-N helium atom Chemical compound [He] SWQJXJOGLNCZEY-UHFFFAOYSA-N 0.000 claims description 8
- 229910000838 Al alloy Inorganic materials 0.000 claims description 7
- 229910000734 martensite Inorganic materials 0.000 claims description 7
- 229910052759 nickel Inorganic materials 0.000 claims description 5
- 238000005279 austempering Methods 0.000 claims description 4
- 239000001257 hydrogen Substances 0.000 claims description 4
- 229910052739 hydrogen Inorganic materials 0.000 claims description 4
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 claims description 3
- 229910052751 metal Inorganic materials 0.000 description 14
- 239000002184 metal Substances 0.000 description 14
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 10
- 229910000831 Steel Inorganic materials 0.000 description 9
- 239000010959 steel Substances 0.000 description 9
- 230000008859 change Effects 0.000 description 7
- 239000012530 fluid Substances 0.000 description 7
- 229910001566 austenite Inorganic materials 0.000 description 6
- 239000000203 mixture Substances 0.000 description 6
- 238000010586 diagram Methods 0.000 description 5
- 239000007788 liquid Substances 0.000 description 5
- 229910052757 nitrogen Inorganic materials 0.000 description 5
- 150000002739 metals Chemical class 0.000 description 4
- 230000009466 transformation Effects 0.000 description 4
- 239000003921 oil Substances 0.000 description 3
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 description 3
- 229920000642 polymer Polymers 0.000 description 3
- QGZKDVFQNNGYKY-UHFFFAOYSA-N Ammonia Chemical compound N QGZKDVFQNNGYKY-UHFFFAOYSA-N 0.000 description 2
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 description 2
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 2
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 2
- UQSXHKLRYXJYBZ-UHFFFAOYSA-N Iron oxide Chemical compound [Fe]=O UQSXHKLRYXJYBZ-UHFFFAOYSA-N 0.000 description 2
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 description 2
- 229910001563 bainite Inorganic materials 0.000 description 2
- 229910052799 carbon Inorganic materials 0.000 description 2
- 229910001562 pearlite Inorganic materials 0.000 description 2
- 239000000843 powder Substances 0.000 description 2
- 230000009467 reduction Effects 0.000 description 2
- 150000003839 salts Chemical class 0.000 description 2
- 238000009827 uniform distribution Methods 0.000 description 2
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 2
- 229910000859 α-Fe Inorganic materials 0.000 description 2
- 229910001104 4140 steel Inorganic materials 0.000 description 1
- 229910001018 Cast iron Inorganic materials 0.000 description 1
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 description 1
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- CWYNVVGOOAEACU-UHFFFAOYSA-N Fe2+ Chemical compound [Fe+2] CWYNVVGOOAEACU-UHFFFAOYSA-N 0.000 description 1
- GWEVSGVZZGPLCZ-UHFFFAOYSA-N Titan oxide Chemical compound O=[Ti]=O GWEVSGVZZGPLCZ-UHFFFAOYSA-N 0.000 description 1
- WGLPBDUCMAPZCE-UHFFFAOYSA-N Trioxochromium Chemical compound O=[Cr](=O)=O WGLPBDUCMAPZCE-UHFFFAOYSA-N 0.000 description 1
- 230000032683 aging Effects 0.000 description 1
- 239000003570 air Substances 0.000 description 1
- 229910021529 ammonia Inorganic materials 0.000 description 1
- 229910052786 argon Inorganic materials 0.000 description 1
- 238000009835 boiling Methods 0.000 description 1
- 239000012267 brine Substances 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 229910052804 chromium Inorganic materials 0.000 description 1
- 239000011651 chromium Substances 0.000 description 1
- VNTLIPZTSJSULJ-UHFFFAOYSA-N chromium molybdenum Chemical compound [Cr].[Mo] VNTLIPZTSJSULJ-UHFFFAOYSA-N 0.000 description 1
- OGSYQYXYGXIQFH-UHFFFAOYSA-N chromium molybdenum nickel Chemical compound [Cr].[Ni].[Mo] OGSYQYXYGXIQFH-UHFFFAOYSA-N 0.000 description 1
- 229910000423 chromium oxide Inorganic materials 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 238000002485 combustion reaction Methods 0.000 description 1
- 230000000052 comparative effect Effects 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 238000005336 cracking Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- KZHJGOXRZJKJNY-UHFFFAOYSA-N dioxosilane;oxo(oxoalumanyloxy)alumane Chemical compound O=[Si]=O.O=[Si]=O.O=[Al]O[Al]=O.O=[Al]O[Al]=O.O=[Al]O[Al]=O KZHJGOXRZJKJNY-UHFFFAOYSA-N 0.000 description 1
- 239000011521 glass Substances 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 150000002431 hydrogen Chemical class 0.000 description 1
- 238000007654 immersion Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 229910052742 iron Inorganic materials 0.000 description 1
- 235000000396 iron Nutrition 0.000 description 1
- ZLNQQNXFFQJAID-UHFFFAOYSA-L magnesium carbonate Chemical compound [Mg+2].[O-]C([O-])=O ZLNQQNXFFQJAID-UHFFFAOYSA-L 0.000 description 1
- 229910000021 magnesium carbonate Inorganic materials 0.000 description 1
- 239000001095 magnesium carbonate Substances 0.000 description 1
- 235000014380 magnesium carbonate Nutrition 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 229910044991 metal oxide Inorganic materials 0.000 description 1
- 150000004706 metal oxides Chemical class 0.000 description 1
- 238000005272 metallurgy Methods 0.000 description 1
- DDTIGTPWGISMKL-UHFFFAOYSA-N molybdenum nickel Chemical compound [Ni].[Mo] DDTIGTPWGISMKL-UHFFFAOYSA-N 0.000 description 1
- 229910052863 mullite Inorganic materials 0.000 description 1
- RVTZCBVAJQQJTK-UHFFFAOYSA-N oxygen(2-);zirconium(4+) Chemical compound [O-2].[O-2].[Zr+4] RVTZCBVAJQQJTK-UHFFFAOYSA-N 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 239000002244 precipitate Substances 0.000 description 1
- 239000000047 product Substances 0.000 description 1
- 239000000377 silicon dioxide Substances 0.000 description 1
- 235000012239 silicon dioxide Nutrition 0.000 description 1
- HPALAKNZSZLMCH-UHFFFAOYSA-M sodium;chloride;hydrate Chemical compound O.[Na+].[Cl-] HPALAKNZSZLMCH-UHFFFAOYSA-M 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000035882 stress Effects 0.000 description 1
- OGIDPMRJRNCKJF-UHFFFAOYSA-N titanium oxide Inorganic materials [Ti]=O OGIDPMRJRNCKJF-UHFFFAOYSA-N 0.000 description 1
- 230000001131 transforming effect Effects 0.000 description 1
- 238000005303 weighing Methods 0.000 description 1
- 229910001928 zirconium oxide Inorganic materials 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/56—Continuous furnaces for strip or wire
- C21D9/573—Continuous furnaces for strip or wire with cooling
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/18—Hardening; Quenching with or without subsequent tempering
- C21D1/19—Hardening; Quenching with or without subsequent tempering by interrupted quenching
- C21D1/20—Isothermal quenching, e.g. bainitic hardening
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/34—Methods of heating
- C21D1/53—Heating in fluidised beds
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/56—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering characterised by the quenching agents
Definitions
- Quenching is conventionally carried out in a number of ways.
- spray quenching a liquid is sprayed onto the object to be quenched.
- gas quenching the object is placed in a flowing stream of a gas or vapor such as air, nitrogen, argon, helium, hydrogen, steam or combustion products.
- fog quenching a gas or vapor stream with entrained liquid droplets is directed onto the surface of the object to be quenched.
- immersion quenching the object is immersed in a liquid bath such as water, brine, oil molten salt, polymer solution, or a liquid cryogen.
- the process of this invention is particularly useful for the heat treating of steel alloy articles and will be described in detail with reference to this type of heat treating.
- the quench rate is generally measured by a procedure variously known in the art as the Magnetic Test, General Motors Quenchometer Test, or Nickel Ball Test.
- the procedure comprises heating a 7/8-inch (22 mm) nickel sphere, weighing approximately 1.8 ounces (50 g) to a given high temperature and then quenching the sphere in the quenchant to be evaluated down to give low temperature. The time it takes for the sphere temperature go from the high to the low temperature is a measure of the quench rate.
- the initial quench rate as measured by the Nickel Ball Test between the temperatures of 1600°F and 684°F is less than 24 seconds.
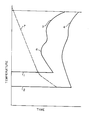
- a fast quench may not always be desirable because of the possibility of stress creation within the alloy. Therefore, if possible without crossing the softer phase threshold, one can reduce the quenching rate by changing the mode of operation of the bed.
- the process may be carried out with the bed fluidized with a low conductivity gas, or with the bed in a slumped condition.
- a convenient time to change from fluidization with a high conductivity gas to another bed operating mode is when the article temperature has dropped below the nose temperature.
- the quenching continues for a period of time and at a quench rate sufficient to achieve the M s temperature of the alloy substantially without forming undesirable softer phases within the part.
- Step (d) of the austempering treatment can be carried out with the bed slumped or fluidized with a low conductivity gas and one can alternate between these two modes of bed operation.
- step (d) can be carried out entirely with the bed fluidized with high conductivity gas, but generally and preferably, is carried out in part with the bed fluidized with low conductivity gas or operated in the slumped mode. Step (d) may be conveniently continued until the article has reached ambient or near ambient temperature.
- Step (d) can be carried out entirely with the bed fluidized with high conductivity gas or step (d) can be carried out in part with the bed fluidized with low conductivity gas or operated in the slumped mode.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Articles (AREA)
- Solid-Phase Diffusion Into Metallic Material Surfaces (AREA)
- Crucibles And Fluidized-Bed Furnaces (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US913320 | 1978-06-07 | ||
| US91332086A | 1986-09-30 | 1986-09-30 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0262324A1 true EP0262324A1 (de) | 1988-04-06 |
Family
ID=25433163
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP87110765A Withdrawn EP0262324A1 (de) | 1986-09-30 | 1987-07-24 | Verfahren zum Schnellabschrecken im Wirbelbett |
Country Status (6)
| Country | Link |
|---|---|
| EP (1) | EP0262324A1 (de) |
| JP (1) | JPS6389615A (de) |
| KR (1) | KR880004112A (de) |
| CN (1) | CN87105737A (de) |
| BR (1) | BR8703860A (de) |
| CA (1) | CA1296603C (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0315975A1 (de) * | 1987-11-10 | 1989-05-17 | Union Carbide Corporation | Verfahren zum Schnellabschrecken |
| US12091744B2 (en) | 2018-06-13 | 2024-09-17 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| US12091739B2 (en) | 2018-06-13 | 2024-09-17 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1311088C (zh) * | 2002-01-18 | 2007-04-18 | 王新辉 | 用风对钢丸进行热处理的方法及其流化床装置 |
| CN101333593B (zh) * | 2008-07-25 | 2010-06-30 | 张家港市东航机械有限公司 | 钢帘线钢丝淬火流化粒子炉中的低位返砂器 |
| CN101886159B (zh) * | 2010-07-13 | 2011-11-16 | 贾会平 | 钢坯加热的方法和装置 |
| WO2020012222A1 (en) * | 2018-07-11 | 2020-01-16 | Arcelormittal | Method to control the cooling of a metal product |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3053704A (en) * | 1953-11-27 | 1962-09-11 | Exxon Research Engineering Co | Heat treating metals |
| FR2447968A1 (fr) * | 1979-01-30 | 1980-08-29 | Celes Sa | Procede de trempe superficielle |
| EP0118836A2 (de) * | 1983-03-07 | 1984-09-19 | Rockwell International Corporation | Verfahren zum Kühlen eines erhitzten Werkstücks |
| EP0144907A2 (de) * | 1983-12-05 | 1985-06-19 | Nissan Motor Co., Ltd. | Verfahren zur Herstellung von Gegenständen aus Gusseisen mit Kugelgraphit durch Umwandlung in der Bainitstufe |
| US4612065A (en) * | 1982-08-17 | 1986-09-16 | Ruhrgas Aktiengesellschaft | Method for the heat treatment of workpieces |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS565917A (en) * | 1979-06-28 | 1981-01-22 | Komatsu Ltd | Fluidized bed hardening device |
| JPS6043410B2 (ja) * | 1981-11-11 | 1985-09-27 | 東レエンジニアリング株式会社 | 流動層炉による金属熱処理方法 |
-
1987
- 1987-07-20 CA CA000542520A patent/CA1296603C/en not_active Expired - Lifetime
- 1987-07-24 BR BR8703860A patent/BR8703860A/pt unknown
- 1987-07-24 EP EP87110765A patent/EP0262324A1/de not_active Withdrawn
- 1987-07-30 JP JP62189051A patent/JPS6389615A/ja active Pending
- 1987-08-03 KR KR1019870008490A patent/KR880004112A/ko not_active Ceased
- 1987-08-19 CN CN198787105737A patent/CN87105737A/zh active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3053704A (en) * | 1953-11-27 | 1962-09-11 | Exxon Research Engineering Co | Heat treating metals |
| FR2447968A1 (fr) * | 1979-01-30 | 1980-08-29 | Celes Sa | Procede de trempe superficielle |
| US4612065A (en) * | 1982-08-17 | 1986-09-16 | Ruhrgas Aktiengesellschaft | Method for the heat treatment of workpieces |
| EP0118836A2 (de) * | 1983-03-07 | 1984-09-19 | Rockwell International Corporation | Verfahren zum Kühlen eines erhitzten Werkstücks |
| EP0144907A2 (de) * | 1983-12-05 | 1985-06-19 | Nissan Motor Co., Ltd. | Verfahren zur Herstellung von Gegenständen aus Gusseisen mit Kugelgraphit durch Umwandlung in der Bainitstufe |
Non-Patent Citations (2)
| Title |
|---|
| HÄRTEREI-TECHNISCHE MITTEILUNGEN, vol. 40, no. 5, September-October 1985, pages 195-197, Munich; R. PULKKINEN et al.: "Beschleunigtes Abkühlen von Stahl und Gusseisen in einem Wirbelbett" * |
| PATENT ABSTRACTS OF JAPAN, vol. 5, no. 54 (C-50)[726], 15th April 1981; & JP-A-56 005 917 (KOMATSU SEISAKUSHO) 22-01-1981 * |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0315975A1 (de) * | 1987-11-10 | 1989-05-17 | Union Carbide Corporation | Verfahren zum Schnellabschrecken |
| US12091744B2 (en) | 2018-06-13 | 2024-09-17 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| US12091739B2 (en) | 2018-06-13 | 2024-09-17 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| US12553119B2 (en) | 2018-06-13 | 2026-02-17 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| US12624441B2 (en) | 2018-06-13 | 2026-05-12 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
Also Published As
| Publication number | Publication date |
|---|---|
| CA1296603C (en) | 1992-03-03 |
| CN87105737A (zh) | 1988-05-04 |
| JPS6389615A (ja) | 1988-04-20 |
| BR8703860A (pt) | 1988-05-03 |
| KR880004112A (ko) | 1988-06-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2117069C (en) | Process and apparatus for surface hardening of refractory metal workpieces | |
| Mola et al. | Correlation between mechanical stability and hardness of austenite in martensite/austenite mixtures | |
| CA1296603C (en) | Process for rapid quenching in a fluidized bed | |
| US3519497A (en) | Method for the thermal treatment of steel rails | |
| Delia et al. | Effect of austenitizing conditions on the impact properties of an alloyed austempered ductile iron of initially ferritic matrix structure | |
| Cerah et al. | Influence of martensite volume fraction and tempering time on tensile properties of partially austenitized in the (α+ γ) temperature range and quenched+ tempered ferritic ductile iron | |
| US5064479A (en) | Thermal treatment in a fluidized bed | |
| US5080729A (en) | Process for rapid quenching in a collapsed bed | |
| Zarubova et al. | Mechanisms of phase transformations during laser treatment of grey cast iron | |
| Dossett | Introduction to cast iron heat treatment | |
| Li | Heat treating of precipitation-hardenable stainless steels and iron-base superalloys | |
| Chevrier et al. | Optimal cooling rate and process control in metallic parts heat treatment | |
| JPS59107018A (ja) | 鋳鉄部品の熱処理方法 | |
| Stojko et al. | Isothermal martensite formation at sub-zero temperatures | |
| Dossett et al. | Heat treating of martensitic stainless steels | |
| RU1788045C (ru) | Способ закалки быстрорежущей стали | |
| Harwarth et al. | Influence of Carbon on the Microstructure Evolution and Hardness of Fe–13Cr–xC (x= 0–0.7 wt.%) Stainless Steel. Materials 2021, 14, 5063 | |
| EP0281249A1 (de) | Verfahren zur Wärmebehandlung von Teilen aus Eisenwerkstoffen | |
| Ahlfors | Heat treatment with unpreceded possibilities and flexibility | |
| JPS6148514A (ja) | 鋼の焼入方法 | |
| Doheim et al. | Effect of fluidised bed parameters on quenching of steel sections | |
| JPH02194120A (ja) | 鋳造品のダイレクトオーステンパー処理法 | |
| Li et al. | Continuous cooling transformation of niobium microalloyed high carbon steels. | |
| Geller et al. | Modeling of oil quenching by a water-air stream controlled by a microcomputer | |
| Pantsar et al. | Effect of processing parameters on the microstructure and hardness of laser transformation hardened tool steel |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE CH DE ES FR IT LI LU NL |
|
| 17P | Request for examination filed |
Effective date: 19880520 |
|
| 17Q | First examination report despatched |
Effective date: 19890725 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19900918 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: VON DEN SYPE, JAAK Inventor name: DELANO, MARK ANTHONY |