EP1346069B1 - Acier magnetique a grains non orientes, procede de fabrication de toles et toles obtenues - Google Patents
Acier magnetique a grains non orientes, procede de fabrication de toles et toles obtenues Download PDFInfo
- Publication number
- EP1346069B1 EP1346069B1 EP01994925A EP01994925A EP1346069B1 EP 1346069 B1 EP1346069 B1 EP 1346069B1 EP 01994925 A EP01994925 A EP 01994925A EP 01994925 A EP01994925 A EP 01994925A EP 1346069 B1 EP1346069 B1 EP 1346069B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheet
- steel sheet
- magnetic steel
- temperature
- oriented magnetic
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1216—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the working steps
- C21D8/1222—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/004—Very low carbon steels, i.e. having a carbon content of less than 0,01%
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/008—Ferrous alloys, e.g. steel alloys containing tin
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/14766—Fe-Si based alloys
- H01F1/14775—Fe-Si based alloys in the form of sheets
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1216—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the working steps
- C21D8/1233—Cold rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1272—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1277—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties involving a particular surface treatment
- C21D8/1283—Application of a separating or insulating coating
Definitions
- the present invention relates to a new steel composition magnetic with non-oriented grains having magnetic properties, improved mechanical and thermal.
- This type of steel is used in particular for the manufacture of parts for electrical engineering, whose role is to couple different circuits electric to allow the transfer of electromagnetic energy from to each other.
- This energy transfer notably supposes that the flux density magnetic (also called induction) obtained when we submit the material to a field, as high as possible.
- the first consists of highly alloyed steels whose level of magnetic losses depends essentially on the chemical composition. These steels contain 1.4 to 3.3% by weight of silicon as well as aluminum up to 0.1 to 1.0% by weight. They have the disadvantage of having a low thermal conductivity and a too high hardness which causes excessive wear of the cutting tools pieces. Their high alloy content also makes them expensive.
- the second family of non-oriented grain magnetic steels is made of low alloyed steels which generally contain only silicon at contents of the order of 0.5% by weight. These steels are said to have improved magnetic permeability, and allow achieve high induction levels for applied fields of around 5000 A / m while maintaining average loss levels. They also have good thermal conductivity, but have poor mechanical properties, with in particular a limit low elasticity and hardness. This is why, in practice, we do not can use this family of steels only for static machines or dynamics at low speeds. Furthermore, the manufacture of parts in these nuances are also problematic, as we observe frequent deformations during their cutting, which leads to material losses and productivity.
- the present invention therefore aims to provide such a material whose range of applications may be wider than that materials of the prior art, and which will in particular increase mass power without risk of significant heating of electrical insulators present.
- a first object of the invention consists of a magnetic steel whose composition comprises, expressed in% by weight: VS ⁇ 0.005 1.20 ⁇ Yes s 1.40 0.18 ⁇ al ⁇ 0.22 0.25 ⁇ mn ⁇ 0.35 0.10 ⁇ P ⁇ 0.14 0.09 ⁇ Sn ⁇ 0.12 0,005 ⁇ S ⁇ 0.015 NOT ⁇ 0.01 O ⁇ 0.01 the rest of the composition consisting of iron and impurities resulting from the preparation.
- the present inventors have in fact discovered that the combination aluminum, tin and phosphorus contents claimed improved surprisingly and noticeably the magnetic, mechanical and of thermal conductivity of the steel grade.
- the tin content of the composition according to the invention must be between 0.09 and 0.12% by weight. Indeed, if it is less than this range, we don't see enough reduction in losses magnetic. On the other hand, if the tin content exceeds 0.12% by weight, the steel has too low a ductility.
- the carbon content of the composition according to the invention must be less than 0.005% by weight because any excess of this value leads to an unacceptable tendency to magnetic aging because severely limiting the service life of the parts.
- the silicon content of the composition according to the invention must be between 1.2 and 1.4% by weight.
- the aluminum content of the composition according to the invention must be between 0.18 and 0.22%. in weight. Aluminum improves magnetic properties of steel but should not be present too large quantity because it is harmful to the ductility of the steel and it reduces its thermal conductivity. We also limit its content to avoid precipitation of too fine aluminum nitrides which would block movements of magnetic domains.
- the nitrogen content of the composition must be less than 0.01% by weight to also limit the precipitation of aluminum nitrides.
- the manganese content of the composition according to the invention must be between 0.25 and 0.35% by weight. Manganese improves mechanical properties of steel by preventing it from breaking during hot rolling. Below 0.25% by weight, it does not improve these mechanical properties sufficiently, while above 0.35% in weight, it degrades the magnetic properties of the shade and it decreases the thermal conductivity of steel.
- the phosphorus is present in the steel according to the invention in a content of 0.10 to 0.14% by weight. It allows hardening of steel while significantly increasing its elastic limit. Its content is limited to 0.14% by weight because it reduces the thermal conductivity of steel. It increases the resistivity of the alloy which reduces the losses due to eddy currents. In one embodiment preferred, its content is between 0.11 and 0.13% by weight.
- the sulfur content is less than 0.015% by weight, because this element is harmful for the characteristics of steel, but it is also superior 0.005% by weight, since a lower content would require a step additional desulfurization which is not justified in the context of the present invention.
- composition according to the invention can be prepared so conventional and by any suitable process comprising a step of decarburization, the carbon level to be reached being very low.
- the steel can be cast in the form of a slab that is heated to a temperature above about 1150 ° C to hot roll it until it reaches a thickness of the order of 2 mm, for example. We can then proceed to wind the sheet as produced and then annealed.
- the hot rolled sheet is then pickled and cold rolled, preferably up to the desired final thickness, to undergo a final heat treatment which is preferably annealing in a non-atmospheric oxidizing. If the carbon content of the sheet is still too high at this stage, decarburization is carried out during annealing.
- the present inventors have however discovered that by applying special conditions during the hot rolling operation and winding it was possible to significantly improve the induction of the sheet obtained while removing a step from the conventional process.
- This process has the important advantage of optimizing the properties sheet metal, because the present inventors have found that its level of induction was very markedly increased, while the magnetic losses by hysteresis are reduced.
- the temperature at the end of rolling is such that it ends in the ferritic field. This characteristic combined with control of a relatively high winding temperature allows recrystallization and the enlargement of the grains of the hot sheet by a self-annealing phenomenon.
- the marked improvement in induction is probably due to the formation of Goss texture components, as can be found in oriented grain steels, but also of planar texture.
- the unfavorable component ⁇ 111 ⁇ is also decreased during the process thanks to the presence of tin which, segregating at the grain boundaries, prevents germination and growth of grains of texture ⁇ 111 ⁇ during recrystallization, thereby promoting grain growth at final annealing after cold rolling.
- the winding temperature is higher than 700 ° C, in particular higher than 720 ° C, which allows to further improve the magnetic performance of materials.
- the present inventors have also found that it is possible to further reduce magnetic losses by optimizing the conditions of the heat treatment which follows cold rolling.
- a heat treatment taking the form of annealing carried out at a temperature above 900 ° C, and in another embodiment preferred, it is carried out continuously in an oven in which the sheet has a residence time less than or equal to 50 s.
- a third object of the invention consists of steel sheets magnetic with non-oriented grains of composition in accordance with this invention and by the sheets obtained by implementing the method according to the invention in its different variants.
- Sheets are also preferred having, for a thickness of 0.65 mm, total magnetic losses less than 5.30 W / kg, in particular less than 4.70 W / kg and an induction greater than 1.72 T when applying a field of 5000 A / m.
- the sheets obtained by the process according to the invention have especially the advantage of not having to be subjected to treatment additional thermal, after cutting the pieces, to allow magnetic properties to express themselves completely. Such treatment would indeed not only expensive but also harmful for behavior subsequent mechanical parts.
- the sheets obtained according to the invention are therefore directly ready for use and we can also cover them with insulating coating on each side if required by the application.
- These sheets may in particular be used to manufacture parts for rotating machines, motors, transformers, but may also be used in the field of household appliances and engineering electrical in general.
- the sheets subjected to the various tests have a thickness of 0.50 mm in order to compare the results obtained, because the magnetic losses are a function of this thickness.
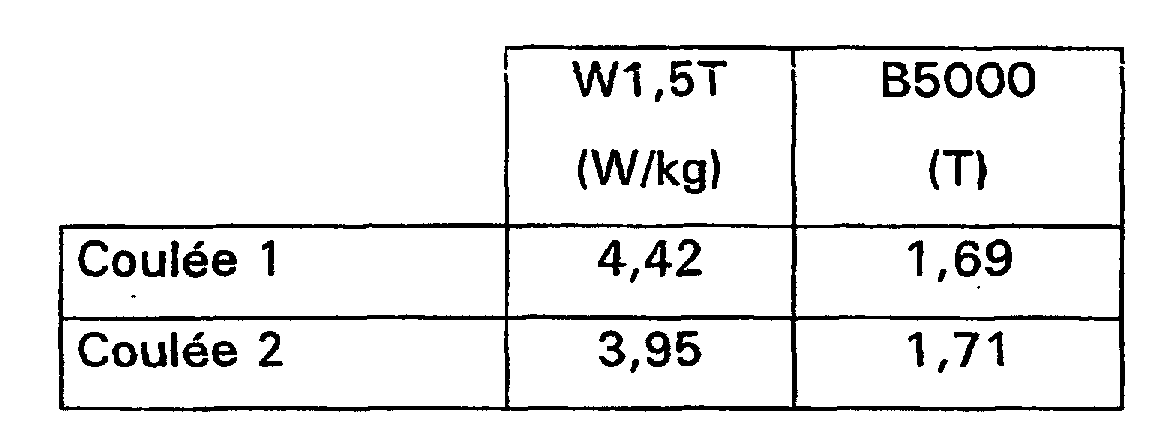
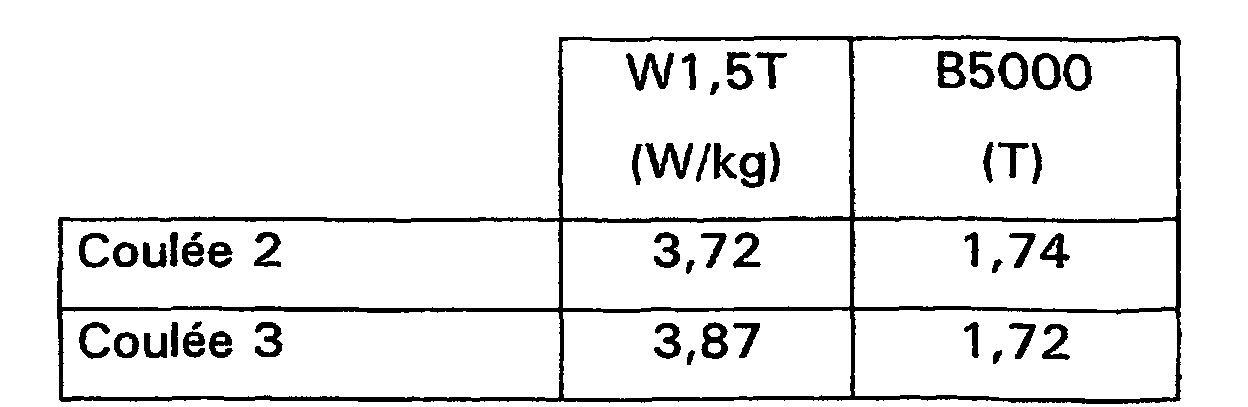
- W1,5T total magnetic loss at 1.5 Tesla and 50Hz expressed in W / kg, B5000 magnetic flux density (or induction) under a field of 5000 A / m, expressed in Tesla, HV5 hardness.
- Two sheets are made from casting 1 and casting 2 according to the invention, by hot rolling the corresponding slabs without following the process according to the invention.
- the winding is carried out at a temperature of approximately 645 ° C.
- the sheets are then pickled and cold rolled.
- the final annealing is carried out continuously at 950 ° C., in a oven in which the sheets stay for 25 s.
- the total magnetic losses W1.5T and the induction B5000 are then measured and the following results are obtained: It can be seen that the magnetic losses have been significantly reduced and that the induction has been improved compared to the composition of the prior art. These improvements come from the claimed balance between the aluminum, phosphorus and tin contents.
- Two sheets are made in casting 2 according to the invention and in casting 3 in a manner analogous to that used in example 1, but by carrying out the winding at a temperature of 720 ° C.
- a series of slabs is made in the casting 4 according to the invention which is hot rolled using the method according to the invention.
- the sheets are then cold rolled until a thickness of 0.50 mm is obtained, then these sheets are annealed continuously in an oven by varying the annealing temperature and the residence time of the sheets in this oven.
- the results are collated in the following table: Annealing temperature (° C) Residence time (s) W1.5T (W / kg) B5000 (T) 1000 25 3.15 1.76 1000 85 3.42 1.75 950 85 4.10 1.75
- Cast sheets according to the invention are subjected to a certain number of conductivity measurements and we see that we get values greater than or equal to 35 W / m.K.
- a high alloy steel of the prior art comprising 2.9% silicon has a conductivity of 20 W / m.K.
- a highly allied nuance of art anterior comprising 1.4% of silicon has an elastic limit of 250 MPa and a hardness of 140 Hv5.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Organic Chemistry (AREA)
- Metallurgy (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Manufacturing & Machinery (AREA)
- Crystallography & Structural Chemistry (AREA)
- Thermal Sciences (AREA)
- Dispersion Chemistry (AREA)
- Power Engineering (AREA)
- Manufacturing Of Steel Electrode Plates (AREA)
- Soft Magnetic Materials (AREA)
Description
| C | ≤ 0,005 | |
| 1,20 ≤ | Si | s 1,40 |
| 0,18 ≤ | Al | ≤ 0,22 |
| 0,25 ≤ | Mn | ≤ 0,35 |
| 0,10 ≤ | P | ≤ 0,14 |
| 0,09 ≤ | Sn | ≤ 0,12 |
| 0,005≤ | S | ≤ 0,015 |
| N | ≤ 0,01 | |
| O | ≤ 0,01 |
- l'élaboration de l'acier et la coulée d'une brame,
- un laminage à chaud de cette brame pour obtenir une tôle, ledit laminage se terminant à une température comprise entre celle du point Ar3 diminuée de 80°C et celle du point Ar3,
- un bobinage de la tôle à une température supérieure à 680°C,
- un laminage à froid puis un traitement thermique de la tôle.
| Composition (% en poids) | Coulée 1 | Coulée 2 | Coulée 3 | Coulée 4 |
| C | 0,003 | 0,003 | 0,003 | 0,003 |
| Si | 1,3 | 1,3 | 1,3 | 1,3 |
| Al | 0,105 | 0,180 | 0,200 | 0,200 |
| Mn | 0,275 | 0,275 | 0,275 | 0,275 |
| P | 0,05 | 0,115 | 0,120 | 0,120 |
| Sn | 0,03 | 0,110 | - | 0,100 |
| S | 0,01 | 0,01 | 0,01 | 0,01 |
| W1,5T | perte magnétique totale à 1,5 Tesla et 50Hz, exprimée en W/kg, |
| B5000 | densité de flux magnétique (ou induction) sous un champ de 5000 A/m, exprimée en Tesla, |
| Hv5 | dureté. |

| Température de recuit (°C) | Temps de séjour (s) | W1,5T (W/kg) | B5000 (T) |
| 1000 | 25 | 3,15 | 1,76 |
| 1000 | 85 | 3,42 | 1,75 |
| 950 | 85 | 4,10 | 1,75 |
| Température de recuit (°C) | Temps de séjour (s) | W1,5T (W/kg) | B5000 (T) |
| 1000 | 25 | 4,2 | 1,76 |
| 950 | 85 | 4,6 | 1,76 |
Claims (15)
- Acier magnétique dont la composition comprend, exprimés en % en poids:
C ≤ 0,005 1,20≤ Si ≤1,40 0,18 ≤ Al ≤ 0,22 0,25≤ Mn ≤ 0,35 0,10 ≤ P ≤ 0,14 0,09 ≤ Sn ≤ 0,12 0,005≤ S ≤ 0,015 N ≤ 0, 01 O ≤ 0,01 - Procédé de fabrication d'une tôle de composition conforme à la revendication 1, comprenant :l'élaboration de l'acier et la coulée d'une brame,un laminage à chaud de cette brame pour obtenir une tôle, ledit laminage se terminant à une température comprise entre celle du point Ar3 diminuée de 80°C et celle du point Ar3,un bobinage de la tôle à une température supérieure à 680 °C,un laminage à froid puis un traitement thermique de la tôle.
- Procédé selon la revendication 2, caractérisé en ce que, en outre, la température de bobinage est supérieure à 700°C.
- Procédé selon la revendication 2 ou 3, caractérisé en ce que ledit traitement thermique est un recuit que l'on effectue à une température supérieure à 900°C.
- Procédé selon la revendication 4, caractérisé en ce que ledit recuit est effectué en continu dans un four dans lequel la tôle a un temps de séjour inférieur ou égal à 50 s.
- Procédé selon la revendication 4 ou 5, caractérisé en ce que ledit laminage à froid est réalisé jusqu'à atteindre l'épaisseur définitive de la tôle et en ce que ledit recuit est un recuit final.
- Tôle d'acier magnétique à grains non orientés de composition conforme à la revendication 1.
- Tôle d'acier magnétique à grains non orientés obtenue par la mise en oeuvre du procédé selon l'une quelconque des revendications 2 à 6.
- Tôle d'acier magnétique à grains non orientés selon la revendication 7 ou 8, caractérisée en ce qu'elle présente, pour une épaisseur de 0,50 mm, des pertes magnétiques totales inférieures à 4 W/kg et une induction supérieure à 1,72 T lorsqu'on applique un champ de 5000 A/m.
- Tôle d'acier magnétique à grains non orientés selon la revendication 9, caractérisée en ce qu'elle présente en outre des pertes magnétiques totales inférieures à 3,5 W/kg.
- Tôle d'acier magnétique à grains non orientés selon la revendication 10, caractérisée en ce qu'elle présente en outre des pertes magnétiques totales inférieures à 3,3 W/kg.
- Tôle d'acier magnétique à grains non orientés selon la revendication 7 ou 8, caractérisée en ce qu'elle présente, pour une épaisseur de 0,65 mm, des pertes magnétiques totales inférieures à 5,30 W/kg et une induction supérieure à 1,72 T lorsqu'on applique un champ de 5000 A/m.
- Tôle d'acier magnétique à grains non orientés selon la revendication 12, caractérisée en ce qu'elle présente en outre des pertes magnétiques totales inférieures à 4,70 W/kg.
- Tôle d'acier magnétique à grains non orientés selon l'une quelconque des revendications 7 à 13, caractérisée en ce qu'elle présente une conductivité thermique supérieure ou égale à 35 W/m.K et une limite d'élasticité supérieure ou égale à 300 MPa.
- Tôle d'acier magnétique à grains non orientés selon l'une quelconque des revendications 7. à 14, caractérisée en ce qu'elle comprend en outre une couche de revêtement isolant sur chacune de ses faces.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0017084A FR2818664B1 (fr) | 2000-12-27 | 2000-12-27 | Acier magnetique a grains non orientes, procede de fabrication de toles et toles obtenues |
| FR0017084 | 2000-12-27 | ||
| PCT/FR2001/004093 WO2002052048A1 (fr) | 2000-12-27 | 2001-12-20 | Acier magnetique a grains non orientes, procede de fabrication de tôles et tôles obtenues |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1346069A1 EP1346069A1 (fr) | 2003-09-24 |
| EP1346069B1 true EP1346069B1 (fr) | 2004-06-16 |
Family
ID=8858246
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01994925A Expired - Lifetime EP1346069B1 (fr) | 2000-12-27 | 2001-12-20 | Acier magnetique a grains non orientes, procede de fabrication de toles et toles obtenues |
Country Status (9)
| Country | Link |
|---|---|
| EP (1) | EP1346069B1 (fr) |
| AT (1) | ATE269421T1 (fr) |
| CZ (1) | CZ303205B6 (fr) |
| DE (1) | DE60103933T2 (fr) |
| EA (1) | EA004912B1 (fr) |
| ES (1) | ES2223961T3 (fr) |
| FR (1) | FR2818664B1 (fr) |
| TR (1) | TR200401448T4 (fr) |
| WO (1) | WO2002052048A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2623626A4 (fr) * | 2010-09-30 | 2017-11-22 | Baoshan Iron & Steel Co., Ltd. | Tôle d'acier électrique non orientée exempte de défaut d'ondulation et son procédé de production |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2835001A1 (fr) * | 2002-01-21 | 2003-07-25 | Usinor | Procede de fabrication d'une tole d'acier magnetique, toles et pieces obtenues |
| WO2025104469A1 (fr) | 2023-11-15 | 2025-05-22 | Arcelormittal | Acier électrique à grains non orientés et procédé de fabrication d'un acier électrique à grains non orientés correspondant |
| WO2025104473A1 (fr) | 2023-11-15 | 2025-05-22 | Arcelormittal | Acier électrique à grains non orientés et procédé de fabrication d'un acier électrique à grains non orientés correspondant |
| WO2025104468A1 (fr) * | 2023-11-15 | 2025-05-22 | Arcelormittal | Acier électrique non orienté et procédé de fabrication d'acier électrique non orienté correspondant |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS583027B2 (ja) * | 1979-05-30 | 1983-01-19 | 川崎製鉄株式会社 | 鉄損の低い冷間圧延無方向性電磁鋼板 |
| JP3446385B2 (ja) * | 1995-04-21 | 2003-09-16 | Jfeスチール株式会社 | 被膜密着性に優れた無方向性電磁鋼板 |
| JPH0941037A (ja) * | 1995-05-19 | 1997-02-10 | Kawasaki Steel Corp | 無方向性電磁鋼板の製造方法 |
| KR100240995B1 (ko) * | 1995-12-19 | 2000-03-02 | 이구택 | 절연피막의 밀착성이 우수한 무방향성 전기강판의 제조방법 |
| US5798001A (en) * | 1995-12-28 | 1998-08-25 | Ltv Steel Company, Inc. | Electrical steel with improved magnetic properties in the rolling direction |
| JP3378934B2 (ja) * | 1996-08-19 | 2003-02-17 | 新日本製鐵株式会社 | 磁気特性と表面性状の優れた無方向性電磁鋼板の製造方法 |
| US6139650A (en) * | 1997-03-18 | 2000-10-31 | Nkk Corporation | Non-oriented electromagnetic steel sheet and method for manufacturing the same |
| JPH11189850A (ja) * | 1997-12-24 | 1999-07-13 | Sumitomo Metal Ind Ltd | 無方向性電磁鋼板およびその製造方法 |
| JP3883029B2 (ja) * | 1998-01-19 | 2007-02-21 | Jfeスチール株式会社 | 軟磁性鋼板 |
| JPH11286725A (ja) * | 1998-04-01 | 1999-10-19 | Nippon Steel Corp | 磁性に優れた無方向性電磁鋼板の製造方法 |
-
2000
- 2000-12-27 FR FR0017084A patent/FR2818664B1/fr not_active Expired - Lifetime
-
2001
- 2001-12-20 EP EP01994925A patent/EP1346069B1/fr not_active Expired - Lifetime
- 2001-12-20 CZ CZ20031798A patent/CZ303205B6/cs not_active IP Right Cessation
- 2001-12-20 AT AT01994925T patent/ATE269421T1/de active
- 2001-12-20 ES ES01994925T patent/ES2223961T3/es not_active Expired - Lifetime
- 2001-12-20 WO PCT/FR2001/004093 patent/WO2002052048A1/fr not_active Ceased
- 2001-12-20 DE DE60103933T patent/DE60103933T2/de not_active Expired - Lifetime
- 2001-12-20 EA EA200300729A patent/EA004912B1/ru not_active IP Right Cessation
- 2001-12-20 TR TR2004/01448T patent/TR200401448T4/xx unknown
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2623626A4 (fr) * | 2010-09-30 | 2017-11-22 | Baoshan Iron & Steel Co., Ltd. | Tôle d'acier électrique non orientée exempte de défaut d'ondulation et son procédé de production |
Also Published As
| Publication number | Publication date |
|---|---|
| TR200401448T4 (tr) | 2004-07-21 |
| EA200300729A1 (ru) | 2003-12-25 |
| ES2223961T3 (es) | 2005-03-01 |
| DE60103933D1 (de) | 2004-07-22 |
| EP1346069A1 (fr) | 2003-09-24 |
| CZ303205B6 (cs) | 2012-05-23 |
| FR2818664B1 (fr) | 2003-12-05 |
| ATE269421T1 (de) | 2004-07-15 |
| EA004912B1 (ru) | 2004-08-26 |
| CZ20031798A3 (cs) | 2004-02-18 |
| DE60103933T2 (de) | 2004-11-04 |
| WO2002052048A1 (fr) | 2002-07-04 |
| FR2818664A1 (fr) | 2002-06-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US11718891B2 (en) | Non-oriented electrical steel sheet and method for producing same, and motor core and method for producing same | |
| RU2771133C1 (ru) | Лист из нетекстурированной электротехнической стали и способ его производства | |
| KR101963056B1 (ko) | 무방향성 전기 강판 및 무방향성 전기 강판의 제조 방법 | |
| JP5668460B2 (ja) | 無方向性電磁鋼板の製造方法 | |
| KR102139134B1 (ko) | 방향성 전자 강판의 제조 방법 | |
| KR101591222B1 (ko) | 무방향성 전기 강판의 제조 방법 | |
| CN107849656B (zh) | 取向性电磁钢板的制造方法 | |
| JP5439866B2 (ja) | 著しく磁束密度が高い方向性電磁鋼板の製造方法 | |
| WO2018179871A1 (fr) | Pr0cédé de fabrication d'une plaque d'acier électromagnétique à grains non orientés, procédé de fabrication de noyau de moteur et noyau de moteur | |
| JP5668767B2 (ja) | 無方向性電磁鋼板製造用の熱延鋼板およびその製造方法 | |
| JP6610789B2 (ja) | 方向性電磁鋼板用熱延鋼板、および方向性電磁鋼板の製造方法 | |
| JP6319574B2 (ja) | 磁気特性に優れる無方向性電磁鋼板 | |
| WO2011148849A1 (fr) | Procédé de production d'une tôle d'acier électromagnétique unidirectionnel | |
| JP2011256437A (ja) | 無方向性電磁鋼板の製造方法 | |
| WO2015107967A1 (fr) | Feuille d'acier électromagnétique non directionnel présentant d'excellentes propriétés magnétiques | |
| JP5428188B2 (ja) | 方向性電磁鋼板の製造方法 | |
| FR2533586A1 (fr) | Procede de fabrication d'une tole d'acier electrique a grain oriente ayant une haute densite de flux magnetique | |
| EP0784100B1 (fr) | Alliage fer-cobalt, procédé de fabrication d'une bande en alliage fercobalt et bande obtenue | |
| US9637812B2 (en) | Non-oriented electrical steel sheet | |
| JP4608562B2 (ja) | 著しく磁束密度が高い方向性電磁鋼板の製造方法 | |
| EP1346069A1 (fr) | Acier magnetique a grains non orientes, procede de fabrication de t les et t les obtenues | |
| JP6146582B2 (ja) | 無方向性電磁鋼板の製造方法 | |
| EP1473371B1 (fr) | Procédé de fabrication de tole d'acier magnétique à grains non orientés et tole obtenue par le procédé | |
| EP0835945B1 (fr) | Tôle d'acier laminé à chaud pour emboutissage profond | |
| FR2835001A1 (fr) | Procede de fabrication d'une tole d'acier magnetique, toles et pieces obtenues |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20030512 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040616 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040616 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040616 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 60103933 Country of ref document: DE Date of ref document: 20040722 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040916 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040916 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20040616 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041231 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2223961 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050317 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041116 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20201126 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20201124 Year of fee payment: 20 Ref country code: FI Payment date: 20201123 Year of fee payment: 20 Ref country code: FR Payment date: 20201120 Year of fee payment: 20 Ref country code: IT Payment date: 20201123 Year of fee payment: 20 Ref country code: LU Payment date: 20201124 Year of fee payment: 20 Ref country code: CH Payment date: 20201119 Year of fee payment: 20 Ref country code: AT Payment date: 20201123 Year of fee payment: 20 Ref country code: GB Payment date: 20201123 Year of fee payment: 20 Ref country code: DE Payment date: 20201119 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20201124 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20210107 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 60103933 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20211219 |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: MAE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20211219 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MK Effective date: 20211220 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 269421 Country of ref document: AT Kind code of ref document: T Effective date: 20211220 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20220405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20211221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20211220 |