EP2143817A2 - Nahtloses stahlrohr für aufwältigungssteigrohr und herstellungsverfahren - Google Patents
Nahtloses stahlrohr für aufwältigungssteigrohr und herstellungsverfahren Download PDFInfo
- Publication number
- EP2143817A2 EP2143817A2 EP08753716A EP08753716A EP2143817A2 EP 2143817 A2 EP2143817 A2 EP 2143817A2 EP 08753716 A EP08753716 A EP 08753716A EP 08753716 A EP08753716 A EP 08753716A EP 2143817 A2 EP2143817 A2 EP 2143817A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- max
- tube
- work
- seamless steel
- mpa
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 229910000831 Steel Inorganic materials 0.000 title claims abstract description 31
- 239000010959 steel Substances 0.000 title claims abstract description 31
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 27
- 238000000034 method Methods 0.000 claims abstract description 33
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims abstract description 19
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 claims abstract description 18
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims abstract description 18
- 229910052799 carbon Inorganic materials 0.000 claims abstract description 14
- 239000011651 chromium Substances 0.000 claims abstract description 11
- 239000010949 copper Substances 0.000 claims abstract description 11
- 229910052739 hydrogen Inorganic materials 0.000 claims abstract description 11
- 239000001257 hydrogen Substances 0.000 claims abstract description 11
- 239000011572 manganese Substances 0.000 claims abstract description 11
- 239000010955 niobium Substances 0.000 claims abstract description 11
- 239000010936 titanium Substances 0.000 claims abstract description 11
- 239000011575 calcium Substances 0.000 claims abstract description 10
- 229910052804 chromium Inorganic materials 0.000 claims abstract description 10
- 229910052802 copper Inorganic materials 0.000 claims abstract description 10
- 229910052748 manganese Inorganic materials 0.000 claims abstract description 10
- 229910052750 molybdenum Inorganic materials 0.000 claims abstract description 10
- 229910052758 niobium Inorganic materials 0.000 claims abstract description 10
- 229910052698 phosphorus Inorganic materials 0.000 claims abstract description 10
- 229910052719 titanium Inorganic materials 0.000 claims abstract description 10
- ZOXJGFHDIHLPTG-UHFFFAOYSA-N Boron Chemical compound [B] ZOXJGFHDIHLPTG-UHFFFAOYSA-N 0.000 claims abstract description 9
- OYPRJOBELJOOCE-UHFFFAOYSA-N Calcium Chemical compound [Ca] OYPRJOBELJOOCE-UHFFFAOYSA-N 0.000 claims abstract description 9
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims abstract description 9
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims abstract description 9
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims abstract description 9
- PWHULOQIROXLJO-UHFFFAOYSA-N Manganese Chemical compound [Mn] PWHULOQIROXLJO-UHFFFAOYSA-N 0.000 claims abstract description 9
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 claims abstract description 9
- OAICVXFJPJFONN-UHFFFAOYSA-N Phosphorus Chemical compound [P] OAICVXFJPJFONN-UHFFFAOYSA-N 0.000 claims abstract description 9
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 claims abstract description 9
- NINIDFKCEFEMDL-UHFFFAOYSA-N Sulfur Chemical compound [S] NINIDFKCEFEMDL-UHFFFAOYSA-N 0.000 claims abstract description 9
- ATJFFYVFTNAWJD-UHFFFAOYSA-N Tin Chemical compound [Sn] ATJFFYVFTNAWJD-UHFFFAOYSA-N 0.000 claims abstract description 9
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 claims abstract description 9
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910052782 aluminium Inorganic materials 0.000 claims abstract description 9
- 229910052785 arsenic Inorganic materials 0.000 claims abstract description 9
- RQNWIZPPADIBDY-UHFFFAOYSA-N arsenic atom Chemical compound [As] RQNWIZPPADIBDY-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910052796 boron Inorganic materials 0.000 claims abstract description 9
- 229910052791 calcium Inorganic materials 0.000 claims abstract description 9
- 239000012535 impurity Substances 0.000 claims abstract description 9
- 229910052742 iron Inorganic materials 0.000 claims abstract description 9
- 239000011733 molybdenum Substances 0.000 claims abstract description 9
- 229910052759 nickel Inorganic materials 0.000 claims abstract description 9
- GUCVJGMIXFAOAE-UHFFFAOYSA-N niobium atom Chemical compound [Nb] GUCVJGMIXFAOAE-UHFFFAOYSA-N 0.000 claims abstract description 9
- 229910052757 nitrogen Inorganic materials 0.000 claims abstract description 9
- 239000011574 phosphorus Substances 0.000 claims abstract description 9
- 229910052710 silicon Inorganic materials 0.000 claims abstract description 9
- 239000010703 silicon Substances 0.000 claims abstract description 9
- 229910052717 sulfur Inorganic materials 0.000 claims abstract description 9
- 239000011593 sulfur Substances 0.000 claims abstract description 9
- 125000004435 hydrogen atom Chemical class [H]* 0.000 claims abstract 5
- 238000012360 testing method Methods 0.000 claims description 36
- 229910000734 martensite Inorganic materials 0.000 claims description 33
- 239000000463 material Substances 0.000 claims description 27
- 238000010791 quenching Methods 0.000 claims description 19
- 230000009466 transformation Effects 0.000 claims description 18
- 238000010438 heat treatment Methods 0.000 claims description 16
- 238000007689 inspection Methods 0.000 claims description 15
- 238000003754 machining Methods 0.000 claims description 11
- 238000009659 non-destructive testing Methods 0.000 claims description 10
- 239000000203 mixture Substances 0.000 claims description 9
- 230000000171 quenching effect Effects 0.000 claims description 8
- 238000005096 rolling process Methods 0.000 claims description 8
- 238000009658 destructive testing Methods 0.000 claims description 6
- 238000009864 tensile test Methods 0.000 claims description 6
- 238000011179 visual inspection Methods 0.000 claims description 6
- 238000005303 weighing Methods 0.000 claims description 6
- 239000008186 active pharmaceutical agent Substances 0.000 claims description 5
- 238000005496 tempering Methods 0.000 claims description 5
- 239000012085 test solution Substances 0.000 claims description 4
- 230000007797 corrosion Effects 0.000 description 11
- 238000005260 corrosion Methods 0.000 description 11
- 238000012512 characterization method Methods 0.000 description 5
- 238000005553 drilling Methods 0.000 description 5
- LFQSCWFLJHTTHZ-UHFFFAOYSA-N Ethanol Chemical compound CCO LFQSCWFLJHTTHZ-UHFFFAOYSA-N 0.000 description 4
- 239000007789 gas Substances 0.000 description 4
- 150000002431 hydrogen Chemical class 0.000 description 4
- 239000003921 oil Substances 0.000 description 4
- 230000001066 destructive effect Effects 0.000 description 3
- 239000000243 solution Substances 0.000 description 3
- 239000000126 substance Substances 0.000 description 3
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 description 2
- GRYLNZFGIOXLOG-UHFFFAOYSA-N Nitric acid Chemical compound O[N+]([O-])=O GRYLNZFGIOXLOG-UHFFFAOYSA-N 0.000 description 2
- 238000005452 bending Methods 0.000 description 2
- 238000005266 casting Methods 0.000 description 2
- 239000006185 dispersion Substances 0.000 description 2
- 235000019441 ethanol Nutrition 0.000 description 2
- 229910017604 nitric acid Inorganic materials 0.000 description 2
- 230000003287 optical effect Effects 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 229910045601 alloy Inorganic materials 0.000 description 1
- 239000000956 alloy Substances 0.000 description 1
- 238000005275 alloying Methods 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 238000005242 forging Methods 0.000 description 1
- 230000002706 hydrostatic effect Effects 0.000 description 1
- 238000009863 impact test Methods 0.000 description 1
- 239000004576 sand Substances 0.000 description 1
- 238000005204 segregation Methods 0.000 description 1
Images



Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/08—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for tubular bodies or pipes
- C21D9/085—Cooling or quenching
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/22—Ferrous alloys, e.g. steel alloys containing chromium with molybdenum or tungsten
-
- E—FIXED CONSTRUCTIONS
- E21—EARTH OR ROCK DRILLING; MINING
- E21B—EARTH OR ROCK DRILLING; OBTAINING OIL, GAS, WATER, SOLUBLE OR MELTABLE MATERIALS OR A SLURRY OF MINERALS FROM WELLS
- E21B17/00—Drilling rods or pipes; Flexible drill strings; Kellies; Drill collars; Sucker rods; Cables; Casings; Tubings
- E21B17/01—Risers
Definitions
- This invention relates to a seamless steel tube for risers used in work-over operations.
- the requirements for operating a well in the seabed involve a plurality or systems and equipment including drilling, production and work-over risers.
- a drilling riser is a pipe between a seabed blow-out preventer (BOP) and a floating drilling rig which is a drilling unit not permanently fixed to the seabed such as a drillship, a semi-submersible or jack-up unit.
- BOP seabed blow-out preventer
- a drilling rig is meant to be the derrick and its associated machinery.
- a production riser is a pipeline carrying oil or gas that joins a seabed wellhead to a deck of a production platform or a tanker loading platform.
- a work-over riser is a flowline which is used to carry on a well work-over, which is performed on an existing well and may involve re-evaluating the production formation, clearing sand from producing zones, jet lifting, replacing downhole equipment, deepening the well, acidizing or fracturing or improving the drive mechanism.
- these pipes need to have a good welding performance just to be welded to weld-on-connectors to build the string.
- a first object of the invention is to provide a seamless steel tube to be used as a riser in work-over operations with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter to reduce the weight of the riser string.
- a second object is to provide a seamless steel tube for the application as a work-over riser with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter to reduce the bending loads in the wellhead and the platform interface.
- a third object of the invention is to provide a method of manufacturing of a seamless steel tube for the application as a work-over riser with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter using upsetting techniques.
- a fourth object of the invention is to provide a method of manufacturing of a seamless steel tube for the application as a work-over riser with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter using machining techniques.
- a fifth object of the invention is to provide a method of manufacturing of a seamless steel tube for the application as a work-over riser with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter able to guarantee the mechanical characteristics to have high fatigue and corrosion resistance and a good welding performance.
- the tubes used as work-over risers may be reused meaning an economical saving.
- the present invention describes a seamless steel tube to be used as a riser in work-over operations with a specific chemistry design and microstructure consisting of a geometry in which ends of the tube have an increased wall thickness and outer diameter.
- the alloy design is based on high strength requirements.
- the main features of the chemical composition of the tube include 0.23-0.28 wt % C, 0.45 -0.65 wt % Mn, and other alloying elements such as Mo, and Cr to achieve the required percentage of martensitic transformation.
- microalloying elements such as Ti and Nb are used as grain refiners.
- the production route for manufacturing the upset seamless pipe for the application of as Work Over Riser includes the following steps: steel casting (Continuous Cast Bar), seamless pipe rolling (MPM process), pipe ends upsetting, heat treatment, destructive testing (including microcleanliness, austenitic grain size, calculate % of martensitic transformation, tensile, hardness, toughness, SSC testing), dimensional control of pipe body and upset ends (outside diameter, out of roundness, excentricity, straightness, internal diameter, length), machining of external and internal upset end, dimensional control (internal diameter, outside diameter and machined length), drift testing at the upset ends, non-destructive testing (NDT) of upset ends, weighing, measuring and marking, external surface visual inspection, UT inspection of pipe body and UT inspection of upset ends (cylindrical section only).
- the production route for manufacturing the machining seamless pipe for the application of as Work Over Riser includes the following steps: steel casting (Continuous Cast Bar), seamless pipe rolling (MPM process), heat treatment, destructive testing (including microcleanliness, austenitic grain size, calculate % of martensitic transformation, tensile, hardness, toughness, SSC testing), dimensional control of pipe body (outside diameter, out of roundness, straightness, internal diameter, length), machining from external surface the complete length of the pipe by programming CNC lath machine in order to achieve final dimensions at the ends, dimensional control (internal diameter, outside diameter, out of roundness, straightness, and length) of pipe body and machined ends, drift testing at the ends, non-destructive testing (NDT) of ends, weighing, measuring and marking, external surface visual inspection, UT inspection of machined pipe body and UT inspection of ends (cylindrical section only).
- the chemical composition of the seamless steel tube of the present invention comprises in weight per cent: carbon 0.23-0.29, manganese 0.45-0.65, silicon 0.15-0.35, chromium 0.90-1.20, molybdenum 0.70- 0.90, nickel 0.20 max, nitrogen 0.010 max, boron 0.0010-0.0030, aluminum 0.010-0.045, sulfur 0.005 max, phosphorus 0.015 max, titanium 0.005-0.030, niobium 0.020-0.035, copper 0.15 max, arsenic 0.020 max, calcium 0.0040 max, tin 0.020 max, hydrogen 2.4 ppm max, the rest are iron and inevitable impurities.
- a more preferred composition comprises: carbon 0.25-0.28, manganese 0.48-0.58, silicon 0.20-0.30, chromium 1.05-1.15, molybdenum 0.80- 0.83, nickel 0.10 max, nitrogen 0.008 max, boron 0.0016-0.0026, aluminum 0.015-0.045, sulfur 0.0030 max, phosphorus 0.010 max, titanium 0.016-0.026, niobium 0.025-0.030, copper 0.10 max, arsenic 0.020 max, calcium 0.0040 max, tin 0.015 max, hydrogen 2.0 ppm max, the rest are iron and inevitable impurities.
- the seamless steel tubes have a geometry, in which ends of tubes have an increased wall thickness and outer diameter, and following mechanical properties:
- the geometry of seamless steel tube of the present invention and the mechanical characteristics are obtained by two methods of manufacturing: upsetting and machining.
- the upsetting manufacturing method comprises the following steps:
- the machining manufacturing method comprises the following steps:
- Both methods are also performed providing a seamless steel pipe with the preferred composition, as disclosed above.
- the seamless steel tube of the present invention may be divided into two zones. As shown in Figure 1 , there is an increased wall thickness and diameter end with internal and external length (upsetting or machined zone) and the tube body. Due to a combination of the manufacturing methods and the chemistry design, both the whole tube body and the ends have the same yield strength of at least 620 MPa (90 ksi) (YS) and at most 724 MPa (105 ksi), a Yield to Tensile Ratio not greater than 0.92, also, the same ultimate tensile strength (UTS) of at least 690 MPa (100 ksi), elongation of at least 18%, hardness Rockwell of at most 25.4 HRC (value as per API 5CT means average per row) and corrosion resistance (Compliance with NACE, acceptance criteria: Passing SSC Method A test as per NACE TM0177-2005, using test solution (a), testing at 85%SMYS, test period 720 hours). Prior Austenitic Grain Size is 5 or less. The product
- the tubes may be utilized in sour and non-sour service.
- the tubes' nominal diameter to be upsetted ends may be from 4 1 ⁇ 2" to 10 3 ⁇ 4".
- the tubes' nominal diameter which ends will to be machined may be from 4 1 ⁇ 2" to 18" due to the manufacturing facilities.
- the tubes' thickness ranges from 10 mm to 50 mm.
- the upsetting manufacturing operation was performed following the steps of:
- the austenitic grain size was measured on as-quenched material by the saturation method as per ASTM E-112. As shown in Figure 6 , the grain size reported on the samples were 9/10 in the pipe body which was above the required size since the minimum required was 5. The upset samples showed a grain size of 8/9 and 9/10 complying with the specifications as illustrated in Figure 6 .
- the transversal face to the rolling axis was metallographically prepared and etched with Nital 2% to perform microstructural observations with an optical microscope.
- Nital Solution of 2% of Nitric acid in Ethyl Alcohol.
- microstructures observed in as-quenched material were mainly martensitic with over 95% of martensitic transformation through the entire thickness of the pipe on both pipe body and upset which indicates that the temperature at which the pipe entered the quenching stage and the quenching itself were homogeneous.
- the microstructures observed in tempered material, tempered martensite was present through the thickness.
- the pipe was rolled in a heavy wall condition.
- the wall thickness was about 44 mm.
- Example 2 As in Example 1, a mechanical characterization was performed, calculating the % of martensitic transformation from the as-quenched material. On the quenched and tempered material, tensile, hardness, and toughness tests were performed on both machined ends and pipe body sections. Specifications were met; good hardenability, yield strength values of over 94 ksi as-tempered HRC values below the maximum allowed (25.4 HRC) and absorbed energy higher than 100 Joules at the specified temperature of -20°C.
- Homogeneity in tensile properties, hardness and toughness test results are a consequence of a very homogenous microstructure through the wall on both machined ends and pipe body in the as quenched and tempered condition.
- Microstructural observations of as-quenched material at the pipe machined body and the ends zones reveal a prior austenitic grain size of 8/9 in both zones measured by the saturation method as per ASTM E-112.
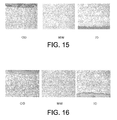
- the modified end on the analyzed sample showed a grain size of 8/9 complying with the specifications as shown in Figure 12 .
- the transversal face to the rolling axis was metallographically prepared and etched with Nital 2% to perform microstructural observations with an optical microscope.
- Nital Solution of 2% of Nitric acid in Ethyl Alcohol.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Geology (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Life Sciences & Earth Sciences (AREA)
- Mining & Mineral Resources (AREA)
- Environmental & Geological Engineering (AREA)
- Fluid Mechanics (AREA)
- General Life Sciences & Earth Sciences (AREA)
- Geochemistry & Mineralogy (AREA)
- Heat Treatment Of Articles (AREA)
- Heat Treatment Of Steel (AREA)
- Metal Extraction Processes (AREA)
- Rod-Shaped Construction Members (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| MX2007004600A MX2007004600A (es) | 2007-04-17 | 2007-04-17 | Un tubo sin costura para la aplicación como secciones verticales de work-over. |
| PCT/MX2008/000054 WO2008127084A2 (es) | 2007-04-17 | 2008-04-17 | Un tubo de acero sin costura para la aplicación como columnas ascendientes de work-over y método para fabricar el mismo |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP2143817A2 true EP2143817A2 (de) | 2010-01-13 |
Family
ID=39673395
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08753716A Withdrawn EP2143817A2 (de) | 2007-04-17 | 2008-04-17 | Nahtloses stahlrohr für aufwältigungssteigrohr und herstellungsverfahren |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US20100193085A1 (de) |
| EP (1) | EP2143817A2 (de) |
| AR (1) | AR066080A1 (de) |
| BR (1) | BRPI0810005A2 (de) |
| CA (1) | CA2682959A1 (de) |
| MX (1) | MX2007004600A (de) |
| NO (1) | NO20093069L (de) |
| WO (1) | WO2008127084A2 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2181240B1 (de) * | 2007-07-02 | 2018-08-29 | Forum US, Inc. | Zentrierstruktur für ein röhrenförmiges glied und herstellungsverfahren dafür |
| CN109161650A (zh) * | 2018-10-30 | 2019-01-08 | 中车戚墅堰机车车辆工艺研究所有限公司 | 一种低合金铸钢、制造方法及其应用 |
Families Citing this family (30)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1627931B1 (de) | 2003-04-25 | 2017-05-31 | Tubos De Acero De Mexico, S.A. | Nahtloses stahlrohr, das zur verwendung als führungsrohr vorgesehen ist, und herstellungsverfahren dafür |
| MXPA05008339A (es) * | 2005-08-04 | 2007-02-05 | Tenaris Connections Ag | Acero de alta resistencia para tubos de acero soldables y sin costura. |
| KR101340165B1 (ko) | 2006-06-29 | 2013-12-10 | 테나리스 커넥션즈 아.게. | 저온에서 개선된 등방성 인성을 갖는 유압 실린더용 무계목정밀 강철 튜브 및 그것의 제조방법 |
| US7862667B2 (en) | 2007-07-06 | 2011-01-04 | Tenaris Connections Limited | Steels for sour service environments |
| US8328960B2 (en) | 2007-11-19 | 2012-12-11 | Tenaris Connections Limited | High strength bainitic steel for OCTG applications |
| MX2009012811A (es) * | 2008-11-25 | 2010-05-26 | Maverick Tube Llc | Procesamiento de desbastes delgados o flejes compactos de aceros al boro/titanio. |
| US20100319814A1 (en) * | 2009-06-17 | 2010-12-23 | Teresa Estela Perez | Bainitic steels with boron |
| EP2325435B2 (de) | 2009-11-24 | 2020-09-30 | Tenaris Connections B.V. | Verschraubung für [ultrahoch] abgedichteten internen und externen Druck |
| US9163296B2 (en) | 2011-01-25 | 2015-10-20 | Tenaris Coiled Tubes, Llc | Coiled tube with varying mechanical properties for superior performance and methods to produce the same by a continuous heat treatment |
| IT1403689B1 (it) | 2011-02-07 | 2013-10-31 | Dalmine Spa | Tubi in acciaio ad alta resistenza con eccellente durezza a bassa temperatura e resistenza alla corrosione sotto tensioni da solfuri. |
| IT1403688B1 (it) | 2011-02-07 | 2013-10-31 | Dalmine Spa | Tubi in acciaio con pareti spesse con eccellente durezza a bassa temperatura e resistenza alla corrosione sotto tensione da solfuri. |
| US8636856B2 (en) | 2011-02-18 | 2014-01-28 | Siderca S.A.I.C. | High strength steel having good toughness |
| US8414715B2 (en) | 2011-02-18 | 2013-04-09 | Siderca S.A.I.C. | Method of making ultra high strength steel having good toughness |
| RU2464327C1 (ru) * | 2011-07-27 | 2012-10-20 | ООО "Компания ИжТехМаш" | Способ изготовления трубы для технологических нужд нефтяных скважин |
| US9340847B2 (en) | 2012-04-10 | 2016-05-17 | Tenaris Connections Limited | Methods of manufacturing steel tubes for drilling rods with improved mechanical properties, and rods made by the same |
| CA2870113C (en) * | 2012-04-27 | 2017-05-09 | Nippon Steel & Sumitomo Metal Corporation | Seamless steel pipe and method for producing the same |
| RU2500821C1 (ru) * | 2012-08-20 | 2013-12-10 | Кирилл Алексеевич Иванов | Способ термомеханической обработки трубы |
| BR112015016765A2 (pt) | 2013-01-11 | 2017-07-11 | Tenaris Connections Ltd | conexão de tubos de perfuração, tubo de perfuração correspondente e método para montar tubos de perfuração |
| US9187811B2 (en) | 2013-03-11 | 2015-11-17 | Tenaris Connections Limited | Low-carbon chromium steel having reduced vanadium and high corrosion resistance, and methods of manufacturing |
| US9803256B2 (en) | 2013-03-14 | 2017-10-31 | Tenaris Coiled Tubes, Llc | High performance material for coiled tubing applications and the method of producing the same |
| EP2789700A1 (de) | 2013-04-08 | 2014-10-15 | DALMINE S.p.A. | Dickwandige vergütete und nahtlose Stahlrohre und entsprechendes Verfahren zur Herstellung der Stahlrohre |
| EP2789701A1 (de) | 2013-04-08 | 2014-10-15 | DALMINE S.p.A. | Hochfeste mittelwandige vergütete und nahtlose Stahlrohre und entsprechendes Verfahren zur Herstellung der Stahlrohre |
| KR102197204B1 (ko) | 2013-06-25 | 2021-01-04 | 테나리스 커넥션즈 비.브이. | 고크롬 내열철강 |
| US20160305192A1 (en) | 2015-04-14 | 2016-10-20 | Tenaris Connections Limited | Ultra-fine grained steels having corrosion-fatigue resistance |
| US11085277B2 (en) * | 2015-10-07 | 2021-08-10 | Benteler Steel/Tube Gmbh | Seamless steel pipe, method of producing a high strength seamless steel pipe, usage of a seamless steel pipe and perforation gun |
| WO2017149570A1 (ja) * | 2016-02-29 | 2017-09-08 | Jfeスチール株式会社 | 油井用低合金高強度継目無鋼管 |
| US11124852B2 (en) | 2016-08-12 | 2021-09-21 | Tenaris Coiled Tubes, Llc | Method and system for manufacturing coiled tubing |
| US10434554B2 (en) | 2017-01-17 | 2019-10-08 | Forum Us, Inc. | Method of manufacturing a coiled tubing string |
| WO2019023536A1 (en) * | 2017-07-27 | 2019-01-31 | Enventure Global Technology, Inc. | DILATABLE CONNECTION BY DISCHARGE |
| EP4190935A1 (de) | 2021-12-06 | 2023-06-07 | Benteler Steel/Tube GmbH | Perforationspistolenrohr und perforationspistole |
Family Cites Families (65)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3413166A (en) * | 1965-10-15 | 1968-11-26 | Atomic Energy Commission Usa | Fine grained steel and process for preparation thereof |
| US3655465A (en) * | 1969-03-10 | 1972-04-11 | Int Nickel Co | Heat treatment for alloys particularly steels to be used in sour well service |
| DE2131318C3 (de) * | 1971-06-24 | 1973-12-06 | Fried. Krupp Huettenwerke Ag, 4630 Bochum | Verfahren zum Herstellen eines Beweh rungs Stabstahles für Spannbeton |
| US3915697A (en) * | 1975-01-31 | 1975-10-28 | Centro Speriment Metallurg | Bainitic steel resistant to hydrogen embrittlement |
| GB2023668B (en) * | 1978-04-28 | 1982-10-13 | Neturen Co Ltd | Steel for cold plastic working |
| US4231555A (en) * | 1978-06-12 | 1980-11-04 | Horikiri Spring Manufacturing Co., Ltd. | Bar-shaped torsion spring |
| DE3070501D1 (en) * | 1979-06-29 | 1985-05-23 | Nippon Steel Corp | High tensile steel and process for producing the same |
| US4281716A (en) | 1979-08-13 | 1981-08-04 | Standard Oil Company (Indiana) | Flexible workover riser system |
| JPS5680367A (en) * | 1979-12-06 | 1981-07-01 | Nippon Steel Corp | Restraining method of cracking in b-containing steel continuous casting ingot |
| US4376528A (en) * | 1980-11-14 | 1983-03-15 | Kawasaki Steel Corporation | Steel pipe hardening apparatus |
| JPS58188532A (ja) * | 1982-04-28 | 1983-11-04 | Nhk Spring Co Ltd | 中空スタビライザの製造方法 |
| JPS61130462A (ja) * | 1984-11-28 | 1986-06-18 | Tech Res & Dev Inst Of Japan Def Agency | 降伏応力110kgf/mm↑2以上の耐応力腐蝕割れ性のすぐれた高靭性超高張力鋼 |
| DE3666461D1 (en) * | 1985-06-10 | 1989-11-23 | Hoesch Ag | Method and use of a steel for manufacturing steel pipes with a high resistance to acid gases |
| US4812182A (en) * | 1987-07-31 | 1989-03-14 | Hongsheng Fang | Air-cooling low-carbon bainitic steel |
| US5538566A (en) * | 1990-10-24 | 1996-07-23 | Consolidated Metal Products, Inc. | Warm forming high strength steel parts |
| IT1263251B (it) * | 1992-10-27 | 1996-08-05 | Sviluppo Materiali Spa | Procedimento per la produzione di manufatti in acciaio inossidabile super-duplex. |
| US5454883A (en) * | 1993-02-02 | 1995-10-03 | Nippon Steel Corporation | High toughness low yield ratio, high fatigue strength steel plate and process of producing same |
| JPH07266837A (ja) * | 1994-03-29 | 1995-10-17 | Horikiri Bane Seisakusho:Kk | 中空スタビライザの製造法 |
| IT1267243B1 (it) * | 1994-05-30 | 1997-01-28 | Danieli Off Mecc | Procedimento di colata continua per acciai peritettici |
| GB2297094B (en) * | 1995-01-20 | 1998-09-23 | British Steel Plc | Improvements in and relating to Carbide-Free Bainitic Steels |
| JP3755163B2 (ja) * | 1995-05-15 | 2006-03-15 | 住友金属工業株式会社 | 耐硫化物応力割れ性に優れた高強度継目無鋼管の製造方法 |
| IT1275287B (it) * | 1995-05-31 | 1997-08-05 | Dalmine Spa | Acciaio inossidabile supermartensitico avente elevata resistenza meccanica ed alla corrosione e relativi manufatti |
| GB9621195D0 (en) | 1996-10-11 | 1996-11-27 | Kvaerner Eng | Off-shore oil or gas production unit |
| ES2159155T3 (es) * | 1997-01-15 | 2001-09-16 | Mannesmann Ag | Procedimiento para la fabricacion de tubos sin costura para tuberias con limite de estirado estable a temperaturas de utilizacion elevadas. |
| CA2231985C (en) * | 1997-03-26 | 2004-05-25 | Sumitomo Metal Industries, Ltd. | Welded high-strength steel structures and methods of manufacturing the same |
| EP0878334B1 (de) * | 1997-05-12 | 2003-09-24 | Firma Muhr und Bender | Stabilisator |
| US5993570A (en) * | 1997-06-20 | 1999-11-30 | American Cast Iron Pipe Company | Linepipe and structural steel produced by high speed continuous casting |
| DE19725434C2 (de) * | 1997-06-16 | 1999-08-19 | Schloemann Siemag Ag | Verfahren zum Walzen von Warmbreitband in einer CSP-Anlage |
| EP0995809B1 (de) * | 1997-09-29 | 2004-02-04 | Sumitomo Metal Industries Limited | Stahl für ölbohrlochrohre mit hohem korrosionswiderstand gegen feuchtes kohlendioxidgas und mit hohem korrosionswiderstand gegen seewasser, sowie nahtlose ölbohrlochrohre |
| JP3562353B2 (ja) * | 1998-12-09 | 2004-09-08 | 住友金属工業株式会社 | 耐硫化物応力腐食割れ性に優れる油井用鋼およびその製造方法 |
| JP4331300B2 (ja) * | 1999-02-15 | 2009-09-16 | 日本発條株式会社 | 中空スタビライザの製造方法 |
| JP4264212B2 (ja) * | 2000-02-28 | 2009-05-13 | 新日本製鐵株式会社 | 成形性の優れた鋼管及びその製造方法 |
| US6384388B1 (en) * | 2000-11-17 | 2002-05-07 | Meritor Suspension Systems Company | Method of enhancing the bending process of a stabilizer bar |
| KR100513991B1 (ko) * | 2001-02-07 | 2005-09-09 | 제이에프이 스틸 가부시키가이샤 | 박강판의 제조방법 |
| US7048811B2 (en) * | 2001-03-07 | 2006-05-23 | Nippon Steel Corporation | Electric resistance-welded steel pipe for hollow stabilizer |
| AR027650A1 (es) * | 2001-03-13 | 2003-04-09 | Siderca Sa Ind & Com | Acero al carbono de baja aleacion para la fabricacion de tuberias para exploracion y produccion de petroleo y/o gas natural, con mejorada resistencia a lacorrosion, procedimiento para fabricar tubos sin costura y tubos sin costura obtenidos |
| EP1375683B1 (de) * | 2001-03-29 | 2012-02-08 | Sumitomo Metal Industries, Ltd. | Hochfestes stahlrohr für airbag und herstellungsverfahren dafür |
| JP2003041341A (ja) * | 2001-08-02 | 2003-02-13 | Sumitomo Metal Ind Ltd | 高靱性を有する鋼材およびそれを用いた鋼管の製造方法 |
| US6669789B1 (en) * | 2001-08-31 | 2003-12-30 | Nucor Corporation | Method for producing titanium-bearing microalloyed high-strength low-alloy steel |
| NO315284B1 (no) * | 2001-10-19 | 2003-08-11 | Inocean As | Stigerör for forbindelse mellom et fartöy og et punkt på havbunnen |
| DE10160942A1 (de) * | 2001-12-12 | 2003-06-18 | Daimler Chrysler Ag | Gebautes Ventil für Hubkolbenmaschinen |
| CN1327023C (zh) * | 2002-03-29 | 2007-07-18 | 住友金属工业株式会社 | 低合金钢 |
| US6669285B1 (en) * | 2002-07-02 | 2003-12-30 | Eric Park | Headrest mounted video display |
| US7074286B2 (en) * | 2002-12-18 | 2006-07-11 | Ut-Battelle, Llc | Wrought Cr—W—V bainitic/ferritic steel compositions |
| US7010950B2 (en) * | 2003-01-17 | 2006-03-14 | Visteon Global Technologies, Inc. | Suspension component having localized material strengthening |
| EP1627931B1 (de) * | 2003-04-25 | 2017-05-31 | Tubos De Acero De Mexico, S.A. | Nahtloses stahlrohr, das zur verwendung als führungsrohr vorgesehen ist, und herstellungsverfahren dafür |
| US20050087269A1 (en) * | 2003-10-22 | 2005-04-28 | Merwin Matthew J. | Method for producing line pipe |
| WO2005090615A1 (ja) * | 2004-03-24 | 2005-09-29 | Sumitomo Metal Industries, Ltd. | 耐食性に優れた低合金鋼の製造方法 |
| JP4140556B2 (ja) * | 2004-06-14 | 2008-08-27 | 住友金属工業株式会社 | 耐硫化物応力割れ性に優れた低合金油井管用鋼 |
| JP4135691B2 (ja) * | 2004-07-20 | 2008-08-20 | 住友金属工業株式会社 | 窒化物系介在物形態制御鋼 |
| JP2006037147A (ja) * | 2004-07-26 | 2006-02-09 | Sumitomo Metal Ind Ltd | 油井管用鋼材 |
| US20060169368A1 (en) * | 2004-10-05 | 2006-08-03 | Tenaris Conncections A.G. (A Liechtenstein Corporation) | Low carbon alloy steel tube having ultra high strength and excellent toughness at low temperature and method of manufacturing the same |
| US7566416B2 (en) * | 2004-10-29 | 2009-07-28 | Sumitomo Metal Industries, Ltd. | Steel pipe for an airbag inflator and a process for its manufacture |
| JP4792778B2 (ja) * | 2005-03-29 | 2011-10-12 | 住友金属工業株式会社 | ラインパイプ用厚肉継目無鋼管の製造方法 |
| US20060243355A1 (en) * | 2005-04-29 | 2006-11-02 | Meritor Suspension System Company, U.S. | Stabilizer bar |
| MXPA05008339A (es) * | 2005-08-04 | 2007-02-05 | Tenaris Connections Ag | Acero de alta resistencia para tubos de acero soldables y sin costura. |
| WO2007023805A1 (ja) * | 2005-08-22 | 2007-03-01 | Sumitomo Metal Industries, Ltd. | ラインパイプ用継目無鋼管とその製造方法 |
| US7744708B2 (en) * | 2006-03-14 | 2010-06-29 | Tenaris Connections Limited | Methods of producing high-strength metal tubular bars possessing improved cold formability |
| KR101340165B1 (ko) * | 2006-06-29 | 2013-12-10 | 테나리스 커넥션즈 아.게. | 저온에서 개선된 등방성 인성을 갖는 유압 실린더용 무계목정밀 강철 튜브 및 그것의 제조방법 |
| US8322754B2 (en) * | 2006-12-01 | 2012-12-04 | Tenaris Connections Limited | Nanocomposite coatings for threaded connections |
| US20080226396A1 (en) * | 2007-03-15 | 2008-09-18 | Tubos De Acero De Mexico S.A. | Seamless steel tube for use as a steel catenary riser in the touch down zone |
| US7862667B2 (en) * | 2007-07-06 | 2011-01-04 | Tenaris Connections Limited | Steels for sour service environments |
| US8328960B2 (en) * | 2007-11-19 | 2012-12-11 | Tenaris Connections Limited | High strength bainitic steel for OCTG applications |
| MX2009012811A (es) * | 2008-11-25 | 2010-05-26 | Maverick Tube Llc | Procesamiento de desbastes delgados o flejes compactos de aceros al boro/titanio. |
| US20100319814A1 (en) * | 2009-06-17 | 2010-12-23 | Teresa Estela Perez | Bainitic steels with boron |
-
2007
- 2007-04-17 MX MX2007004600A patent/MX2007004600A/es active IP Right Grant
-
2008
- 2008-04-16 AR ARP080101566A patent/AR066080A1/es unknown
- 2008-04-17 US US12/595,167 patent/US20100193085A1/en not_active Abandoned
- 2008-04-17 CA CA002682959A patent/CA2682959A1/en not_active Abandoned
- 2008-04-17 BR BRPI0810005A patent/BRPI0810005A2/pt not_active IP Right Cessation
- 2008-04-17 WO PCT/MX2008/000054 patent/WO2008127084A2/es not_active Ceased
- 2008-04-17 EP EP08753716A patent/EP2143817A2/de not_active Withdrawn
-
2009
- 2009-09-28 NO NO20093069A patent/NO20093069L/no not_active Application Discontinuation
Non-Patent Citations (1)
| Title |
|---|
| See references of WO2008127084A2 * |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2181240B1 (de) * | 2007-07-02 | 2018-08-29 | Forum US, Inc. | Zentrierstruktur für ein röhrenförmiges glied und herstellungsverfahren dafür |
| CN109161650A (zh) * | 2018-10-30 | 2019-01-08 | 中车戚墅堰机车车辆工艺研究所有限公司 | 一种低合金铸钢、制造方法及其应用 |
Also Published As
| Publication number | Publication date |
|---|---|
| BRPI0810005A2 (pt) | 2015-10-27 |
| WO2008127084A2 (es) | 2008-10-23 |
| MX2007004600A (es) | 2008-12-01 |
| AR066080A1 (es) | 2009-07-22 |
| US20100193085A1 (en) | 2010-08-05 |
| WO2008127084A4 (es) | 2009-03-19 |
| CA2682959A1 (en) | 2008-10-23 |
| NO20093069L (no) | 2009-12-30 |
| WO2008127084A3 (es) | 2008-12-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20100193085A1 (en) | Seamless steel pipe for use as vertical work-over sections | |
| EP2650389B1 (de) | Verfahren zur Herstellung von Stahlrohren für Bohrgestänge mit verbesserten mechanischen Eigenschaften | |
| JP4502011B2 (ja) | ラインパイプ用継目無鋼管とその製造方法 | |
| EP2492361B1 (de) | Hochfeste Stahlrohre mit ausgezeichneter Härte bei niedrigen Temperaturen und Sulfidspannungsrisskorrosionfestigkeit | |
| RU2664347C2 (ru) | Высококачественный материал для гибких длинномерных труб и способ его изготовления | |
| US10240221B2 (en) | Stainless steel seamless pipe for oil well use and method for manufacturing the same | |
| EP2484784B1 (de) | Stahlrohre mit schweren Wänden mit ausgezeichneter Härte bei niedrigen Temperaturen und Sulfidspannungsrisskorrosionfestigkeit | |
| EP1546417B1 (de) | Hochfestes nahtloses stahlrohr mit hervorragender beständigkeit gegen der wasserstoffinduzierter rissbildung und herstellungsverfahren dafür | |
| JP6112267B1 (ja) | 継目無鋼管及びその製造方法 | |
| EP2562284B1 (de) | Cr-haltiges stahlrohr für ein leitungsrohr mit hervorragender bruchfestigkeit der durch schweissungshitze betroffenen teile bei intergranularer stresskorrosion | |
| EP2789701A1 (de) | Hochfeste mittelwandige vergütete und nahtlose Stahlrohre und entsprechendes Verfahren zur Herstellung der Stahlrohre | |
| EP2789700A1 (de) | Dickwandige vergütete und nahtlose Stahlrohre und entsprechendes Verfahren zur Herstellung der Stahlrohre | |
| RU2533573C2 (ru) | Профилированная стальная проволока с высокими механическими характеристиками, стойкая к водородному охрупчиванию | |
| EP2565287A1 (de) | Hochfester edelstahl für ein ölbohrloch und hochfestes edelstahlrohr für ein ölbohrloch | |
| US8168008B2 (en) | Martensitic stainless steel pipe | |
| EP3330398B1 (de) | Stahlrohr für ein leitungsrohr und verfahren zur herstellung davon | |
| EP3492612B1 (de) | Hochfestes nahtloses stahlrohr und steigrohr |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20091117 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20100602 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20161101 |