JP4639089B2 - 中空金属管を素材とする内周突起付きリングの製造方法 - Google Patents
中空金属管を素材とする内周突起付きリングの製造方法 Download PDFInfo
- Publication number
- JP4639089B2 JP4639089B2 JP2005002330A JP2005002330A JP4639089B2 JP 4639089 B2 JP4639089 B2 JP 4639089B2 JP 2005002330 A JP2005002330 A JP 2005002330A JP 2005002330 A JP2005002330 A JP 2005002330A JP 4639089 B2 JP4639089 B2 JP 4639089B2
- Authority
- JP
- Japan
- Prior art keywords
- inner peripheral
- ring
- hollow metal
- metal tube
- diameter
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K23/00—Making other articles
- B21K23/04—Making other articles flanged articles
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Forging (AREA)
Description
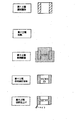
熱間鍛造方法による製造方法が示されており、図8はこの特許文献1に示されている熱間鍛造法を使用した内周突起付きリングの製造工程の説明図である。
外径D0:79mm
内径D1:65.9mm 肉厚TA:6.55mm
突起部 内径D2:61.8mm
肉厚TB:8.6mm
長さ B:40.2mm
素材寸法
外径:79mm
内径:65.2mm 肉厚:6.9mm
長さ:37.6mm
材質:SUJ2(HRB105以下)
上下の金型寸法:
大径部 外径79mm×高さ50mm
円柱部 外径65.9mm×高さ16.7mm
突出部 外径62.8mm×高さ2.5mm
角R R1:1mm R2:6mm R3:1mm
外径拘束用金型
内径80mm
の諸元とした。

2・・・素材(中空金属管)
10・・・内周突起付きリング
11・・・円筒部 12・・・突起部
13・・・内周面(突起部) 14・・・内周面(円筒部)
20・・・上金型(第1金型)
21・・・突出部 22・・・大径部 23・・・円柱部
30・・・下金型(第2金型)
31・・・突出部 32・・・大径部 33・・・円柱部
40・・・外径拘束用金型
Claims (2)
- 内周突起部を有するリングの冷間鍛造方法であって、中空金属管を素材とし、該素材を該素材の外周形状を拘束する円筒形状の外径拘束用金型内に挿入した後、前記リングの内面形状を画定する円柱部と、該円柱部の素材側に備わり前記内周突起部の内周面を形成する面を備え、前記円柱部の直径より小さい直径である突出部と、を各々有し、前記円柱部の角を円弧形状に丸めて前記円柱部と前記突出部の接続部とした第1金型と第2金型により前記素材の軸方向に鍛圧し、該素材の中央部を径方向内側に張出して、前記内周突起部を形成することを特徴とする内周突起付きリングの冷間鍛造方法。
- 前記中空金属管が、継目無鋼管を加工して得た中空金属管であることを特徴とする請求項1に記載の内周突起付きリングの冷間鍛造方法。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2005002330A JP4639089B2 (ja) | 2004-01-07 | 2005-01-07 | 中空金属管を素材とする内周突起付きリングの製造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2004001887 | 2004-01-07 | ||
| JP2005002330A JP4639089B2 (ja) | 2004-01-07 | 2005-01-07 | 中空金属管を素材とする内周突起付きリングの製造方法 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2005219122A JP2005219122A (ja) | 2005-08-18 |
| JP4639089B2 true JP4639089B2 (ja) | 2011-02-23 |
Family
ID=34995169
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2005002330A Expired - Fee Related JP4639089B2 (ja) | 2004-01-07 | 2005-01-07 | 中空金属管を素材とする内周突起付きリングの製造方法 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP4639089B2 (ja) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5669128B2 (ja) * | 2009-08-26 | 2015-02-12 | 山陽特殊製鋼株式会社 | 転動疲労寿命に優れた機械部品の製造方法 |
| JP6083552B2 (ja) * | 2011-03-03 | 2017-02-22 | 山陽特殊製鋼株式会社 | 冷間鍛造によるベアリング素形材の製造方法 |
| CN102699193B (zh) * | 2012-05-30 | 2015-05-13 | 上海锅炉厂有限公司 | 一种压制半环管成型的模具及加工方法 |
| CN114178451B (zh) * | 2021-12-14 | 2024-06-21 | 无锡派克新材料科技股份有限公司 | 一种C形截面Ti64钛合金锻件制坯方法 |
| CN115837443B (zh) * | 2022-10-28 | 2025-07-29 | 贵州航天新力科技有限公司 | 一种内凸台环件成形装置 |
| CN115647270B (zh) * | 2022-11-14 | 2025-03-18 | 遵义航天新力精密铸锻有限公司 | 异形窗锻造净近成型工装及成型工艺 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS61296937A (ja) * | 1985-06-25 | 1986-12-27 | Toyota Motor Corp | 円筒部品の鍛造加工法 |
| JPS63154240A (ja) * | 1986-12-15 | 1988-06-27 | Toyota Motor Corp | 中空ベベルギヤ部品の成形方法 |
| JPH01317638A (ja) * | 1988-06-17 | 1989-12-22 | Kotani Tanko Kk | 自動車用ハブユニット軸受外輪の製造方法及び装置 |
| JP2755716B2 (ja) * | 1989-08-28 | 1998-05-25 | エヌティエヌ株式会社 | 複列玉軸受外輪素形材の鍛造方法 |
| JPH0785821B2 (ja) * | 1992-01-31 | 1995-09-20 | 大同メタル工業株式会社 | ブッシュの成形方法 |
| JP3720922B2 (ja) * | 1996-08-15 | 2005-11-30 | 光洋精工株式会社 | 複列軸受の製造方法および装置 |
| JP2001300668A (ja) * | 2000-04-19 | 2001-10-30 | Sanyo Special Steel Co Ltd | 鋼管切断リングを母材とする内周突起付きリングの製造方法 |
-
2005
- 2005-01-07 JP JP2005002330A patent/JP4639089B2/ja not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| JP2005219122A (ja) | 2005-08-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5309690B2 (ja) | 転がり軸受の内外輪の製造方法 | |
| JP4022472B2 (ja) | ロール縁部を製造する方法 | |
| CN113976789B (zh) | 一种带内外法兰结构的钛合金薄壁超大锥角异形环锻件空心缩径挤压成形工艺方法 | |
| CN112404340B (zh) | 三片式法兰球阀阀盖辗扩锻造成形工艺 | |
| GB2319199A (en) | Die forging system | |
| US20080089631A1 (en) | Raceway Ring for Radial Ball Bearing and Manufacturing Method Thereof, and Manufacturing Method of High Accurate Ring and Manufacturing Apparatus Thereof | |
| US2751676A (en) | Method of cold working metal | |
| CN112207215A (zh) | 多台阶大型异形环件的成形方法 | |
| JP2005219122A (ja) | 中空金属管を素材とする内周突起付きリングの製造方法 | |
| CN105382162B (zh) | 空心钢锭预制的环状坯料的镦粗拔长方法 | |
| JP6123917B2 (ja) | 環状部材の製造方法 | |
| JP2022120828A (ja) | 金属製カップの製造方法 | |
| JPH0152094B2 (ja) | ||
| JPH08508678A (ja) | ホイール・リム | |
| CN110216233B (zh) | 一种厚壁无缝弯头的生产方法 | |
| CN112296228B (zh) | 三片式法兰球阀阀盖辗扩模 | |
| RU2071863C1 (ru) | Способ получения головок торцевых ключей | |
| JP3746828B2 (ja) | 円筒状部品の製造方法 | |
| JP2001300668A (ja) | 鋼管切断リングを母材とする内周突起付きリングの製造方法 | |
| CN105855798B (zh) | 一种绳头锥套的制造方法 | |
| JPS6330095B2 (ja) | ||
| JPH07144247A (ja) | 段付き部品の鍛造金型及び段付き部品の鍛造方法 | |
| JP3240307B2 (ja) | 環状部材の口絞り、口拡げ同時成形加工方法 | |
| JPS6068130A (ja) | 円筒物の成形方法及びその装置 | |
| JP2004351436A (ja) | 成形方法および成形型 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20071203 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20100409 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20100420 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20100618 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20100914 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20101018 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20101102 |
|
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20101129 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20131203 Year of fee payment: 3 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 4639089 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| LAPS | Cancellation because of no payment of annual fees |