WO1999011707A1 - Resin composition - Google Patents
Resin composition Download PDFInfo
- Publication number
- WO1999011707A1 WO1999011707A1 PCT/JP1998/000947 JP9800947W WO9911707A1 WO 1999011707 A1 WO1999011707 A1 WO 1999011707A1 JP 9800947 W JP9800947 W JP 9800947W WO 9911707 A1 WO9911707 A1 WO 9911707A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- resin
- resin composition
- weight
- ethylene
- evoh
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D35/00—Pliable tubular containers adapted to be permanently or temporarily deformed to expel contents, e.g. collapsible tubes for toothpaste or other plastic or semi-liquid material; Holders therefor
- B65D35/02—Body construction
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L29/00—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by an alcohol, ether, aldehydo, ketonic, acetal or ketal radical; Compositions of hydrolysed polymers of esters of unsaturated alcohols with saturated carboxylic acids; Compositions of derivatives of such polymers
- C08L29/02—Homopolymers or copolymers of unsaturated alcohols
- C08L29/04—Polyvinyl alcohol; Partially hydrolysed homopolymers or copolymers of esters of unsaturated alcohols with saturated carboxylic acids
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L101/00—Compositions of unspecified macromolecular compounds
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2205/00—Polymer mixtures characterised by other features
- C08L2205/03—Polymer mixtures characterised by other features containing three or more polymers in a blend
- C08L2205/035—Polymer mixtures characterised by other features containing three or more polymers in a blend containing four or more polymers in a blend
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L23/00—Compositions of homopolymers or copolymers of unsaturated aliphatic hydrocarbons having only one carbon-to-carbon double bond; Compositions of derivatives of such polymers
- C08L23/02—Compositions of homopolymers or copolymers of unsaturated aliphatic hydrocarbons having only one carbon-to-carbon double bond; Compositions of derivatives of such polymers not modified by chemical after-treatment
- C08L23/04—Homopolymers or copolymers of ethene
- C08L23/08—Copolymers of ethene
- C08L23/0846—Copolymers of ethene with unsaturated hydrocarbons containing atoms other than carbon or hydrogen
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L77/00—Compositions of polyamides obtained by reactions forming a carboxylic amide link in the main chain; Compositions of derivatives of such polymers
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/31504—Composite [nonstructural laminate]
- Y10T428/31725—Of polyamide
Definitions
- the present invention provides an ethylene-vinyl alcohol copolymer having excellent barrier properties, mechanical strength, flexibility, stretchability, melt stability, scrap recovery, heat adhesion, paintability, stain resistance, transparency, etc. (A), a polyamide resin (B), an ethylene monounsaturated carboxylic acid random copolymer or a metal salt thereof (C), and a resin other than the resin having a solubility parameter of 11 or less (calculated from the Fedors equation).
- the present invention relates to a resin composition having good compatibility comprising a thermoplastic resin (D).
- Hydrophobic thermoplastic resins such as polyolefins and polystyrene are used in the food packaging field for containers such as films, bottles, cups, etc. due to their excellent melt moldability, secondary processing, mechanical properties, and economy.
- non-food field it is widely used in daily necessities, household appliances, automobile parts, and the like.
- multilayer structures of these resins and ethylene-vinyl alcohol copolymer hereinafter, referred to as EVOH) are widely used in the food field and the like where a barrier property against oxygen, flavor and the like is required.
- EV0H is a highly hydrophilic resin, and has a problem of compatibility when blended with a hydrophobic thermoplastic resin, and has a problem that a resin composition having good physical properties cannot be obtained.
- polyolefin resins with polar functional groups have been replaced.
- Various compatibilizers represented are being studied, but their effects are not always sufficient, and the development of a high-performance compatibilizer that allows both to be well compatible is desired.
- thermoplastic single-layer barrier material with barrier properties.
- Japanese Patent Application Laid-Open No. 6-180150 discloses, as an example of a single-layer barrier material having a barrier property, a two-piece having a mouth portion and a cylindrical body portion.
- thermoplastic resins such as polyolefin and polystyrene have various drawbacks because of their hydrophobicity.
- the adhesiveness (adhesion) to the paint vehicle is poor because the surface of the molded product is non-polar.
- it is necessary to maintain the adhesion by performing a primer treatment it is necessary to maintain the adhesion by performing a primer treatment
- the painting cost is high.
- paints have been moving from organic solvent-based paints to water-based paints in view of global environmental issues.However, water-based paints have lower adhesion to hydrophobic thermoplastic resins, The development of a thermoplastic resin with improved adhesion is further desired.
- EVOH has been recognized for its effectiveness in packaging films for foods and the like, especially in the food field that requires barrier properties against oxygen, odors, and flavors.
- EVOH itself lacks toughness, there are few cases where EVOH is used alone.
- an EVOH film has a drawback that pinholes are apt to occur when it is repeatedly deformed by bending or the like.
- One way to improve the flexibility, which is a drawback of EVOH is to use EVOH with a thermoplastic resin layer of polyethylene, polypropylene, polyamide, etc., or various adhesive resin layers to use it as a multilayer structure. Many.
- EVOH has excellent chemical resistance, oil resistance, stain resistance, and plasticizer shielding properties, so it is widely used to laminate an EVOH film on the surface of various interior materials such as wallpaper, decorative plywood, and PVC leather.
- EVOH film has a high gloss, and in applications such as wallpaper and leather that require glossiness, the glossiness of the glossiness roll is thermocompression-bonded, but the glossiness is reduced. There is a problem that the light can not be sufficiently erased.
- the methods for removing the gloss of the film include (1) sandblasting, (2) surface treatment with chemicals, and (3) blending of powdered inorganic substances. Are known.
- scraps When manufacturing multi-layer containers (bottles, cups, etc.) made of thermoplastic resin and EVOH resin, scraps (bottle burrs, cup punching debris) are generated in the manufacturing process.
- a method of collecting and utilizing such scrap generally, a method of interposing a scrap collecting layer between a thermoplastic resin layer and an EVOH layer has been adopted.
- melt-extruding a scrap recovery layer containing a thermoplastic resin and an EVOH resin poor flow compatibility between the EVOH and the thermoplastic resin in the recovery layer, or a flow abnormality considered to be caused by thermal degradation of the EVOH, may occur. This may cause a wavy pattern in the multilayer sheet including the scrap recovery layer and its thermoformed product.
- ethylene content is 20 to 65 mol%
- the saponification degree of vinyl acetate component is 96% or more.
- a method of blending EVOH with 68 to 98 mol% and a saponification degree of vinyl acetate component of 20% or more has been proposed (Japanese Patent Laid-Open No. 3-215032; US Pat. No. 5,049,921).
- Japanese Patent Laid-Open No. 3-215032 Japanese Patent Laid-Open No. 3-215032
- US Pat. No. 5,049,921 Japanese Patent Laid-Open No. 3-215032
- Japanese Patent Application Laid-Open No. Hei 4-1644941 discloses that an ethylene unsaturated unsaturated carboxylic acid or a derivative thereof is graft-reacted to 50 to 99.5% by weight of polyolefin, 0.4 to 50% by weight of EVOH, and polyolefin, and further melted with polyamide.
- a polyolefin-based resin composition having excellent gas barrier properties and comprising 0.1 to 15% by weight of a graft polymer mixed therewith is described.
- Japanese Patent Application Laid-Open No. Hei 4-164944 discloses that polyolefin 0.4 to 50% by weight, EV ⁇ H 50 to 99.5% by weight.
- an EVOH-based resin composition comprising 0.1% to 15% by weight of the above graft polymer and having excellent gas barrier properties, stretchability and flexibility in a high-humidity atmosphere.
- the modified polyolefin that is melt-mixed with the polyamide is obtained by grafting an unsaturated carboxylic acid or a derivative thereof to the polyolefin, and is not a random copolymer as in the present invention.
- the object of the present invention cannot be achieved by using a graft copolymer.
- JP-A-8-217934 discloses that ethylene-unsaturated carboxylic acid having an EV ⁇ H of 50 to 85 parts by weight and an unsaturated carboxylic acid content of 4 to 15 mol% is disclosed.
- Thermoplastic resin composition consisting of 10 to 40 parts by weight of copolymer ionomer and 1 to 25 parts by weight of polyamide is excellent in gas barrier properties, impact resistance, pinhole resistance, stretchability, drawability and transparency Is described.
- JP-A-9-177945 European Publication No. 797625
- 0.01 to 3 parts by weight of a fatty acid metal salt is blended with respect to 100 parts by weight of the resin composition to improve heat stability. Also described are resin compositions.
- this resin composition still has insufficient effects of improving flexibility, particularly flex resistance, as a resin composition containing EVOH as a main component, as shown in Comparative Examples described later. Further, it does not disclose that a specific hydrophobic thermoplastic resin is further added to the three-component resin composition.
- JP-B-51-41657 (U.S. Pat. Nos. 3,857,754 and 3,975,463) discloses a low-density polyethylene selected from the group consisting of 30 to 98 parts by weight, EV ⁇ H 2 to 70 parts by weight, and an ionomer or polyamide. It describes a resin composition comprising 0.5 to 15 parts by weight of a thermoplastic polymer having a carboxy group in at least one main chain or side chain and having excellent processability and gas barrier properties.
- the publication states that both polyamide and ionomer can be blended, it is preferable to blend both at the same time, and No effect is described. Also, there is no description of the compounding ratio between the polyamide and the ionomer.
- an object of the present invention is to provide good compatibility with excellent barrier properties, mechanical strength, flexibility, stretchability, melting stability, heat adhesion, paintability, stain resistance, transparency, and the like.
- An object of the present invention is to provide a resin composition and a resin composition excellent in scrap collecting property without generation of a wavy pattern in a multilayer structure of a thermoplastic resin and EVOH.
- the barrier property in the present invention is not limited to a barrier property against gases such as oxygen, nitrogen, and carbon dioxide gas, that is, is not limited to a gas barrier property, but includes an aroma component (for example, limonene, etc.) (Eg, skatole) or non-adsorbent and non-permeable to hydrocarbons such as gasoline. Disclosure of the invention
- thermoplastic resin (D) other than the above resin having the formula:
- thermoplastic resin (D) is the matrix phase and the ethylene-vinyl alcohol copolymer (A) is the dispersed phase, or the ethylene-vinyl alcohol copolymer (A) is the matrix phase
- the resin (D) be a dispersed phase.
- the elastic modulus of the thermoplastic resin (D) at 20 ° C. is preferably 500 kgZcm 2 or less.
- a polyamide resin (B) and an ethylene monounsaturated carboxylic acid random copolymer or a metal salt (C) thereof are first melt-mixed, and then ethylene-vinyl alcohol is mixed.
- a method for producing a resin composition to be melt-mixed with the polymer (A) and the thermoplastic resin (D) may be mentioned.
- Preferable embodiments using the resin composition of the present invention include a multilayer structure including at least one layer of a resin composition, a mouth portion of a tubular container, and a molded article having a coating applied to the surface thereof.
- Examples include thermoformed containers, flexible films, and matte films having a surface gloss of at least one side of 60% or less.
- Another useful embodiment of the present invention is a scrap recovery method for recovering scrap of a molded product containing a thermoplastic resin (D) as a main component other than the above resin having one (calculated from the Fedors equation).
- the metal salt of higher aliphatic carboxylic acid and hydrotalcite Preferred is a scrap recovery method containing at least one of the following compounds.
- a preferred embodiment is a multilayer structure including at least one scrap collecting layer made of the resin composition obtained by the above-mentioned collecting method.
- EVOH (A) used in the present invention is obtained by saponifying an ethylene-vinyl ester copolymer, and has an ethylene content of 15 to 70 mol%, preferably 20 to 65 mol%, and most preferably 25 to 60 mol%, and moreover, those having a saponification degree of the vinyl ester component of 85% or more, preferably 90% or more can be used. If the ethylene content is less than 15 mol%, melt moldability is poor, and water resistance and hot water resistance are reduced. On the other hand, if it exceeds 70 mol%, the barrier properties will be insufficient. If the degree of saponification is less than 85%, the barrier properties and the thermal stability deteriorate.
- the obtained film has reduced stain resistance, and the film is converted to polyvinyl chloride containing a plasticizer.
- the ability of plasticizers to suppress bleed-out also decreases.
- a typical vinyl ester used in the production of EVOH is vinyl acetate, but other fatty acid vinyl esters (vinyl propionate, vinyl pivalate, etc.) can also be used.
- EVOH can contain 0.0002 to 0.2 mol% of a vinylsilane compound as a copolymerization component.
- examples of the vinyl silane-based compound include vinyl trimethoxy silane, vinyl triethoxy silane, vinyl tri (3-methoxy-ethoxy) silane, and methacryloxypropyl methoxy silane. Among them, vinyltrimethoxysilane and vinyltriethoxysilane are preferably used.
- comonomers eg, propylene, butylene, unsaturated power, rubonic acid or its ester ⁇ (meth) acrylic acid, (meth) methyl acrylate, (meth) Ethyl acrylate ⁇ and vinylpyrrolidone ( ⁇ -vinylpyrrolidone, etc.) can also be copolymerized.
- Suitable melt index ( ⁇ I) of EVOH used in the present invention (190 ° C, 21 Under 60 g load) is 0.1 to 50 g / 10 min., Optimally 0.5 to 30 gZl Omin. However, if the melting point is around 19 O: or more than 190, measure at 216 Og load at multiple temperatures above the melting point, and plot the reciprocal of the absolute temperature on the horizontal axis and plot the logarithm of Ml on the vertical axis in a semilogarithmic graph. And extrapolated to 190.
- These EVOH resins can be used alone or in combination of two or more.
- the polyamide resin (B) used in the present invention is a polymer having an amide bond.
- the polyamide resin (B) include polyproamide (nylon-16)-, polydecaneamide (nylon-11), and polylauryl lactam ( Homopolymers such as Nylon-12), polyhexamethylene adipamide (Nylon-6,6), polyhexamethylene sebacamide (Nylon-1,6,12), and coprolactam lauryl lactam copolymer (Nylon-1 / 6 / 12), Proprolactam Z-aminoundecanoic acid polymer (nylon-6 / 1 1), Proprolactam ⁇ -aminononanoic acid polymer (nylon 1,6,9), Proprolactam / hexamethylene diammonium adipate Copolymer (Nylon-6 / 6, 6), Prolactam ⁇ Hexamethylene diammonium acetate ⁇ Hexamethylene diammonium seba Copolymer (nylon-6 ⁇ 6,
- polyamides containing 6 nylon components are preferred. Since EVOH and nylon react and gel during the melting process, it is preferable to use nylon having a melting point of 240 ° C or less, and preferably 230 ° C or less, from the viewpoint of suppressing thermal degradation of the blend composition. Good.
- the polyamide (B) used in the present invention has a suitable melt index (Ml) (210, under a load of 2160 g) of 0.1 to 50 gZl 0 min., Optimally 0.5 to 30 g / 10 min. n.
- the melting point is around 210 or exceeds 210, it is measured under a load of 2160 g at multiple temperatures above the melting point, and the reciprocal of absolute temperature is plotted on the abscissa and the log of MI is plotted on the ordinate on a semilogarithmic graph. , 210 extrapolated values.
- the ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C) used in the present invention is a polymer obtained by random copolymerizing ethylene and an unsaturated carboxylic acid, or neutralizing the carboxylic acid component thereof. It is a so-called ionomer that is a metal salt obtained by Here, it is extremely important that ethylene and unsaturated carboxylic acid are randomly copolymerized. If a copolymer obtained by grafting unsaturated carboxylic acid to polyethylene was used, it will be shown in a comparative example described later. Thus, the effects of the present invention cannot be achieved.
- the random copolymer or its metal salt is superior to the graft copolymer, but the random copolymer has better compatibility with the polyamide resin (B) than the graft copolymer. It is considered that Further, in the case of a graft copolymer, a gel 'fish eye is easily generated, probably because a hydroxyl group in EVOH reacts with a carboxyl group in the graft copolymer, which is not preferable. In particular, when melt molding is performed for a long time, the generation of gel fish eyes is remarkable. Also, in the present resin composition, it is not clear why it is better to use the metal salt ionomer than the ethylene monounsaturated carboxylic acid random copolymer, but the ionomer has better compatibility with nylon. It is considered that
- the content of the unsaturated carboxylic acid is preferably 2 to 15 mol%, more preferably 3 to 12 mol%.
- the unsaturated carboxylic acid include acrylic acid, methacrylic acid, ethacrylic acid, maleic acid, monomethyl maleate, monoethyl maleate, and maleic anhydride. Lylic acid is preferred.
- Other monomers that may be included in the copolymer include vinyl esters such as vinyl acetate and vinyl propionate, methyl acrylate, ethyl acrylate, isopropyl acrylate, isoptyl acrylate, and acrylic.
- Examples thereof include unsaturated carboxylic esters such as n-butyl acid, 2-ethylhexyl acrylate, methyl methacrylate, isobutyl methacrylate, and getyl maleate, and carbon monoxide.
- unsaturated carboxylic esters such as n-butyl acid, 2-ethylhexyl acrylate, methyl methacrylate, isobutyl methacrylate, and getyl maleate, and carbon monoxide.
- the metal ion in the ionomer examples include an alkali metal such as lithium, sodium, and potassium, and an alkaline earth metal such as zinc, magnesium, and calcium. Particularly, zinc is preferred in view of compatibility with nylon.
- the degree of neutralization in the ionomer is preferably 100% or less, particularly 90% or less, and more preferably 70% or less.
- the lower limit of the degree of neutralization is usually 5% or more, especially 10% or more, and more preferably 30% or more.
- the ethylene-unsaturated carboxylic acid random copolymer or its metal salt used in the present invention preferably has a melt index (MI) (at 190 ° C. under a load of 2160 g) of preferably 0.05 to 50 g / 10. Min, more preferably 0.1 SSO gZlO min.
- MI melt index
- These ethylene monounsaturated carboxylic acid random copolymers or metal salts thereof can be used alone or in combination of two or more.
- the thermoplastic resin (D) used in the present invention is a thermoplastic resin different from the components (A), (B) and (C), and it is important that the solubility parameter be 11 or less. It is. That is, since the solubility parameters (calculated from the Fedors equation) of the thermoplastic resin (D) and the ethylene monounsaturated carboxylic acid random copolymer or its metal salt (C) are close, 4 The compatibility between the components (A), (B), (C) and (D) is improved. When the solubility parameter of the thermoplastic resin (D) is 11 or more, the compatibility among the four components (A), (B), (C), and (D) decreases, and the scrap recovery of the blended resin composition is reduced.
- thermoplastic resin (D) having a solubility parameter of 11 or less examples include a polyolefin resin, a styrene resin, and a polyvinyl chloride resin.
- polyolefin resins are most preferred, and are selected from homopolymers of ⁇ -olefin such as high-density or low-density polyethylene, polypropylene, polybutene-11, ethylene, propylene, butene-11, hexene-11, etc.
- copolymers of ⁇ -olefins are exemplified. Also included are those obtained by copolymerizing the following components with ⁇ -olefin.
- copolymerization component with ⁇ -olefin examples include diolein, vinyl chloride, vinyl compounds such as vinyl acetate, unsaturated carboxylic acids such as maleic acid, acrylic acid, and methacrylic acid, and anhydrides thereof.
- styrene resin examples include polystyrene, acrylonitrile-butadiene-styrene copolymer resin (ABS), and acrylonitrile-styrene copolymer resin (AS). These thermoplastic resins can be used alone or in combination of two or more.
- the thermoplastic resin (D) used in the present invention preferably has a melt index (MI) (at 190, under a load of 2160 g) of preferably 0.05 to 100 gZl O, more preferably 0.05 to 50 gZ. 10 minutes, optimally 0.5-30 gZlO.
- MI melt index
- the melting point is near 190 or exceeds 190, measure at a plurality of temperatures above the melting point under a load of 2160 g and plot the reciprocal of absolute temperature on the horizontal axis and the logarithm of MI on the vertical axis in a semilogarithmic graph. And the value is extrapolated to 190 ° C.
- a polyamide (B) and an ethylene monounsaturated carboxylic acid random copolymer or a metal salt (C) thereof are used as compatibilizers.
- the main feature is the use of the component.
- a resin with poor compatibility that is, As a measure to improve the compatibility between EVOH (A), which is a very different resin, and thermoplastic resin (D), the compatibility between polyamide (B), which has good compatibility with EVOH (A), and thermoplastic resin (D) is considered.
- the use of a good ethylene monounsaturated carboxylic acid random copolymer or its metal salt (C) as a compatibilizer has led to the discovery of the resin composition of the present invention.
- the compounding weight ratio of each component in the resin composition of the present invention satisfies the following formulas (1) to (4).
- Equations (1) to (4) are preferably
- a decrease in the compatibility between the components leads to a decrease in the mechanical strength of the resin composition itself or a decrease in the barrier properties, thermal adhesion, paintability, glossiness, flexibility, and stretchability.
- a wave pattern is generated on the multilayer sheet including the scrap recovery layer and its thermoformed product.
- the blending weight ratio of the polyamide resin (B) to the ethylene monounsaturated carboxylic acid random copolymer or its metal salt (C) W (B) / W (B + C) force should be 0.5 or less. It is preferable from the viewpoint of thermal stability, more preferably 0.45 or less, and most preferably 0.4 or less.
- the compounding weight ratio W (B) / W (B + C) is in such a range, the melt stability of the resin composition is improved, and a molded article having a good appearance even in a long-time melt molding is obtained. And increase productivity. The reason for this Although it is not clear, the reaction between the EVOH and the polyamide is thought to have adversely affected the melt stability.
- the dispersion form of each resin is not particularly limited, but it is preferable that the thermoplastic resin (D) be the matrix phase and EVOH (A) be the dispersed phase depending on the application. In some cases, it is more preferable that EVOH (A) be the matrix phase and the thermoplastic resin (D) be the dispersed phase.
- thermoplastic resin (D) is the matrix phase and EVOH (A) is the dispersed phase retains the characteristics of the thermoplastic resin as a whole, but imparts its properties by blending EVOH. It is useful in that it can. That is, it is useful for oral applications of tubular containers that can improve barrier properties while maintaining thermal adhesion and mechanical strength, and molded articles that can improve coating properties while maintaining mechanical strength. It is also widely used as a scrap recovery composition containing a thermoplastic resin as a main component and a small amount of an EVOH component.
- Such a dispersion form can be obtained by reducing the value of W (A) ZW (A + D) or by making the melt viscosity of (A) larger than the melt viscosity of (D).
- the value of W (A) / W (A + D) is preferably 0.65 or less, more preferably 0.6 or less.
- the value of W (A) / W (A + D) exceeds 0.65, it becomes difficult for the thermoplastic resin to form a matrix phase.
- thermoplastic resin (D) is the dispersed phase
- This type of dispersion involves increasing the value of W (A) / W (A + D). Alternatively, it can be obtained by making the melt viscosity of (A) smaller than the melt viscosity of (D).
- the value of W (A) / W (A + D) is preferably 0.65 or more, more preferably 0.7 or more. If the value of W (A) / W (A + D) is less than 0.65, it becomes difficult for EVOH to form a matrix phase.
- the elastic modulus (ASTM D 882) of the thermoplastic resin (D) at 20 is preferably 500 kg / cm 2 or less. . More preferably a 2 hereinafter 400 k gZcm, even more preferably at 300 KgZcm 2 below.
- EVOH has higher rigidity and lacks flexibility compared to general polymers, so it has low resistance to bending and cannot be used in flexible packaging applications in many cases. Further, in a process having a stretching step for a skin pack package, a shrink package, a thermoformed film or a sheet, a gas barrier property is deteriorated due to a poor thickness distribution of the thermoformed product due to uneven stretching, and furthermore, a poor appearance is a problem. Therefore, a composition having a low Young's modulus that can be stretched with a smaller force is desired in order to develop good bending resistance and ductility. In response to such a demand, it is effective to mix the thermoplastic resin (D) with the EVOH (A), and it is particularly effective to set the elastic modulus at 20 of the thermoplastic resin (D) to 500 kgZcm 2 or less. It is.
- thermoplastic resin (D) having an elastic modulus of 500 kg / cm 2 or less examples include very low density polyethylene (VLDPE), ethylene-vinyl acetate copolymer (EVA), and ethylene-methyl methacrylate copolymer (EMAA), ethylene-ethyl acrylate copolymer (EEA), ethylene-propylene copolymer (EPR), styrene-based elastomer (SEBS resin, etc.).
- VLDPE very low density polyethylene
- EVA ethylene-vinyl acetate copolymer
- EMAA ethylene-methyl methacrylate copolymer
- EAA ethylene-ethyl acrylate copolymer
- EPR ethylene-propylene copolymer
- SEBS resin styrene-based elastomer
- the resin composition of the present invention contains at least one of a metal salt of a higher aliphatic carboxylic acid and a hydrotalcite compound, so that EVOH (A) reacts with the polyamide resin (B) to form EVOH. Can prevent thermal degradation, As will be apparent from the examples described later, it is also possible to obtain an excellent molded product having no wavy pattern or the like in a multilayer coextrusion sheet containing a scrap layer.
- a hydrate port hydrotalcite compound M X A 1 y (OH) 2x + 3y _ 2z (A) z ⁇ aH 2 0 M is Mg, C a, or Zn, A is CO 3 or HP_ ⁇ 4 , X, y, z, and a are positive numbers
- a hydrated talcite compound which is a double salt represented by the following formula.
- the following compounds are particularly preferred. You.
- hydrotalcite compound a hydrotalcite-based solid solution described in JP-A-11-308439 (US Pat. No. 4,954,557), [Mg
- Metal salts of higher aliphatic carboxylic acids are metal salts of higher fatty acids having 8 to 22 carbon atoms, and higher fatty acids having 8 to 22 carbon atoms include lauric acid, stearic acid, myristic acid and the like.
- Examples of the metal include sodium, potassium, magnesium, calcium, zinc, barium, and aluminum. Of these, alkaline earth metals such as magnesium, calcium and barium are preferred.
- the content of the metal salt of these higher aliphatic carboxylic acids and the hydrotalcite compound is preferably 0.01 to 3 parts by weight, more preferably 0.01 to 3 parts by weight, based on the total weight of the resin composition. Suitably, it is 0.05 to 2.5 parts by weight.
- the resin composition of the present invention may contain other additives (such as a heat stabilizer, a plasticizer, an ultraviolet absorber, an antioxidant, a coloring agent, a filler, and other resins) without impairing the object of the present invention. Free to use in range.
- the composition of the present invention can be easily obtained by melt-kneading each component with a usual melt-kneading apparatus.
- the method of blending is not particularly limited, but EVOH (A), polyamide resin (B), ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C), thermoplastic resin (D ) Is simultaneously pelletized with a single-screw or twin-screw extruder or the like, or first, the polyamide resin (B) and the ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C) are mixed together. Melting, cooling, pelletizing, dry blending with EVOH (A) and thermoplastic resin (D), pelletizing with a single screw or twin screw extruder and drying.
- a polyamide resin (B) and an ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C) are melt-blended, and then EVOH
- the object of the present invention can be effectively achieved by a method of melt-blending (A) with the thermoplastic resin (D).
- blend pellets should be formed using an extruder with a high degree of kneading. It is desirable to seal with nitrogen gas and extrude at low temperature.
- the resin composition comprising the acid random copolymer or its metal salt (C) and the thermoplastic resin (D) can be formed into a single-layer molded product of the present composition. It can also be used as a molded product having more than one kind of multilayer structure.
- the composition layer and the adjacent thermoplastic resin layer are made of high-, medium-, or low-density copolymers of polyethylene, vinyl acetate, acrylates, or butenes, hexenes, and other olefins.
- Polyolefins such as modified polyethylene, ionomer resin, polypropylene homopolymer, or polypropylene copolymerized with ⁇ -olefins such as ethylene, butene, and hexene, and modified polypropylene blended with rubber-based polymer, or Thermoplastic resins obtained by adding or grafting maleic anhydride to the resin are preferred.
- Other thermoplastic resin layers include polyamide resin, polyester resin, polystyrene resin, polyvinyl chloride resin, acrylic resin, polyurethane resin, polycarbonate resin, and polyvinyl acetate resin. No.
- an adhesive resin layer may be provided between the composition layer of the present invention and the thermoplastic resin layer adjacent thereto.
- unsaturated carboxylic acid or its anhydride such as maleic anhydride
- an olefin-based polymer or copolymer for example, LLDPE, VLDPE, etc.
- ethylene vinyl monoacetate for example, LLDPE, VLDPE, etc.
- Copolymers and ethylene- (meth) acrylate copolymer grafts are typical examples.
- the method for obtaining the multilayer structure is not particularly limited, but includes an extrusion lamination method, a dry lamination method, an extrusion blow molding method, a coextrusion lamination method, a coextrusion sheet molding method, a coextrusion pipe molding method, Examples include a co-extrusion professional molding method, a co-injection molding method, and a solution coating method.
- the laminated body can be subjected to a secondary working after reheating by vacuum pressure deep drawing, blow molding or the like in the range of the melting point of EVOH or less.
- thermoplastic resin layer resin composition layer / thermoplastic resin layer resin composition layer Z adhesive resin layer thermoplastic resin layer
- thermoplastic resin layer adhesive resin layer / resin composition layer / Adhesive resin layers / thermoplastic resin layers are typical examples.
- a thermoplastic resin layer is provided on both outer layers, different resins may be used, or the same resin may be used. Further, scrap generated during extrusion molding, blow molding, thermoforming, or the like may be blended with the thermoplastic resin layer or provided separately as a collecting layer.
- barrier properties, mechanical strength, flexibility, elongation, melt stability, scrap recovery, heat adhesion, paintability, stain resistance, transparency, etc. are improved. It is effective for various uses because excellent molded products can be obtained.
- thermoplastic resin (D) is the matrix phase
- EVOH (A) is the dispersed phase
- a resin composition in which the thermoplastic resin (D) is the matrix phase and the EVOH (A) is the dispersed phase is used as a single-layer barrier material with barrier properties. It can be used as a single-layer barrier container (bottle, cup, etc.), a paper container or a barrier spout (pouring spout) for a bag-in-box. It is also useful for plastic-resistant household goods and household electrical parts with stain resistance, such as plastic automobile parts with improved paintability. Further, it can also be used for fuel tanks or fuel tubes utilizing barrier properties against organic solvents.
- the thermoplastic resin (D) becomes the matrix phase
- EVOH (A) becomes the dispersed phase.
- the fat composition is used as the mouth of a two-piece tubular container will be described.
- the use of such a resin composition is effective in that barrier properties can be improved while maintaining thermal adhesiveness and mechanical strength.
- thermoplastic resin (D) used in this case polyolefin is preferable, and polyethylene is most preferable, from the viewpoints of mechanical strength and thermal adhesion to the tube portion.
- D) is preferably 0.2 or more, more preferably 0.3 or more, and most preferably 0.4 or more, from the viewpoint of ensuring good barrier properties. .
- thermoplastic resin (D) is a matrix phase and the EVOH (A) is a dispersed phase is used as a molded article having a surface coated with a paint.
- the use of such a resin composition is effective in that a molded article capable of improving coatability while maintaining mechanical strength is obtained.
- thermoplastic resin (D) used in this case a polyolefin is preferable from the viewpoint of mechanical strength, rigidity, impact resistance, etc., and polypropylene is particularly preferable.
- the EVOH (A) used preferably has an ethylene content of 50 mol% or less, more preferably 45 mol% or less, and more preferably 40 mol% or less, from the viewpoint of efficiently improving paintability. That is optimal.
- the degree of saponification is preferably 90% or more, more preferably 92 to 98%, and most preferably 93 to 97%.
- the value of the weight ratio W (A) ZW (A + D) of the thermoplastic resin (D) and EVOH (A) depends on the mechanical strength, rigidity, impact resistance, etc. of the thermoplastic resin (D). It is preferably 0.3 or less, more preferably 0.2 or less, and most preferably 0.15 or less in consideration of economical efficiency without loss.
- the blending weight ratio of the total amount of the polyamide resin (B) and the ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C) to the total weight of the resin composition W (B + C) ZW (T ) Is preferably 0.15 or less, more preferably 0.1 or less.
- a resin composition in which EVOH (A) is a matrix phase and thermoplastic resin (D) is a dispersed phase can provide EVOH with improved flexibility, stretchability, and transparency, and can be used as a flexible film, Bag-in-box that requires bending resistance, skin pack packaging, shrink packaging, and thermoformed containers that require ductility and thermoformability Useful for
- a resin composition in which EVOH (A) is the matrix phase and the thermoplastic resin (D) is the dispersed phase can reduce the glossiness while maintaining the excellent stain resistance of EVOH. It is also useful for eraser films.
- thermoplastic resin (D) used for the matte film polyolefin is preferred from the viewpoint of mechanical strength and economy, and polyethylene is particularly preferred.
- the polyethylene is preferably a resin in which 60% by mole or more of its constituent components are composed of an ethylene component.
- Comonomers that can be used at a ratio of less than 40 mol% include, for example, olefins such as propylene and butylene, isogens such as isoprene and butadiene, styrene and its derivatives, various acrylates, various methacrylates, Vinyl acetate and the like.
- ⁇ , ⁇ monounsaturated fatty acids such as maleic anhydride and various functionalities such as carboxylic anhydride, glycidyl ether methacrylate, ethylene oxide and propylene oxide.
- a compound having a group a polyethylene resin obtained by copolymerizing or grafting an ⁇ , / 3-unsaturated fatty acid and the carboxylic anhydride in a proportion of 0.0005 to 0.5 mol% is particularly preferably used in the present invention.
- thermoplastic resin (D) is 4 to 45% by weight based on the total amount of (A), ( ⁇ ), (C) and (D) when used for an anti-glare film. And the range of 10 to 30% by weight is more preferable. If the content is less than 4% by weight, the glossiness may not be satisfied. If the content exceeds 45% by weight, the morphology changes, and the characteristics inherent in the ⁇ V ⁇ film may not be maintained.
- the weight ratio of the polyamide resin ( ⁇ ) to the ethylene monounsaturated carboxylic acid random copolymer or its metal salt (C) in the case of using for an anti-glare film is 2:98 to 70:30, preferably 3:97 to 60. : 40, optimally 5: 95-50: 50 You. If the proportion of the polyamide resin is less than 2%, the dispersibility of the entire system will be insufficient, and not only the glossiness will be unsatisfactory, but also the mechanical properties will be insufficient. If it exceeds 70%, the reaction rate between EVOH and Nai-Pont will increase, and productivity will be a problem.
- the total amount of the polyamide resin (B) and the random copolymer of ethylene monounsaturated carboxylic acid or its metal salt (C) when used for an anti-glare film is (A), (B), (
- the glossiness of at least one side of the matte film is 60% or less, preferably 50% or less, and most preferably 40% or less. Films exceeding 60% are unsuitable as matte film.
- the glossiness mentioned here is the average value of the measured values at any five locations measured with the Murakami-type Hikarizawa meter.
- the thickness of the matte film is preferably from 10 to 50 ⁇ m. If it exceeds 50 £ m, the rigidity of the film will increase, and when laminating on the base material of interior materials such as paper wallpaper and polyvinyl chloride wallpaper, the pattern may be limited.
- EVOH (A) and a thermoplastic resin (A) and a thermoplastic resin (B)
- a molded product containing D) as a main component particularly a multilayer molded product having a layer (A) and a layer (D), a polyamide resin (B) and an ethylene monounsaturated carboxylic acid random copolymer or A molded article to which the metal salt (C) is added as a compatibilizer
- the molded product mainly composed of EVOH (A) and thermoplastic resin (D) means that the total weight of (A) and (D) accounts for more than half of the total molded product weight. .
- the wavy pattern generated in the product can be remarkably improved by blending the polyamide resin (B) with the random copolymer of ethylene and monounsaturated carboxylic acid or its metal salt (C).
- the effect is particularly remarkable when at least one of a metal salt of a higher aliphatic carboxylic acid and a hydrotalcite compound is added to (B) and (C).
- the preferred compounding amount of the metal salt of the higher aliphatic carboxylic acid and the talcite compound at the mouth is 0.1 to 50 parts by weight based on the total amount of (B) + (C).
- the resin composition thus recovered is effectively used as a multilayer structure having at least one scrap recovery layer.
- a multilayer sheet for thermoforming when used, a thermoformed container having a good appearance can be obtained.
- a multilayer structure having at least one EVOH layer in addition to the scrap collecting layer is useful from the viewpoint of barrier properties.
- thermoplastic resin (D) used in such a recovered composition is not particularly limited, polypropylene is preferred from the viewpoints of mechanical strength, impact resistance, secondary workability, economy, and the like. Polystyrene is preferably used from the viewpoints of rigidity, gloss, secondary workability, economy and the like.
- thermoplastic resin (D) and EV ⁇ H (A) W (A) ZW (A + D) is the mechanical strength, rigidity, and impact resistance of thermoplastic resin (D). It is preferably not more than 0.3, more preferably not more than 0.25, and most preferably not more than 0.2 in consideration of economy and the like without impairing the performance.
- the blending weight ratio of the total amount of the polyamide resin (B) and the ethylene-unsaturated carboxylic acid random copolymer or its metal salt (C) to the total weight of the resin composition W (B + C) ZW (T ) Is preferably 0.15 or less, more preferably 0.1 or less, and most preferably 0.08 or less.
- the resin composition of the present invention is excellent in barrier properties, mechanical strength, flexibility, stretchability, melt stability, scrap recoverability, heat adhesion, paintability, stain resistance, transparency, and the like. It can be usefully used in various applications.
- FIG. 1 is a sectional view of a tubular container showing one embodiment of the present invention.
- FIG. 2 is an enlarged sectional view of the tubular container of FIG.
- the examples related to the mouth of the gu 2-piece tubular container>, the examples related to the gulp coatability>, the examples related to the gulp scrap recoverability>, the examples related to the gu pliable film> The resins shown in Tables 1 to 4 below were used as raw materials.
- Table 1 describes EVOH (A)
- Table 2 describes polyamide resin (B)
- Table 3 describes ethylene copolymer resin (C)
- Table 4 describes thermoplastic resin (D).
- VLDPE Ultra low density e.
- a tube-shaped container was produced by an injection molding method using a tube-shaped container molding machine by an injection molding method disclosed in Japanese Patent Application Laid-Open No. 56-25411 (Japanese Patent Publication No. 64-7850). .
- the obtained resin composition pellets were supplied to an injection molding machine, while a die of the molding machine was supplied with a cylindrical tube to be a body part prepared in advance.
- a 35 ⁇ inline screw type injection molding machine was used as the injection molding machine, and the mouth was formed under the conditions of a cylinder temperature of 240 ° C and a nozzle temperature of 235 ° C.
- the obtained tube-shaped container had an outer diameter of 35 mmci), an outer diameter of the oral squeeze port of 12 mm ⁇ i), an inner diameter of 7 mmc /), and a wall thickness of the oral part of 2 mm.
- the cylindrical tube is made of low-density polyethylene (LDPE, Mitsui Petrochemical, Ultzex 3520 L, thickness 150 M) Adhesive resin (Mitsui Petrochemical, Admer NF 500, thickness 20 n) / EVOH (B-1, thickness 20 / x) / Adhesive resin (Mitsui Petrochemical, Admer NF 500, thickness 20) ZLDPE (Mitsui Petrochemical, Ultzex 3520L, thickness 150, made by coextrusion using an annular die. You.
- HDPE (D-1) It was confirmed that the trix phase, EVOH (A-3), was a dispersed phase.
- the resin composition was melt-extruded at 235 ° C by the T-die method, and a film having a thickness of 100 was formed.Then, using a ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ x- -Tran 100 type oxygen permeability measuring device manufactured by Modern Control Co., Ltd. The oxygen permeability coefficient was measured under the conditions of 20-65% RH.
- Miso was filled from the bottom opening of the formed tubular container, and the tube bottom was sealed by heat bonding. Next, aluminum foil (thickness 25 / i) was attached only to the extrusion port, and the cap was closed.
- the tube container filled with the miso is left in a constant temperature and high humidity bath at 40-50% RH, and after 24 hours, the tube container is taken out. was visually observed and evaluated according to the following criteria A to D.
- A No cracks, chips or cracks.
- the appearance of the oral cavity was evaluated visually.
- the molded article immediately after the start of the injection molding and the molded article 24 hours after the start of the molding were evaluated according to the following criteria A to D.
- C Clear gel, fish eye, or surface roughness partially occurred.
- D A clear gel, fish eye, or rough surface occurred over the entire surface, and the color of the oral part turned pale yellow.
- FIG. 1 shows a tubular container according to an embodiment, in which an oral head 2 having an external thread 2 a at an upper part of a cylindrical body 1 and a shoulder part 2 b at a lower part is thermally bonded at an oral shoulder part 3.
- Fig. 2 shows the structure of the cylindrical body 1.
- the heat sealing layer (LDPE) 5, adhesive resin 6, barrier resin EVOH7, adhesive resin 8 and outer layer (LDPE) 9 are arranged in this order from the inner layer side. Are laminated.
- Example 1 Example 1 was repeated except that the resin composition and the mixing ratio were changed so that the pellets having the resin compositions shown in Table 5 could be obtained instead of the four-component resin composition pellets prepared in Example 1.
- a tubular container was produced in the same manner as in Example 11. When the resin composition was composed of two or three components, the blending was performed by one kneading operation, and when the resin composition was composed of one component, the kneading operation was not performed. Table 5 summarizes the evaluation results.
- Example 11 Example 11
- Example 11 A tubular container was produced in the same manner as in Example 11 except that the composition was the same as that of Example 11, and the four kinds of resin components were kneaded by only one kneading operation to form a pellet. Table 5 shows the evaluation results.
- the obtained pellets were subjected to various types of strength measurement test pieces and painting test reference pieces at 220 using an injection molding machine FS8OS manufactured by Nissei Plastic Industry.
- polypropylene (D-3) was the matrix layer
- EVOH (A-1) was the dispersion layer.
- Table 6 shows the evaluation results.
- the adhesion strength was determined by a cross-cut peeling test in accordance with JISDO224.15. (Strength) was measured.
- the adhesion strength (secondary adhesion strength) of the coating film after being immersed in warm water at 40 hours for 240 hours was similarly evaluated. The ranking of the evaluation was performed according to the following film surface conditions.
- Example 2 Example 2 was repeated except that the resin composition and the mixing ratio were changed so that pellets having the resin compositions shown in Table 6 could be obtained instead of the four-component resin composition pellets prepared in Example 2. Samples were prepared in the same manner as in —1 and evaluated. When the resin composition was composed of two or three components, the blending was performed by one kneading operation, and when the resin composition was composed of one component, the kneading operation was not performed. Table 6 summarizes the evaluation results.
- Example 21 Sample pieces were prepared and evaluated under the same conditions as in Example 2-1 except that the four kinds of resin components were kneaded with only one kneading operation and pelletized with the same composition as in Example 1. Was done. Table 6 shows the evaluation results.
- the obtained resin composition pellets composed of 4 components, EVOH (A-2), polypropylene (D-4) and adhesive resin (maleic anhydride-modified polypropylene) are put into separate extruders, and 4 types and 7 layers are added.
- a 7-layer sheet (total of 300/150/25/50/25/150/300 ⁇ ) is formed by co-extrusion using the PPZREGZ adhesive resin ZEVOH / adhesive resin ZREGZP P (300/150/300 ⁇ ). Layer thickness: 1000).
- Extrusion molding uses PP with a screw screw (65 ⁇ ) at a temperature of 240, REG with a screw screw (40mm (at 220 ° C), and an adhesive resin with a screw screw (40 ° ⁇ ). Temperature of 220 ° C EVOH was performed by extruding each at a temperature of 210 using a -screw screw (40 mmd)). The obtained sheet maintained a good appearance 24 hours and 72 hours after the start of molding, and there was no occurrence of sheet delamination or wavy pattern due to abnormal flow due to poor compatibility in the REG layer. .
- polypropylene (D-4) was a matrix layer
- EVOH (A-2) was a dispersion layer.
- the sheet obtained after 24 hours and 72 hours obtained in this way is thermoformed into a cup shape (mold shape 70 ⁇ X7-0 mm) using a thermoforming machine (manufactured by Asano Seisakusho) (press air: 5 kggcm).
- a thermoforming machine manufactured by Asano Seisakusho
- Plug 45 ⁇ X65mm, syntax form, sheet temperature: 150 ° C, plug temperature: 20, mold temperature: 70).
- the appearance of the formed cap was visually evaluated.
- the resulting cup did not have any delamination or wavy pattern of the sheet due to poor compatibility in the blend belt as in the case of the sheet.
- sheet appearance or cup appearance was determined according to the following criteria. A: Uniform and good film surface without wave pattern and delamination.
- Table 7 shows the evaluation results.
- Example 3-1 instead of the four-component resin composition pellets prepared in Example 3-1, the resin types and the mixing ratios were changed so that pellets having the resin compositions shown in Table 7 were obtained.
- a resin composition was obtained in the same manner as in 1. At this time, when the resin composition was composed of two or three components, the blending was performed by one kneading operation.
- a seven-layer sheet having the same configuration as that of Example 3-1 except for the resin composition layer was prepared in the same manner as in Example 3-1 except that the obtained resin composition was used, and thermoformed to form a cup. Molded. Table 7 summarizes the evaluation results.
- Example 3-1 instead of 4 parts by weight of the blend of polyamide (B-1) and the ionomer (C-12) used in Example 3-1 (blend ratio: 2575 parts by weight), 4 parts by weight of the blended substance was used.
- a resin composition was obtained in the same manner as in Example 3-1 except that 1 part by weight of calcium stearate (manufactured by NOF Corporation) was dry-blended.
- a seven-layer sheet having the same configuration as that of Example 3-1 except for the resin composition layer was prepared in the same manner as in Example 3-1 except that the obtained resin composition was used, and thermoformed to form a cup. Molded. Table 7 shows the evaluation results.
- a resin composition was obtained in the same manner as in Example 3-1 except that hydrotalcite (DHT-4A, manufactured by Kyowa Chemical) was used instead of calcium stearate used in Example 3-6.
- hydrotalcite DHT-4A, manufactured by Kyowa Chemical
- a seven-layer sheet having the same configuration as that of Example 3-1 except for the resin composition layer was prepared in the same manner as in Example 3-1 except that the obtained resin composition was used, and thermoformed to form a cup. Molded. Table 7 shows the evaluation results.
- Example 3-1 The same composition as that of Example 3-1 was used, but the polyamide (B-1) and the ionomer (C-2) were not kneaded in advance, but the four resin components were kneaded by only one kneading operation.
- a resin composition was obtained in the same manner as in Example 3-1 except that the resin composition was changed.
- a seven-layer sheet having the same configuration as that of Example 3-1 except for the resin composition layer was prepared in the same manner as in Example 3-1 except that the obtained resin composition was used, and thermoformed to form a cup. Molded. Table 7 shows the evaluation results.
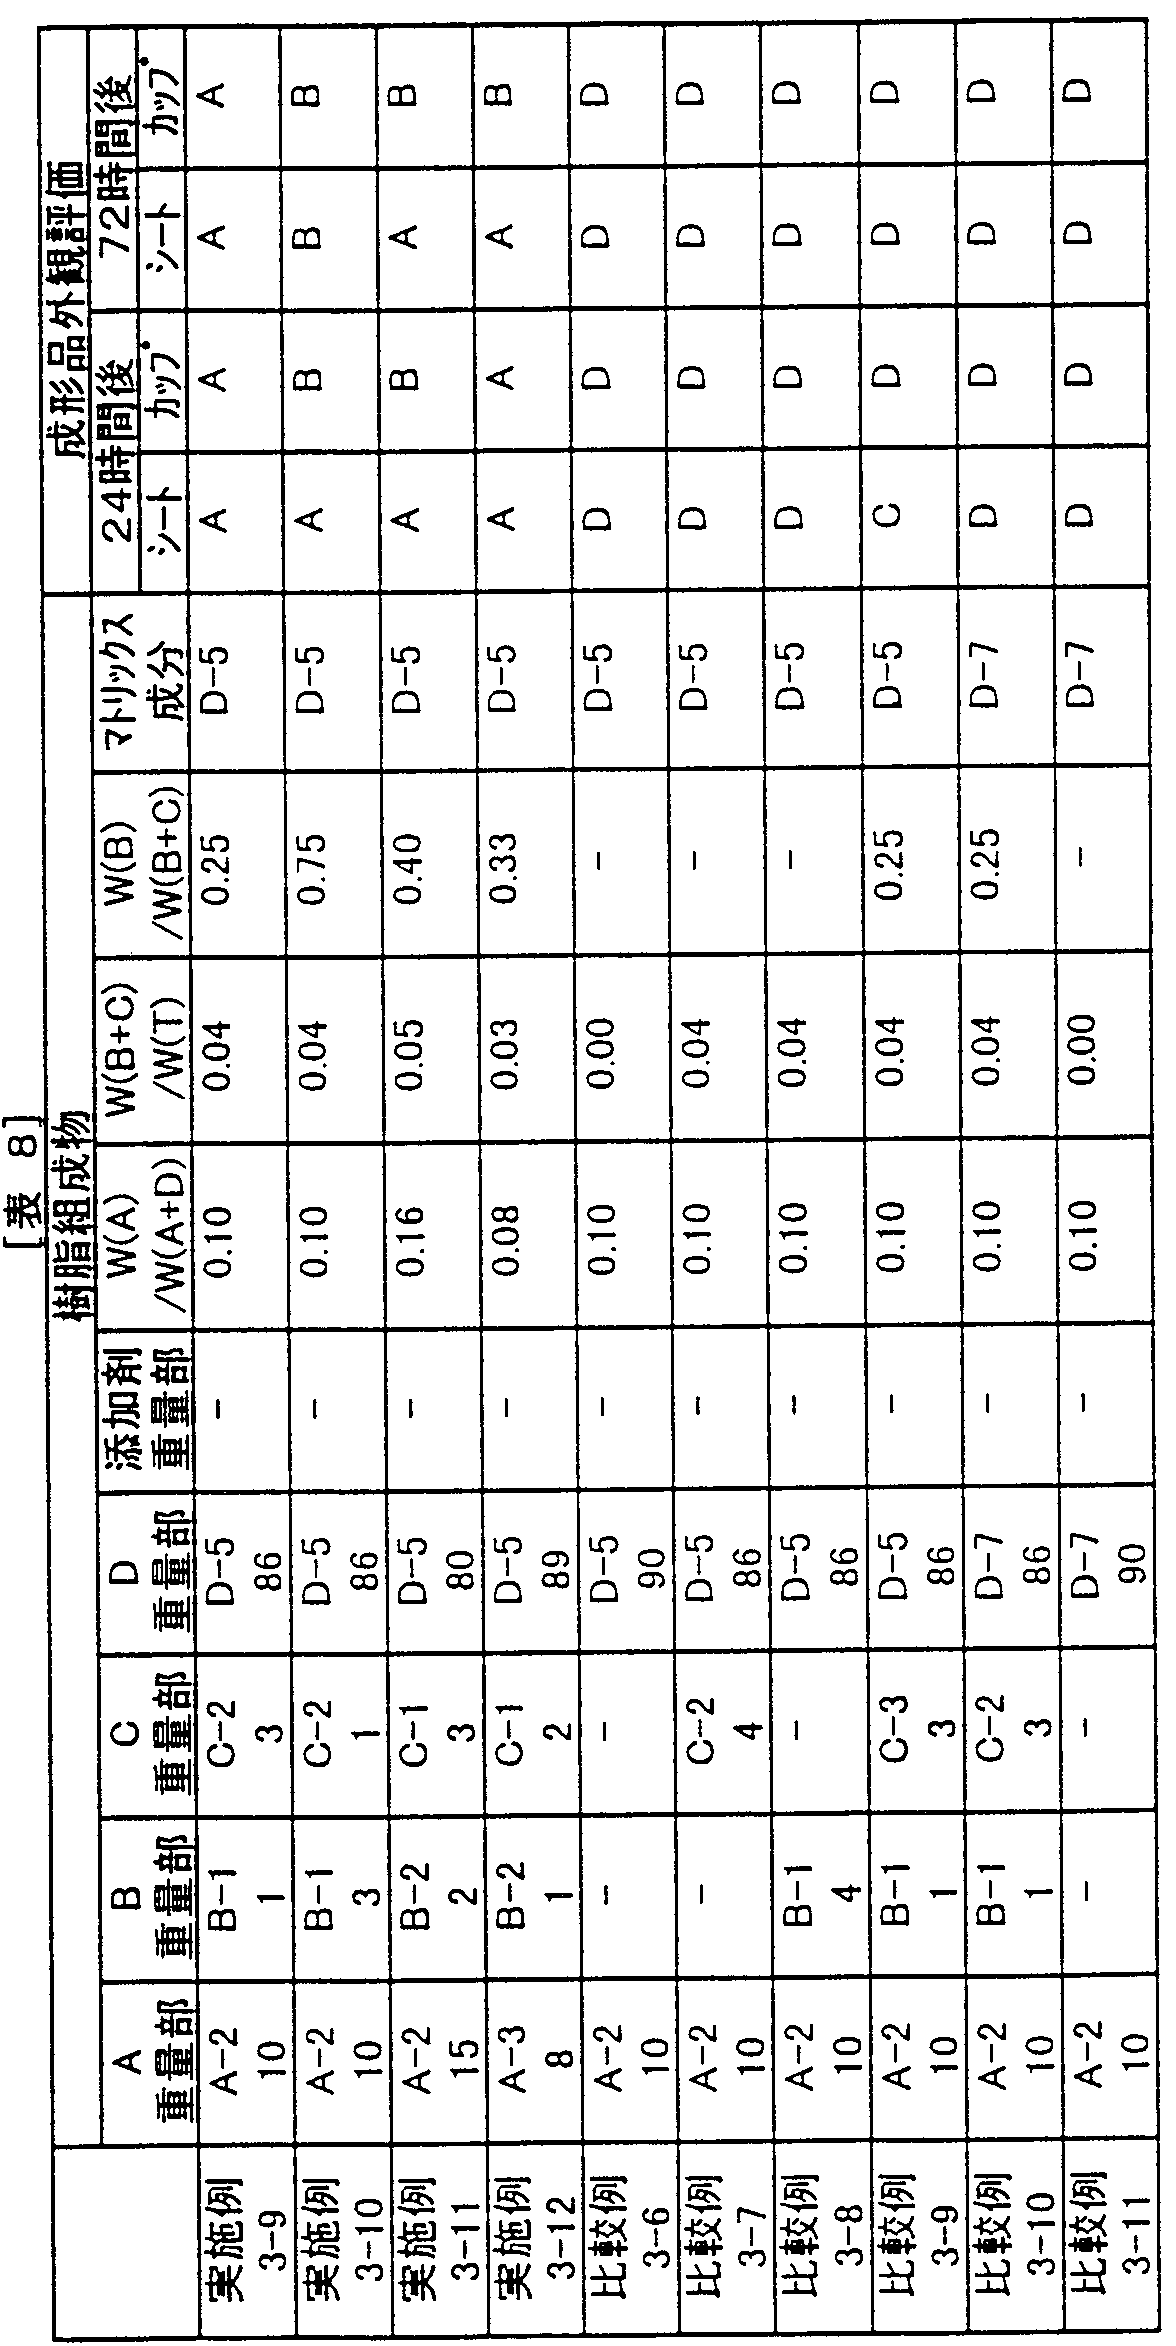
- Example 3-9 In Example 3-1, polystyrene (PS; D-5) was used instead of polypropylene (D-4), and a polystyrene (D-5) layer was provided on both sides of the EVOH (A-2) layer.
- a resin composition (REG) consisting of four components was obtained in the same manner as in Example 3-1 except that a co-extruded sheet (490 100 490) of the layer was prepared and the scrap obtained therefrom was used.
- the obtained four-component resin composition pellets, EVOH (A-2), polystyrene (D-5) and adhesive resin (maleic anhydride-modified ethylene-vinyl acetate copolymer) are put into separate extruders.
- PS / REG Z adhesive resin ZEVOHZ adhesive resin / REGZPS 300/1 50/25 / 50/25/1 50/300
- the sheet was extruded to form a seven-layer sheet (total thickness: 1000).
- PS is used at a temperature of 240 using a screw screw (65m ⁇ )
- REG is used at a temperature of 220 using a screw screw (40 ⁇ )
- the adhesive resin is formed using a single screw (40 ⁇ ).
- EVOH was extruded using a single screw (40 ⁇ ) at a temperature of 21O: respectively.
- the sheet obtained after 24 hours and 72 hours obtained in this way is thermoformed into a cup shape (mold shape 70 ⁇ X 70 mm) using a thermoforming machine (manufactured by Asano Seisakusho) (air pressure: 5 kg / cm 2 , Plug: 45 ⁇ X 65mm, Syntax Form, Sheet Temperature: 130 ° C, Plug Temperature: 20, Die Temperature: 70).
- a thermoforming machine manufactured by Asano Seisakusho
- Table 8 shows the evaluation results.
- Example 3-9 In place of the four-component resin composition bellet prepared in Example 3-9, the resin type and the mixing ratio were changed so that pellets having the resin composition shown in Table 8 were obtained. In the same manner as in 9, a resin composition was obtained. At this time, when the resin composition was composed of two or three components, the blending was performed by one kneading operation.
- Example 3-9 Except for using the obtained resin composition, the same procedure as in Example 3-9 was repeated except for the resin composition layer. Outside, a seven-layer sheet having the same configuration as in Example 3-9 was prepared and thermoformed to form a nip. Table 8 summarizes the evaluation results.
- Example 3-1 polyethylene terephthalate (P-7) was used on both sides of the EVOH (A-2) layer using polyethylene terephthalate (PET; D-7) instead of polypropylene (D-4).
- a resin composition consisting of four components was prepared in the same manner as in Example 3-1 except that a three-layer co-extruded sheet (370/10073730) having a layer was prepared, and a scrap obtained therefrom was used. (REG) was obtained.
- the obtained resin composition pellets composed of four components, EVOH (A-2), polyethylene terephthalate (D-7) and adhesive resin (maleic anhydride-modified ethylene-vinyl acetate copolymer) are separately extruded.
- PETZREGZ adhesive resin / EVOH / adhesive resin ZREGZPET 300/15/25/50/25/15/30/30) 0 / i) to form a 7-layer sheet (total thickness: 1000).
- PET was used at a temperature of 270 ° C using a single screw (65 mmci)
- REG was used at a temperature of 22 using a single screw (4 Omrnci)
- the adhesive resin was used as a single screw. This was carried out by extruding at a temperature of 27 O: using a screw (40 mm (i)) and EVOH at a temperature of 210 using a single screw (40 ⁇ ).
- the sheets obtained after 24 hours and 72 hours obtained in this way are thermoformed into a cup shape (mold shape 70 ⁇ X 70 mm) using a thermoforming machine (manufactured by Asano Seisakusho) (pressed air: 5 kg / cm plug: 45 ⁇ x 65 mm, syntax form, sheet temperature: 110 :, plug temperature: 20 :, mold temperature: 70).
- a thermoforming machine manufactured by Asano Seisakusho
- Table 8 shows the evaluation results.
- a film having a thickness of 25 was measured using a Poitsuk integrating sphere light transmittance meter.
- a 12-inch x 8-inch film is made into a 3.5-inch diameter cylinder, gripping both ends, initial gripping interval 7 inches, maximum gripping interval 1 inch, the first 3.5 inches of the stroke add a twist of 440 degrees at the beginning of the stroke, and then the 2.5 inches are repeated horizontal reciprocating motions at a speed of 40 degrees 20 ° C — 100 times under the condition of 65% RH The number of pinholes in the film after the repetition was measured.
- a 0.6-inch hemisphere attached to the tip is pushed up in the center of a circular film of a constant area stretched horizontally, and the force when the film bursts is read.
- the film samples were measured after conditioning for 2 weeks under the conditions of 20-65% RH. (Equipment used: Toyo Seiki Co., Ltd. Film Impact Tester)
- the test was performed under the conditions of 20 ° C. and 65% RH using OX—Tra ⁇ 10—50 ° manufactured by Modern Control Corporation.
- Example 4 Example 4 was repeated except that the resin type and the mixing ratio were changed so that pellets having the resin compositions shown in Table 9 were obtained instead of the resin composition pellets composed of four components prepared in 1-11. A single-layer film was formed in the same manner as in 11, and evaluated. When the resin composition was composed of two or three components, the blending was performed by one kneading operation, and when the resin composition was composed of one component, the kneading operation was not performed. Table 9 summarizes the evaluation results. Show.
- Example 41 A single-layer film was formed in the same manner as in Example 4-11, except that kneading of the four types of resin components was performed only by one kneading operation to pelletize the same resin composition. evaluated. Table 9 shows the evaluation results.
- PA-6 Amilan CN 1010T manufactured by Toray
- the appearance of the gel fisheye was evaluated by observing the appearance of the film after forming the film for 8 hours with naked eyes and according to the following criteria A to D.
- a film was prepared in the same manner as in Example 5-1 to prepare a film in which the blending resin and the blending amount of Example 5-1 were changed, measured the glossiness, and observed the appearance.
- Table 10 shows the compounded resin, the compounded amount, and the measurement result of each example.
- EVOH (A) used the following.
- Ethylene-methacrylic acid random copolymer ⁇ methacrylic acid content 3.1 mol%, melt index 1.5 gZlO content (190, 2160 g load) ⁇ ⁇ c-2
- Metal salt of random copolymer of ethylene and methacrylic acid (Ionomer) ⁇ Methanacrylic acid content 5.3 mol%, degree of neutralization 60%, counter-ion type Zn, melt index 0.7 gZl O Min (190, 2160 g load) ⁇
- Metal salt of random copolymer of ethylene and methacrylic acid (methacrylic acid content: 6.7 mol%, degree of neutralization: 36%, counter ion species Na, melt index: 2.10 min (190, 2160 g load) ⁇
- thermoplastic resin (D) The following thermoplastic resin (D) was used.
- the evaluation of the stain resistance was based on water-based pens (Sakura felt-tip pens), oil-based pens (Zebra-made Macky extra-fine), lipsticks (Shiseido's Lescente Rouge Excellent RD 524), and crayon (Sakura crayon thick roll red). Lines were drawn using writing materials, and the degree of discoloration remaining after wiping using a household thinner for neutral detergent (Lion ma lemon) and oil-based pen was evaluated by JIS gray scale. Regarding bleed resistance, two sheets were laminated so that the laminated film surfaces overlap at 70 ° C, and a load of 100 g / cm was left for 24 hours, and the condition of the film surface was visually observed. did.
- Example 5-10 evaluation was performed in the same manner as in Examples 5-10 for the polyvinyl chloride-based film on which the EVOH composition film was not laminated. Table 11 shows the evaluation results. "]
- an ethylene-vinyl alcohol copolymer (A), a polyamide resin (B), an ethylene-unsaturated carboxylic acid random copolymer or a metal salt thereof (C) having excellent compatibility and a solubility of 11 or less can be obtained.
- a resin composition comprising a thermoplastic resin (D) other than the above-mentioned resin having a property parameter (calculated from the Fedors equation).
Landscapes
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Laminated Bodies (AREA)
- Compositions Of Macromolecular Compounds (AREA)
Description




Claims
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE1998633249 DE69833249T2 (de) | 1997-09-04 | 1998-03-09 | Harzzusammensetzung |
| EP19980905806 EP0940438B1 (en) | 1997-09-04 | 1998-03-09 | Resin composition |
| US09/297,569 US6294602B1 (en) | 1997-09-04 | 1998-03-09 | Resin composition |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP9/239890 | 1997-09-04 | ||
| JP23989097 | 1997-09-04 | ||
| JP24115197 | 1997-09-05 | ||
| JP9/241151 | 1997-09-05 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO1999011707A1 true WO1999011707A1 (en) | 1999-03-11 |
Family
ID=26534471
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP1998/000947 Ceased WO1999011707A1 (en) | 1997-09-04 | 1998-03-09 | Resin composition |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6294602B1 (ja) |
| EP (2) | EP1548052B1 (ja) |
| KR (1) | KR100323791B1 (ja) |
| CN (1) | CN1129643C (ja) |
| DE (2) | DE69839856D1 (ja) |
| WO (1) | WO1999011707A1 (ja) |
Families Citing this family (32)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NZ314939A (en) * | 1996-06-19 | 1998-10-28 | Kuraray Co | Composition comprising ethylene-vinyl alcohol polymer, polyamide resin, and hydrophobic plasticiser |
| TW431967B (en) | 1998-04-09 | 2001-05-01 | Kuraray Co | Coinjection stretch blow molded container |
| CA2270515A1 (en) * | 1999-04-30 | 2000-10-30 | Universite Laval | Process for making multiphase polymeric film having a laminar structure with controlled permeability and/or controlled mechanical properties |
| CA2310925C (en) | 1999-06-11 | 2005-10-11 | Kuraray Co., Ltd. | Multilayered structure |
| US6686011B1 (en) | 2000-01-28 | 2004-02-03 | Kuraray Co., Ltd. | Coinjection stretch-blow molded container |
| AU778561B2 (en) | 2000-09-01 | 2004-12-09 | Kuraray Co., Ltd. | Ethylene-vinyl alcohol copolymer composition and multilayered container using the same |
| WO2003022699A1 (en) * | 2001-09-06 | 2003-03-20 | Unilever N.V. | Transparent container |
| CA2467708C (en) * | 2003-05-20 | 2011-07-12 | Kuraray Co., Ltd. | Resin composition and method for producing the same |
| US7700692B2 (en) * | 2006-04-28 | 2010-04-20 | E.I. Du Pont De Nemours And Company | Process for recycling polyolefin blend composition using an ethylene copolymer compatibilizing agent |
| US8431650B2 (en) | 2006-04-13 | 2013-04-30 | E I Du Pont De Nemours And Company | Process for recycling polyolefin blend composition using an ethylene copolymer compatibilizing agent |
| JP4820416B2 (ja) * | 2006-09-01 | 2011-11-24 | 東洋製罐株式会社 | 吸着性金属超微粒子含有吸着剤 |
| KR101412832B1 (ko) * | 2007-01-17 | 2014-06-27 | 에스케이이노베이션 주식회사 | 충격강도가 보강된 차단성 수지 조성물 및 그것을 포함한다층 구조의 성형품 |
| US20090321981A1 (en) * | 2008-01-15 | 2009-12-31 | RheTech, Inc. | Cellulosic inclusion thermoplastic composition and molding thereof |
| EP2292690B1 (en) * | 2008-06-23 | 2013-01-02 | Kuraray Co., Ltd. | Polyvinyl chloride resin composition and method for producing same |
| JP6045057B2 (ja) | 2009-03-30 | 2016-12-14 | 株式会社クラレ | 樹脂組成物及び多層構造体 |
| JP5652050B2 (ja) | 2010-08-19 | 2015-01-14 | 横浜ゴム株式会社 | 熱可塑性樹脂組成物の製造方法 |
| JP5644332B2 (ja) | 2010-09-29 | 2014-12-24 | 横浜ゴム株式会社 | 熱可塑性エラストマー組成物の製造方法 |
| US9415990B2 (en) * | 2013-02-13 | 2016-08-16 | Cryovac, Inc. | Bag-in-box system for use in dispensing a pumpable product |
| WO2014163149A1 (ja) * | 2013-04-04 | 2014-10-09 | 日本クロージャー株式会社 | 熱可塑性樹脂から成る層を有する成形体 |
| EP3395889B1 (en) * | 2015-12-24 | 2022-03-30 | Mitsubishi Chemical Corporation | Ethylene-vinyl alcohol copolymer composition pellet and process for producing the same |
| EP3470195B1 (en) | 2017-10-12 | 2026-04-29 | The Procter & Gamble Company | Blow molded article with visual effects, preform, method |
| JP6621505B2 (ja) * | 2018-06-08 | 2019-12-18 | 日本クロージャー株式会社 | 射出成形体 |
| US11046473B2 (en) | 2018-07-17 | 2021-06-29 | The Procter And Gamble Company | Blow molded article with visual effects |
| WO2020049907A1 (ja) * | 2018-09-07 | 2020-03-12 | 宇部興産株式会社 | ポリアミド樹脂組成物 |
| US11724847B2 (en) | 2018-10-19 | 2023-08-15 | The Procter & Gamble Company | Blow molded article with debossing |
| JP7547730B2 (ja) | 2019-01-23 | 2024-09-10 | 東ソー株式会社 | 樹脂組成物およびその樹脂組成物を用いた成形品 |
| EP3953130B1 (en) | 2019-04-11 | 2024-08-14 | The Procter & Gamble Company | Blow molded article with visual effects |
| WO2021142194A1 (en) | 2020-01-08 | 2021-07-15 | The Procter & Gamble Company | Blow molded multilayer article with color gradient |
| KR102398287B1 (ko) * | 2020-07-30 | 2022-05-13 | 홍민 | 용기 일체형 세척 도구 |
| JP7563039B2 (ja) * | 2020-08-17 | 2024-10-08 | 東ソー株式会社 | 樹脂組成物、改質剤およびその改質剤を含む組成物 |
| BR112023018943A2 (pt) * | 2021-03-22 | 2023-10-10 | Dow Mitsui Polychemicals Co Ltd | Composição de resina para filme a vácuo, película para filme a vácuo, método para produção de película para filme a vácuo, material de embalagem de filme a vácuo e embalagem de filme a vácuo |
| US20240336769A1 (en) * | 2023-04-10 | 2024-10-10 | Equistar Chemicals, Lp | Polymer recyclate blend products |
Citations (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS4810149A (ja) * | 1971-06-18 | 1973-02-03 | ||
| JPS4939678A (ja) * | 1972-08-20 | 1974-04-13 | ||
| JPS6268840A (ja) * | 1985-09-20 | 1987-03-28 | Toyo Seikan Kaisha Ltd | 樹脂組成物及び該組成物から成る容器 |
| JPS62121745A (ja) * | 1985-08-06 | 1987-06-03 | Kureha Chem Ind Co Ltd | 燻煙処理可能な食品包装フイルム |
| JPS62283152A (ja) * | 1986-05-30 | 1987-12-09 | Kureha Chem Ind Co Ltd | 燻煙処理可能な食品包装フイルム |
| JPS63260413A (ja) * | 1987-02-25 | 1988-10-27 | デユポン・カナダ・インコーポレーテツド | 遮断性を有する製品の射出成型法 |
| JPH0489851A (ja) * | 1990-08-02 | 1992-03-24 | Kuraray Co Ltd | 抗菌性組成物 |
| JPH0532831A (ja) * | 1991-08-01 | 1993-02-09 | Sumitomo Bakelite Co Ltd | 熱可塑性樹脂組成物 |
| JPH0570634A (ja) * | 1991-09-17 | 1993-03-23 | Sumitomo Bakelite Co Ltd | 熱可塑性樹脂組成物 |
| JPH0834889A (ja) * | 1994-05-18 | 1996-02-06 | Kuraray Co Ltd | 樹脂組成物および多層構造体 |
| JPH0853593A (ja) * | 1994-08-10 | 1996-02-27 | Dainippon Ink & Chem Inc | 帯電防止された熱可塑性樹脂組成物 |
| JPH0976429A (ja) * | 1995-09-18 | 1997-03-25 | Toray Ind Inc | 熱収縮チューブ |
| JPH1086302A (ja) * | 1996-09-13 | 1998-04-07 | Sumitomo Bakelite Co Ltd | 多層フィルム |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3857754A (en) * | 1971-06-18 | 1974-12-31 | Toyo Seikan Kaisha Ltd | Resinous compositions having improved processability and gas permeation resistance and molded structures thereof |
| JPH0611826B2 (ja) * | 1985-09-20 | 1994-02-16 | 三井東圧化学株式会社 | 樹脂組成物 |
| US4950513A (en) * | 1988-03-17 | 1990-08-21 | E. I. Du Pont De Nemours And Company | Laminar articles of a polyolefin and a nylon/polyvinyl alcohol blend |
| US5214090A (en) | 1990-02-01 | 1993-05-25 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Resin composition and use thereof |
| JP2865352B2 (ja) * | 1990-02-01 | 1999-03-08 | 日本合成化学工業株式会社 | エチレン―酢酸ビニル共重合体ケン化物系組成物及びその用途 |
| JP2892487B2 (ja) | 1990-10-29 | 1999-05-17 | 日本合成化学工業株式会社 | ポリオレフィン系樹脂組成物及びその用途 |
| US5177138A (en) | 1990-02-01 | 1993-01-05 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Resin composition including a saponified ethylene-vinyl acetate copolymer, polyolefin, a graft copolymer and hydrotalcite |
| US5280065A (en) | 1990-02-01 | 1994-01-18 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Saponified ethylene-vinyl acetate copolymer composition and the use thereof |
| US5160475A (en) | 1990-02-01 | 1992-11-03 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Method of producing shaped articles having excellent impact resistance |
| US5298334A (en) * | 1990-02-01 | 1994-03-29 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Saponified ethylene-vinyl acetate copolymer composition and the use thereof |
| JP2892486B2 (ja) | 1990-10-29 | 1999-05-17 | 日本合成化学工業株式会社 | エチレン―酢酸ビニル共重合体ケン化物系組成物及びその用途 |
| US5278229A (en) | 1990-02-01 | 1994-01-11 | Nippon Gohsei Kagaku Kogyo Kabushiki Kaisha | Polyolefin composition and the use thereof |
| JP3268813B2 (ja) * | 1992-03-13 | 2002-03-25 | 日本合成化学工業株式会社 | 樹脂組成物及びその製造法 |
| US6011115A (en) | 1994-12-14 | 2000-01-04 | Dupont-Mitsui Polychemicals Co. Ltd. | Thermoplastic resin composition and its use |
| JPH0977945A (ja) | 1995-09-12 | 1997-03-25 | Du Pont Mitsui Polychem Co Ltd | 熱可塑性樹脂組成物及びその用途 |
| JP3737547B2 (ja) | 1994-12-14 | 2006-01-18 | 三井・デュポンポリケミカル株式会社 | 熱可塑性樹脂組成物及びその用途 |
-
1998
- 1998-03-09 CN CN98801677A patent/CN1129643C/zh not_active Expired - Lifetime
- 1998-03-09 DE DE69839856T patent/DE69839856D1/de not_active Expired - Lifetime
- 1998-03-09 EP EP20050002308 patent/EP1548052B1/en not_active Expired - Lifetime
- 1998-03-09 WO PCT/JP1998/000947 patent/WO1999011707A1/ja not_active Ceased
- 1998-03-09 KR KR1019997003987A patent/KR100323791B1/ko not_active Expired - Fee Related
- 1998-03-09 DE DE1998633249 patent/DE69833249T2/de not_active Expired - Lifetime
- 1998-03-09 US US09/297,569 patent/US6294602B1/en not_active Expired - Lifetime
- 1998-03-09 EP EP19980905806 patent/EP0940438B1/en not_active Expired - Lifetime
Patent Citations (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS4810149A (ja) * | 1971-06-18 | 1973-02-03 | ||
| JPS5141657B2 (ja) * | 1971-06-18 | 1976-11-11 | ||
| JPS4939678A (ja) * | 1972-08-20 | 1974-04-13 | ||
| JPS62121745A (ja) * | 1985-08-06 | 1987-06-03 | Kureha Chem Ind Co Ltd | 燻煙処理可能な食品包装フイルム |
| JPS6268840A (ja) * | 1985-09-20 | 1987-03-28 | Toyo Seikan Kaisha Ltd | 樹脂組成物及び該組成物から成る容器 |
| JPS62283152A (ja) * | 1986-05-30 | 1987-12-09 | Kureha Chem Ind Co Ltd | 燻煙処理可能な食品包装フイルム |
| JPS63260413A (ja) * | 1987-02-25 | 1988-10-27 | デユポン・カナダ・インコーポレーテツド | 遮断性を有する製品の射出成型法 |
| JPH0489851A (ja) * | 1990-08-02 | 1992-03-24 | Kuraray Co Ltd | 抗菌性組成物 |
| JPH0532831A (ja) * | 1991-08-01 | 1993-02-09 | Sumitomo Bakelite Co Ltd | 熱可塑性樹脂組成物 |
| JPH0570634A (ja) * | 1991-09-17 | 1993-03-23 | Sumitomo Bakelite Co Ltd | 熱可塑性樹脂組成物 |
| JPH0834889A (ja) * | 1994-05-18 | 1996-02-06 | Kuraray Co Ltd | 樹脂組成物および多層構造体 |
| JPH0853593A (ja) * | 1994-08-10 | 1996-02-27 | Dainippon Ink & Chem Inc | 帯電防止された熱可塑性樹脂組成物 |
| JPH0976429A (ja) * | 1995-09-18 | 1997-03-25 | Toray Ind Inc | 熱収縮チューブ |
| JPH1086302A (ja) * | 1996-09-13 | 1998-04-07 | Sumitomo Bakelite Co Ltd | 多層フィルム |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP0940438A4 * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0940438B1 (en) | 2006-01-18 |
| US6294602B1 (en) | 2001-09-25 |
| EP0940438A4 (en) | 2000-12-06 |
| KR20000068912A (ko) | 2000-11-25 |
| EP1548052B1 (en) | 2008-08-06 |
| CN1243530A (zh) | 2000-02-02 |
| KR100323791B1 (ko) | 2002-02-19 |
| EP1548052A1 (en) | 2005-06-29 |
| EP0940438A1 (en) | 1999-09-08 |
| DE69833249D1 (de) | 2006-04-06 |
| DE69839856D1 (de) | 2008-09-18 |
| CN1129643C (zh) | 2003-12-03 |
| DE69833249T2 (de) | 2006-09-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR100323791B1 (ko) | 수지 조성물 | |
| EP0401666B1 (en) | Resin composition | |
| JP3626591B2 (ja) | 樹脂組成物 | |
| JP2836943B2 (ja) | 樹脂組成物および多層構造体 | |
| US20100119746A1 (en) | Resin composition and multilayer structure | |
| JPH0717806B2 (ja) | 樹脂組成物 | |
| JP3574500B2 (ja) | 樹脂組成物および多層構造体 | |
| JP2659027B2 (ja) | 樹脂組成物 | |
| JP4133997B2 (ja) | スクラップ回収法および多層構造体 | |
| JP2003063543A (ja) | 絞り出し多層容器 | |
| JPH0940825A (ja) | 樹脂組成物及びその用途 | |
| JPH0641197B2 (ja) | 加熱延伸多層構造体 | |
| JP3442584B2 (ja) | 脂肪族系ポリアミド樹脂を最外層とする包装用積層フィルム | |
| JP2020189970A (ja) | 樹脂組成物およびチューブ状容器の口頭部 | |
| JP3616691B2 (ja) | 熱可塑性樹脂組成物及びその用途 | |
| JP4179404B2 (ja) | 成形物のスクラップを回収する方法 | |
| JP6534151B2 (ja) | 多層構造体 | |
| JP4052617B2 (ja) | 樹脂組成物 | |
| JP2000246843A (ja) | 畜肉包装用多層フィルム | |
| JP3629096B2 (ja) | 樹脂組成物およびその用途 | |
| JP2000248136A (ja) | 柔軟性に優れたエチレン−ビニルアルコール共重合体樹脂組成物 | |
| JPH01279949A (ja) | 樹脂組成物及び積層体 | |
| JP3449747B2 (ja) | 樹脂組成物および多層構造体 | |
| JP4868659B2 (ja) | 樹脂組成物および積層体 | |
| JP2003063542A (ja) | 絞り出し多層容器 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 98801677.X Country of ref document: CN |
|
| AK | Designated states |
Kind code of ref document: A1 Designated state(s): CN KR US |
|
| AL | Designated countries for regional patents |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LU MC NL PT SE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 09297569 Country of ref document: US Ref document number: 1019997003964 Country of ref document: KR Ref document number: 1019997003987 Country of ref document: KR |
|
| WWW | Wipo information: withdrawn in national office |
Ref document number: 1019997003964 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1998905806 Country of ref document: EP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application | ||
| WWP | Wipo information: published in national office |
Ref document number: 1998905806 Country of ref document: EP |
|
| WWP | Wipo information: published in national office |
Ref document number: 1019997003987 Country of ref document: KR |
|
| WWG | Wipo information: grant in national office |
Ref document number: 1019997003987 Country of ref document: KR |
|
| WWG | Wipo information: grant in national office |
Ref document number: 1998905806 Country of ref document: EP |