EP0336862A1 - Verfahren zur Herstellung einer äusseren Schrägkante an einem zylindrischen Ziehteil - Google Patents
Verfahren zur Herstellung einer äusseren Schrägkante an einem zylindrischen Ziehteil Download PDFInfo
- Publication number
- EP0336862A1 EP0336862A1 EP89420120A EP89420120A EP0336862A1 EP 0336862 A1 EP0336862 A1 EP 0336862A1 EP 89420120 A EP89420120 A EP 89420120A EP 89420120 A EP89420120 A EP 89420120A EP 0336862 A1 EP0336862 A1 EP 0336862A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- punch
- cup
- stamping
- die
- carried out
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 7
- 238000000034 method Methods 0.000 claims description 8
- 239000011159 matrix material Substances 0.000 claims description 3
- 230000002093 peripheral effect Effects 0.000 claims description 2
- 230000000694 effects Effects 0.000 claims 1
- 101100327917 Caenorhabditis elegans chup-1 gene Proteins 0.000 description 4
- 238000005520 cutting process Methods 0.000 description 3
- 238000000605 extraction Methods 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 238000004140 cleaning Methods 0.000 description 1
- 230000000295 complement effect Effects 0.000 description 1
- 235000014510 cooky Nutrition 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D35/00—Combined processes according to or processes combined with methods covered by groups B21D1/00 - B21D31/00
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D22/00—Shaping without cutting, by stamping, spinning, or deep-drawing
- B21D22/20—Deep-drawing
- B21D22/26—Deep-drawing for making peculiarly, e.g. irregularly, shaped articles
Definitions
- the present invention relates to a method for producing an external chamfer on a stamped cylindrical part.
- Such an external chamfer is conventionally produced by a resumption in turning of the straight edge of the stamped part, this resumption being carried out by means of a tool which removes chips in sufficient quantity to produce the chamfer.
- the invention aims to remedy this drawback.
- a method for producing an external chamfer on a stamped cylindrical part consisting, starting from a flat metallic part: - First of all to carry out a conical pre-stamping of the part to be obtained, using a punch whose end piece has a shape of a truncated cone with an angle substantially equal to that of the chamfer to be obtained, with provision for a peripheral rim plan, - then axially severing the outer periphery of the frustoconical end piece obtained, for example by vertical guillotine shears, - And then straighten, by a final stamping, the frustoconical side wall of this stamped in order to obtain a cup with coaxial wall, the edge of this cup then being provided with an external chamfer.
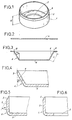
- the part to be obtained 1 is a cup whose bottom 5 is pierced with an orifice 2 for the passage of a drive shaft, and whose edge is provided with an external chamfer 3 This chamfer 3 is practically essential for carrying out the introduction of the cup 1 into an associated bore.
- FIGS 2 to 6 show the essential successive stages in the manufacture of the cup 1.
- the first operation is performed on a first station. It consists of cutting, in a very conventional manner between punch and die, a metal disc 4 of diameter much larger than that of the cup 3.
- This disc 4 is then transferred to another station, where a conical pre-stamping of this disc 4 is carried out, FIG. 3, the angle at the apex ⁇ of the pre-stamping cone being equal to that of the chamfer to be obtained, while is provided , at the periphery of this stamped, a flat edge.
- the tool is shaped so that the small base 5 of the truncated cone 6 obtained has the same diameter as the bottom of the cup to be obtained, and that its flank or apothem 7 has a constant length L substantially equal to the height H (FIG. 1) of this cup.
- the part 6 is then transferred to another station, comprising a guillotine shears with circular periphery which axially cuts, in the vertical direction 8, the external periphery of the frustoconical stamp 6.
- the stamp 6 is then transferred to a fourth station, where its side 7 is straightened axially, that is to say vertically: this side 7 then becomes circular cylindrical and perpendicular to the bottom 5 of the stamp.
- This side 7 is then provided with an external chamfer 3 of angle ⁇ , which is the result that we aim to obtain.
- the piece 6 obtained is then optionally passed through a calibration station, then is made, on a last station ( Figure 6), the central hole 2 for passage of the drive shaft of the cup.
- the tools used for cutting the disc 4 ( Figure 2) and for drilling the hole 2 ( Figure 6) are conventional tools operating as a cookie cutter. They are therefore not represented.
- FIG. 7 shows the tool used for stamping, according to FIG. 3, the frustoconical part 6 from the disc 4.
- This tool comprises a complementary punch 10 and a matrix 11, of frustoconical shape.
- a conventional sidewall press 12 comes to press strongly on the periphery of the disc 4 in order to maintain it during stamping, which prevents the material from wrinkling.
- an extraction pusher 24, pushed upwards by an axial spring 13, equips the die 11.
- FIG. 8 The tool allowing the axial sectioning, according to FIG. 4, of the periphery of the stamping 6, is represented in FIG. 8. It is a circular cutting tool comprising a circular cylindrical punch 14, an associated die 15, a press -wall 16, and an extraction pusher 17 pushed back by a spring 18.
- the tool used for the straightening according to FIG. 5 is represented in FIG. 9. It comprises a beveled flank press 19, a circular cylindrical matrix, of diameter D equal to the external diameter of the cup 1 to be obtained, a pusher 21 with spring. 22, and a circular cylindrical punch 23, of diameter d equal to the inside diameter of the aforementioned cup 1.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Forging (AREA)
- Shaping Metal By Deep-Drawing, Or The Like (AREA)
- Superconductors And Manufacturing Methods Therefor (AREA)
- Photoreceptors In Electrophotography (AREA)
- Metal Extraction Processes (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Processing Of Meat And Fish (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Adornments (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT89420120T ATE81804T1 (de) | 1988-04-06 | 1989-03-31 | Verfahren zur herstellung einer aeusseren schraegkante an einem zylindrischen ziehteil. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR8804971 | 1988-04-06 | ||
| FR8804971A FR2629742B1 (fr) | 1988-04-06 | 1988-04-06 | Procede de realisation d'un chanfrein exterieur sur une piece cylindrique emboutie |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0336862A1 true EP0336862A1 (de) | 1989-10-11 |
| EP0336862B1 EP0336862B1 (de) | 1992-10-28 |
Family
ID=9365324
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89420120A Expired - Lifetime EP0336862B1 (de) | 1988-04-06 | 1989-03-31 | Verfahren zur Herstellung einer äusseren Schrägkante an einem zylindrischen Ziehteil |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US4910989A (de) |
| EP (1) | EP0336862B1 (de) |
| AT (1) | ATE81804T1 (de) |
| CA (1) | CA1289418C (de) |
| DE (1) | DE68903291T2 (de) |
| ES (1) | ES2035619T3 (de) |
| FR (1) | FR2629742B1 (de) |
| GR (1) | GR3006221T3 (de) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4109447A1 (de) * | 1990-07-19 | 1992-01-23 | Degussa | Oberflaechenmodifizierte siliciumdioxide |
| EP0791414A1 (de) * | 1996-02-26 | 1997-08-27 | Karl Marbach GmbH + Co. | Stanz- und Formwerkzeug |
| US5755132A (en) * | 1996-02-26 | 1998-05-26 | Karl Marbach Gmbh & Co. | Punching and forming tool |
| CN111822942A (zh) * | 2019-04-22 | 2020-10-27 | 安克创新科技股份有限公司 | 装饰网的加工方法 |
| CN112808858A (zh) * | 2021-01-25 | 2021-05-18 | 重庆理工大学 | 用于制作弹簧抱挎的级进模 |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2009511377A (ja) * | 2005-10-11 | 2009-03-19 | アイアン マウント コーポレーション | 容器並びに容器を製造する方法及び装置 |
| CN101628409B (zh) * | 2008-07-15 | 2011-06-22 | 施俊兆 | 金属工具盒的成型方法 |
| CN102139436B (zh) * | 2010-01-29 | 2013-08-14 | 江苏白雪电器股份有限公司 | 一种金属防护罩的加工方法 |
| CN102615184A (zh) * | 2012-04-04 | 2012-08-01 | 无锡欧易博阀业科技有限公司 | 盘状工件拉伸模具 |
| CN102974976A (zh) * | 2012-11-15 | 2013-03-20 | 重庆黄龙机械制造有限公司 | 金属周转箱的制作方法 |
| WO2014134767A1 (zh) * | 2013-03-04 | 2014-09-12 | Ding Yuwu | 一种汽车钢圈轮辐生产制造工艺及其专用模具 |
| CN104384844A (zh) * | 2014-10-08 | 2015-03-04 | 柳州科尔特锻造机械有限公司 | 一种工程机械钢圈轮辐生产工艺 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2321085A (en) * | 1941-11-06 | 1943-06-08 | Electromaster Inc | Method for producing drawn cups with faced and beveled edges |
| US2611475A (en) * | 1948-10-07 | 1952-09-23 | Remington Arms Co Inc | Cup drawing apparatus |
| US3406554A (en) * | 1965-07-06 | 1968-10-22 | Continental Can Co | Apparatus for and method of forming containers |
| DE1932139A1 (de) * | 1969-06-25 | 1971-01-21 | Dynamit Nobel Ag | Verfahren zur Herstellung tiefgezogener Hohlkoerper |
| US4534201A (en) * | 1982-12-29 | 1985-08-13 | American Can Company | Undercut punch to control ironing |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US448748A (en) * | 1891-03-24 | Method of and machine for making cup-shaped articles | ||
| US161634A (en) * | 1875-04-06 | Improvement in methods of producing flanged lids and collars for sheet-metal cans | ||
| US2415940A (en) * | 1944-10-05 | 1947-02-18 | Remington Arms Co Inc | Metal cupping process |
| SU590053A1 (ru) * | 1976-05-10 | 1978-01-30 | Ижевский механический институт | Способ получени кольцевых деталей |
| SU1016008A1 (ru) * | 1980-07-14 | 1983-05-07 | Предприятие П/Я М-5344 | Способ получени полых изделий с выступом на дне |
-
1988
- 1988-04-06 FR FR8804971A patent/FR2629742B1/fr not_active Expired - Fee Related
-
1989
- 1989-03-30 CA CA000595247A patent/CA1289418C/fr not_active Expired - Lifetime
- 1989-03-31 AT AT89420120T patent/ATE81804T1/de not_active IP Right Cessation
- 1989-03-31 DE DE8989420120T patent/DE68903291T2/de not_active Expired - Fee Related
- 1989-03-31 ES ES198989420120T patent/ES2035619T3/es not_active Expired - Lifetime
- 1989-03-31 EP EP89420120A patent/EP0336862B1/de not_active Expired - Lifetime
- 1989-04-03 US US07/332,564 patent/US4910989A/en not_active Expired - Fee Related
-
1992
- 1992-11-12 GR GR920402557T patent/GR3006221T3/el unknown
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2321085A (en) * | 1941-11-06 | 1943-06-08 | Electromaster Inc | Method for producing drawn cups with faced and beveled edges |
| US2611475A (en) * | 1948-10-07 | 1952-09-23 | Remington Arms Co Inc | Cup drawing apparatus |
| US3406554A (en) * | 1965-07-06 | 1968-10-22 | Continental Can Co | Apparatus for and method of forming containers |
| DE1932139A1 (de) * | 1969-06-25 | 1971-01-21 | Dynamit Nobel Ag | Verfahren zur Herstellung tiefgezogener Hohlkoerper |
| US4534201A (en) * | 1982-12-29 | 1985-08-13 | American Can Company | Undercut punch to control ironing |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4109447A1 (de) * | 1990-07-19 | 1992-01-23 | Degussa | Oberflaechenmodifizierte siliciumdioxide |
| EP0791414A1 (de) * | 1996-02-26 | 1997-08-27 | Karl Marbach GmbH + Co. | Stanz- und Formwerkzeug |
| US5755132A (en) * | 1996-02-26 | 1998-05-26 | Karl Marbach Gmbh & Co. | Punching and forming tool |
| CN111822942A (zh) * | 2019-04-22 | 2020-10-27 | 安克创新科技股份有限公司 | 装饰网的加工方法 |
| CN111822942B (zh) * | 2019-04-22 | 2022-04-29 | 安克创新科技股份有限公司 | 装饰网的加工方法 |
| CN112808858A (zh) * | 2021-01-25 | 2021-05-18 | 重庆理工大学 | 用于制作弹簧抱挎的级进模 |
| CN112808858B (zh) * | 2021-01-25 | 2022-11-15 | 重庆理工大学 | 用于制作弹簧抱挎的级进模 |
Also Published As
| Publication number | Publication date |
|---|---|
| FR2629742A1 (fr) | 1989-10-13 |
| GR3006221T3 (de) | 1993-06-21 |
| ATE81804T1 (de) | 1992-11-15 |
| ES2035619T3 (es) | 1993-04-16 |
| CA1289418C (fr) | 1991-09-24 |
| DE68903291T2 (de) | 1993-06-17 |
| FR2629742B1 (fr) | 1994-01-14 |
| DE68903291D1 (de) | 1992-12-03 |
| US4910989A (en) | 1990-03-27 |
| EP0336862B1 (de) | 1992-10-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0336862B1 (de) | Verfahren zur Herstellung einer äusseren Schrägkante an einem zylindrischen Ziehteil | |
| BE1003541A3 (fr) | Procede et appareil pour former des panneaux d'extremites de recipients. | |
| FR2563756A1 (fr) | Procede et appareil pour former un panneau de bout de recipient | |
| EP0363285B1 (de) | Leicht zu öffnende Flaschenkapsel aus Aluminiumfolie sowie Verfahren zu ihrer Herstellung | |
| FR2542224A1 (fr) | Matrice de retenue d'ebauche | |
| EP0117213A1 (de) | Vorrichtung zur Kaltverformung metallischer Werkstücke mit entgegengesetzten Axialteilen | |
| EP0310726B1 (de) | Verfahren zum Herstellen konischer Metalldosen und Werkzeug zur Durchführung des Verfahrens | |
| CA2031859C (fr) | Procede et dispositif d'emboutissage de recipients de forme tronconique, et recipient ainsi embouti | |
| FR2515885A1 (fr) | Procede de production d'une electrode composite pour bougie d'allumage et cette electrode | |
| FR2549401A1 (fr) | Procede et dispositif de fabrication de cages a poches pour roulements | |
| EP0243257B1 (de) | Verfahren zum Herstellen eines Vakuumröhresockels, ohne dass ein weiteres Abschneiden der Innenleiter nach dem Giessen notwendig ist und Vorrichtung dafür | |
| CH500024A (fr) | Procédé de fabrication de produits métalliques par emboutissage | |
| FR2631262A1 (fr) | Procede pour la production de profiles metalliques creux, et dispositif pour l'execution du procede | |
| TW202606827A (zh) | 利用沖床沖壓特殊工件之成型方法 | |
| FR2695338A1 (fr) | Procédé pour la réalisation de rangées de piqûres sur une surface d'outil destiné à présenter une fonction de râpe, et outils réalisés. | |
| EP0034977A1 (de) | Industrielles Verfahren zur Herstellung von Schmuck, insbesondere von mit eingefassten Steinen versehenen Ringen, vorzugsweise aus Edelmetall, Vorrichtung zur Durchführung dieses Verfahrens und der erhaltene Schmuck | |
| EP0337882A1 (de) | Verfahren und Vorrichtung zur Herstellung von geformten Gemüsen oder Früchten sowie geformte Gemüse oder Früchte, hergestellt nach dem Verfahren | |
| BE528289A (de) | ||
| CH380431A (fr) | Dispositif pour évider et couper des fruits avec élimination du trognon | |
| BE464669A (de) | ||
| BE517037A (de) | ||
| FR2709111A1 (fr) | Barquette métallique notamment en acier à deux compartiments et procédé de fabrication de ce type de barquettes. | |
| CH103565A (fr) | Procédé et machine pour la fabrication d'une ébauche de tube compressible et ébauche obtenue par ledit procédé. | |
| BE508433A (de) | ||
| FR2638393A1 (fr) | Procede et dispositif pour fabriquer une boite de carton a fenetre transparente, et boite d'emballage ainsi fabriquee |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE ES FR GB GR IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19900120 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: A2C GROUPE PRATIC-ADEMVA |
|
| 17Q | First examination report despatched |
Effective date: 19920318 |
|
| RTI1 | Title (correction) | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| ITF | It: translation for a ep patent filed | ||
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE ES FR GB GR IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19921028 |
|
| REF | Corresponds to: |
Ref document number: 81804 Country of ref document: AT Date of ref document: 19921115 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 68903291 Country of ref document: DE Date of ref document: 19921203 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19930331 Ref country code: LI Effective date: 19930331 Ref country code: GB Effective date: 19930331 Ref country code: CH Effective date: 19930331 Ref country code: BE Effective date: 19930331 Ref country code: AT Effective date: 19930331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19930401 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19930401 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2035619 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: FG4A Free format text: 3006221 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| BERE | Be: lapsed |
Owner name: A2C GROUPE PRATIC-ADEMVA Effective date: 19930331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19931001 |
|
| 26N | No opposition filed | ||
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19930331 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: MM2A Free format text: 3006221 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 89420120.1 Effective date: 19931110 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19980218 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19980305 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 19990503 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19991130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050331 |